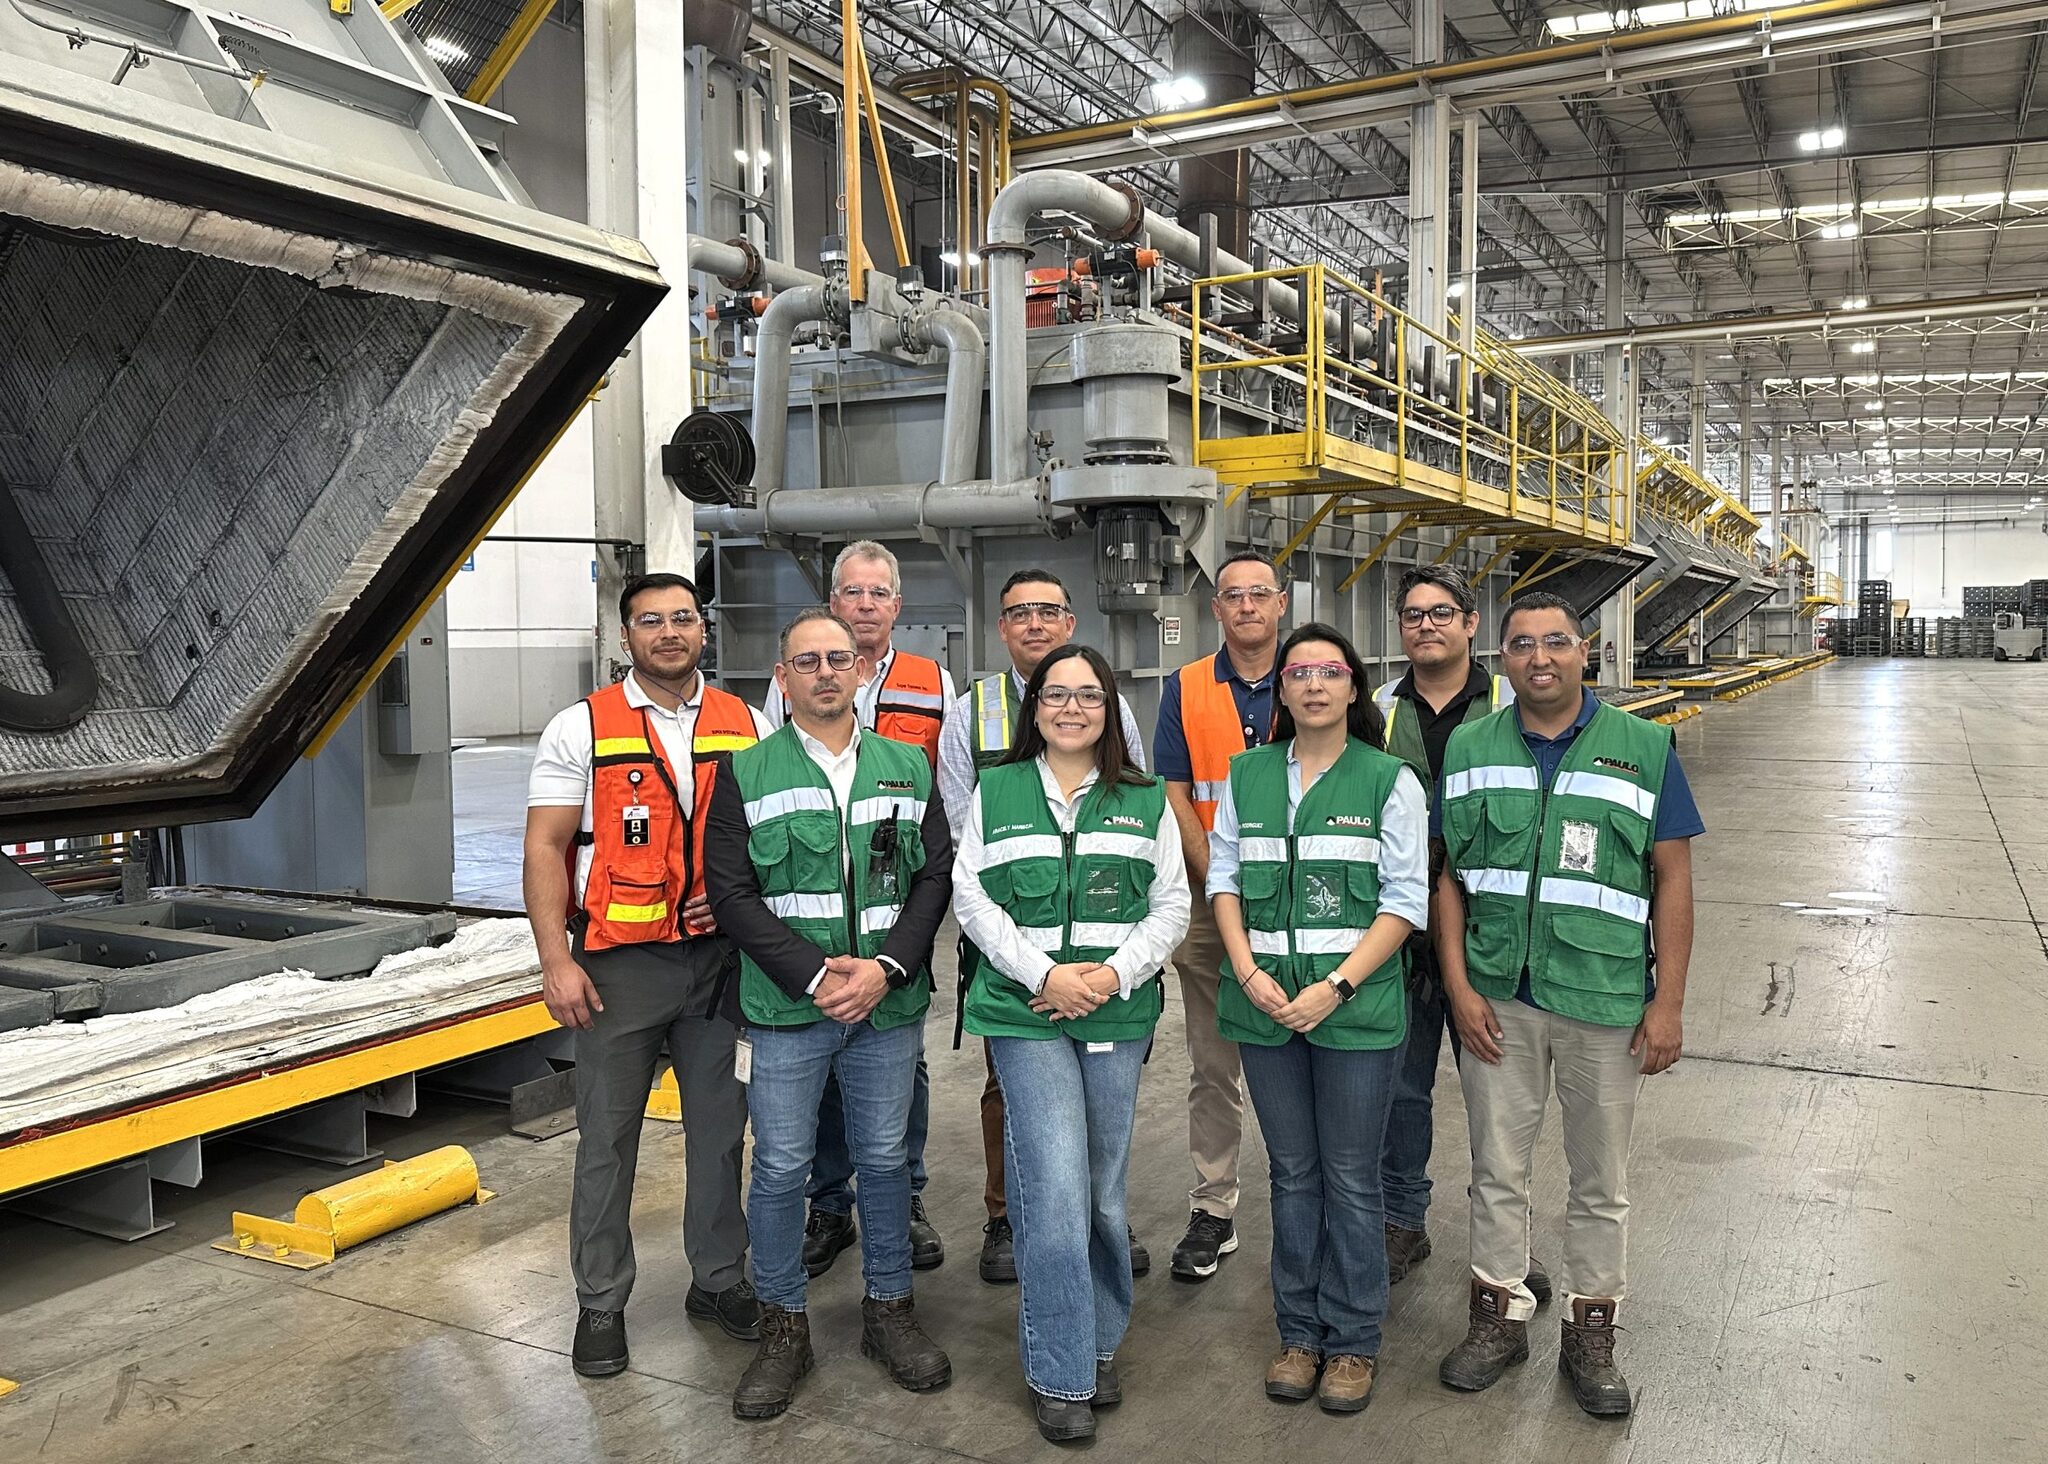
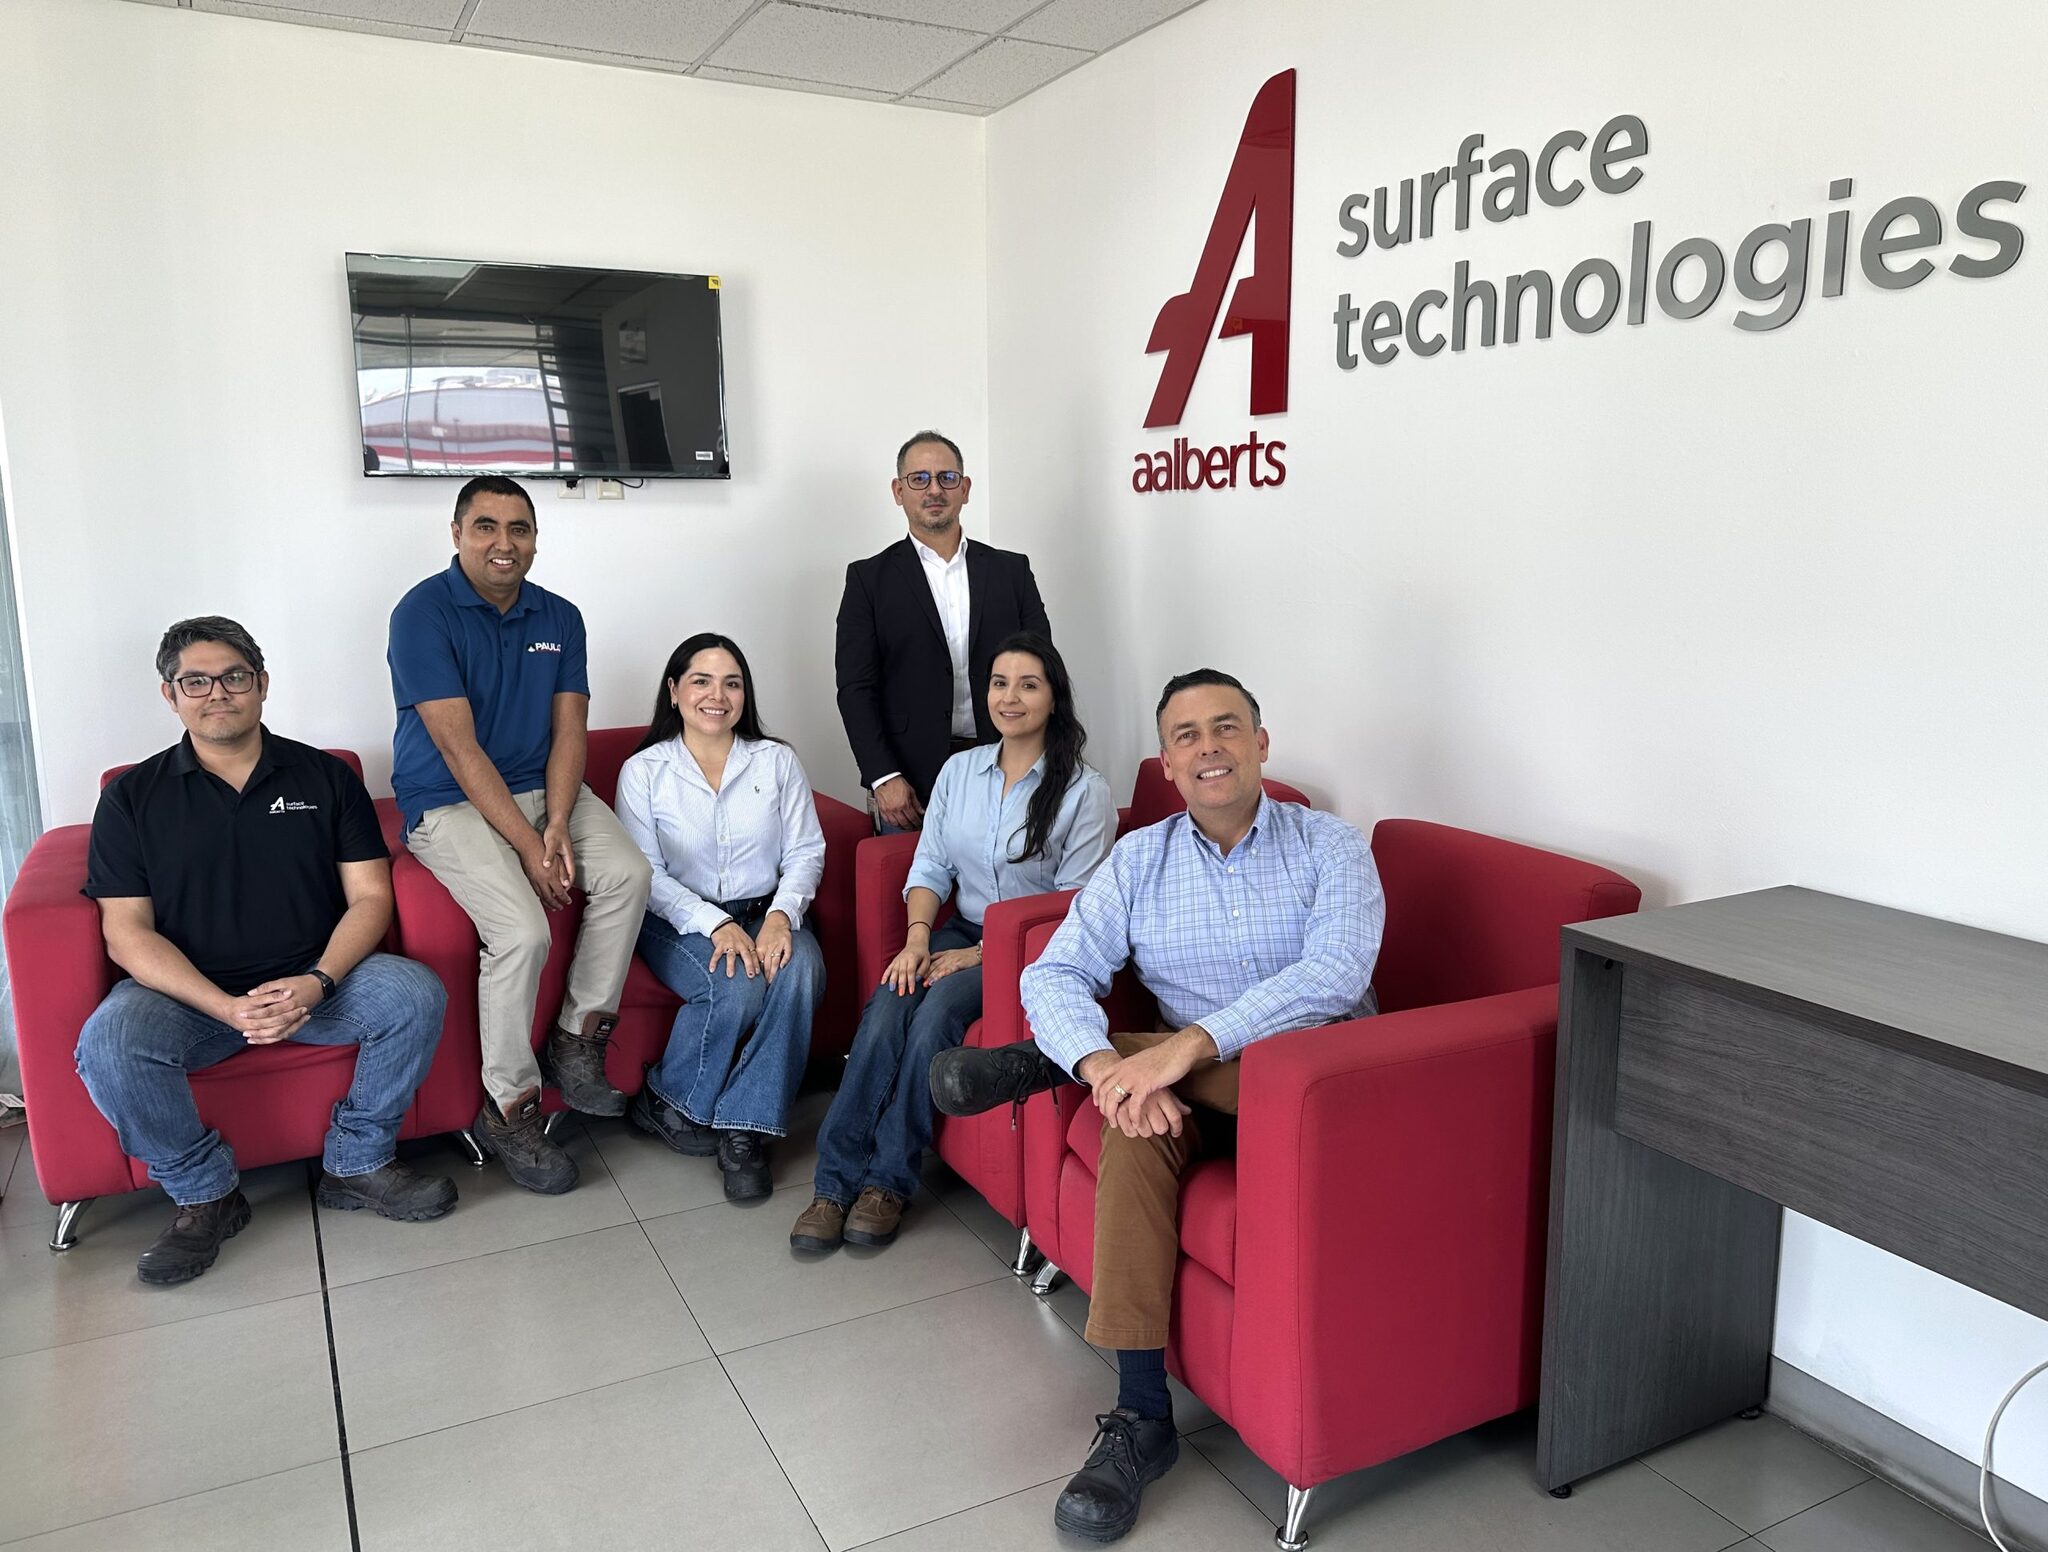
August of 2017 commercial heat treater “Paulo“(now part of global commercial heat treater Aalberts Surface Technologies) broke ground on what was originally to be a 45,000 square foot facility in Monterrey, Mexico focusing on heat treating of automotive components. April of 2018 production started and the original 45,000 square foot facility quickly expanded to 110,000 square feet.
What “The Monty Heat Treat News” saw April 13 of this year was a facility which any commercial heat treat firm would be proud to show.
“Aalberts Surface Technologies-Paulo” in Monterrey focuses on two heat treating processes, stress relieving and Ferritic Nitrocarburizing (FNC) with FNC being far and away the main focus of this plant. Both processes take place in one of 8 large, gas fired “Tip-Up” furnaces each capable of a gross weight capacity of 100,000 pounds.
As mentioned the facility is very strongly tilted towards auto parts and consequently the plant has CQI-9 and IATF 16949 certifications.
“Mr. Aldo Rodriguez“, General Director, has been with this project since the very beginning including locating the greenfield site before construction even began. “Aldo” had this to say;
“We honor and cherish the memory of “Paulo” and look forward to a very bright future under the banner “Aalberts Surface Technologies-Paulo”. With Aalberts’s backing and their impressive resources there is nothing we cannot do. We look forward to continuing to grow into new technologies and markets”.
“The Monty” looks forward to revisiting this facility in the future to see what these new markets and technologies will look like.
Left to Right;Aldo G. Rodriguez, Gerardo Carrillo (Engineering & Maintenance), Aracely Mariscal (Administration & Human Resources), Gina Rodriguez (Quality Assurance), Uriel Avila, (Production), Christian Mendez (Scheduling)
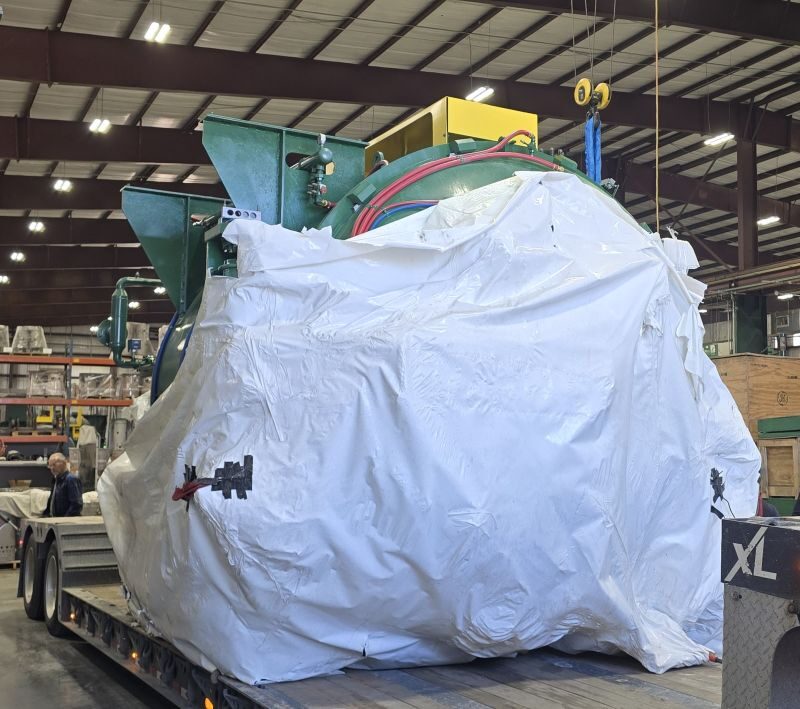
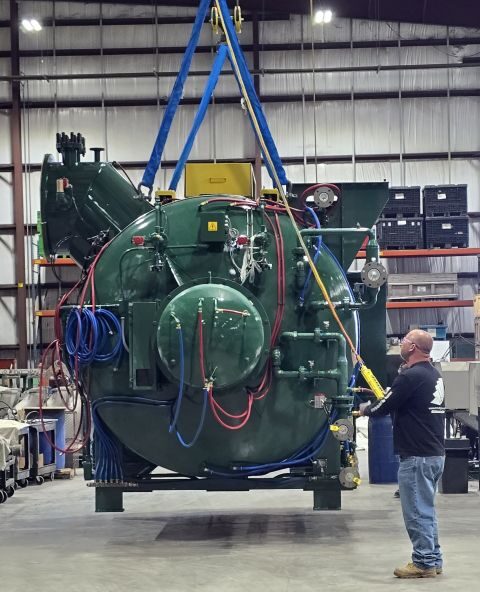
“Trinity Turbine Technology“in Rosharon, Texas, USA, a family owned turbine rebuilder has a problem which many companies would like to have, too much business for their current manufacturing capabilities. In particular heat treating has been a bottleneck-the solution? Double their heat treating capacity. The firm recently installed a new vacuum furnace provided by Ipsen of Rockford, IL, USA.
The furnace will complement their current furnaces which include a 2400F bottom loading vacuum furnace and two open air units. The new furnace can be seen in these photos taken during installation.
“About; Trinity Turbine Technology is a privately owned business that was established in 2002 by a family wanting to create a one-stop shop for all customers where they are able to receive quality work for component repair, coating, field services, capital parts and all other Turbine related needs under one roof, for ease and satisfaction. What once started as a small shop has now expanded to large corporation that has recently moved to a new 85,000 sq ft. facility. This new shop contains new and updated equipment, highly trained and skilled personnel as well as daily hands on work from the owners to ensure TTT is able to continuously provide cutting edge services and technology throughout the always advancing Turbine and Power Generation Industry. Our company prides itself on customer satisfaction, cost effective services, and innovative options by employing the top-rated personnel in each field, training with the latest technology and equipment as well as providing customers with personal contacts and around-the clock support for any and all needs they may have. Trinity Turbine Technology is also the parent company to Trinity Coatings. By having coating abilities in house, it allows for close monitoring of our processes resulting in higher levels of quality as the parts never have to leave our facility. This also aids in responsiveness, cost control, reliability and faster turn around time. We are also excited to announce Trinity Turbine Technology’s newest division, Trinity Turbine Services. Trinity Turbine Services offers outage services for our customers with Heavy Industrial Frame Gas Turbines and Steam Turbine Units during both scheduled and unscheduled outages. We have some of the most highly skilled and trained Project Managers and Field Service personnel in the industry for both Union and Non-Union projects readily available to come support all of your outage needs!”
This week“Gord Montgomery” of“The Monty Heat Treat News”will be having a close look at the state of heat treating in the Mexican market. While Mexico does boast a fledgling aerospace industry centered around Queretaro the true success story for Mexican in-house heat treaters lies in the auto parts industry and that is where are attention will be focused. Over the course of the week we will be attending“Heat Treat Mexico”being held April 14-16 in Monterrey as well as visiting a number of large in house heat treaters.-reports with photos will be provided over the course of the week.
We will leave you with this report from our last visit “
Manufacturer Brings Additional Heat Treatment in House; Danfoss Power Solutions-Queretaro, Mexico (formerly Eaton Corp) is a supplier of hydraulic solutions to the heavy equipment industry. This facility with over 500 employees entered production 8 years ago and part of their manufacturing process includes a very impressive heat treat department consisting of 9 batch IQ furnaces doing carburizing utilizing an endothermic atmosphere. The facility has one particular product line which requires a FNC process-this has always been sent out to a local commercial heat treater.
Danfoss Power Solutions-Queretaro, Mexico (formerly Eaton Corp) is a supplier of hydraulic solutions to the heavy equipment industry. This facility with over 500 employees entered production 8 years ago and part of their manufacturing process includes a very impressive heat treat department consisting of 9 batch IQ furnaces doing carburizing utilizing an endothermic atmosphere. The facility has one particular product line which requires a FNC process-this has always been sent out to a local commercial heat treater.
Gord Montgomery (The Monty Heat Treat News), César Luna González (Heat Treat Manager, Danfoss), Damian Bratcher (Director International Operations, SSi)
For a variety of reasons Danfoss in 2023 decided to bring this process in house, the reasons include faster turn around times, less inventory requirements and greater control over quality. The end result of this decision was that in 2023 the company invested in a used Ipsen vacuum nitriding system with working dimensions of 36” X 48” X 36” with a 2,000 pound capacity. Danfoss approached SSi Mexico about updating the controls, this update was just completed and testing has revealed that the metallurgical results are everything that Danfoss had hoped for.
Last week Gord and Jordan of “The Monty Heat Treat News” had the opportunity to tour this facility and what we found was an immaculate facility and the term immaculate includes the heat treat department. All heat treaters know that it is not an easy proposition keeping a facility utilizing quench oil clean but the heat treat team at Danfoss has managed this difficult task.
While the entire team at Danfoss deserves credit we should point out that the Heat Treat Production Manager, Mr. Cesar Luna Gonzales has obviously done a great job of motivating everybody in the department. Also deserving of a great deal of credit is Ms. Landy Alpizar, Metallurgical Engineer who has been involved with this project from day 1.
April 5/2026“The Monty”had an exclusive story entitled;“Boeing Invests $7 Million in 2 Bottom Loading Vacuum Furnaces”.The story made for fascinating reading for anybody in the heat treatment industry, this prompted “The Monty”to dig a little deeper into the story and get a few more details about the equipment and the order.
To this end we approached“Mr. Dave Farmery”, President of “Vac Aero” with a few questions-here are his answers;
Dave congratulations on your recent order from Boeing for two new vacuum furnaces, it must have made your day if not your year;
DF; It is a tremendous vote of confidence and a meaningful acknowledgment of our ability to design, build, and deliver mission-critical equipment to the world’s largest airplane manufacturer.”
The press release had very few technical details about the furnaces themselves. Can you share with us some information about the size of the furnaces, capacity hot zone etc?
DF; The two are:
Model VAV6060 HV-2 10^2 range 2-bar quench 60”x 60” 3000lbs all metal hot zone
Model VAV6098 HV-2 10^2 range 2-bar quench 60”x 98” 4000lbs all metal hot zone
Both systems are designed for high-performance aerospace applications and long-term operational reliability.
Why Vac Aero? Certainly I know that few vacuum furnace builders have the aerospace experience that your company has but at the end of the day the competition for this order must have been fierce. What made Boeing decide to go with your company?
DF; That’s a great question, and the answer is straightforward: decades of trust built on results. Our relationship with Boeing dates back to 1965. Over that time, we’ve developed a deep, collaborative understanding of their materials, processes, and production challenges. That experience allows us to approach furnace design not simply as an equipment supplier, but as a long-term solutions partner.
One telling example is that Boeing is still operating a Vac Aero furnace that has been running at peak performance for over 35 years. We’ve supported that system throughout its life with hot-zone replacements, control upgrades, and spare-parts support. Customer service and lifecycle support are core to how this Vac Aero grows.
Additionally, our expertise in vacuum oil quenching is truly second to none. On the service side, Vac Aero has processed more than 50,000 shipsets of Boeing landing gear, and that legacy performance was a key differentiator in this decision.
Will these be the largest bottom load vacuum furnaces Vac Aero has ever built?
DF; No, these are not the largest. We have previously built a larger system—the VAV8484 HV-2, featuring a 10² vacuum range, 2-bar quench capability, and an all-metal hot zone measuring 60” x 98”. That project further demonstrates our ability to scale furnace design to meet demanding aerospace and defense requirements.
My impression is that 2026 is shaping up to be a very good year for you, how many new furnace orders are you forecasting for 2026?
DF; 2026 is indeed shaping up to be one of our strongest years yet. Our sales pipeline is at an all-time high, and we fully expect to continue our growth trajectory. Boeing, GE, and Pratt & Whitney—customers who have trusted Vac Aero for decades—are once again returning to us for additional furnaces. Looking ahead, I see continued momentum driven by customer-focused solutions, long-term partnerships, and opportunities that extend well beyond 2026.
Who would have thought that Artificial Intelligence centers would cause new vacuum furnace orders to go through the roof? That is exactly what has been happening recently-“The Monty” has run across several vacuum manufacturers who report having received orders due to this increased demand.
AI centers requiredmassive, continuous (24/7), and highly variable power which in many cases leaves only one solution, gas turbines. The advantages of gas turbines are obvious; they can be deployed in 12-24 months and can ramp up to full power in a matter of minutes, claims which most other power sources can’t boast of.
Gas turbine manufacturers such as “Siemens”, “GE” and “Mitsubishi” all maintain large in-house heat-treating departments, primarily focused on vacuum brazing furnaces. As demand grows for gas turbines so to does the need for vacuum furnaces.
As an example of increased demand “Siemens Energy”nearly doubled its gas turbine sales from 100 units in 2024 to 194 in 2025.
Not to be outdone “Mitsubishi” is planning on doubling it’s production capacity by 2027 to meet this increasing demand.
While new gas turbines can be on line within 12-24 months the increased demand is causing a “bottleneck” in the production of new turbines with deliveries inching up to 6-8 years for some models.
A good example of a gas turbine supplier and their heat-treating requirements is “GE Gas Turbine” in Greenville, South Carolina, USA. In 2024“The Monty Heat Treat News”rated this location as the 14th largest captive heat treater in North America;“15 Largest Captive Heat Treats-North America”with a total of 16 vacuum furnaces at that time.
You will be hearing more on this subject in the near future from “The Monty”.
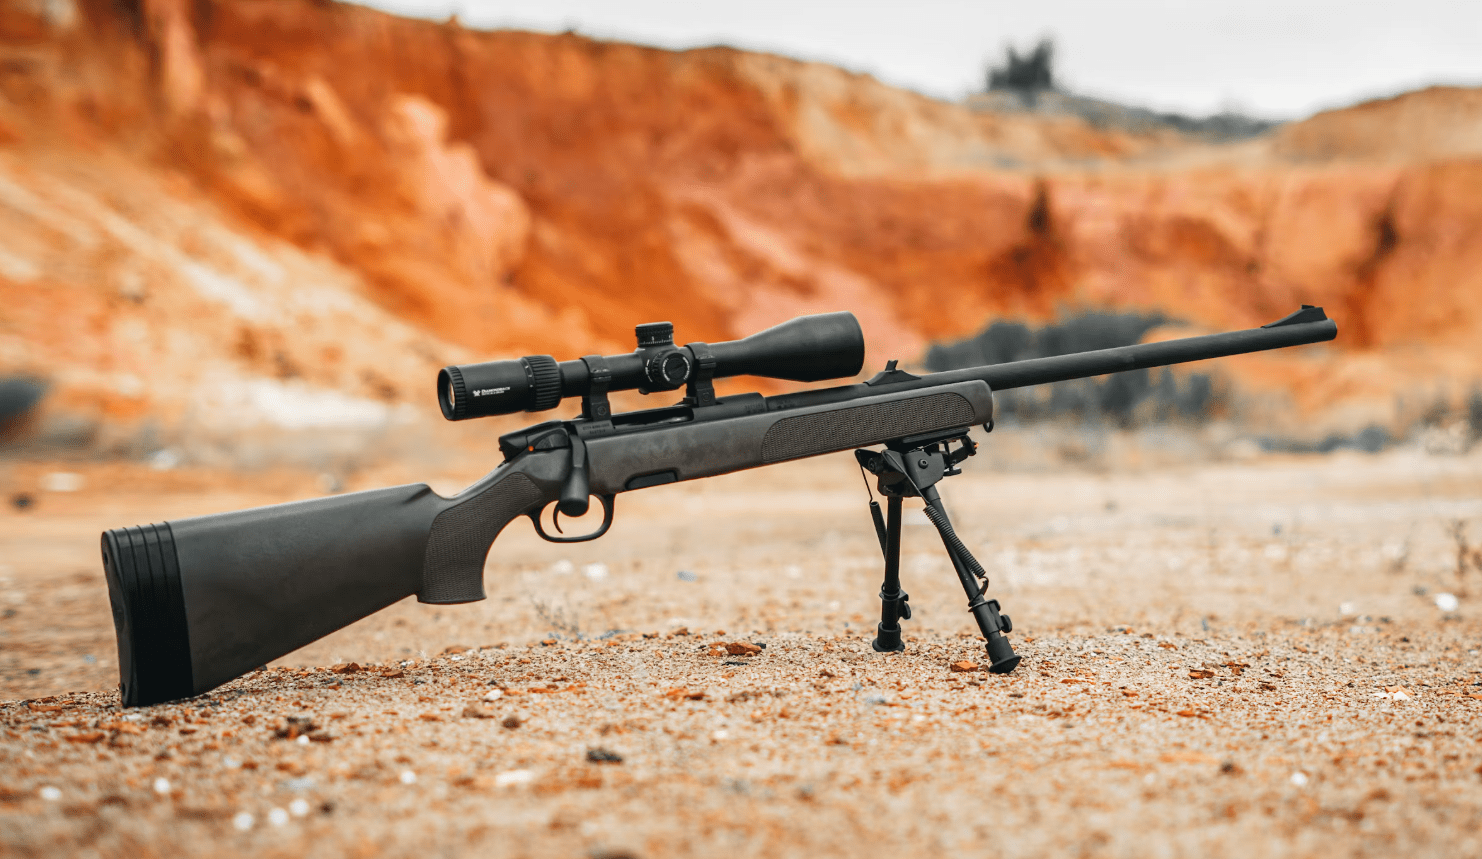
“One device instead of four. A European manufacturer from the defense sector chooses SECO/WARWICK vacuum technology;
This Partner has decided on a groundbreaking modernization of its heat treatment processes by placing an order with SECO/WARWICK for a Vector (HPGQ)vacuum furnace equipped with high-pressure gas quenching at 15 bar abs. Importantly, the selected solution will replace four separate technological installations originally planned.
Thanks to consultations and process trials conducted jointly with the SECO/WARWICK team, the Partner became convinced that all required operations can be performed in a single, versatile vacuum furnace. This translates into significant investment cost savings, simplified production and higher process efficiency.
The technology selection process was consultative in nature and included a series of technical meetings and technological trials. Initially, the customer planned to purchase a vacuum furnace with oil quenching, being convinced that only such a solution would meet their technological requirements.
The furnace will be used to heat treat components used in the production of high-precision small arms, intended primarily for the civilian market (sport shooting, hunting), as well as in versions adapted for uniformed services.
According to the original assumptions, the production process would have required four separate devices: an oil quenching furnace, a tempering furnace, a cryogenic unit and a washing system to clean parts after oil quenching.
However, a joint technological analysis conducted by SECO/WARWICK’s sales team and research and development department demonstrated that all these processes can be performed in a single device. Successful trials in a vacuum furnace with gas quenching confirmed that the proposed solution meets the customer’s technological requirements while significantly simplifying the entire production process.
“Projects like this clearly show how important technological consulting and a partnership-based approach to the customer are. Initially, several separate devices were considered, each handling subsequent stages of the process. After analysis and technological testing, it turned out that all these operations can be carried out in a singlevacuum furnace with gas quenching. This means not only substantial investment savings but also simplified production, shorter process times and reduced labor requirements. For the Partner, it is also the first step toward modern vacuum processes and moving away from the atmospheric technologies previously used,”said Maciej Korecki, Vice President of the Vacuum Segment at SECO/WARWICK.”
“Solar Atmospheres, the largest American-owned heat treater in the United States, is proud to support NASA’s Artemis II mission. Our expertise spans thermal processing of raw materials, nickel-based tubing, and critical aerospace components—playing a vital role in bringing next-generation space technology to life. At the core of some of these components is the 6Al–4V titanium Launch Abort System (LAS), one of the most complex safety systems ever engineered.
The LAS aboard the Orion spacecraft functions as a rocket capable of outrunning another rocket in an emergency. In the event of a catastrophic launch anomaly, its manifold enables the abort motor to ignite and safely propel the crew module away from the rocket. Designed to endure extreme conditions with zero margin for error, the LAS represents the pinnacle of aerospace safety and performance. Solar Atmospheres is honored to contribute to this mission-critical technology, providing the precision, reliability, and advanced thermal processing that space exploration demands.”
Welcome to the April, 2026 edition of“The Monty Heat Treat News” for 30 years the most up to date heat treatment industry news source on the planet. Some news and trends we are following in this edition include these;
Our news section is always complimented by a very complete and up to date list of quality surplus heat treatment equipment. As few recent additions include these;
As always the entire team at “The Monty” looks forward to your thoughts and comments. Sincerely, Gord, Jordan & Dale Montgomery.
“The Monty Heat Treat News” is part of WG Montgomery Ltd., a family owned business serving the heat treatment industry since 1969. We can be reached at 705 259-3650. [email protected]
Advertising inquiries can be addressed to; Jordan Montgomery, [email protected]
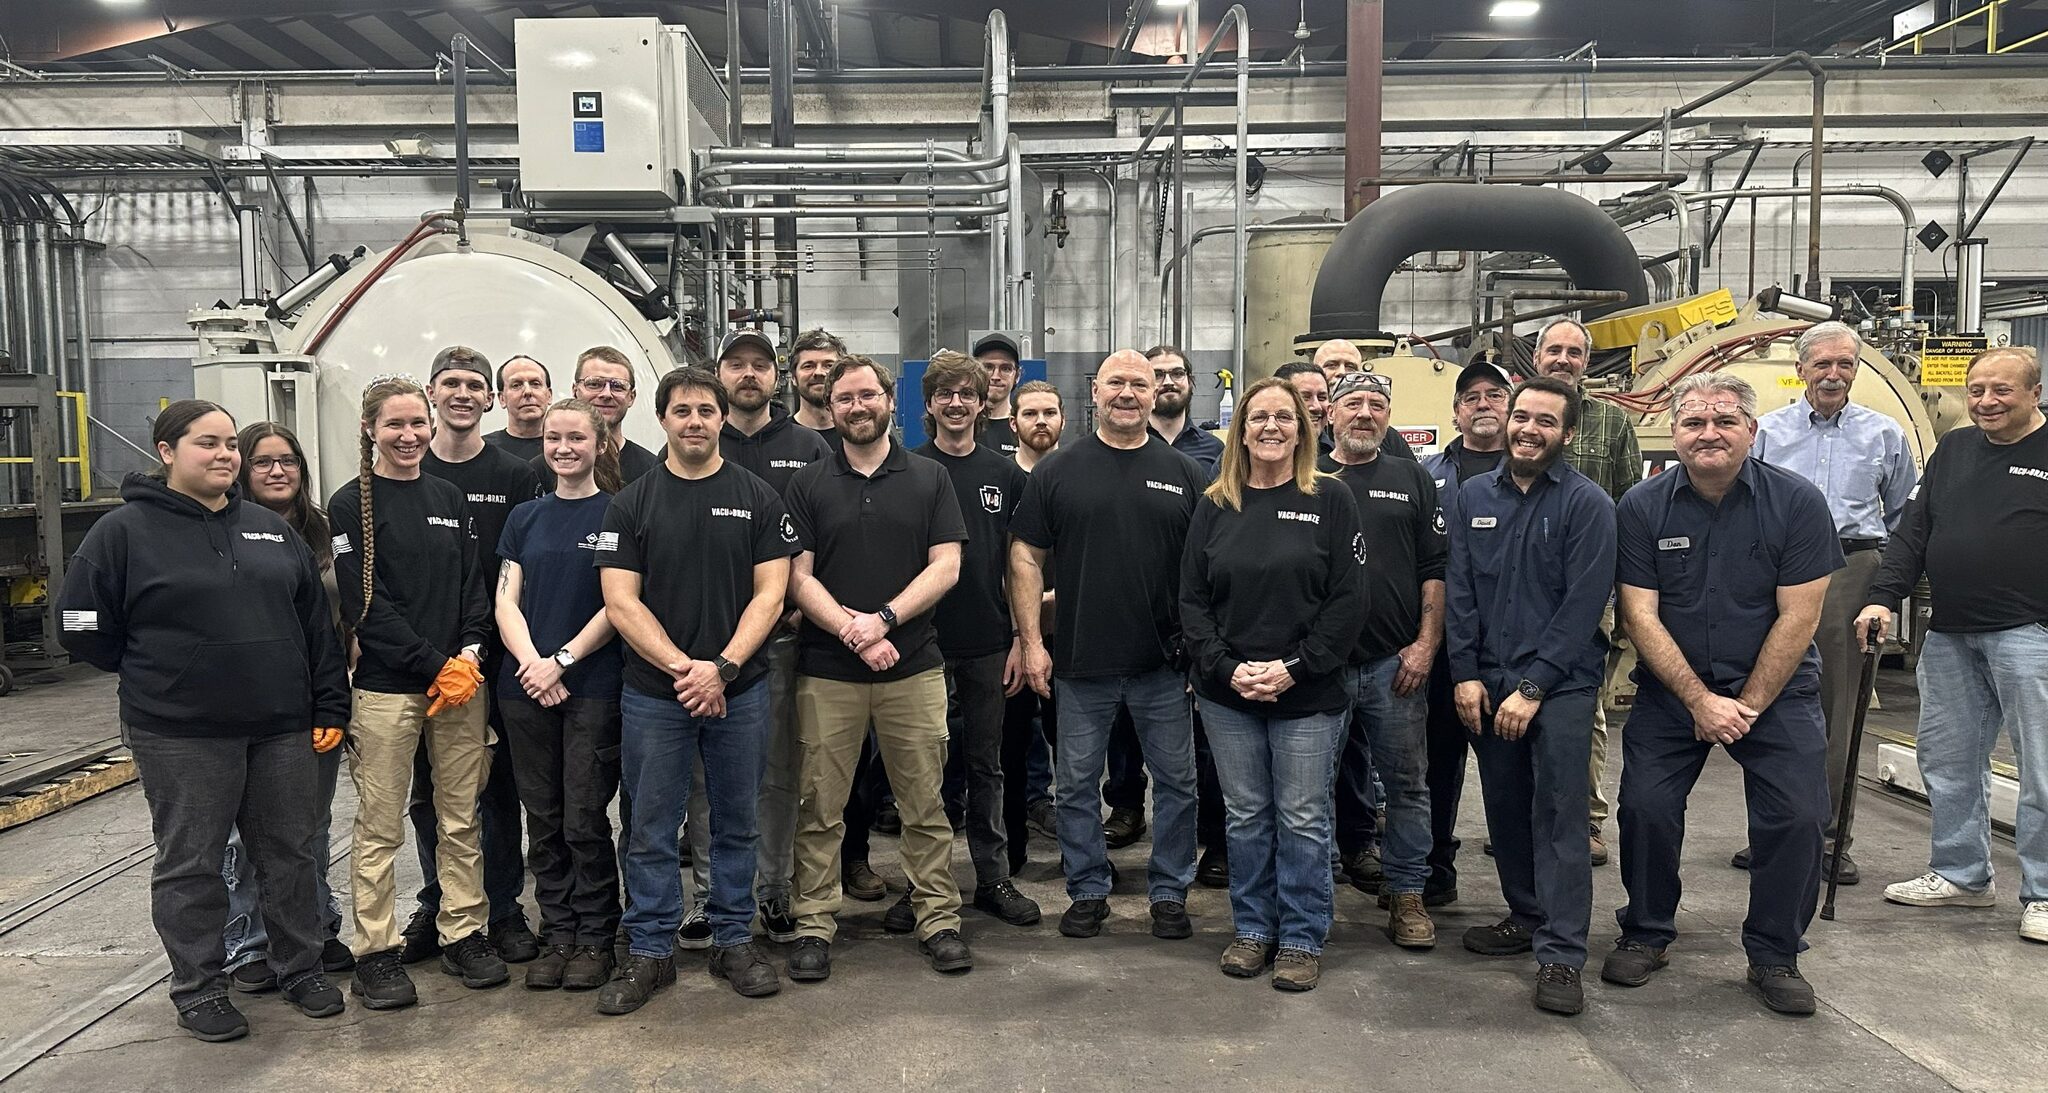
In 2025 commercial heat treater “Vacu Braze”of Quakertown, PA, USA was named as one of the “52 Largest North American Commercial Heat Treaters” by “The Monty Heat Treat News”. In spite of this very impressive achievement the firm is not “sitting on their laurels”, rather this achievement seems to have spurred the company on to even bigger and better things-“Gord Montgomery” of “The Monty” was able to witness first hand some of these new investments just last week.
Founded in 1981 by “Mr. Ralph Puerta”(who remains on the board of directors) the company has followed a fairly typical path followed by most commercial heat treaters in that from rather humble beginnings the company has invested and grown over the years to their current size which includes over 40 employees in an almost 60,000 square foot building (we do feel compelled to add that while this path is common for many commercial heat treaters, few are as successful at it as Vacu Braze).
While the name “Vacu Braze” suggests a facility focused almost entirely on vacuum work this is not entirely the case. It is certainly true that the company has a very impressive number of vacuum furnaces (24 at last count with up to 12 bar quenching) but it also boasts a number of atmosphere furnaces, complimented by several nitriding furnaces.
While “Vacu Braze” has been successful for a number of reasons, a top one is that the company has chosen to service what are “growth” industries these days, Defense, Medical and Power Generation-all industries showing robust growth these days. To be able to service these industries “Vacu Braze” has NADCAP, AS9100 and ISO 13485 certifications.
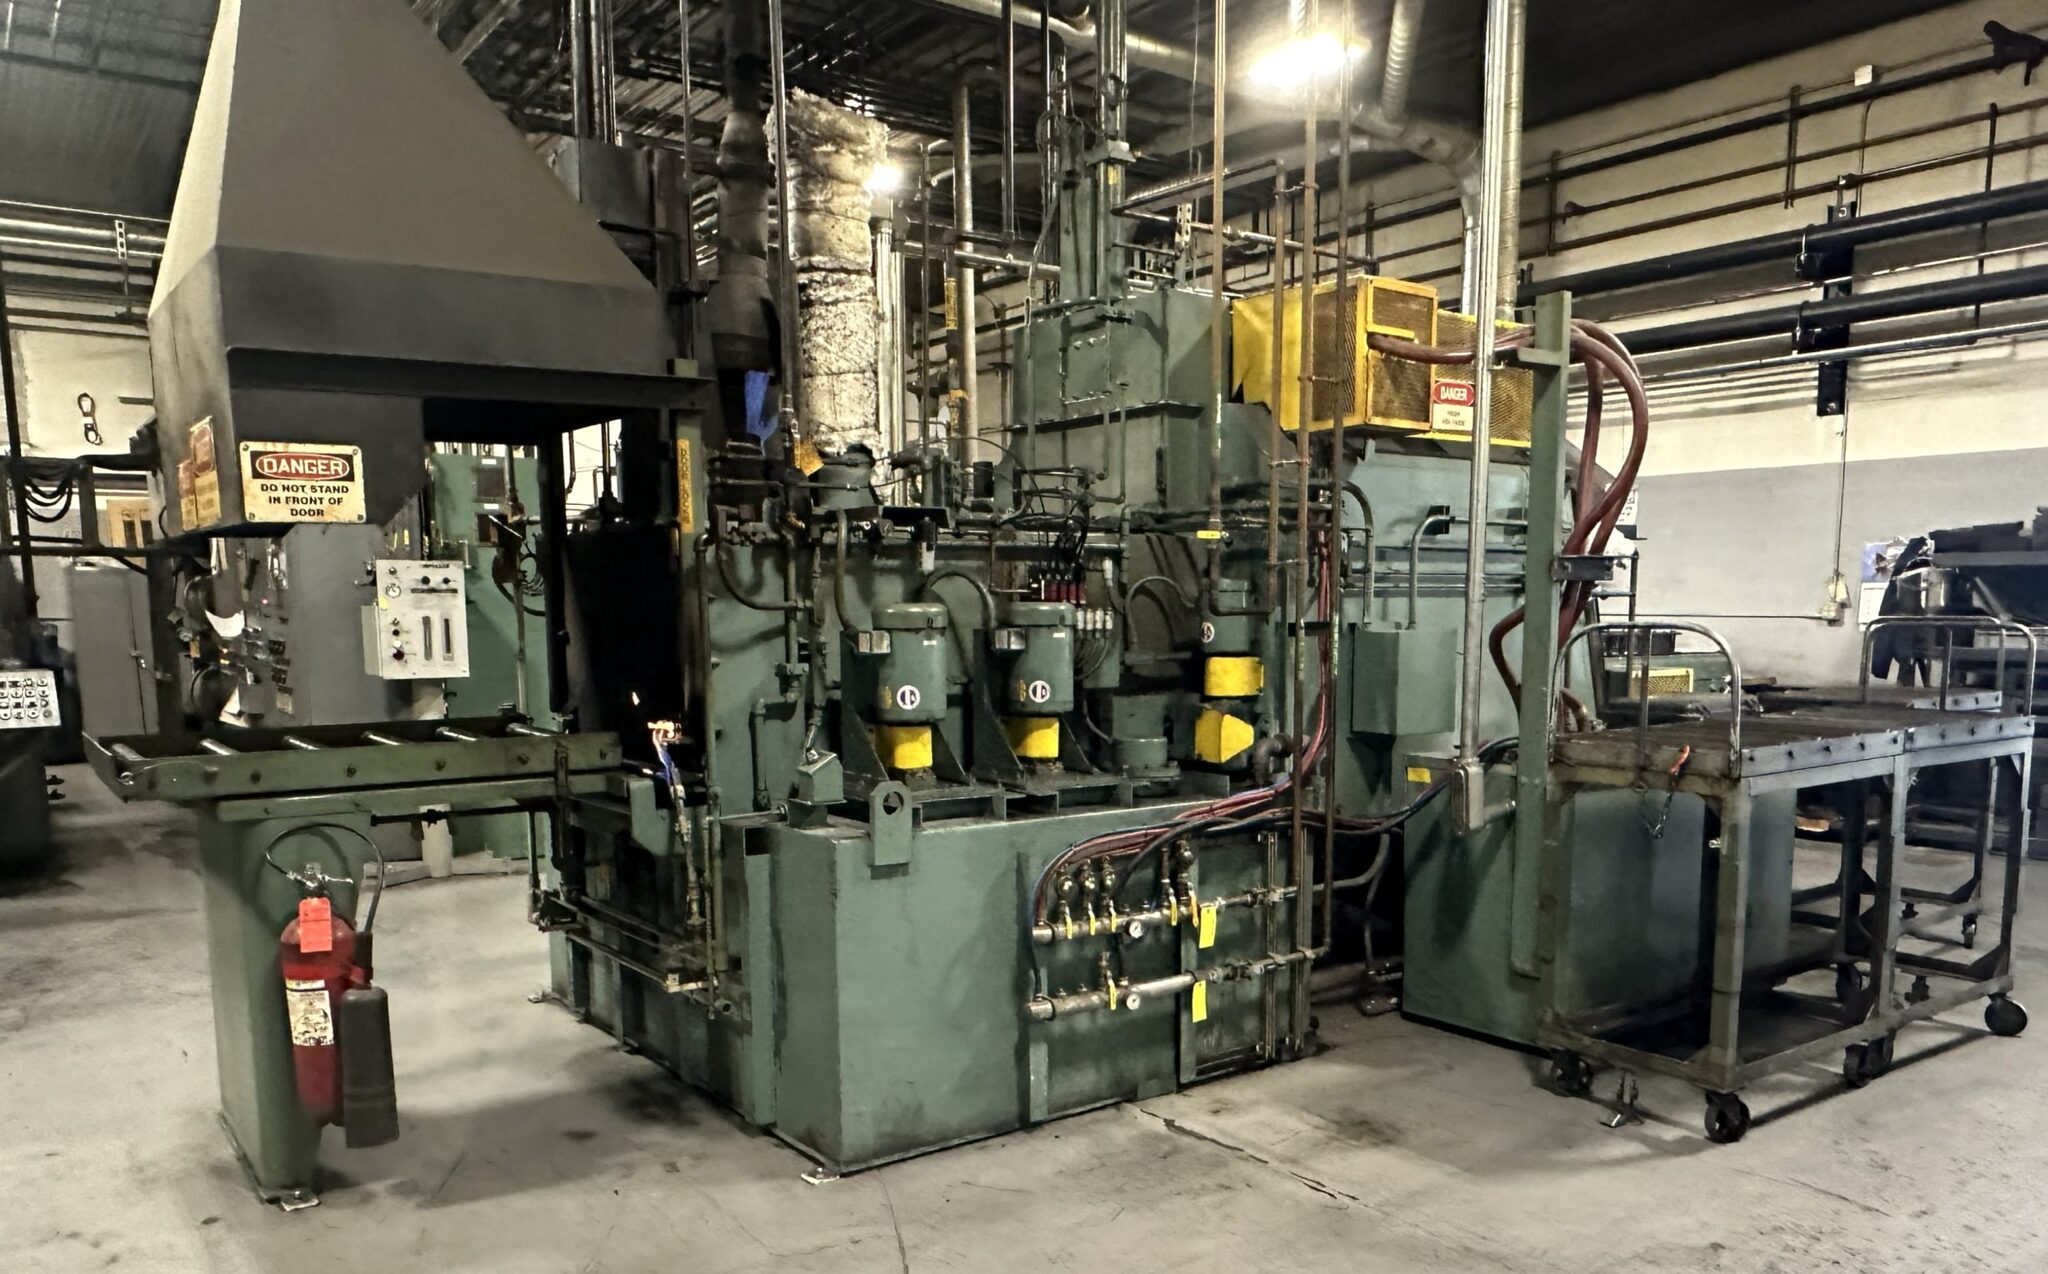
New Pit Nitrider
“Vacu Braze” saw a change of management in 2026 with “Mr. Kirk Palermo”, who has 20 years’ experience in the industry taking the position of President earlier this year. As previously mentioned, the founder of the company “Mr. Ralph Puerta” has moved on to the board of directors. Ralph has this to say about Kirk’s new position;
“I can’t be prouder of the job Kirk has done over the years for this company. He has shown initiative, ambition and incredible foresight, all of which has lead the company into a very strong growth position”.
In the introduction to this story, we spoke about the firm making major investments in 2026. One obvious one is the brand new 18,000 square foot addition. Another one is the addition of a new pit, gas nitriding system with working dimensions of 48″ X 108″ deep-a photo of which is included in this press release. What we have not mentioned is the fact that the company has also made very impressive investments in other thermal processing systems-investments which we have to mention down the road a bit. Look forward to an update of this story.
Gord Montgomery Kirk Palermo
Kirk Palermo, Ralph Puerta
(Editors Note; February 19th of this year “The Monty” had a news story entitled “North American Furnace Builder Changing Sales Direction”. In this story we spoke about how furnace builder “Aichelin” has been making changes to their outside sales network. According to this press release the firm recently hired “Mr. Damon Bizuka” formerly with vacuum furnace builder “Furnacare” to handle their sales efforts in the US southeast.Formerly this area was covered by the very competent team at independent sales rep firm “CF Thermal”). “Aichelin Americas welcomes Damon Bizuka as Business Development Manager – Southeast.
In this role, Damon will be responsible for supporting customers across Virginia, Tennessee, Mississippi, North Carolina, South Carolina, Alabama, Georgia, and Florida, focusing on the sale of:
• Large, custom-engineered heat treatment systems
• Advanced automation solutions
• Equipment rebuilds, modifications, and relocations
• Products and projects across the full Aichelin Americas portfolio Damon brings over a decade of experience in technical sales, sales engineering, and business development, with deep expertise in vacuum furnaces, metallurgy, and complex engineered systems. His background includes successfully growing new territories and delivering strong results in highly technical, consultative environments.”
 August of 2017 commercial heat treater “Paulo“(now part of global commercial heat treater Aalberts Surface Technologies) broke ground on what was originally to be a 45,000 square foot facility in Monterrey, Mexico focusing on heat treating of automotive components. April of 2018 production started and the original 45,000 square foot facility quickly expanded to 110,000 square feet.