

Did you like this article? Click here to subscribe to The Monty.
View our recent magazines and podcasts by clicking the following link. https://themonty.com/magazine/

Did you like this article? Click here to subscribe to The Monty.
View our recent magazines and podcasts by clicking the following link. https://themonty.com/magazine/


 THIS IS ANOTHER EXAMPLE OF A MANUFACTURER OFFERING COMMERCIAL HEAT TREATING AND TIES IN WITH OUR STORY ABOUT TRANSMISSION SUPPLIER TREMEC OFFERING COMMERCIAL HEAT TREATING
Over the years “The Monty Heat Treat News” has had the privilege of visiting two locations of Captive/Commercial heat treater Kern Liebers Schramberg, Germany and Queretaro, Mexico-visits which resulted in an article in 2018 entitled “Do Manufacturers Make Good Commercial Heat Treaters”. The original article is further down in its entirety but to quickly sum up Kern Liebers is a German manufacturer who heat treat their own products in house but who also offers commercial heat treating at 6 of their global locations, a combination which is reasonably rare and even rarer is the fact that they seem to make money from it.
In addition to the notes below “The Monty Heat Treat News” has also mentioned the company when they installed a new vacuum nitriding system from German furnace builder Rohde, a picture of which can be found here.


The company makes our news section today for the fact that they continue to flourish and a result is this brand new addition to the Queretaro, Mexico plant. What you see here is an IVA Schmetz, high pressure nitrogen quenching furnace with working dimensions of 36” X 36” X 72” which just arrived last week. This furnace will join 2 vacuum nitriders, a large pit furnace and several other styles of furnaces all dedicated to both captive and commercial heat treating.
“MAY 13/2019 QUERETARO, MEXICO; Kern Liebers is a company which intrigues us as they seem to be that very rare of breeds, a company which successfully combines manufacturing with captive and commercial heat treating. Recently they have been promoting themselves with press releases such as this combined with a photo of the plant in Mexico. “We present the two plants KERN-LIEBERS MEXICO in the state of Queretaro. One of them is dedicated to the production of stampings, stampings and heat treatments, while the other is focused on springs. More than 540 employees work in these facilities of 22.400 square meters of extension, where we offer amenities such as a gym for the exclusive use of employees and their families, among others.” To go with this news item we include our original news item from a few months ago along with a photo of part of their heat treating department.
“OCTOBER 2018 PRESS RELEASE; Do Manufacturers Make Good Commercial Heat Treaters? Kern Liebers; Generally our opinion is that manufacturers who have in house heat treating capacity make poor commercial heat treaters for a wide variety of reasons. However having said that we very recently visited a manufacturer who for years now has been offering commercial heat treating from their in house heat treating departments and has been very successful at it. KERN-LIEBERS is a medium-sized family owned company based in southwest Germany who specializes in the production of highly complex strip and wire parts and assemblies. The KERN-LIEBERS group of companies develops and manufactures precision products at over 50 locations around the world and currently 6 of these locations have in house heat treating capacity which offer commercial heat treating.
Two weeks ago we visited the Schramberg, Germany location which has the ability to offer Gas Nitriding, Nitrocarburizing – also of stainless steels, case hardening, carburizing, austempering and vacuum hardening. One look at the equipment tells us why the company is successful at commercial heat treating, it is new and varied In addition as Kern Liebers services a number of different industries they have a wide variety of certifications including IATF 16949 and CQI9 to name a few. While a majority of the heat treat capacity is dedicated to their own products by sales volume, the commercial heat treating side of the business is substantial and contributes a significant part on it. It is important to note that while the company probably did not set out to be a commercial heat treater they certainly treat it as an independent profit center with worldwide heat treatment .
Mrs. Li Haas [email protected] is working for the sales department in Germany, who is connected to all the heat treatment teams of the other locations. Other locations offering commercial heat treating include China – Taicang near Shanghai and Tianjin near Beijing, India – Tumkur near Bangalore, Czech Republic – Budweis, and Mexico – Querétaro . While many of the processes are duplicated in the various locations some such as Plasma Nitriding is only available in one location (Taicang/Tianjin, China) or Induction Hardening which is only available in India and the Czech Republic. As we speak the company is making major investments in many of their plants, including two new pit furnaces from Rohde Furnaces in Germany-one for the Mexico location and another for the Czech Republic. Rohde is also in the process of installing 2 new vacuum nitriding furnaces in Mexico. Rohde has already equipped all worldwide Kern Liebers plants with either pit or chamber furnaces. Other planned additions include more of an emphasis on nitriding capacity especially in China and especially as it relates to heat treating of stainless steels. So while we feel that most captive heat treaters do not make a good commercial heat treater we can point to Kern Liebers and say; “here is a company that manufactures a very good product and is also a darn good commercial heat treater.”
Did you like this article? Click here to subscribe to The Monty.
View our recent magazines and podcasts by clicking the following link. https://themonty.com/magazine/


 THIS IS ANOTHER EXAMPLE OF A MANUFACTURER OFFERING COMMERCIAL HEAT TREATING AND TIES IN WITH OUR STORY ABOUT TRANSMISSION SUPPLIER TREMEC OFFERING COMMERCIAL HEAT TREATING
Earlier this year we had an exclusive news item about how Additive Manufacturing firm Burloak Technologies was installing a brand new in house heat treating department at their Burlington, Canada facility. We can now say that this AS9100 and Nadcap compliant facility is now in operation and in a very interesting development also taking on commercial heat treatment business for vacuum, air, solution and T6/aging cycles. We say interesting because generally captive heat treaters do not make good commercial heat treaters although there are exceptions-Gleason Works in Rochester, NY, USD is a good example of a company successfully blending captive and commercial heat treating. Having said that the individual in charge of the department at Burloak, is a former Schaeffler Bearings employee and a very experienced fellow with a great deal of knowledge of both captive and commercial heat treating.
The Canadian commercial heat treating market (which largely means the province of Ontario) is in a real state of flux these days. Bluewater Thermal, one of the largest commercials in the country closed their Ontario facility just last year and another large commercial will be removing a great deal of capacity at the end of the year. While other commercial heat treaters are investing in more equipment the sum total means a reduced amount of heat treating in the province in the future.
July 9 2020. “Burloak Technologies Installing In-House Heat Treatment Department; In Burlington, Ontario, Canada we find Burloak Technologies who describe their company thusly; “Burloak Technologies is Canada’s leading supplier of highly engineered additive manufactured components for demanding applications.” https://burloaktech.com/ The company makes our news section today due to the fact that for months, if not years the company has been planning their brand new, state of the art in house heat treating department and just this week one of the first pieces of equipment arrived-a new Titan vacuum furnace from Ipsen in Rockford, Illinois, USA. Installation and Nadcap qualification are the next steps. Future plans are very ambitious to say the least, with several more large pieces of equipment on order, this includes a furnace for processing aluminum. Additive manufacturing is proving to be a rapidly growing market for furnace manufacturers, already this year we have announced several large heat treatment investments in the field and we would expect this will grow rapidly in the future.”
Did you like this article? Click here to subscribe to The Monty.
Surplus heat treat equipment? Click here for a free appraisal and our help in selling it.


Pleasant Prairie, WI – August 26, 2024 – PAI Industries, renowned manufacturer and distributor of high-quality parts to the heavy duty truck industry, has partnered with ECM to bring heat treatment in-house with a NANO vacuum furnace system. Adding to the already impressive 112,000 ft2 manufacturing facility with state-of-the-art machinery in Suwanee, GA, and exemplary outsourced heat treating, this in-house system expands PAI’s capabilities to expedite production and increase capacity.
Transitioning from primarily out-sourced heat treatment to in house vacuum technology, they will be able to perform low pressure carburizing and through-hardening 24/7 – thanks to the modularity of the ECM NANO system, an external loader, 3- position temper oven & queuing positions. Additional benefits provided by vacuum technology include: no IGO, zero CO2 furnace emissions, no fire hazards/open flames, increased repeatability, and improved metallurgical results. Prior to project acceptance, testing was conducted in the ECM NANO located in the ECM USA Synergy Center (Pleasant Prairie, WI) to further validate improved metallurgical properties.
Visit us online to learn more about ECM Vacuum Furnaces (www.ecm-usa.com) and PAI Industries (www.paimanufacturing.com).
About PAI Industries. PAI Industries manufactures and distributes quality service parts to the heavy-duty truck industry. For over 50 years, we’ve been supplying distributors throughout the world. PAI owes its remarkable success to its dedicated and knowledgeable employees. With decades of experience designing and field-testing products, both our Engineering and Sales Staff are available to answer your most challenging technical questions. As proud US manufacturers, PAI’s commitment to its customers is evidenced by maintaining the highest levels of quality for the products and services we provide. Quality, continual improvement, and customer satisfaction are the personal responsibility of every PAI employee.
About ECM Technologies. ECM Technologies is an innovative low pressurevacuumfurnacemanufacturerwith headquarters in Grenoble, France. With subsidiaries and ventures around the world, including ECM USA located in Pleasant Prairie, Wisconsin USA. ECM’s global presence is well known in the automotive, aerospace, nuclear, energy, electronic, induction and 3D additive industries. With such versatile product lines and service capabilities, ECM is the ideal furnace system supplier for heat treatment processes ranging from rapid thermalprocessing(RTP) to low pressure vacuum carburizing (LPC). Our service capabilities include advanced automation, robotics, after sales, spare parts, on-site training and more.
Did you like this article? Click here to subscribe to The Monty.
View our recent magazines and podcasts by clicking the following link. https://themonty.com/magazine/

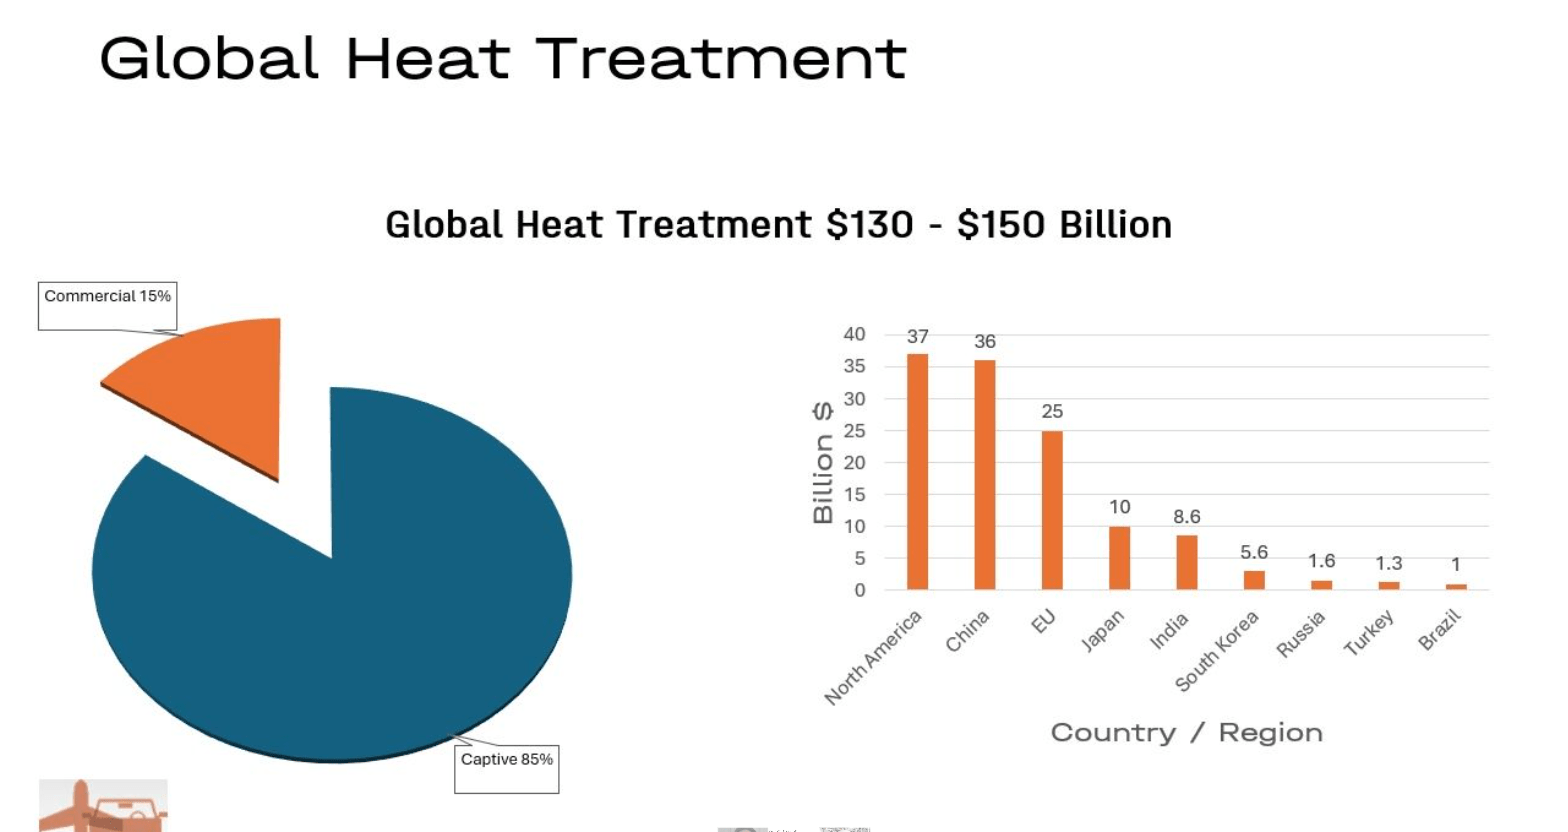
- Asia Pacific Market accounts for 44% or US$47bil
- USA at 22% or US$ 24bil
- Rest of the World (ROW) at 34% or US$36bil
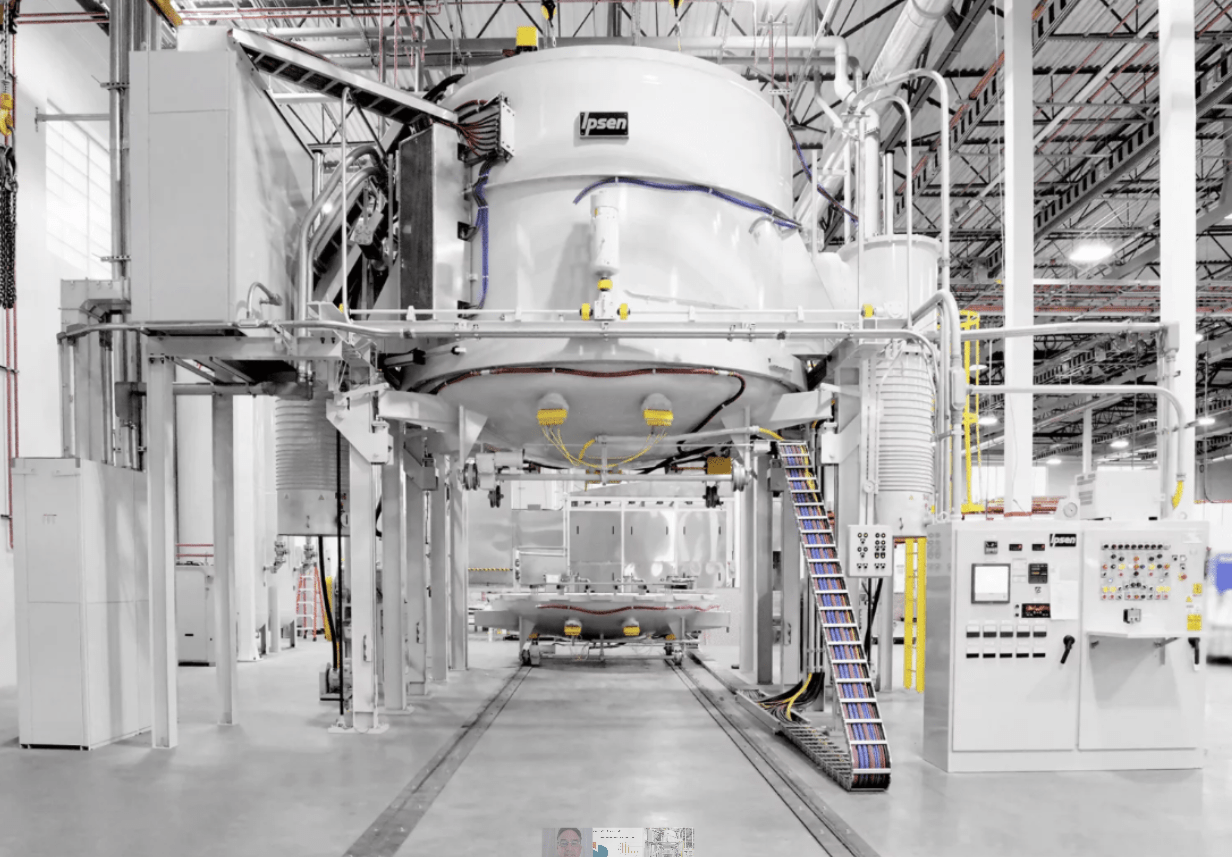
When you walk into a heat-treating department and see your first vertical vacuum furnace, you’d be forgiven for staring openly at the jaw-dropping sight.
There, perched a story or more in the air on metal legs, is a gigantic vacuum pressure vessel. Wires and hoses, pumps and controls—all attached at various angles—could draw comparisons to science-fiction icons like the Iron Giant or the alien spacecraft from H.G. Wells’ War of the Worlds. They are magnificent machines. Awe inspiring. And, most importantly, very useful.
Looking Closer – Why Buy a Vertical Vacuum Furnace?
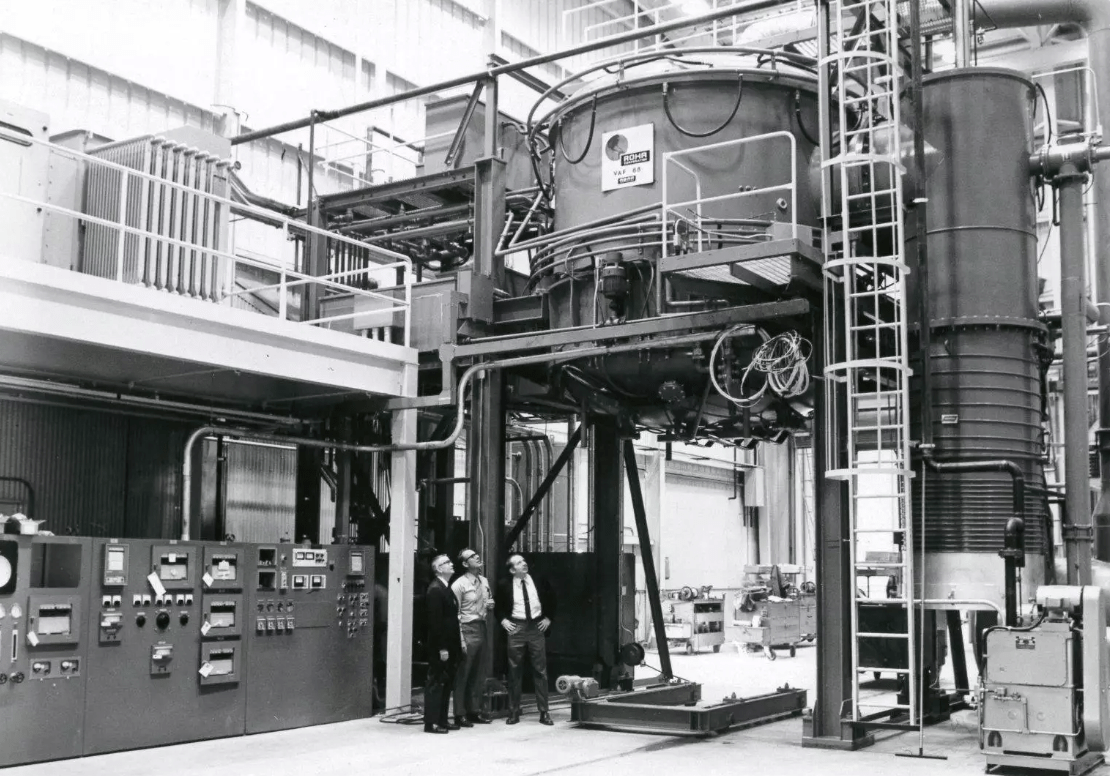
While these furnaces could do just about everything their horizontal counterparts could do—annealing, carburizing, hardening, tempering, etc.—the vertical furnaces could uniquely handle delivering heat and quenching with a high level of control for very large or very long cylindrical parts with varying thicknesses. Picture a cross-section of an aircraft fuselage, or the engine nozzle of an orbital rocket.
“Heat-treaters were looking for more capacity out of a furnace in one load. Trying to load a part that’s big or deep into a horizontal furnace becomes a problem,” added Jim Grann, Ipsen’s Technical Director. “When you have a piece that’s six feet in diameter and 25 feet deep, how do you load and unload that into a horizontal furnace?”
Bottom loading vertical vacuum furnaces allowed huge pieces like this to be sitting flat on the hearth or suspended from the top on a jig within the hot zone. This allowed engineers to take advantage of the geometry of the whole diameter of the chamber, not be restricted by the cross-section width of the pressure vessel at different elevations above the hearth like they might in a horizontal furnace.
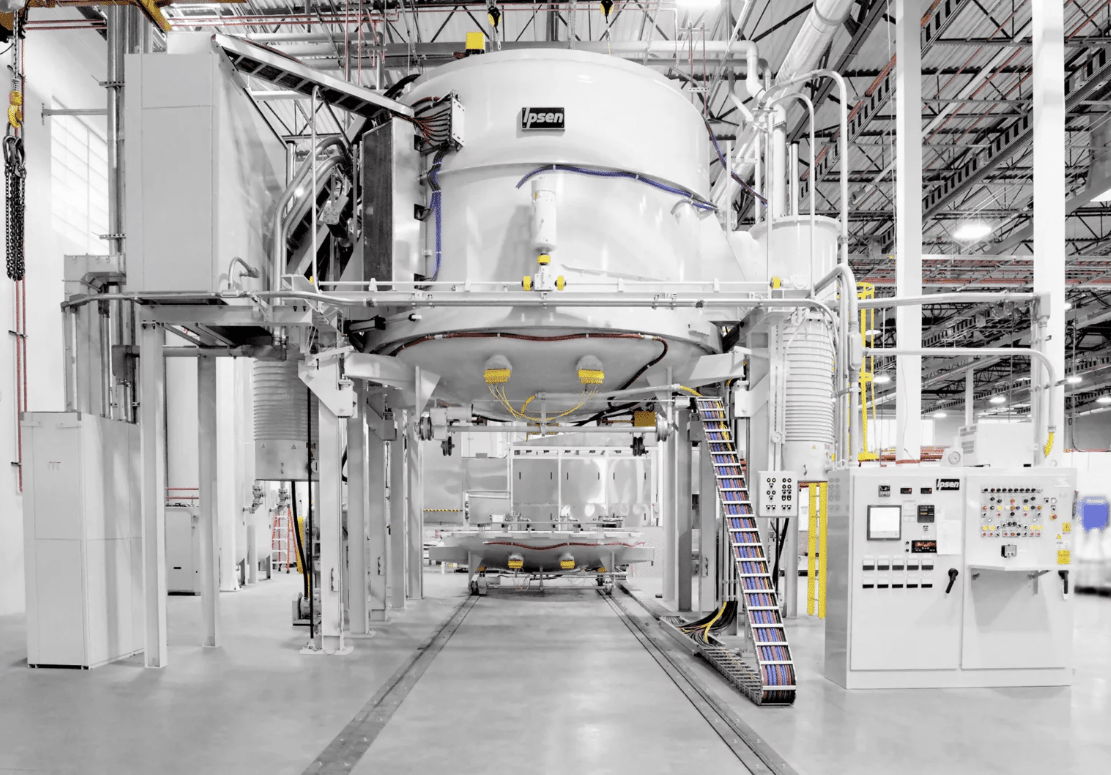
“When it comes to handling these large parts, vertical vacuum furnace owners are often able to rely on existing overhead crane infrastructure for loading and unloading parts onto the hearth mounted on the traversing bottom head,” Heninger explained.
“Compare that to a horizontal furnace that would require a loader with long forks feeding these gigantic pieces deep into the hot zone. Ensuring the forks remain rigid and parallel over a long travel distance to place the load without colliding with hot zone elements can be expensive,” Grann added. Buying or building a loading system that can handle that rigidity over a long span can add significant cost to the expense of the setup. Storing such a loader when not in use further adds to the overall footprint.
Looking for More – Beyond Big Parts
Not everyone who buys a vertical vacuum furnace has a constant stream of gigantic parts, however. “We had an assumption that we changed about three years ago. We believed that people would buy these vertical furnaces so that people could put big parts into it. Now, we see users building fixtures with big round plates on it like a pizza oven,” Grann explained of the trend. The demand to handle smaller parts between orders for the larger piece work drove systemic innovation in fixture design. In addition to the multi-tiered platforms, basket systems and hanging racks took advantage of the larger usable overall volume available in a vertical vacuum furnace for parts with strange dimensions.
“This demand to use fixtures to handle smaller parts changed the way we looked at the design of the control zones,” Grann noted. Due to the demand in the aerospace industry for accurate temperature readings and process monitoring, additional positions for thermocouple monitoring within the designs of vertical vacuum furnaces made managing processes that handled parts with a wide range of geometries at the same time possible.
“Even though a vertical furnace may be very tall, a lot of the mass of the parts may be at the bottom of the chamber, with the hearth and the fixture,” Heninger explained. “Customers may run a partial load with parts only going so far up into the chamber. So you’re more likely to see top and bottom elements and ring elements for better temperature control throughout the chamber.”
Companies in global locations where ground square footage was at a premium looked at vertical furnaces as a way to build upwards instead of outwards, reducing the footprint of each furnace while maintaining the capabilities of handling large workloads.
Look Out Below: What Are Top-Loading Vertical Furnaces?
A rarer counterpart to the bottom-loading vertical vacuum furnace, Ipsen’s VTL top-loading furnace also emerged as a solution for incredibly long parts. “Top-loaders and bottom-loaders are distinct furnace types. Top-loaders excel at handling exceptionally long components, such as tubes exceeding 300 inches in length,” said Heninger.
Sometimes lowered into a pit beneath ground-level, these furnaces could handle hardening massive driveshafts for everything from big trucks to oceangoing vessels. “For a top-loader, you need an area for the furnace, but then you also need an area for the part to be lowered into the furnace,” said Heninger.
Imagine gargantuan pistons the size of semi-trailers pushing camshafts that run the entire length of a ship. For every ship that crosses the ocean, each piston and shaft requires heat treatment. In those cases, top-loading vertical vacuum furnaces can often be the solution.

A Critical Eye – When Not to Select a Vertical Furnace
“Vertical furnaces are flexible, but that doesn’t mean that they’re a universal solution,” explained Janusz Kowalewski, Ipsen’s Sales Director for Southeast Asia. Most notably, hot zone maintenance is more complicated when your technicians need to be a story or two above the shop floor to replace consumable parts. There are extra considerations that come with managing the human interface—ladders, catwalks and handrails. And, of course, the height of the facility’s roof will limit the size of the furnace. “One cautionary tale taught installers and riggers to be mindful of the location of the overhead crane, so that it doesn’t get stuck on the wrong side of a vertical furnace or lose half of its travel span,” Kowalewski recalled.
Fixtures in a vertical vacuum furnace tend to be more elaborate to take advantage of the space, and typically cost more than what is used in a horizontal furnace. And while bottom-loading furnaces may take up less floor space while operating, there are still additional space demands. “Bottom-loading vertical furnaces still need space for the hearth to drop down and move away from the base of the furnace for loading and unloading the parts payloads,” Kowalewski noted.
“Also, recipes for vertical and horizontal are not necessarily interchangeable. Moving a process from a horizontal machine to a vertical machine may require a recertification of the process before production can continue,” Grann added.
Looking Ahead – Vertical Vacuum Trends
“While traditionally, we’ve seen clients using our vertical vacuum furnaces for annealing and brazing parts, requiring only a 2-bar quench, aerospace companies are starting to approach us for higher pressure quench solutions,” Heninger observed. “We have started to see more demand for 6-bar up to 15-bar furnaces from aerospace companies and we’re building more of these as the demand increases.”
What Ipsen has seen over the years is a tendency for customers who buy one vertical vacuum furnace to add more to their fleet over time. Once the maintenance team is trained, the recipes are approved, the fixtures and procedures are in place, and the orders start coming in, the demand for vertical vacuum furnace production remains strong.
Did you like this article? Click here to subscribe to The Monty.
View our recent magazines and podcasts by clicking the following link. https://themonty.com/magazine/
