ECM USA is pleased to announce the appointment of Marco Möser to Senior Sales Engineer for the Western U.S., reinforcing our dedication to meet increasing demand for advanced vacuum furnace technology across the United States. With more than 25 years of experience in the heat treatment industry, Marco brings extensive expertise in supporting OEMs on large-scale automotive programs (ex. 8/9/10-speed transmission programs). His strong technical expertise and analytical approach position him to play a key role in advancing ECM USA’s sales strategy and enhancing customer success.
Prior to joining ECM USA, Marco held senior leadership roles, including Sales Director and Vice President, for specialized alloy fixturing and foundry organizations across Europe and the Americas. Throughout his career, he has demonstrated a consistent ability to drive sales growth, optimize performance, and strengthen team collaboration.
Marco’s professional background includes multiple executive-level positions, as well as, completion of an Executive Development Program at The Wharton School in Philadelphia, further underscoring his leadership capabilities and strategic insight.
Solar Atmospheres is pleased to announce the installation and full commissioning of a new 10-bar vacuum furnace at its Fontana, California facility, further expanding the company’s high-pressure vacuum heat treating capabilities in the western United States.
The furnace, manufactured by sister company Solar Manufacturing, is a state-of-the-art horizontal vacuum system featuring a 48” wide x 48” high x 96” deep hot zone and a maximum load capacity of 12,000 pounds. Equipped with an advanced vacuum pumping package capable of achieving an ultimate vacuum level of 1×10⁻⁶ Torr, the system is ideally suited for processing titanium and other high-performance alloys that require exceptionally clean, tightly controlled vacuum environments.
“This investment gives our customers another regional solution for high-pressure quenching of large components and heavy workloads,” said Derek Dennis, President of Solar Atmospheres California. “It also allows us to drive greater efficiency and cost competitiveness through increased capacity and economies of scale. This addition reflects our continued commitment to innovation, quality, and delivering measurable value to our customers.”
The new furnace strengthens Solar Atmospheres’ ability to support aerospace, defense, medical, and power generation markets with advanced vacuum heat treating technology and reliable turnaround performance.
For more information about vacuum heat treating services at Solar Atmospheres, visit solaratm.com, or contact Frank Trujillo at 866-559-5994 ext. 1333, or [email protected].
“Metlab Heat Treat” inWyndmoor, PA, USA at the time had the largest commercially available pit carburizing furnaces in North America and because of this they drew customers from as far away as Mexico and Canada. For some reason this capacity has never been replaced and to this day “The Monty” still fields inquiries from gear manufacturers from all over North America looking for a carburizing source for large gears and shafts.
Our most recent inquiry came from a manufacturer looking for a commercially available heat-treating source in the Chicago area who could carburize parts12′ long X 38″ diameter with a weight of roughly 14,000 pounds. Our search turned up several possibilities in the area but none had the combination of length and diameter required;
“Hi-Hard Rolls”, Harvey, IL , parts up to 37″ diameter X 150″ long.
“General Surface Hardening”, Chicago, IL. Large pit carburizing furnace.
“Overton Gear” , Chicago, IL. Up to 80″ diameter X 100″ deep, 20,000 pounds
At the end of the day the customer went with commercial heat treater “Worldwide Heat Treat”, in Houston, Texas who as far as we can tell has the largest commercially available pit carburizing furnaces in North America with several pit furnaces, the largest having working dimensions of 100″ diameter X 144″ deep and capable of 60,000 pound loads.
It’s interesting that there is such a difference between North America and Europe when it comes to large component carburizing capabilities. We at “The Monty” put this down to the fact that pit furnaces are far more common in Europe than North America and also the presence of so many ‘windmill” manufacturers in Europe which require enormous gears. This has encouraged commercial heat treaters to install furnaces capable of handling these components.
Whether their is enough large gear heat treating requirements in North America to justify the enormous expense of installing a pit furnace capable of handling 100,000 pound parts is debatable but when some North American gear suppliers are forced to source their heat treating requirements to Europe it certainly suggests there is a business case to be made for this investment.
One of the world’s best known aircraft manufacturers recently placed an order for multiple vacuum furnaces. This multi-million-dollar order has been placed with a North American vacuum furnace builder with delivery expected towards the end of 2026. There will be a formal announcement at an upcoming press conference April 2 and “The Monty Heat Treat News” will be in attendance to provide all the details.
Today “The Monty Heat Treat News” digs deep in our “Heat Treat Podcast” archives to find one of our most popular discussions. In this episode our host “Carlos Torres” speaks with “Mr. Trevor Jones”, President of one of the largest vacuum furnace builders in North America “Solar Manufacturing”.
Job Title: Vice President of Sales
Location: Remote-based, with enterprise-wide responsibility for revenue performance across all BWTS operations, including the Houston, TX facility and six (6) additional industrial facilities in PA, MI, IN, and IL.
Role Overview
The Vice President of Sales is the senior commercial executive accountable for revenue growth, margin discipline, and forecast accuracy across BWTS. This role owns the end-to-end sales function—strategy, execution, pipeline management, and talent development—ensuring the business delivers consistent, predictable performance aligned with private equity growth objectives.
The VP of Sales partners closely with the CEO, executive leadership, and operations to translate market opportunity into executable sales plans, scalable processes, and measurable results. This is a hands-on leadership role requiring direct involvement in strategic accounts and critical deals while building a disciplined, repeatable sales engine.
Core Responsibilities
Revenue & Growth Accountability
Own company-wide revenue performance, including new business, existing account growth, pricing discipline, and margin protection.
Develop and execute annual and multi-year sales plans aligned with EBITDA targets and investment thesis.
Drive consistent pipeline generation and conversion to ensure forecast accuracy and revenue predictability.
Identify and pursue strategic growth opportunities, including new markets, customer segments, and service expansion.
Sales Strategy & Execution
Establish clear sales strategy by facility, market, and customer segment, aligned with operational capacity and capital priorities.
Lead and close complex, high-value opportunities and serve as executive sponsor for key accounts.
Ensure pricing, quoting, and commercial terms align with profitability targets and operational constraints.
Monitor competitive dynamics and market trends to proactively adjust strategy.
Process, Forecasting & Controls
Own CRM discipline, pipeline governance, and standardized sales reporting across the organization.
Deliver accurate forecasts with clear upside/downside risk visibility.
Implement and enforce consistent sales processes to support scalability and diligence-readiness.
Partner with finance to support budgeting, variance analysis, and performance tracking.
Leadership & Organizational Development
Build, lead, and hold accountable a performance-driven sales organization.
Set clear KPIs, expectations, and compensation alignment tied to revenue, margin, and cash outcomes.
Coach and develop sales talent while identifying gaps and succession needs.
With the Executive Team, work to drive cross-functional alignment between sales, operations, quality, and technical teams to ensure execution.
Executive & Board Engagement
Serve as the primary commercial voice in executive leadership discussions.
Present clear, data-driven updates on revenue performance, pipeline health, and market conditions.
Support private equity stakeholders with transparency, rigor, and credibility in reporting and planning.
Represent BWTS with customers, partners, and industry stakeholders at the executive level.
Qualifications & Experience
Proven success leading sales growth in industrial manufacturing or technical services environments.
Demonstrated ability to build predictable revenue engines in multi-site or multi-region businesses.
Strong track record closing complex, long-cycle, high-value deals.
Experience operating in PE-backed or similarly performance-driven environments strongly preferred.
“Retech, a SECO/WARWICK Group company, has announced the sale of two customized Vacuum Induction Melting (VIM) casting systems to a long-standing overseas partner supporting power generation turbine manufacturing.
The two systems, engineered to support equiaxed (EQ) and directionally solidified (DS) casting processes, will be used in the production of high-performance, nickel-based alloy turbine components. These casting technologies are critical for achieving the structural integrity, thermal resistance, and performance consistency required in modern power generation turbines operating under extreme conditions.
Both VIM systems are based on Retech’s proven core designs but incorporate customer-specific modifications, underscoring the company’s commitment to delivering fully customized solutions rather than off-the-shelf equipment. In this case, Retech engineered tailored feeder configurations to align with the customer’s established production practices, enabling efficient, repeatable casting while maintaining precise thermal and atmospheric control throughout the process.
“Customization is central to how we approach every project,” said Earl Good, Retech President. “These systems were designed to build on prior installations while incorporating specific changes requested by the customer to support their current and future production goals.”
The order represents a continuation of a decades-long relationship between Retech and the customer, dating back to the 1980s. Several legacy Retech furnaces installed at the facility remain in active operation today, a testament to the durability, serviceability, and long-term value of Retech equipment. The customer has indicated plans to further expand capacity in the coming years, including additional system purchases and the replacement of older furnaces.
With a global installed base and deep expertise in vacuum melting, casting, and refining technologies, Retech continues to support critical industries, including power generation, aerospace, and advanced materials, by delivering reliable, high-precision solutions tailored to each customer’s application.”
Recently “The Monty Heat Treat News” has had several news items about the UK heat treatment market, unfortunately many of them have been rather depressing as they mention tales of closures and bankruptcies. However this item is more positive in that it announces the acquisition of a commercial heat treat facility, a facility which at one point boasted of having the first commercially available 10 bar vacuum furnace in the entire UK.
We start off this story with a profile of the company by “The Monty” which appeared on our site back in 2013, it is followed by the announcement of the acquisition and who the purchasing party is;
“MARCH 11, 2013;Lush Heat Treatment/UK. So is captive and commercial heat treating any different in the UK than anyplace else in the world? We all know the answer which is that heat treating around the world is pretty much the same everywhere you go. Just to make sure though we at “The Monty “are visiting several locations around the country this week and our first stop was at a commercial heat treater by the name of Lush Heat Treatment Ltd., Birchwood Industrial Estates, Hatfield, Herts, UK. http://lush-heat.co
What we saw was a medium sized commercial operation, family owned which was started back in 1952 and is currently run by George Lush son of the founder. While this company can provide batch carburizing, gas nitriding and vacuum heat treatment it is pretty plain the direction the company is going, vacuum heat treating for the aerospace industry. Lush was the first commercial operation in the UK to offer 10 bar quenching and in addition to this furnace and a few others has a fairly recent TAV bottom loading vacuum furnace with 6 bar nitrogen/argon quenching. In our opinion this is not a large company but very well organized, very clean and with technology and certification (such as Nadcap) which is surprising in a company of this size. In the photos below you see the TAC furnace and in front Mr. George Lush, Matt Cross (SSI UK) and Gord Montgomery.”
“MARCH 17 2026; BRATTLEBORO, Vt.–(BUSINESS WIRE)–G.S. Precision (“GSP” or the “Company”), a leading manufacturer of complex, highly engineered products used in mission critical aerospace, defense, and semiconductor systems, has completed two transactions that significantly expand the Company’s unique capabilities and provide for strategic platform expansion. The Company has acquired Lush Heat Treatment LTD (“Lush”) and the assets of Headwater Precision (“Headwater”).
“These acquisitions support our platform growth strategy and vision to be the most trusted global partner in precision manufacturing and assembly of highly engineered mission critical products, recognized for our commitment to innovation and quality,” said James R. Callan, Chief Executive Officer of GSP. “We welcome the addition of these distinctive capabilities, which include advanced coating and specialized heat treat technologies to enhance our customers’ success. Our acquisition process and partnership with AE Industrial brings an enhanced experience for family/founder companies; honoring their history, expert teams, and industry knowledge while leveraging our own unique family culture that emphasizes deep respect of those relationships.”
Founded in 1952 in Hatfield, United Kingdom, Lush is an industry leading provider of vacuum and endothermic processing and brazing services for the aviation space, nuclear and defense sectors. Lush will be integrated into GSP subsidiary F.T. Gearing Systems, a supplier of precision submicron gear systems to the aerospace and defense sector.
GSP has also acquired the assets of Headwater, which include high precision manufacturing assets, including state of the art robotics, laser, CNC, and advanced coating technologies.”
Vacuum Furnace Builder Ipsen USA based in Rockford, IL has appointed Mr. Matt Clinite VP of Sales. For almost 12 years Matt has worked with Ipsen in a variety of sales positions. Very recently Matt was appointed to the top sales position with the company, VP of Sales a position in which we at “The Monty” believe he will do a tremendous job. In the group photo Matt is second from the right.
“Burloak Technologies Inc, Oakville, Ontario, Canada, has completed its most recent Nadcap audit, supporting the use of the company’s heat treatment capabilities in demanding sectors.
Burloak’s Ontario facility also offers standalone specialized thermal processing, including:
Hot Isostatic Pressing (HIP)
Vacuum heat treatment
Ageing, tempering & stress relieving
Solution/anneal & quench for aluminium alloys
Thermal cycles for aluminium, stainless steels, titanium, Inconel alloys, etc
Beyond these thermal processing solutions, the company also offers metal Additive Manufacturing services. The company works within the aerospace, space, defence, oil & gas, automotive and medical sectors. In addition to Nadcap certification, Burloak holds AS9100 and ISO 17025 accreditations. It is also registered with Canada’s Controlled Goods Program (CGP).”
For more on this captive/commercial heat treater “The Monty Heat Treat News” has this exclusive background story;
“MARCH 17, 2021; Burloak Technologies Completes In House Heat Treating Department; Over the course of this year we have watched with interest as additive manufacturing firm Burloak Technologies in Burlington, Ontario, Canada has developed their in house heat treating department. With the addition of their new Quintus Technologies Hot Isostatic Press (pictured below) the installation is now complete. This by the way is the first commercial HIP unit available in Canada.
“September 14, 2020 Burloak Technologies Installing In-House Heat Treatment Department; Earlier this year we had an exclusive news item about how Additive Manufacturing firm Burloak Technologies was installing a brand new in house heat treating department at their Burlington, Canada facility. We can now say that this AS9100 and Nadcap compliant facility is now in operation and in a very interesting development also taking on commercial heat treatment business for vacuum, air, solution and T6/aging cycles. We say interesting because generally captive heat treaters do not make good commercial heat treaters although there are exceptions-Gleason Works in Rochester, NY, USD is a good example of a company successfully blending captive and commercial heat treating. Having said that the individual in charge of the department at Burloak, is a former Schaeffler Bearings employee and a very experienced fellow with a great deal of knowledge of both captive and commercial heat treating.”
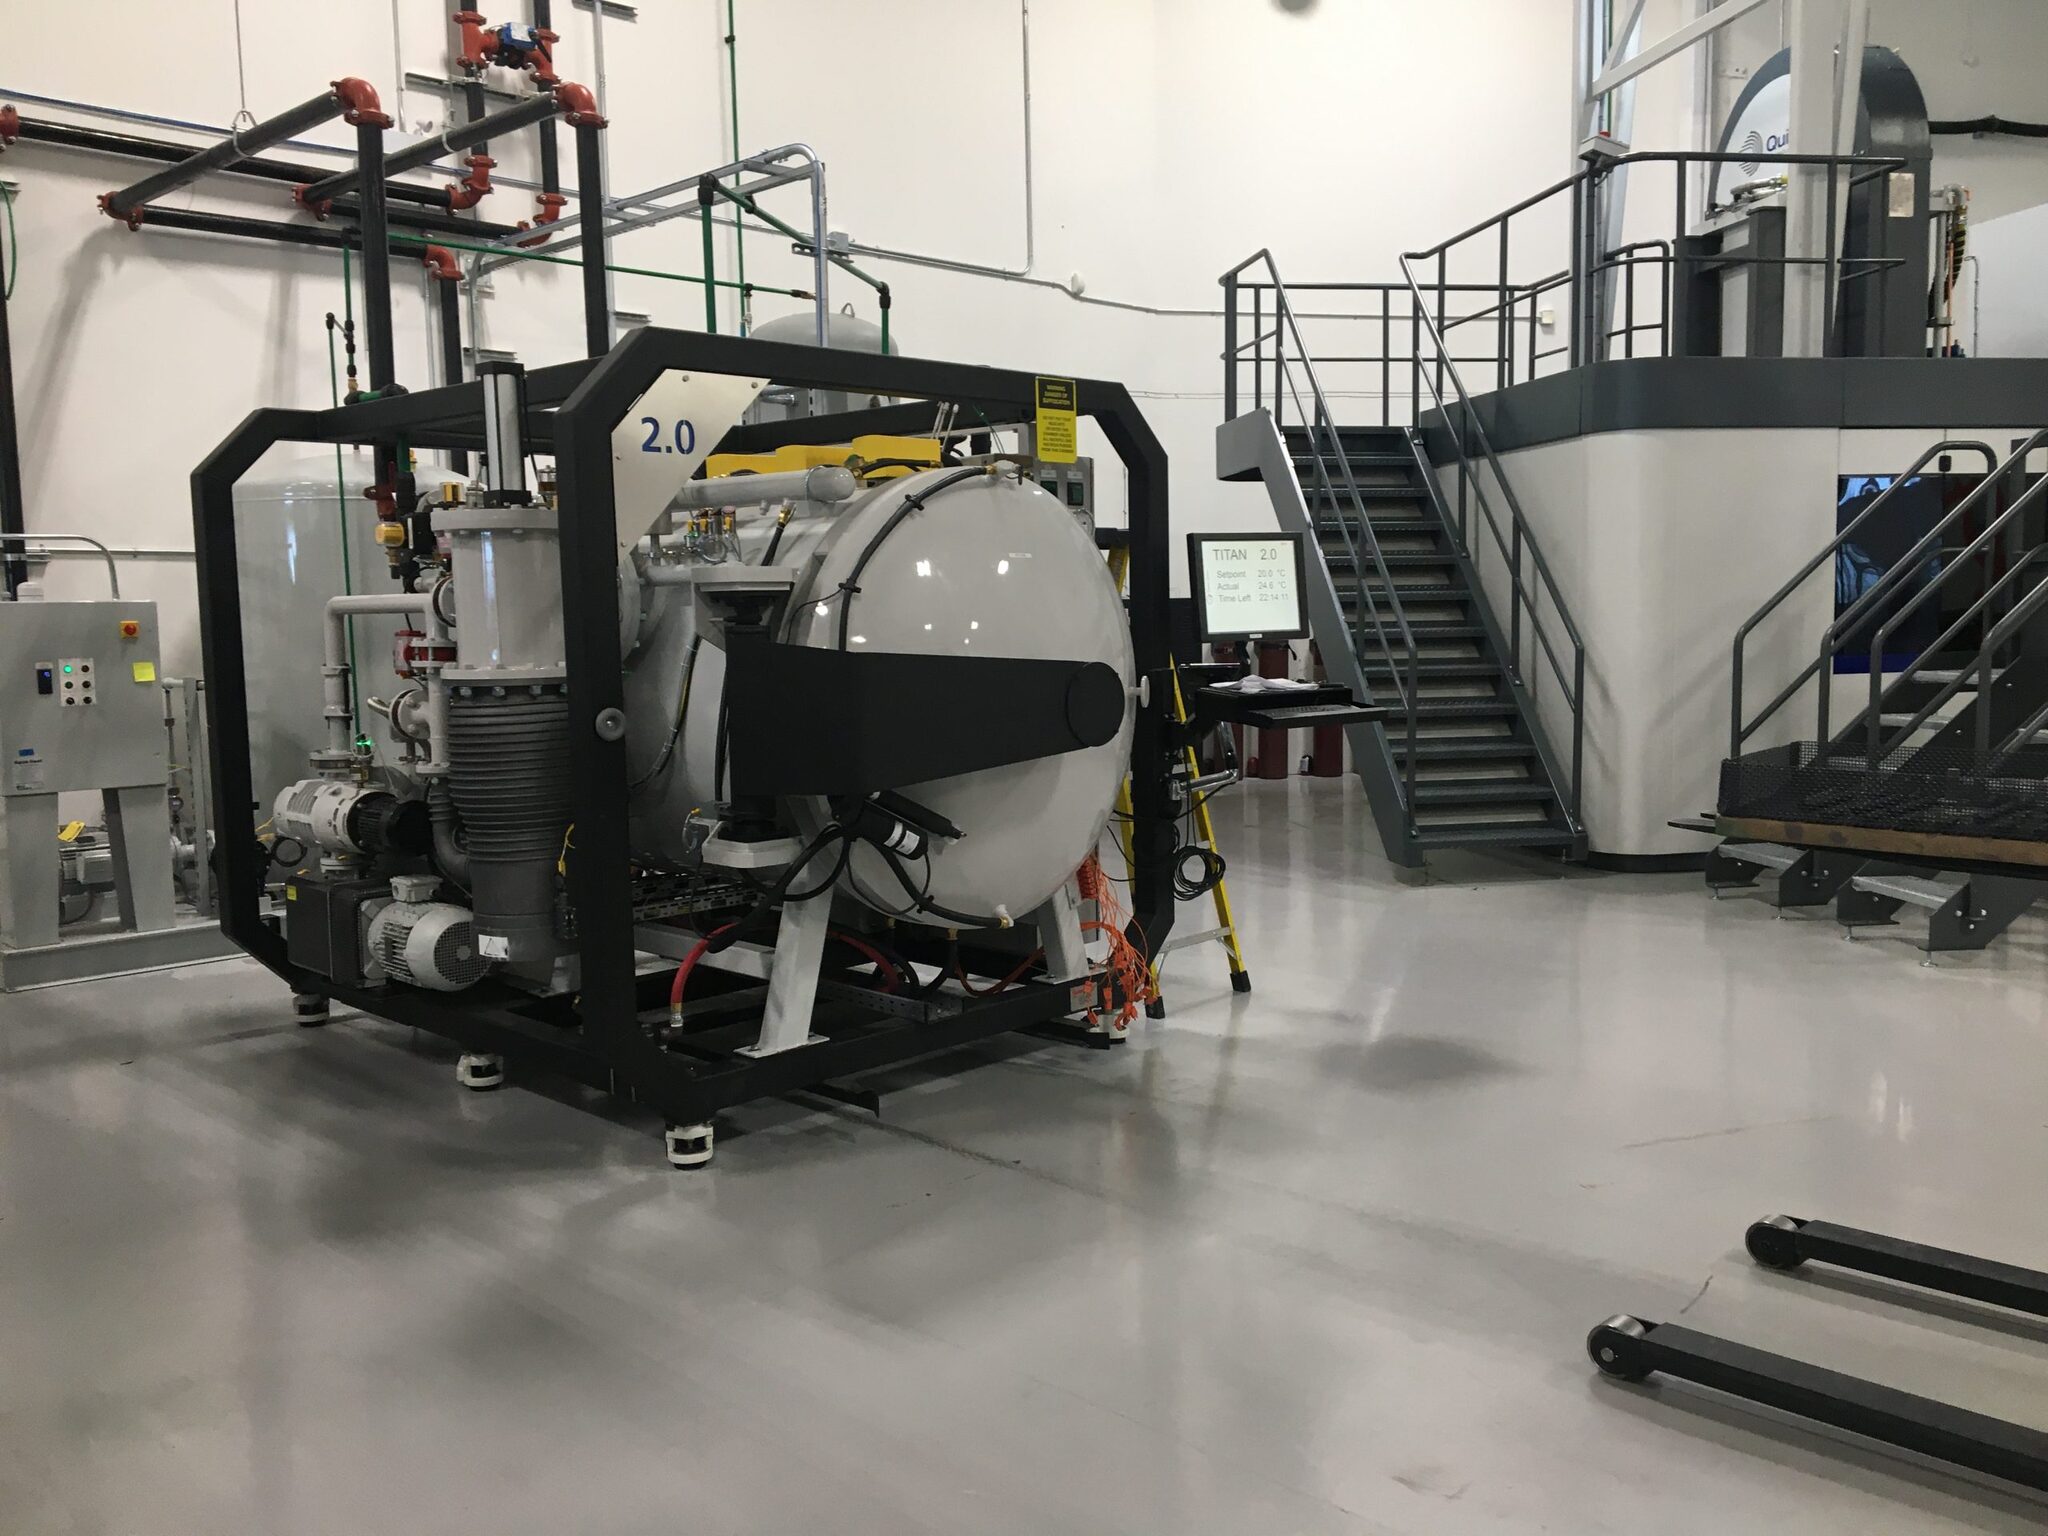
“July 9 2020. “Burloak Technologies Installing In-House Heat Treatment Department; In Burlington, Ontario, Canada we find Burloak Technologies who describe their company thusly; “Burloak Technologies is Canada’s leading supplier of highly engineered additive manufactured components for demanding applications.” https://burloaktech.com/ The company makes our news section today due to the fact that for months, if not years the company has been planning their brand new, state of the art in house heat treating department and just this week one of the first pieces of equipment arrived-a new Titan vacuum furnace from Ipsen in Rockford, Illinois, USA. Installation and Nadcap qualification are the next steps. Future plans are very ambitious to say the least, with several more large pieces of equipment on order, this includes a furnace for processing aluminum. Additive manufacturing is proving to be a rapidly growing market for furnace manufacturers, already this year we have announced several large heat treatment investments in the field and we would expect this will grow rapidly in the future.”