three NO comics style text, vintage attention message, retro dangerous poster
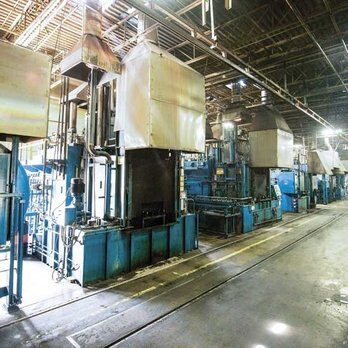
It is always a hot topic whether manufacturers should bring heat treating in house or “farm” it out to commercial heat treaters. Many considerations enter the mix including;
Do the volumes justify the high costs of installing a heat treat department?
Does the manufacturer want to add a process which in many cases they have little to no experience with?
Do the benefits of controlling quality and “turn around time” by bringing heat treat in house outweigh the initial investment?
Does a manufacturer really want to bring what is quite often a dirty, hot furnace into their manufacturing facility?
The team at “The Monty Heat Treat News” has fielded this question many times over the years-the topic popped up again this past week when we were approached by a US manufacturer who asked exactly that question “should I invest in my own heat treat department due to long turnaround times by my local heat treaters”? With his permission and our agreement that no names would be mentioned this is the manufacturers dilemma and our response:
“Manufacturer: I have some interest in bringing heat treating in house. The parts are run in batches of about 200 lbs. maximum. Some parts are 8610, need a .030 case hardened and quenched and tempered RC42 to RC60 depending on the application.
One group of parts are 4340 that get carbo-nitrided .005 deep and ideally need marquenched RC48-54 to reduce distortion in some reamed holes. These parts have been difficult to get done consistently and have a high minimum charge making us carry a large inventory of parts.”
“The Monty”; What is the value of the commercial heat treating per year”
“Manufacturer; With the scrap costs on the 4340 parts we are over $50,000 per year and it limits our ability to expand some product lines. Some work we have to either turn down or charge $350.00 for 2 lbs. of parts and wait 2 to 4 weeks to get them back. I do know a couple of companies that have similar problems because the heat treaters in this area do not have equipment for low volume parts. If we need an non standard process or case depth we have paid $500.00 to get 5 lbs. of parts in two weeks or waited 6 weeks at $350.00.”
“The Monty”; In this particular case the answer is absolutely, 100% clear-do not bring heat treating in house! The general rule of thumb is that to make economic sense a manufacturer can only afford to invest in equipment what they are sending out to a commercial heat treater over the course of a year. In this case, that number is $50,000 and there is no way in this situation that they will find the equipment they need for $50,000.00. This of course does not take into account the learning curve of heat treating, the amount of space required and the need to hire somebody to run the department.
Our advice? Find another heat treater who specializes in small lot sizes.-there are plenty of them out there.
Have a question for “The Monty”-we look forward to it! [email protected]
Lets start off the week of March 9th, 2026 by having a look at some well known (and some not so well known) individuals who are changing direction in the global heat treatment industry;
Jim Feltner, CEO, FPM Heat Treating. For a number of years now Jim Feltner has been CEO of one of the largest commercial heat treaters in North America “FPM Heat Treating” in the Chicago area. According to these comments from Jim, he is changing direction in his career; “I’m excited to share that I have joined Magnetic Inspection Laboratory, Inc. (MIL) in Elk Grove Village, IL as President. MIL has a long-standing reputation in Aerospace and Defense coatings, specialty metal finishing, and non-destructive testing serving critical customers where quality and reliability matter most.
I look forward to building on the foundation that MIL has built and strengthening operational excellence, investing in people, technology, and driving disciplined growth in the Aerospace and Defense markets. Thank you to everyone who has supported me throughout my career. I am energized for what’s ahead.”
Bob Ferry , VP Engineering & Quality, FPM Heat Treating. In related news Bob Ferry who spent a very impressive 43 years with FPM recently parted ways with the company. He is now President of his own heat treat consulting firm at which we are sure he will do very well based upon his experience.
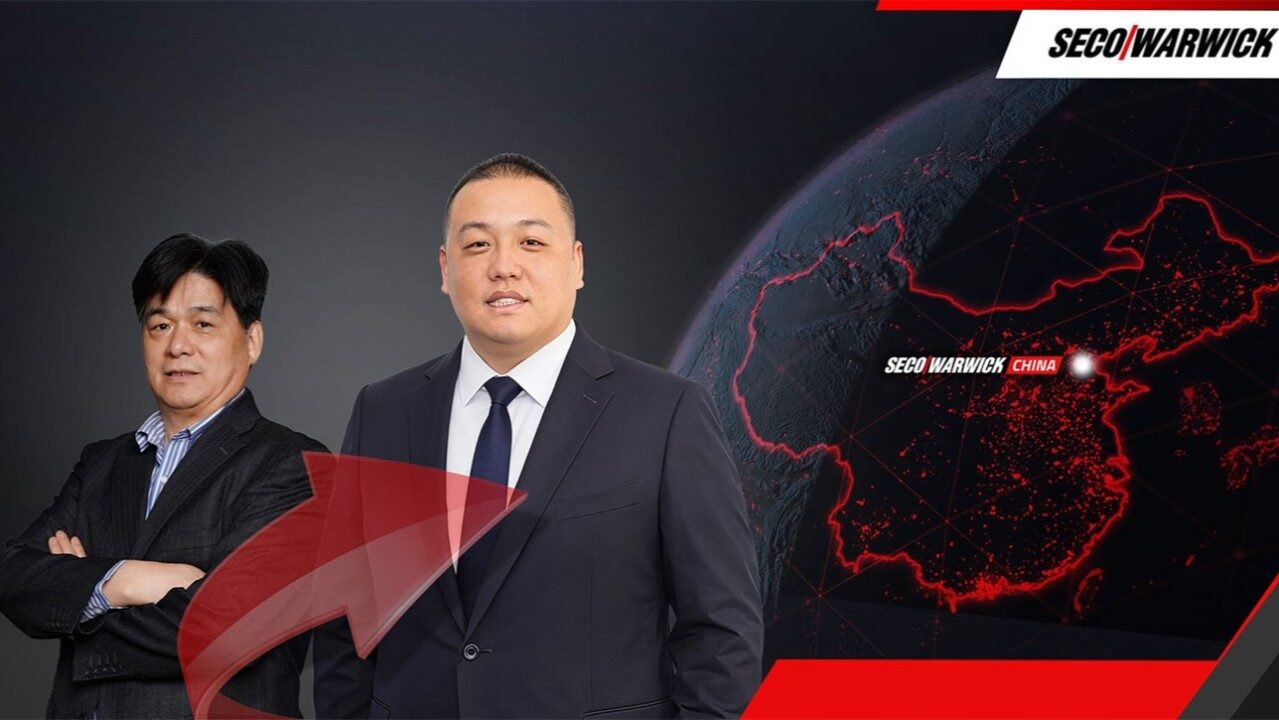
Pan Gaojun, SECO/WAREWICK, China.Mr. Pan Gaojun recently took over as Managing Director of furnace builder SECO/WARWICK China. He takes over from Mr. Liu Yedong who held this position for 10 years. Liu will now serve as Vice Chairman of the Board of Directors of SECO/WARWICK China and Senior Advisor to the Operating Board.
Erik Santora, ALD, Germany. ALD is known both as one of the world’s largest suppliers of LPC (Low Pressure Carburizing) systems and also as one of the globe’s largest LPC commercial heat treaters. Recently Erik Santora joined the company as Sales Manager in Hanau, Germany.
James Timlin, Bodycote ADE, UK. In the UK, Mr. James Timlin was recently appointed as the Sales Director for the ADE (Aerospace, Energy & Defense) Division of heat treating giant Bodycote.
Riccardo De Luca, Regional Sales Manager, Bodycote. After a number of years in the European heat treat industry in a variety of positions Mr. Riccardo De Luca has been appointed Regional Sales Manager, GNA North with commercial heat treater Bodycote. GNA stands for Germany North & Netherlands an area which Bodycote is very strong in.
Dean Russell (Senior and Junior), Industrial Thermal Systems. For many years Dean Russell Senior and Junior have acted as independent sales representatives covering the thermal processing industry in the US North East, most notably as representatives of vacuum furnace builder Ipsen. Very recently the company parted ways with Ipsen (there was a formal announcement of this last week on “The Monty”).
St. Marys, PA — Gasbarre Thermal Processing Systems (Gasbarre) has received an order for a custom-engineered box furnace and loading system to be installed at a U.S.-based manufacturing facility, marking a new customer relationship and demonstrating Gasbarre’s ability to deliver solutions tailored to highly specific operational requirements.
The project required a furnace design that could meet strict space, access, and installation constraints while supporting a non-standard thermal application. Gasbarre worked closely with the customer to develop a solution that fit within the available footprint and complied with facility limitations that had previously restricted equipment options.
Gasbarre was selected based on its ability to respond quickly, collaborate closely throughout the approval process, and engineer a system specifically aligned with the customer’s needs — rather than adapting an off-the-shelf design. The project progressed under a tight timeline, with Gasbarre providing consistent engagement from initial inquiry through final authorization.
“Some applications don’t allow for compromise, whether due to space, schedule, or process requirements,” said Patrick Weymer, Business Development Manager for Gasbarre. “This project reflects our ability to engineer practical, reliable solutions when standard equipment simply won’t work.”
The system supports a specialized high-temperature thermal operation that was previously validated at a smaller scale and is now being expanded to meet increased capacity requirements. The direct fired furnace is designed to operate in an air atmosphere up to 2100°F and represents the largest configuration that can be accommodated within the facility’s constraints.
Gasbarre Thermal Processing Systems designs and manufactures engineered thermal processing equipment for demanding industrial applications, partnering closely with customers to solve unique challenges with precision and discretion.
In 31st place on our list of the “52 Largest North American Commercial Heat Treaters 2025″you will find “Metex Heat Treating” of Mississauga, Ontario, Canada. This 40 year old, family owned business processes over 8o million pounds of material per year, mainly through mesh belt continuous furnace lines, batch IQ furnace and Induction hardening processes.
The firm just placed an order for a new gas fired “AFC-Holcroft” UBQ furnace with working dimensions of 36″ X 72″ X 36″ with FNC capabilities. When the furnace is installed, it will bring the number of batch IQ furnaces at this location up to 8, although this will be the third with working dimensions of 36″ X 72″ X 36″. With this addition “Metex” will have the largest installed batch IQ capacity of any commercial heat treater in Canada.
It is rather ironic that we mention “Metex” in terms of Batch IQ capacity when they are probably best known around North America for their mesh belt furnace capacity. With 7 mesh belt lines the company is able to process an astounding 26,000 pounds per hour of fastener work.
For more about “Metex” we would suggest these exclusive news items from “The Monty Heat Treat News”;
“CAN-ENG Furnaces International Ltd. (CAN-ENG) is proud to announce that it has been certified as a FANUC Authorized System Integrator (ASI), expanding its capabilities in robotic automation for industrial furnace systems and thermal processing equipment. This certification recognizes CAN-ENG’s advanced training and expertise in FANUC robot integration, supporting manufacturers worldwide with custom automation solutions for heat treatment and thermal processing applications.
As a FANUC Authorized System Integrator, CAN-ENG is part of a global network of trusted robotic system integrators specializing in industrial automation solutions. This partnership provides customers with direct access to FANUC industrial robots, advanced automation technologies, and technical support delivered through CAN-ENG as a single-source provider. CAN-ENG works closely with manufacturers to select, design, and integrate robotic automation systems that deliver high performance, reliability, and operational safety and efficiency.
CAN-ENG’s engineers have been trained and certified directly by FANUC, ensuring expert application of robotic automation in thermal processing systems, including heat treatment furnaces, material handling automation, and high-volume industrial furnace operations. With strong in-house engineering and on-site support, CAN-ENG helps manufacturers modernize production through high-performance industrial robotics.
This collaboration reinforces CAN-ENG’s role as a single-source automation partner for industrial furnace projects. By offering a unified approach from industrial furnace design and in-house manufacturing to robot programming, system integration, and long-term support CAN-ENG simplifies project execution and delivers reliable turnkey automation solutions for demanding industrial environments.
About CAN-ENG Furnaces International Ltd.; CAN-ENG is a leading global designer and manufacturer of industrial furnace systems and thermal processing equipment for ferrous and non-ferrous metals. For more than 65 years, CAN-ENG has specialized in batch and continuous heat treatment furnaces, serving automotive, steel, aluminum, forging, stamping, oil and gas, rail, and foundry industries worldwide.
CAN-ENG’s rugged furnace designs are recognized for innovation, durability, and efficiency, incorporating energy-saving furnace technology, automated material handling, and advanced industrial robotics to improve production flow, throughput, and facility performance.”
(Editors Note; February 19th“The Monty Heat Treat News” had a news item entitled “North American Furnace Builder Changing Sales Direction”. In that news item we mentioned that furnace builder “Aichelin”, through their USA division “AFC-Holcroft” had replaced a number of their independent sales representatives in favor of direct sales people. This press release from Ipsen mentions replacing one of their independent sales reps with a direct sales person.)
“Cherry Valley, ILLINOIS (March 4, 2026) – Ipsen announces that Industrial Thermal Systems, led by Dean Russell III and Dean Russell IV, is no longer representing Ipsen in the Northeast region. Ipsen appreciates the Russells’ years of dedication and service to Ipsen customers and wishes them continued success in their future endeavors.
Effective immediately, Ipsen will support customers in the region directly. Chad Mehmel, Northeast Regional Sales Engineer, will assume responsibility for all inquiries related to new furnace equipment, while continuing to support customers with replacement parts, retrofits, and hot zones.
Chad has been with Ipsen since October 2023 and has worked closely with customers on aftermarket solutions and equipment performance. His technical background and hands-on experience position him well to support customers’ equipment planning and project needs.
All service-related matters, including field service and technical assistance, will continue to be directed to Guy Kemble, Northeast Regional Service Manager.
Ipsen’s Parts, Service, Retrofits, and Equipment teams remain fully committed to ensuring a seamless transition and uninterrupted support. The company values the continued partnership of its customers and looks forward to supporting their operations.
Customers are encouraged to contact Chad Mehmel or Guy Kemble directly, or submit an inquiry through the online contact form at https://ipsenglobal.com/request-a-quote/.
“The Monty Heat Treat News” March 2026 Edition; Welcome to the March 2026 Edition of “The Monty Heat Treat News” for over 30 years the heat treatment industry’s largest source of news and industry trends. Some “trends” and industry exclusive “news” headlines in this issue include these;
In addition to our exclusive news items “The Monty” is proud to point out the most recent additions to our “Surplus Heat Treat Equipment Section”. As few examples include these;
As always “The Monty Heat Treat News” looks forward to your thoughts and comments. “The Monty Heat Treat News” is a division of William G. Montgomery Ltd., a family owned business serving the global heat treatment industry since 1968. Sincerely Gord, Jordan and Dale Montgomery.
Mödling / Göppingen / Düsseldorf. As part of the integration of NITREX, the AICHELIN Group is strengthening the organization of UPC in Germany and further intensifying the integration of its expertise in plant engineering, process control, and digital solutions. With personnel changes at United Process Controls GmbH (UPC Marathon) in Göppingen and at QMULUS in Düsseldorf, the Group is reinforcing its technological focus and responding to the growing importance of digital solutions in the heat treatment industry.
Daniel Panny Appointed Head of UPC; Effective March 1, 2026, Daniel Panny has assumed management of the UPC site in Göppingen. In this role, he holds overall responsibility for the site and has been granted power of attorney (Prokura). At the same time, he continues in his position as Head of Sales Europe at UPC.
Daniel Panny brings more than 20 years of experience in the heat treatment industry and contributes extensive market, industry, and sales expertise to his expanded role. This combination of operational site responsibility and European sales leadership is intended to further strengthen strategic market development and consistently drive the sustainable growth of UPC.
Karl-Michael Winter, who previously served as Managing Director of UPC and in a dual role as VP R&D / Engineering at NITREX Metal, will in the future support the AICHELIN Group’s R&D team as Senior Consultant R&D NITREX, contributing his many years of expertise in development.
Mike Löpke Appointed Head of QMULUS; Effective February 1, 2026, Mike Löpke has taken over the management of QMULUS. This division of the AICHELIN Group focuses on all software-related topics, primarily on the eponymous product “QMULUS,” an IIoT platform. In addition to controlling industrial plants, the platform places an expanded focus on coordination, analysis, and visualization of real-time data. The objective is to create process transparency, identify optimization potential, and enable more efficient plant control, including through the use of AI and machine learning. In March, the QMULUS development team will open a new office in Düsseldorf, further strengthening proximity to customers and partners in the German market.
Close Integration of Hardware, Process Know-how, and Digital Solutions; UPC specializes in control and automation systems for heat treatment plants and plays a central role within the AICHELIN Group in the further development of digital solutions. In combination with existing process control systems such as FOCOS 4.0 and the cloud-based analytics platform QMULUS, this creates a seamless connection between plant control, automation, and data-driven optimization.
Energy efficiency, process stability, and transparency are becoming increasingly important. At the same time, demand is growing for digital solutions that capture plant conditions in real time and enable predictive optimization.
“With the further development of our organization in Germany, we are creating the conditions to more closely integrate our technology and software expertise. Our ambition is not only to supply individual products, but to deliver holistic solutions along the entire process chain,” says Christian Grosspointner, CEO of the AICHELIN Group. “The combination of proven heat treatment technology, process know-how, and digital IIoT applications is a key element of our strategic direction.”
The structural adjustments are part of the Group-wide organizational development, ensuring clear responsibilities, faster decision-making processes, and stronger collaboration across locations and companies.
About the AICHELIN Group; The AICHELIN Group, headquartered in Mödling near Vienna and part of the Berndorf AG, is one of the world’s leading providers of heat treatment solutions. Its portfolio includes industrial furnaces, industrial heating systems, nitriding systems, control and automation systems, Industry 4.0 solutions, as well as service offerings. The company’s roots date back to 1868. In addition to the traditional AICHELIN brand, the Group includes AFC-Holcroft, SAFED, BOSIO, NOXMAT, and NITREX, making it one of the world’s top three heat treatment companies with around 1,350 employees. The AICHELIN Group operates subsidiaries in Austria, Germany, Slovenia, France, Poland, Turkey, China, India, and the USA. Its global presence is further strengthened by an international sales network. www.aichelin.com
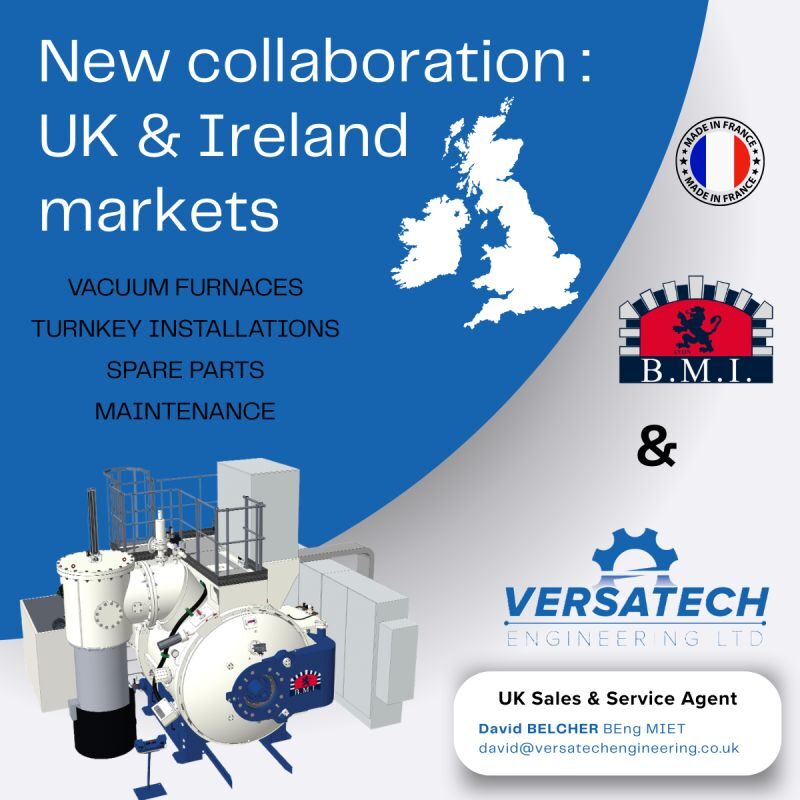
Vacuum furnace builder “BMI” is known as the largest vacuum furnace builder in France although the bulk of their systems are delivered to customers as far afield as Taiwan. Recently they have been very aggressive at moving into new markets such as North America.
This press release tells us how they have hired a new sales representative to cover the United Kingdon and Ireland;
“We are pleased to announce our partnership with Versatech Engineering, who will now represent BMI across the United Kingdom and Ireland. This collaboration marks an important step in strengthening our presence in these markets and delivering high-performance heat treatment solutions supported by local expertise and technical excellence. We look forward to supporting customers in the UK and Ireland with reliable technology and dedicated service.”
BMI Furnaces at Ramada, Portugal
(Editors Note; Bob is well remembered by many long time USA heat treaters. Bob started at Metal-Lab in Sturtevant in 1979 before it was bought by Lindbergh and then Bodycote. He started in the heat treat world back when we still did pack Carburizing and used retorts. Bob was instrumental in the success of the Bodycote Sturtevant facility developing many of the processes and procedures still in place today.)
“Robert “Bob” James Struebing, 68, passed away on February 24, 2026. Born on April 14, 1957, in Racine, Wisconsin to Roy Struebing and Hannelore (née Cziossek) Struebing.
Bob graduated from Case High School, where he was a standout athlete, playing football and excelling in track. His strong work ethic and competitive spirit carried with him throughout his life.
Following high school, Bob proudly enlisted in the United States Marine Corps. There he attained the rank of Corporal, awarded the Good Conduct Medal and the M-16 Rifle Marksman Badge while serving in Supply Administration and Operations. Bob remained deeply honored of his service, especially coming from a proud military family.
On June 24, 1981, Bob married the love of his life, Veronica (née Schilg) in Waukegan, IL. Together they built a beautiful life centered on love, happiness, and family. Their marriage of over four decades was filled with devotion, laughter, and the joy of raising their children.
Bob dedicated over 40 years of his career to Bodycote, where he worked as a heat treater and earned the title of Production Manager. After retirement, Bob couldn’t sit still for long and soon returned to work part-time at Hestia Heat Treating, motivated by staying busy and productive.
Above all else, Bob was a family man. He was a great father and an even better grandfather. He cherished time spent at the family cabin, sharing many laughs and stories. Moments that seem small but mean so much more.
Bob was an avid Wisconsin sports fan, especially a loyal supporter of the Green Bay Packers. He took great pride in his German heritage and was an active member of the Racine German Club. Whether cheering on his teams, sharing family traditions, or gathering everyone together, Bob’s presence was steady, strong, and full of love.
He is survived by his wife, Veronica Struebing; his children, Josh (Amber) Struebing, Erik (Wendy) Struebing, and Sara (David) Clark; and his grandchildren, EmaLee, Drake, Dayton, Ila, and Mack. He is further survived by his loving brothers and sisters, and many nieces and nephews.
Bob was preceded in death by his parents, Bud and Hano Struebing, and his granddaughter, Dakota Marie.
A memorial service to celebrate Bob’s life will be held Thursday, March 5th at 9:30 AM at the Draeger-Langendorf Funeral Home and Crematory, 4600 County Line Road. Prior to the service, there will be a visitation beginning at 8:30 a.m. Immediately following the service, family and friends will proceed to Southern Wisconsin Veterans Memorial Cemetery, where Bob will be laid to rest with honors.
The family would like extended their gratitude to Racine Fire Station 4 and to all the Emergency Department staff at Ascension Hospital for their life saving efforts.”


 In 31st place on our list of the “52 Largest North American Commercial Heat Treaters 2025″ you will find “Metex Heat Treating” of Mississauga, Ontario, Canada. This 40 year old, family owned business processes over 8o million pounds of material per year, mainly through mesh belt continuous furnace lines, batch IQ furnace and Induction hardening processes.