We are indeed privileged today to be speaking with “Mr. Max Stormo”, “Ipsen Customer Service (ICS) Operations Manager”. In this interview Max shares with us details about how Ipsen Souderton, PA focuses on hot zone related fabrication, machining and assembly, retrofits and aftermarket parts;
Max we always like to start our interviews with a bit of personal background, for instance could you please share with us how you ended up in this new position.
“In early 2024, the timing was right as I was looking for a new opportunity. I was contacted by Ipsen regarding the open site leadership position in Souderton, and I quickly realized this could be a good fit for both myself and Ipsen. As I continued through interview process, I was very impressed with the company, product and people I met. I got the opportunity to tour both facilities, see the processes and meet many people and was very excited about the potential of joining the Ipsen organization. Ipsen matched the opportunity I was looking for, and I knew I could join the organization and be a key contributor to the vision the organization had in place for the Souderton location.
I am new to the thermal processing equipment industry but having spent a career in manufacturing, was very familiar with heat-treating and heat-treating processes. The knowledge I had was all in the atmospheric heat treating. Vacuum heat treating was new to me, and I found the technology incredibly intriguing having spent most of my career in aerospace and oil & gas manufacturing.
Significant selling points for me deciding to join Ipsen were the leadership and the employees I met throughout interview process. Ipsen’s leadership team was open and transparent and transparent throughout the process. I trusted opportunity that presented itself with Ipsen and was excited when I accept the role.”
You have a very impressive title “Ipsen Customer Service (ICS) Operations Manager” – what are your responsibilities in this position?
“As the site leader for Ipsen in Souderton, Pennsylvania, I’m responsible for all operational activities that include leading the manufacturing, purchasing, production control, shipping and receiving, and warehousing. Safety, quality and continuous improvement are critical aspects of our core values and vision for Ipsen, so I take personal ownership of these aspects. Trust, collaboration, communication and employee engagement are critical to achieving these core values and are reflective of our culture and the way we lead at Ipsen. This has been the gateway to realizing the transformational improvements that we’ve made in 2024 and 2025.”
Ipsen North America is based in Rockford, Illinois which is where furnace assembly is located, and you are in Souderton, PA. What does your facility offer? In fact, lets elaborate on that a bit, could you please tell us the size of your plant and the number of employees?
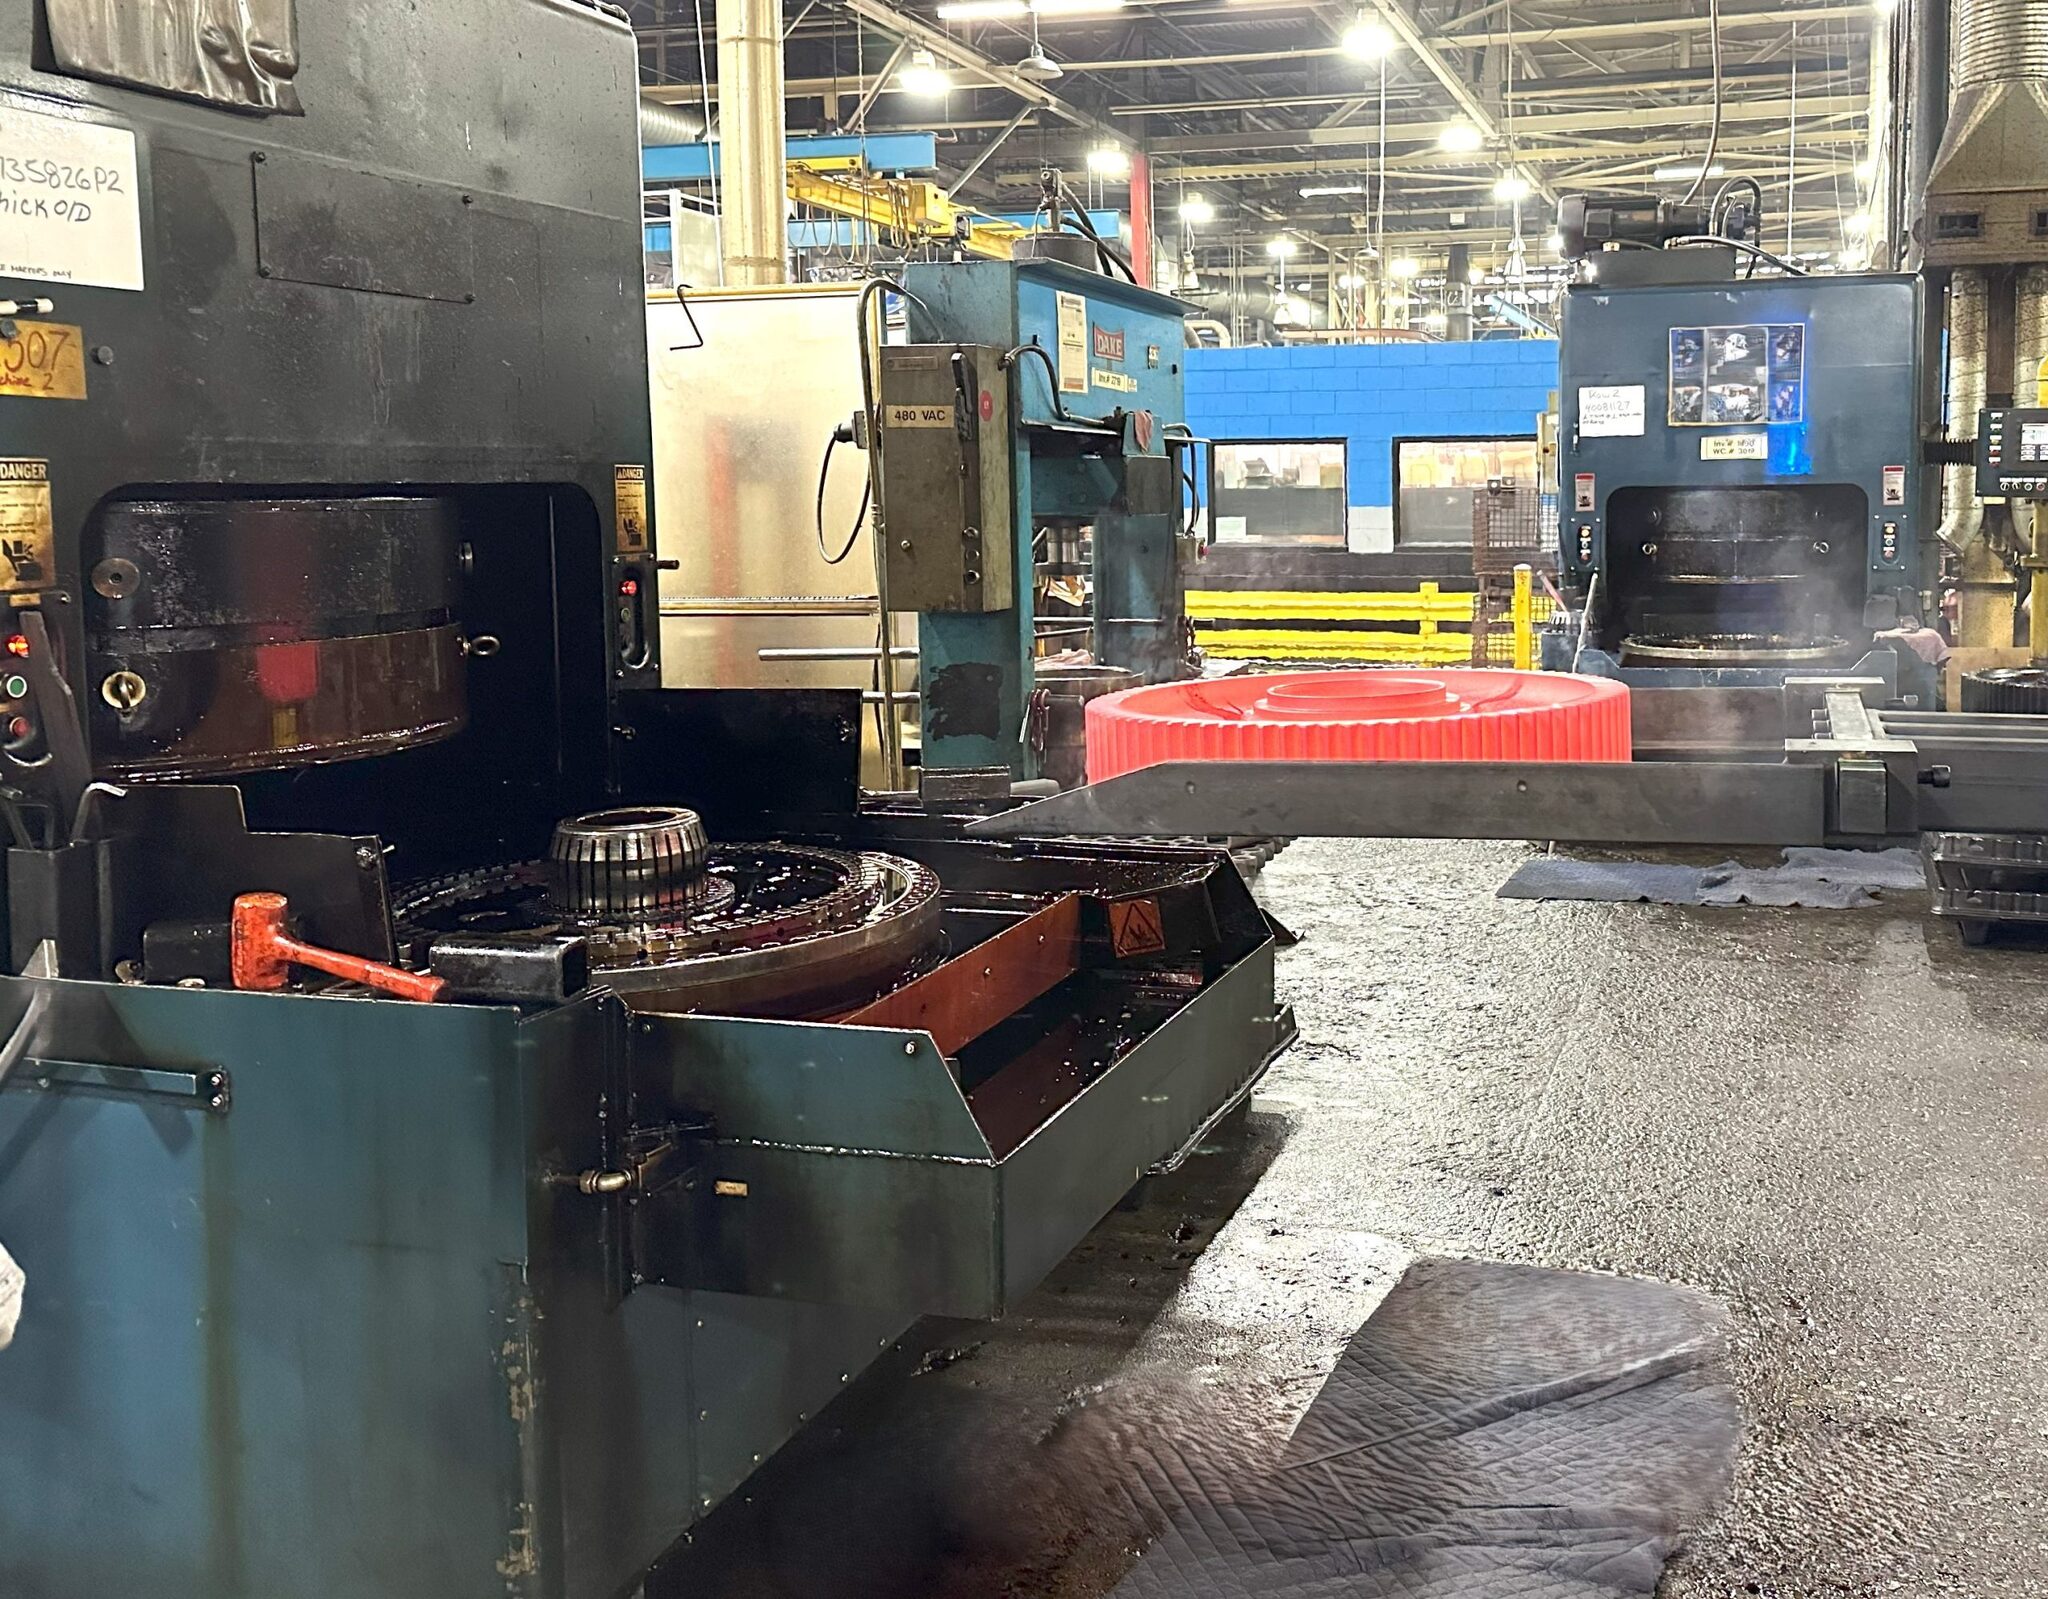
“Ipsen Souderton’s team is focused almost entirely on hot zone related fabrication, machining and assembly, serving the new equipment, retrofit, and aftermarket parts side of Ipsen. Hot zone retrofits and aftermarket parts ship directly from our factory to our customers. We also support non-hot zone aftermarket parts for our VFS customers.
(Ipsen merged with Vacuum Furnace Systems in 2007.)
Ipsen Souderton is approximately 60 employees including factory workers and support staff.”
Is it ever an issue the geographical distance between the two plants?
“The advantage of having this location is that it gives Ipsen strong representation on both the east coast as well as the Midwest. The two plants complement each other by focusing on two unique elements of our total business. In Souderton, we are heavy fabrication, machining and hot zone manufacturing focused, while the Cherry Valley, Illinois plant is primarily focused on engineering and assembly, from a manufacturing perspective. Because our focus is so different, the geographic distance works in our favor for many reasons.”
My understanding is that you have made some very substantial investments in new equipment in Souderton, please give us some details.
“Our CapEx investment strategy has been focused on automating equipment and processes. In 2024-25, we’ve added additional CNC machining centers, CNC fabrication work centers, and a fiber laser system. The driver behind this CapEx strategy is to improve quality, increase throughput, reduce lead times and improve the overall experience for our current and future customers.
We’ve also invested significant time and resources in OpEx (operational excellence) by enhancing processes, looking for opportunities to reduce steps, handling, time and travel in the manufacturing process. We want to minimize the number of times a part is touched, reduced travel times both within our factory and to our facilities and customers. We’ve also made a major investment on the system side, rolling out enhanced ERP tools and adding real-time MES capability on the shop floor.
Let’s talk a bit about hot zones. Are you able to share with us how many hot zones per year you are producing and how many you would like to be building? In other words, do you have a goal that you would like to reach?
“In both 2024 and 2025 we doubled our hot zone output. We anticipate an additional 10-15% volume growth in 2026 based on our trends and outlooks. We also fulfilled over 4,000 parts orders out of our Souderton location last year. We make all critical components in house which allows for quick turnaround to customers.”
Continuing the topic of hot zones, do you provide units for competitors furnaces, or do you focus on replacement hot zones strictly for Ipsen furnace systems?
“Approximately 90% of our business for retrofit hot zones is made of a mix of Ipsen style and VFS style hot zones. VFS continues to be a significant part of retrofit hot zone business. 10% or less of our retrofit hot zone business is comprised of hot zones for competitor’s furnace but we are always willing to review new opportunities.”
Are you limited geographically to North America or do provide your products and services to the entire globe as required?
“Because Ipsen furnaces are operating around the world, we ship all over the globe – both parts and retrofits. On any given day, we may have orders from North and South America, Europe, and Asia. We serve a global market.”
My understanding is that while you certainly have a very impressive manufacturing background, this is your first foray into the world of thermal processing equipment. After 19 months in the industry what are your impressions about heat treating equipment, Ipsen and the industry in general? Is it much different from other industries you have been involved with?
“Having spent my entire career in operations, specifically in the manufacturing industry, I’ve been associated with thermal processing of the manufactured components in every organization I have been a part of. It is a process that was either done in house in small batch quantity, or we outsourced to a third party. Ipsen has been my OEM experience in thermal processing equipment.
Thermal processing is a vital global industry and has been for generations. It continues to advance as emerging technologies and an ever-evolving industrial landscape place new demands on manufacturing. From aerospace and energy to medical and beyond, thermal processing is an essential service that supports virtually every manufacturing sector and continues to expand each year. This growth is fueled by the need to support increasingly complex applications and new product development.”
Care to make some comments about the coming year? Predictions are always tricky and I am probably being very unfair even asking the question but what are you forecasting for 2026?
“For 2026, from an operations perspective, we’re going to continue our focus on OpEx and CapEx, concentrating on quality, continuous improvement, system utilization, automation, people and culture development. These investments continue to drive our business to the next level.
Our goal is to exceed customer expectations for service, quality, and timeliness – at Ipsen we refer to it as “Quality at Speed.” Internally, we are constantly asking the questions: How do we better serve our customers? How do we push to be the benchmark that competitors have to compare themselves against?
From a customer service perspective, quality must come first in our industry. Lead time and quality expectations matter. Systems, processes and investments are all being driven from that point of view.
To that end, we are pursuing the processes of Lean Manufacturing/Continuous Improvement to remove non-value-added activities out of the process and streamline process flow. We want a continuing effort towards 5S, streamlining process flow, minimizing transportation waste, and diversifying our supply chain.
We have several new capital investments online and ready to serve our customers and our organization, with a continued focus on optimization.
The passion and pursuit of excellence is booming in Pennsylvania.”
“Kencoa Aerospace has begun expanding its defense and space business in the North American market.
On January 6, Kencoa Aerospace announced that it had completed the acquisition of Aremac Heat Treating, a U.S.-based heat treatment specialist, through its American subsidiary, Kencoa Aerospace LLC.
Lee Minkyu, CEO of Kencoa Aerospace, stated, “This acquisition marks a significant turning point in our global growth strategy centered on the space and defense sectors. By acquiring a heat treatment specialist located near our existing U.S. production base, we will further expand Kencoa’s role within the North American space and defense industry supply chain.”
He added, “Through continuous technological advancement and strategic investment, we aim to become a trusted company for global space and defense customers and partners.”
Kencoa decided to acquire the heat treatment specialist as part of its ongoing strategy to expand its global space and defense business. Through this acquisition, the company has strengthened its local heat treatment production base targeting the North American space and defense markets and established a production system capable of reliably meeting the stringent quality standards and delivery requirements unique to the defense and space sectors. The company plans to further reinforce its business foundation within the U.S. defense and space industry supply chain.
The company explained that by securing additional heat treatment processes essential for manufacturing core components for space launch vehicles and defense aircraft, it has enhanced its competitiveness in the North American market. With supply chain stability emerging as a key issue across the global space and defense industries, Kencoa expects strong demand for its local production system.
To respond to the North American defense market, Kencoa Aerospace has built a local production system by acquiring an aerospace and defense company with over 20 years of experience in Georgia, U.S. This has drawn attention as a case of a Korean company acquiring a U.S. defense firm. Kencoa continues to expand its production of defense and space components and its customer base in the United States.
Aremac Heat Treating, founded in 1968, is a heat treatment specialist located near Georgia. Prior to the acquisition, it operated a factory of approximately 5,300 square meters on a site of about 43,000 square meters, carrying out heat treatment processes for the space and defense industries.
Kencoa Aerospace plans to gradually expand its production capacity, focusing on the North American market. Centered on the space and defense sectors, the company will expand its Georgia production facility to about 33,000 square meters, strengthen its precision machining capabilities, and enhance its specialized workforce to establish a foundation for mid- to long-term growth.
During the process of expanding its production base in the Georgia region, Kencoa Aerospace discussed cooperation plans with Georgia Governor Brian Kemp. The company expects that, with support from the U.S. government, it will further enhance its competitiveness in the North American space and defense markets and positively impact the expansion of global orders linked to the Korean space industry.
Kencoa Aerospace LLC is Kencoa Aerospace’s key subsidiary responsible for space and defense manufacturing in the United States. Based in Georgia, it produces engine-related parts and precision-machined products for the space and defense aviation sectors, handling local customer needs and manufacturing functions in the North American space and defense market.”
January 2, 2026 it was announced that Allison Transmission had acquired the Off-Highway Drive & Motion Systems business of Dana Incorporated-read the press release below and we will then tell you why a heat treatment publication such as “The Monty Heat Treat News” cares;
“INDIANAPOLIS, January 2, 2026 — Allison Transmission Holdings, Inc. (NYSE: ALSN, “Allison”, “the Company”) today announced it has completed its acquisition of the Off-Highway Drive & Motion Systems business of Dana Incorporated, a leading provider of drivetrain and propulsion solutions, for approximately $2.7 billion. The combination of industry-leading products and advanced technologies will accelerate Allison’s growth and broaden the Company’s position as a global provider of commercial duty mobility and work solutions that Improve the Way the World Works.”
A quick scan of the list reveals “Dana Fairfield Manufacturing”, Lafayette, Indiana as the third largest single location captive heat treater in North America with “Allison Transmission”, Speedway, Indiana in the fourth position. While nothing physically changes with this acquisition some names will change.
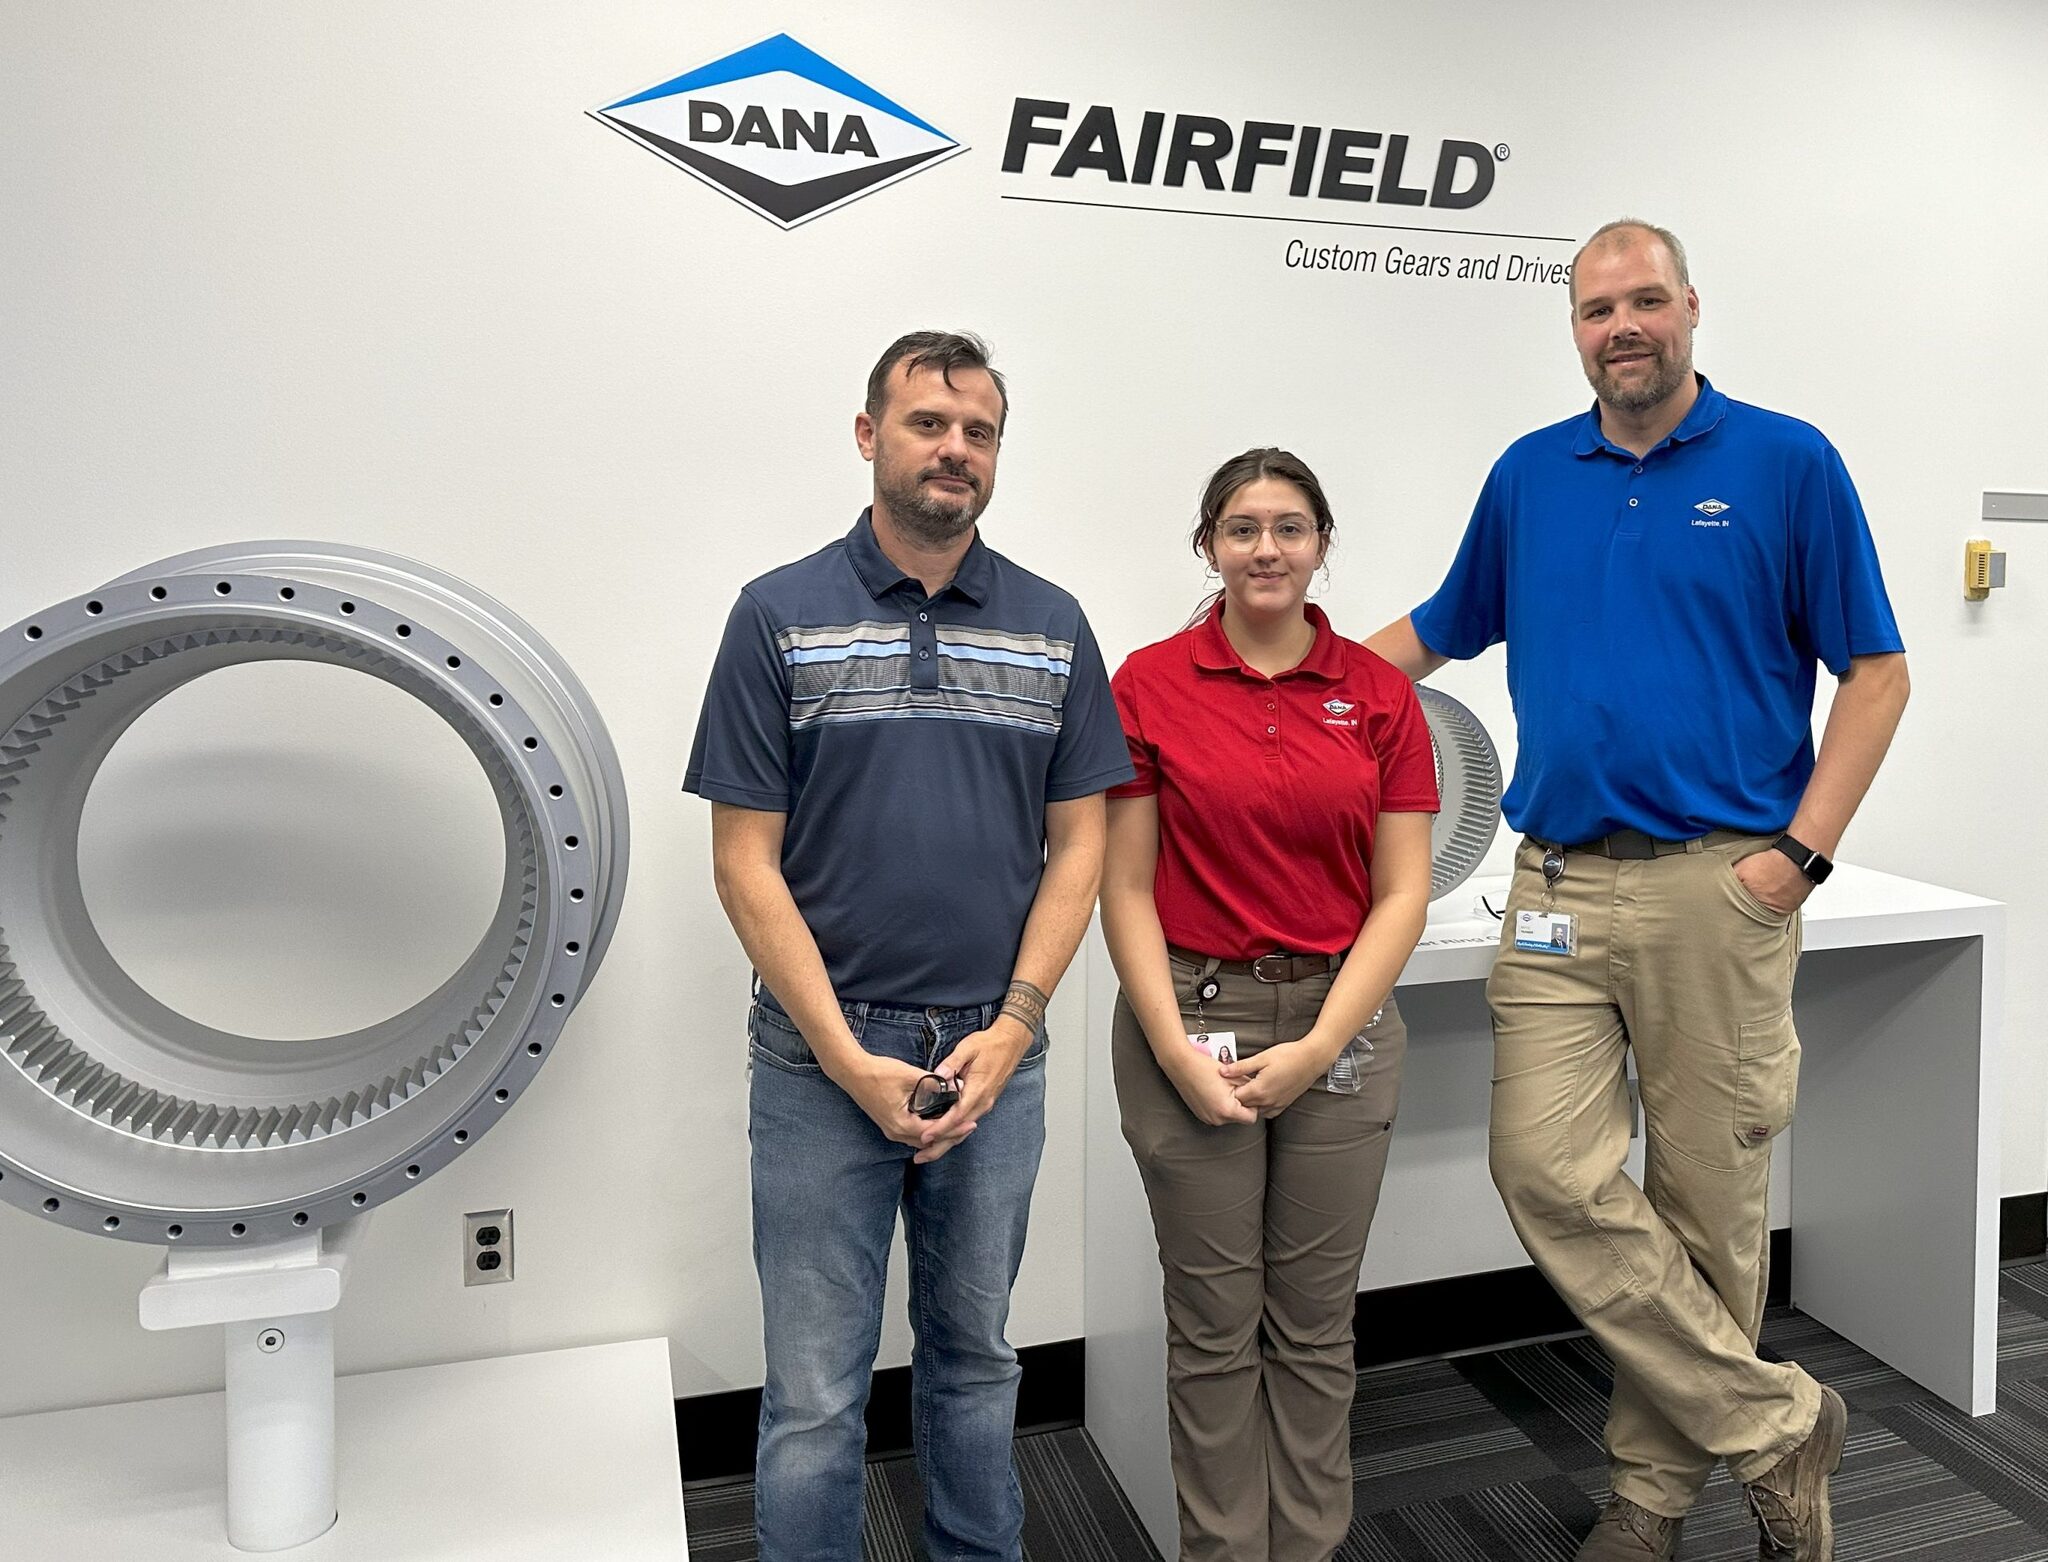
In an industry exclusive Gord Montgomery of “The Monty Heat Treat News’ was granted permission to tour and photograph the “Dana Fairfield Manufacturing” facility in 2023-a rare honor indeed. The result was this article and photos.
“Dana Inc., Lafayette, IN- “Top 15” Captive Heat Treater; Each year “The Monty Heat Treat News” puts together a list of the largest and most impressive single location, captive (in-house) heat treats in North America (the list and our criteria to be considered can be found at https://themonty.com/articles/15-largest-captive-heat-treats-north-america/).
It is interesting to note that 3 of the locations on this list are represented by Dana Inc., facilities, 2 in Mexico and 1 in Lafayette, Indiana, USA-it is the Indiana facility which is our focus today. Just last week Gord Montgomery of “The Monty Heat Treat News” had the chance to visit this location for the first time and what we found was very impressive. (At this point I would like to thank my hosts, Bryce Tanner, Manufacturing Engineering Project Manager, Aaron Flesher, Metallurgist and Zenah Baker, Control Metallurgist).
Our experience with visiting Dana facilities over the years lead us to think of large volume auto and truck components. However this location is quite a bit different, we will let Dana summarize this facility. “Dana Fairfield® engineers, manufactures, tests, certifies, and supplies precision-made gears and gear drives for an expansive range of industrial and mobile applications.” https://www.fairfieldmfg.com/
The result is that the facility can be considered High Mix/Low Volume in that typical orders might be 100-200 high precision gears which are destined for such various industries as agriculture, oil & gas, power generation and defense.
There is no way to describe the heat treat department other than by saying it is mammoth. 80,000 square feet houses 7 two row pusher furnace lines, a large roller hearth hardening line, 2 annealers, 7 batch IQ furnaces, 2 nitriders, 5 induction hardeners (scanning and tooth to tooth), 4 pit carburizing furnaces, 6 endothermic generators and 21 press quench systems. Datalogging and state of the art controls round out the picture of this clean heat treat.
In terms of capabilities the company can process gears up to 36” in diameter, with a weight of up to 900 pounds, shafts up to 2,000 pounds while the Induction systems can handle up to an 80” internal diameter.
In summary anybody with an interest and knowledge of in-house heat treating would find this a fascinating tour and after our visit we have no doubt but that Dana, Lafayette, Indiana deserves to be on our list of “The 15 Largest Single Location Heat Treats in North America”.
The link below will take you to the January 2026 edition of “The Monty Heat Treat News” the longest running heat treat industry news source in the world. Some stories we are looking at in this issue include these;
Probably few people in the heat treatment industry still remember Rich as he has not been active for quite a few years but he had a long and distinguished career in the industry. For many years he worked with Detrex Furnaces which ultimately was acquired by AFC-Holcroft which in turn was acquired by Aichelin of Austria. During his career he worked as a sales engineer travelling around North America and the world.
“Richard James Gagnon, affectionately known as “Butch,” passed away on January 2, 2026. He was 77 years old.
Butch was born on January 1, 1949, in Medford, Massachusetts, to Paul and Mary Gagnon. He graduated from Medford High School in 1967 and went on to attend college in Boston. Throughout his professional life, Butch worked as a heat-treating engineer with Atmosphere Furnace and later with Dietrich’s Heating and Cooling, where he was known for his strong work ethic and technical skill.
Beyond his career, Butch’s true passion was roller skating—a love that defined some of the happiest years of his life. He skated daily and found particular joy in pairs and partner competitions, as well as freestyle skating. His dedication and talent led him to win a National Championship with the U.S. Roller Skating Association. From 1975 until 2005, Butch was the owner of the Ambassador Roller Rink in Clawson, Michigan, where he helped shape generations of skaters and created a welcoming community centered on the joy of the sport. He also served as past president of the Roller-Skating Teachers Association of Michigan, forming deep friendships and lifelong bonds along the way.
Family was central to Butch’s life. He was a devoted father and a proud grandfather who cherished his grandchildren. He attended as many cheerleading events and hockey games as possible, always eager to support and encourage them.
Butch is survived by his children, Steve (Ramona Rushing) Gagnon, Angie (Scott) McInerney, and Kyle Gagnon; his grandchildren, Sophia, Blake, and Dillon; and his siblings, Joan Gagnon Hagstrom, Joyce Barry, Sandra Gasbaro, Lisa Gagnon Maurer, and Jimmy Gagnon. He was preceded in death by his parents, Paul and Mary Gagnon, and his brother, Paul Gagnon.
A gathering of friends and family will be held on Wednesday, January 7, from 1:00 p.m. until 3:30 p.m., with a Celebration of Butch’s Life beginning at 3:30 p.m., at Gramer Funeral Home, 705 North Main Street (Livernois, between 14 and 15 Mile Road), Clawson, Michigan 48017. For convenience, a covered, no-step entrance is available on the north side of the funeral home under the carport.”
“The Manchester (Bury), UK site of aerospace thermal processing specialists, Wallwork, has secured Rolls Royce approval of their recently opened vacuum brazing development laboratory and assembly area. The site has a high concentration of modern vacuum heat treatment furnaces of varying capacities and is able to efficiently process differing sizes and volumes of metal components.
Quality engineer Helen Ellis, who was part of the team that supported the accreditation application, noted, “We are constantly working to extend the scope of our aerospace quality approvals to give clients confidence that our manufacturing processes conform to the highest standards.”
Manchester is the largest aerospace processing location in the Wallwork group and has seen significant investment in recent years. The site already has extensive approvals for mainstream heat treatment processes from many UK and international aerospace primes such as BAe Systems, Airbus, Safran, Bombardier, Moog and others. Common treatments to improve metal component performance and endurance include case hardening, carburising, hardening and tempering, nitriding and more.
Vacuum brazing is a process for joining metal components, sometimes made from different metals, that is equally suited to small assemblies and to
more complex fabrications made up from many components. It is a process that offers design engineers a high degree of flexibility to produce engineered parts to meet differing technical and environmental challenges. Assemblies made by this process are exceptionally strong, shock and vibration proof. Wallwork technicians work with clients through the full design and development cycle form prototyping and testing through to volume production with total quality control and traceability.
Sales manager Howard Maher concluded, “Vacuum brazing is a relatively new addition to the range of metal improvement services available at this site. Achieving this additional Rolls Royce approval so soon after commissioning the new vacuum brazing area is a tribute to the skills and in-depth technical capability in the company and will help attract more high value aerospace work.””
“London, UK – [December 16 2025] – Bodycote, the world’s leading provider of advanced heat treatment and specialist thermal processing services, has achieved independent validation by Bureau Veritas for its proprietary product carbon footprint (PCF) calculators across nine core processes representing approximately 80 percent of Group revenues.
Customers can now request carbon-footprint data for the heat treatment of their products from a Bureau Veritas-validated calculator tool with the confidence that the methodology and tool used have been independently assured and calculations follow recognised best practice. This data will enable customers to:
● Measure and report product carbon footprints with confidence
● Compare the carbon performance of different thermal-processing routes
● Select lower-carbon options such as vacuum processing or low-pressure carburizing (LPC)
The validation was performed by Bureau Veritas, one of the world’s most respected providers of environmental verification services, in accordance with ISO 14064, the internationally recognized standard for greenhouse-gas accounting, validation, and verification.
“Validating our product carbon footprint tools through Bureau Veritas reflects Bodycote’s commitment to scientific integrity and leadership in sustainable manufacturing,” said Jim Fairbairn, Chief Executive Officer of Bodycote. “By providing robust, credible carbon data at the product level, Bodycote is helping manufacturers accelerate their journey to net-zero while also advancing our own strategic priorities — to optimise operations, perform efficiently, and grow revenues in lower-carbon service lines.”
“This initiative is a cornerstone of Bodycote’s sustainability and commercial strategy,” said Lily Heinemann, Chief Sustainability Officer at Bodycote. “The validated calculators represent a major step forward for a sector that has historically faced challenges in quantifying process-level emissions due to the technical complexity of thermal processing.”
“Sustainability and corporate strategy go hand in hand,” added Heinemann. “As we expand our low-carbon process portfolio, validated carbon measurement becomes a powerful enabler for both.”
“Mark Hemsath joins our team as a distinguished leader in aerospace heat treating and advanced furnace technologies. With more than 30 years of experience driving innovation in vacuum systems, nitriding processes, and high-performance thermal equipment, Mark has shaped the industry through both his engineering expertise and executive leadership. Recognized among the “25 Most Influential People in the North American Heat Treating Industry,” he has played a central role in advancing modern furnace design and metallurgical processing. Mark’s background includes guiding global operations for leading furnace manufacturers and overseeing the development of cutting-edge aerospace vacuum furnaces, Low-Pressure Carburizing (LPC) systems, Ferritic Nitrocarburizing (FNC) technologies, and large-scale gas and ion nitriding installations.
He has contributed to major aerospace programs, directed multimillion-dollar system deployments, and authored widely referenced papers and presentations that continue to shape best practices in the field. As Executive Consultant, Mark brings exceptional technical perspective and problem-solving capability to our team, supporting clients with expertise that spans advanced furnace engineering, nitriding, hydrogen and vacuum processing, and complex heat-treating methodologies. His strategic insight strengthens our ability to deliver highly specialized, reliable, and efficient solutions across demanding applications. Mark holds an MBA in Finance from the University of Toledo and a B.S. in Business from Miami University, complementing his technical depth with strong business and operational acumen.”
Over the years Mr. Mark Hemsath has held a variety of high-profile positions in the global heat treatment industry-making his a very well-known name in the industry. Most recently he was President, “Nitrex/UPC-Marathon/GM Enterprises” before parting ways with the company earlier this year after Austrian furnace builder “Aichelin” acquired the Nitrex/UPC-Marathon/GM Enterprises brands.
Since then, many have wondered where Mark would resurface, this photo offers us a suggestion. Mark can be seen second from the right in this picture posted shortly before Christmas which shows Mr. Thomas Wingens (second from the left) and his team at “Wingens Consultants” , a heat treat consultant firm located in Pittsburgh, PA, USA. While this photo did not include any details at all, it certainly points to Mark possibly joining the firm.
We are sure there will be more to this story.
New Commercial Heat Treater located in Tennessee
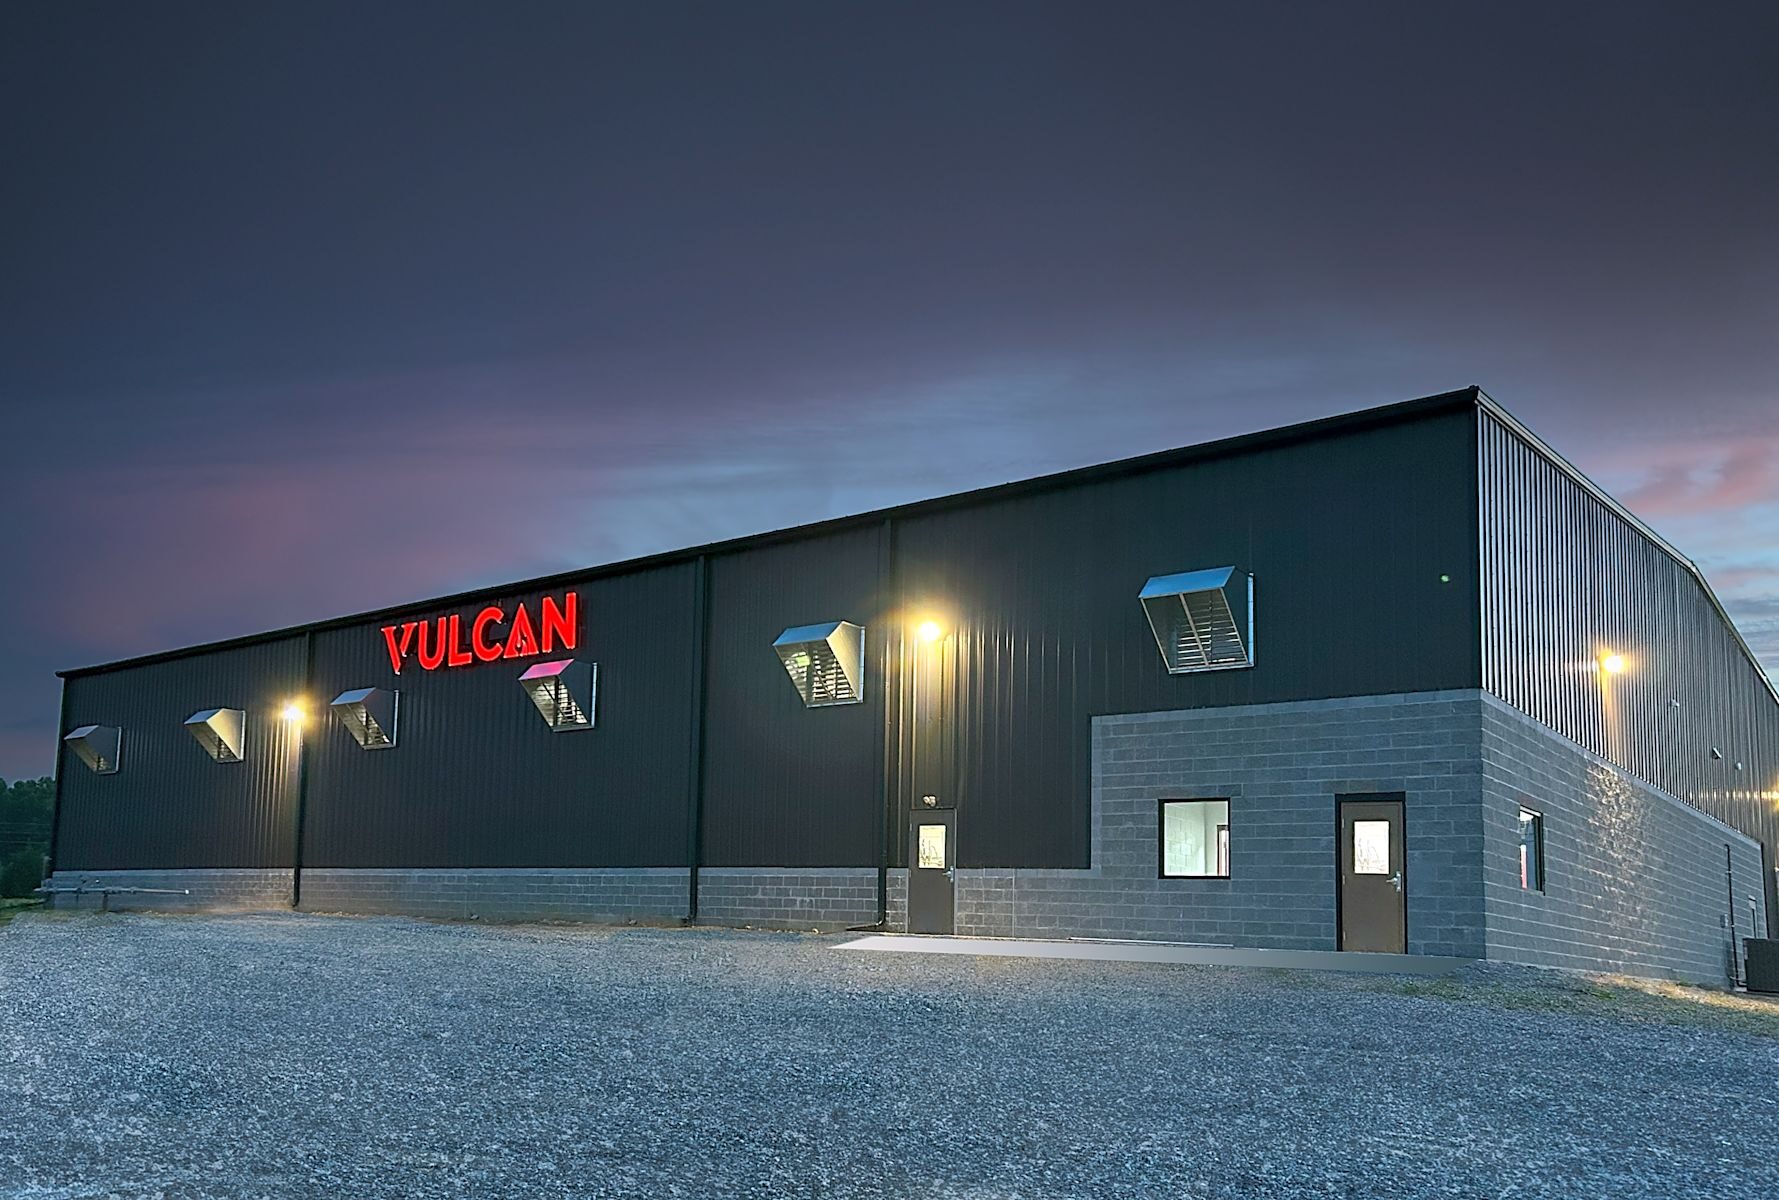
Vulcan Thermal has officially opened a new commercial heat treating operation in Surgoinsville, Tennessee, expanding capacity and shortening turnaround times for manufacturers across Northeast Tennessee and the surrounding region. The facility is located at 390 Phipps Bend Road in the Phipps Bend Industrial Park, positioning Vulcan Thermal close to a growing concentration of metalworking and manufacturing activity.
Announced in March 2024 with state and regional leaders, the project represents a $5 million investment and is expected to create approximately 30 new jobs in Hawkins County. The site totals 15,000 square feet, and supports Vulcan Thermal’s strategy of providing responsive commercial processing and value-added services for customers who need consistent results and dependability.
Built to serve regional manufacturers with faster lead times
Vulcan Thermal is a subsidiary of EHT, Inc., founded in 1984 and headquartered in St. Marys, Pennsylvania. In Tennessee and Pennsylvania, the organization provides heat treatment and related services to major suppliers in industrial segments including automotive and agricultural manufacturing, with the combined organization expected to employ nearly 100 people across both states.
Vulcan Thermal’s website emphasizes a “more than one operation under the same roof” approach—helping customers reduce lead times and transportation costs by consolidating steps that often require multiple vendors.
Equipment and capacity: installed today, room to grow tomorrow
The Tennessee operation is built with both immediate production capability and planned expansion in mind:
Two batch furnaces are currently installed.
The site is planned to add a third batch furnace.
The facility is also planned to add a 48-inch continuous mesh belt line, currently located on-site.
Importantly, the foundations for the planned installations have already been built, enabling a straightforward expansion path as customer demand grows.
This combination of current capacity plus “ready-to-install” expansion is designed to help regional manufacturers secure processing slots with confidence—especially when production schedules tighten.
Quality systems and metallurgical support
To support demanding manufacturing requirements, the Tennessee facility includes a full metallurgical lab and is continuously monitored for process control and traceability. The operation is fully CQI-9 compliant and ISO 9001 certified, aligning with the expectations of quality-driven customers in automotive and other critical supply chains.
Services designed to reduce handoffs and simplify finishing
Vulcan Thermal markets itself as a full-service operation supporting manufacturing customers, with core services including heat treating, steam treating, tumbling (mass finishing), and inspection.
The company also highlights additional support services—such as packaging and assembly—to help customers streamline outbound logistics and reduce vendor lead times.
In steam treating specifically, Vulcan Thermal positions itself as a long-time leader in the process, stating that with over 35 years of experience it remains the largest commercial steam treater in the United States.
Why Surgoinsville
In announcing the project, Vulcan Thermal cited the strong cooperation from state and local officials and the advantages of locating in Phipps Bend Industrial Park as key factors in the decision.
For customers, the benefits are practical: closer proximity to processing capacity can reduce freight cost, improve responsiveness, and create a more reliable path from production to shipment-ready parts.
Request a quote / contact
Vulcan Thermal is actively seeking new business relationships across Tennessee and neighboring states. For quoting, capability discussions, or to schedule a tour, visit.
Tennessee: 390 Phipps Bend Road, Surgoinsville, TN 37873
Pennsylvania: 316 Battery Street, Saint Marys, PA 15857
Interior heat treat area: “Inside Vulcan Thermal’s Surgoinsville, Tennessee facility—commercial heat treat capacity supported by on-site metallurgical resources, continuous monitoring, and an expansion-ready layout.”
Exterior building at dusk: “Vulcan Thermal’s 15,000-square-foot Surgoinsville, Tennessee operation, located in the Phipps Bend Industrial Park and built to expand with additional furnace and mesh belt capacity.”

 “Kencoa Aerospace has begun expanding its defense and space business in the North American market.






 Vulcan Thermal has officially opened a new commercial heat treating operation in Surgoinsville, Tennessee, expanding capacity and shortening turnaround times for manufacturers across Northeast Tennessee and the surrounding region. The facility is located at 390 Phipps Bend Road in the Phipps Bend Industrial Park, positioning Vulcan Thermal close to a growing concentration of metalworking and manufacturing activity.