
(Editor’s Note; In this press release Maciej Korecki, Vice President of the SECO/WARWICK Group’s Vacuum Segment states; “This order will support the production of components for gas turbines”. Recently “The Monty Heat Treat News” published an article entitled, “AI Data Centers Spiking New Vacuum Furnace Orders” which at least partially explains why demand is so strong for gas turbines).
“SECO/WARWICK will deliver an advanced single-chamber Vector vacuum furnace with gas quenching to one of the world’s most demanding markets—the Japanese high-tech sector. This is SECO/WARWICK’s first vacuum furnace order for this Partner.
The equipment will be delivered to a company specialized in the heat treatment of metals and the production of precision components for the energy, medical, automotive and machinery industries. The contract is being executed in cooperation with SECO/WARWICK’s Japanese vacuum segment trading partner.
The single-chamber Vector vacuum furnace is built on a horizontal structure and will feature a heating chamber with impressive working zone dimensions of 1016x1016x1524 mm (40″ x 40″ x 60″), allowing for the heat treatment of large and oversized components. The round heating chamber ensures excellent temperature distribution at ±5°C (±9°F). Additional heating elements in the doors and the rear wall further enhance temperature uniformity and reduce heating and soaking times.
The heart of the vacuum system is a powerful setup based on two mechanical pumps, a Roots pump, and a diffusion pump supported by a holding pump, enabling high operating vacuum and very clean heat treatment processes such as annealing, aging and brazing. The partial pressure system protects the batch surface from alloy element sublimation and minimizes the risk of contamination in the hot zone. The blower-based quenching system provides quenching pressure up to 6 bar abs., which is crucial for new types of blades and gas turbine components that require fast, controlled cooling while maintaining high material structure quality.
Japan: A Demanding Market; Entering the Japanese market with an advanced vacuum furnace is significant not only for business but also for branding.
“Japan is an extremely demanding market, very technologically mature and traditionally difficult for non-Japanese companies to enter. The fact that a renowned customer is investing in our solution confirms the highest quality of SECO/WARWICK technology. This order will support the production of components for gas turbines, which play a key role in improving energy efficiency and reducing CO2 emissions,” said Maciej Korecki, Vice President of the SECO/WARWICK Group’s Vacuum Segment.”

“
The new furnace significantly increases our heat-treating capabilities by expanding available processing capacity and improving workflow efficiency across our operations. With two Mentor Pro furnaces now in service, AGF DEFCOM can better manage production demands, reduce scheduling bottlenecks, and maintain consistent delivery performance for our customers.
Adding a second furnace also enhances overall productivity by allowing more jobs to be processed simultaneously. This increased flexibility helps shorten lead times, speed up turnaround times, and ensure we can continue meeting customer requirements without compromising quality.
As our business continues to grow, strategic investments like this enable AGF DEFCOM to stay ahead of customer needs while supporting future expansion. We are proud to strengthen our capabilities and look forward to delivering even greater value through improved efficiency, capacity, and service.”

With more than 10 years of experience in strategic marketing, business development, and market leadership, Vanessa has worked across aerospace, power generation, and other highly regulated industrial markets. She holds an Executive MBA from HEC Lausanne and is passionate about helping advanced technologies and manufacturing capabilities create safer, more resilient, and more sustainable industries.)
From New Product Introduction to Full-Rate Production: Why Heat Treatment Partnerships Matter in Aerospace
Aerospace OEMs and Tier 1 suppliers are increasingly turning to specialist heat treatment and surface finishing partners for rapid and scalable support across the New Product Introduction lifecycle, says Vanessa Pfeiffer, Director Strategic Market Development Aerospace, Defence & Energy
From New Product Introduction to Full-Rate Production: Why Heat Treatment Partnerships Matter in Aerospace
Aerospace OEMs and Tier 1 suppliers are increasingly turning to specialist heat treatment and surface finishing partners for rapid and scalable support across the New Product Introduction lifecycle, says Vanessa Pfeiffer, Director Strategic Market Development Aerospace, Defence & Energy
Aerospace manufacturers are under growing pressure to scale new platforms without compromising quality, capacity, traceability, cost control or delivery certainty. As programmes move from design and qualification into industrialisation and full-rate production, every process step must be capable of delivering repeatable performance at pace – especially where components are safety-critical, tightly specified and destined for long service lives.
Heat treatment and surface finishing remain critical to aerospace performance. As modern engines and structures operate at higher temperatures and stresses, thermal and metallurgical process history becomes more tightly coupled to design outcomes. With the right techniques and controls in place, demanding requirements for fatigue life, creep resistance and fracture toughness can be met consistently — not just in trials, but across repeatable production.
That makes metallurgical processing far more than downstream production steps. For OEMs and Tier 1 suppliers, specialist metallurgical providers are increasingly acting as strategic partners for industrialization and supply chain resilience. They help de-risk the journey from New Product Introduction (NPI) to series production, maintain continuity of supply, and scale production globally.
Increasingly, OEMs and Tier 1 suppliers are looking beyond technical processing capability alone, prioritising industrial partners with globally qualified production networks, multi-process capability, scalable capacity and operational redundancy to support industrial ramp-up and long-term programme resilience.
Why heat treatment and surface engineering matter
So, let’s look at the key stakeholders in the NPI programme for an aerospace component requiring heat treatment and/or surface coatings. There are three primary organisations involved. These ecosystems are led by original equipment manufacturers (OEMs) like Airbus and Boeing, who are responsible for the overall aerospace platform, defining requirements, and ensuring specifications are met. Then comes the component maker. Typically, these are Tier 1 or 2 supply chain partners that help design and build components for major systems, such as engines, landing gear, structures, and actuation and control.
Thirdly, there is the heat treatment and metallurgical service supplier. These companies often provide a portfolio of services. Heat treatment technologies might include case hardening, tempering, solution and ageing treatments, annealing, and normalising to help ensure component strength, hardness, toughness, ductility, fatigue performance and wear resistance, while preserving dimensional stability. These heat treatment processes are often applied to applications such as gear shafts and actuator shafts/rods.
Surface coatings represent another set of processes that prolong component life and protect them from environmental factors such as corrosion and abrasion. These might include high-velocity oxygen-fuel and plasma spray processes, and organic, ceramic, and polymer coatings applied to parts such as combustion liners and transitions, compressor blades and landing gear parts.
Meanwhile, some heat treatment and metallurgical process suppliers, such as Bodycote, also provide specialist services, like Hot Isostatic Pressing, which uses high heat and pressure to transform metal into a 100% dense solid. This technique is critical for high-integrity parts in demanding aerospace applications such as turbine blades and vanes, brackets and mounts and landing-gear interface components.
Design and process definition
On NPI programmes, in particular, OEMs, component manufacturers, and specialist heat treatment and surface finishers form close tri-party relationships, often as early as possible in the design cycle. These early-stage interactions can add significant value across the aerospace ecosystem – from design through to delivery and MRO – and are particularly important for long-lifetime platforms that can last decades.
So, what do those NPI relationships look like in the real world? Often, they begin at the design and process definition stage. Here, engineers, methods teams, and quality specialists from all three organisations get together to define the materials, processes, and testing requirements for a specific NPI component. Key programme outcomes must be defined, including performance requirements, preliminary component designs, initial specifications, and the identification of critical materials and properties.
In today’s more integrated supply chains, heat treaters and surface finishers advise on specifications and optimise processes for efficient industrial production. This technical consultancy includes advising on part design for manufacturability. Consequently, these organizations are often locked in early on multi-year aerospace platforms, delivering value from end to end.
Feasibility and qualification
The next stage in NPI development is feasibility and qualification. Here, input from specialist metallurgical providers helps streamline processes, often through the elimination of certain machining or grinding workflows. At this point, with the specifications and initial designs in place, component suppliers such as machining companies, forging houses, and casting shops translate them into actual manufacturing workflows.
Again, metallurgical process providers play an important role, helping validate feasibility, interpret requirements, and ensure parts are produced safely and consistently. With comprehensive material and process testing capabilities, specialist providers can collaborate with component suppliers to develop specific heat treatment cycles, temperature profiles, and surface hardness targets, while running Design of Experiments to optimise processes.
Prototyping and early trials establish technical trust and determine who is positioned to support the programme during industrialization. Structured trials and process validations, often including microstructure analysis, provide the component supplier with confidence for consistent production capability and adherence to quality system compliance.
Transition to series production
As the part moves into development, the NPI phase marks a transition from engineering and process specialists to production teams, with the focus shifting to operational performance. Metallurgical process specialists help demonstrate process repeatability and quality control, while developing predictable cycle times and scheduling for reliable execution that aligns with customer sales, inventory, and operations planning (SIOP).
The expectation here is for the specialist provider to demonstrate proven expertise in NPI-to-series handover methodologies, resulting in consistent lead times, accurate yield deliverables, and rigorous quality compliance, thereby eliminating the risk of bottlenecks for the component maker. Proactive communication ensures transparency and visibility into project progress.
Meanwhile, effective, flexible, and scalable production strategies are put in place to support strong capacity planning for demand fluctuations. Suppliers must be equipped to manage “short cycle” customer requirements when necessary, often going over and above contractual expectations. And stringent traceability and monitoring need to be put in place for optimized performance.
Long-term production
Long-term production comes next. Successful full series production depends on how well metallurgical process providers can integrate with customers’ operational rhythms. Large suppliers rely on structured SIOP systems and expect partners to meet forecast and capacity requirements. Aerospace programmes can run for many years, and OEMs seek long-term agreements with the supply chain – often through dual-supplier strategies – and based on investment commitments that deliver continuous improvement and capacity growth.
Heat treatment and surface finishers must demonstrate access to worldwide production networks, while maintaining backup and mitigation strategies to enhance supply chain resilience and address single-source concerns. A proven willingness to invest in capital equipment and automation to reduce costs and enhance efficiency can provide a sustainable long-term advantage. These providers must be resourced to manage any operational issues, while providing flexibility for customers’ internal versus external processing mix.
These capabilities are crucial to long-term supply chain resilience. Geographic flexibility and dual-source strategies reduce operational risk, allowing work to be transferred between sites when required. This helps maintain continuity, even during the most severe demand spikes. Metallurgical partners are therefore not only evaluated on technical capability, but also scalability, multi-site redundancy and long-term programme stability.
The power of partnership
With decades of experience in the aerospace sector, Bodycote can support all stages of the NPI lifecycle and enjoys preferred status with many major aerospace companies, including Airbus, BAE Systems, Boeing, Honeywell, Pratt & Whitney, and Rolls-Royce.
Knowledgeable and experienced teams of engineers, scientists and technicians can provide technical support at the design, testing and qualification stages, with services including design-to-cost, spec interpretation, engineering feasibility, test optimization and NPI readiness.
This is backed by a global network of aerospace-approved facilities that supports flexible capacity allocation, multi-site redundancy and scalable production across aerospace programmes. This operational flexibility helps customers maintain continuity across fluctuating production schedules and long programme lifecycles.
Ultimately, aerospace OEMs and Tier 1 suppliers are increasingly seeking strategic manufacturing partners like Bodycote to help next-generation platforms reach for the sky.

“June 2026; Texas Heat Treating is pleased to announce that the company is now registered with the U.S. Department of State’s Directorate of Defense Trade Controls (DDTC) under the International Traffic in Arms Regulations (ITAR).
This registration authorizes Texas Heat Treating to receive, handle, and process defense-related articles, technical data, and services that are subject to ITAR requirements. Our ITAR registration further demonstrates our commitment to supporting customers in the aerospace, defense, and other regulated industries while maintaining strict compliance with applicable U.S. export control regulations.”

 Since we are in the midst of the world’s largest sporting event of 2026 “FIFA World Cup 2026™, please allow us to use a “sporting” term for the title of this press release.
“McLaughlin Furnace Group” of Avilla, Indiana, USA is pleased to announce that in the past few months they have seen an unprecedented surge in interest for nitriding systems which has resulted in 3 orders (a hat trick in soccer and hockey parlance means 3 goals-hence our use of the term) in just the past few months. The orders come from two different in house heat treaters and while not all of the systems are exactly the same, each system is very similar. As an example one of the gas fired systems has working dimensions of 36″ X 72″ with a weight capacity of 5,000 pounds, an operating temperature of 850F-1250F, +-15F with an Inconel 600 Retort.
“John Hillenbrand”, Sales Manager for “McLaughlin” had these comments;
“We have seen a significant increase in RFQs for nitriding over the past few months which has led to 3 new pit nitrider orders. The nitriding market is booming and needs new capacity now. We pride ourselves on being able to provide the highest quality furnaces in a fraction of the time. Ultimately, this was key in being awarded these new nitriding furnaces. As an example, while our competition was quoting 34 weeks, we were able to offer a delivery of 16-18 weeks-a delivery which we are on track to meet. “

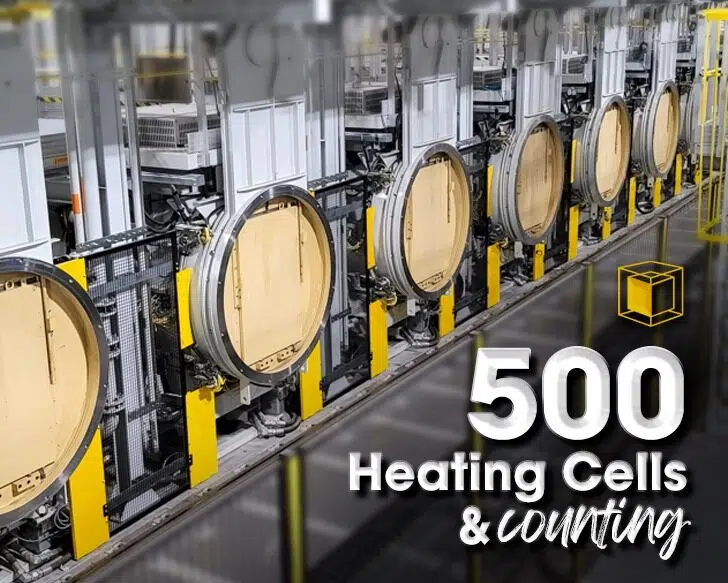
Pleasant Prairie, WI – June 22, 2026 – Just over a year after celebrating a long-standing automotive customer’s achievement of processing their 1,000,000th load through their ECM vacuum furnace systems, ECM has achieved another major accomplishment – the commissioning of the 500th heating cell in North America (Canada, USA & Mexico).
These furnaces range from single-cell to large-scale multi-cell installations with multi-process capabilities, such as: LPC, FNC, nitriding, brazing, sintering, debinding, degassing, high pressure gas and oil quenching, and more. Over the past five years, many of these installations have incorporated ECM Robotics for material handling and integrated pre-/post-processing equipment to create fully automated, all-inclusive manufacturing solutions. This milestone reflects the continued confidence that commercial and captive heat treaters place in ECM technology, service, and expertise. ECM remains committed to delivering advanced furnace solutions and services, and we look forward to supporting the North American heat treat industry with the next 500 heating cells & beyond.
About ECM Technologies. ECM Technologies is an innovative low pressure vacuum furnace manufacturer with headquarters in Grenoble, France. With subsidiaries and ventures around the world, including ECM USA located in Pleasant Prairie, Wisconsin USA. ECM’s global presence is well known in the automotive, aerospace, nuclear, energy, electronic, induction and 3D additive industries. With such versatile product lines and service capabilities, ECM is the ideal furnace system supplier for heat treatment processes ranging from rapid thermal processing (RTP) to low pressure vacuum carburizing (LPC). Our service capabilities include advanced automation, robotics, after sales, spare parts, on-site training and more.
(Editors Note; While it is not mentioned in this press release the new vessel is being built by “American Isostatic Presses Inc”. of Ohio.
“Kittyhawk Inc has placed an order for a new Hot Isostatic Pressing (HIP) vessel for installation at its Garden Grove, California, USA, facility. The investment is intended to support growing demand for HIP services from the commercial aerospace, space and defence sectors, as well as other industries. The additional capacity is expected to help address increasing production requirements, complex supply chain demands and shortened delivery schedules.
The new vessel, measuring 1.17 × 2.54 m, will increase the company’s processing capacity for a range of component sizes and is expected to improve throughput at the Garden Grove site. Kittyhawk states that the expansion will help reduce production bottlenecks, improve turnaround times and provide greater scheduling flexibility for customers operating in regulated industries.
Founded in 1981, Kittyhawk provides HIP services to customers in the aerospace, defence, automotive, oil and gas, and medical sectors. The company operates in accordance with AS9100 and Nadcap requirements, complies with International Traffic in Arms Regulations (ITAR) and Export Administration Regulations (EAR), and holds a Class 07 Federal Firearms License (FFL).
The investment forms part of the company’s ongoing expansion strategy as it seeks to increase HIP capacity and support future customer requirements.”

On a regular basis “The Monty Heat Treat News” informs the industry about individuals in the industry making career changes-promotions, retirements, changes in direction-these are the individuals who make our headline for Friday, June 19th 2026;
- Christian Saint-Denis Retiring. While not well known to the global heat treatment industry, “Christian Saint-Denis” held a high level position in the heat treatment department at fastener manufacturer “Infasco” in Marieville, Quebec, Canada. “Infasco” operates one of the larger in-house fastener heat treat departments in North America. His retirement is immediate.
Earlier this year “The Monty Heat Treat News” had an in-depth article entitled; “Is There a Shortage of Large Pit Carburizing Capacity in North America?”. The story provoked such an avalanche of interest that we are providing regular updates on this topic, and today we have another update about new pit carburizing capacity being added.
“Northern Heat Treat” in Capreol, Ontario, Canada (which might hold the distinction of being the northern most commercial heat treater in North America) has announced that they are bringing on line more pit carburizing capacity.
The firm has always serviced the mining industry, which typically means large gears and shafts and in the face of increasing demand for large pit carburizing capacity (their words, not ours) they have initiated the installation of a large pit carburizing furnace. Planned production startup of the gas fired 92″ deep furnace is Q3-Q4 of this year.
We will keep you updated on this and other stories related to pit carburizing capacity in North America and abroad.
