“Rockbreaker” is a trade name for a steel hydraulic hammer tool used in the construction, mining, quarrying and demolition industries to literally break rock and concrete. The name is owned by “Caldervale Group Ltd”., of Airdrie, Scotland who manufacturers and ships the tools around the world with North America being their largest market.
“All Rockbreaker steel tools are manufactured from top quality steels, machined and heat treated in the company’s own production facilities in Calderdale, Airdrie ensuring that each breaker tool has the consistent impact, strength, hardness and ductility needed in the rugged conditions experienced in the construction, mining, quarrying and demolition industries.
Rockbreaker Steels are totally manufactured under a strict quality control management system certified to British Standard BS EN ISO 9001, 2008 ensuring the production of superior quality breaker steels. We are committed to research and development as an integral part of our existence to produce the world’s finest most versatile hydraulic breaker steels deserving the world-wide earned reputation. Continual improvement in process`s and procedures.”
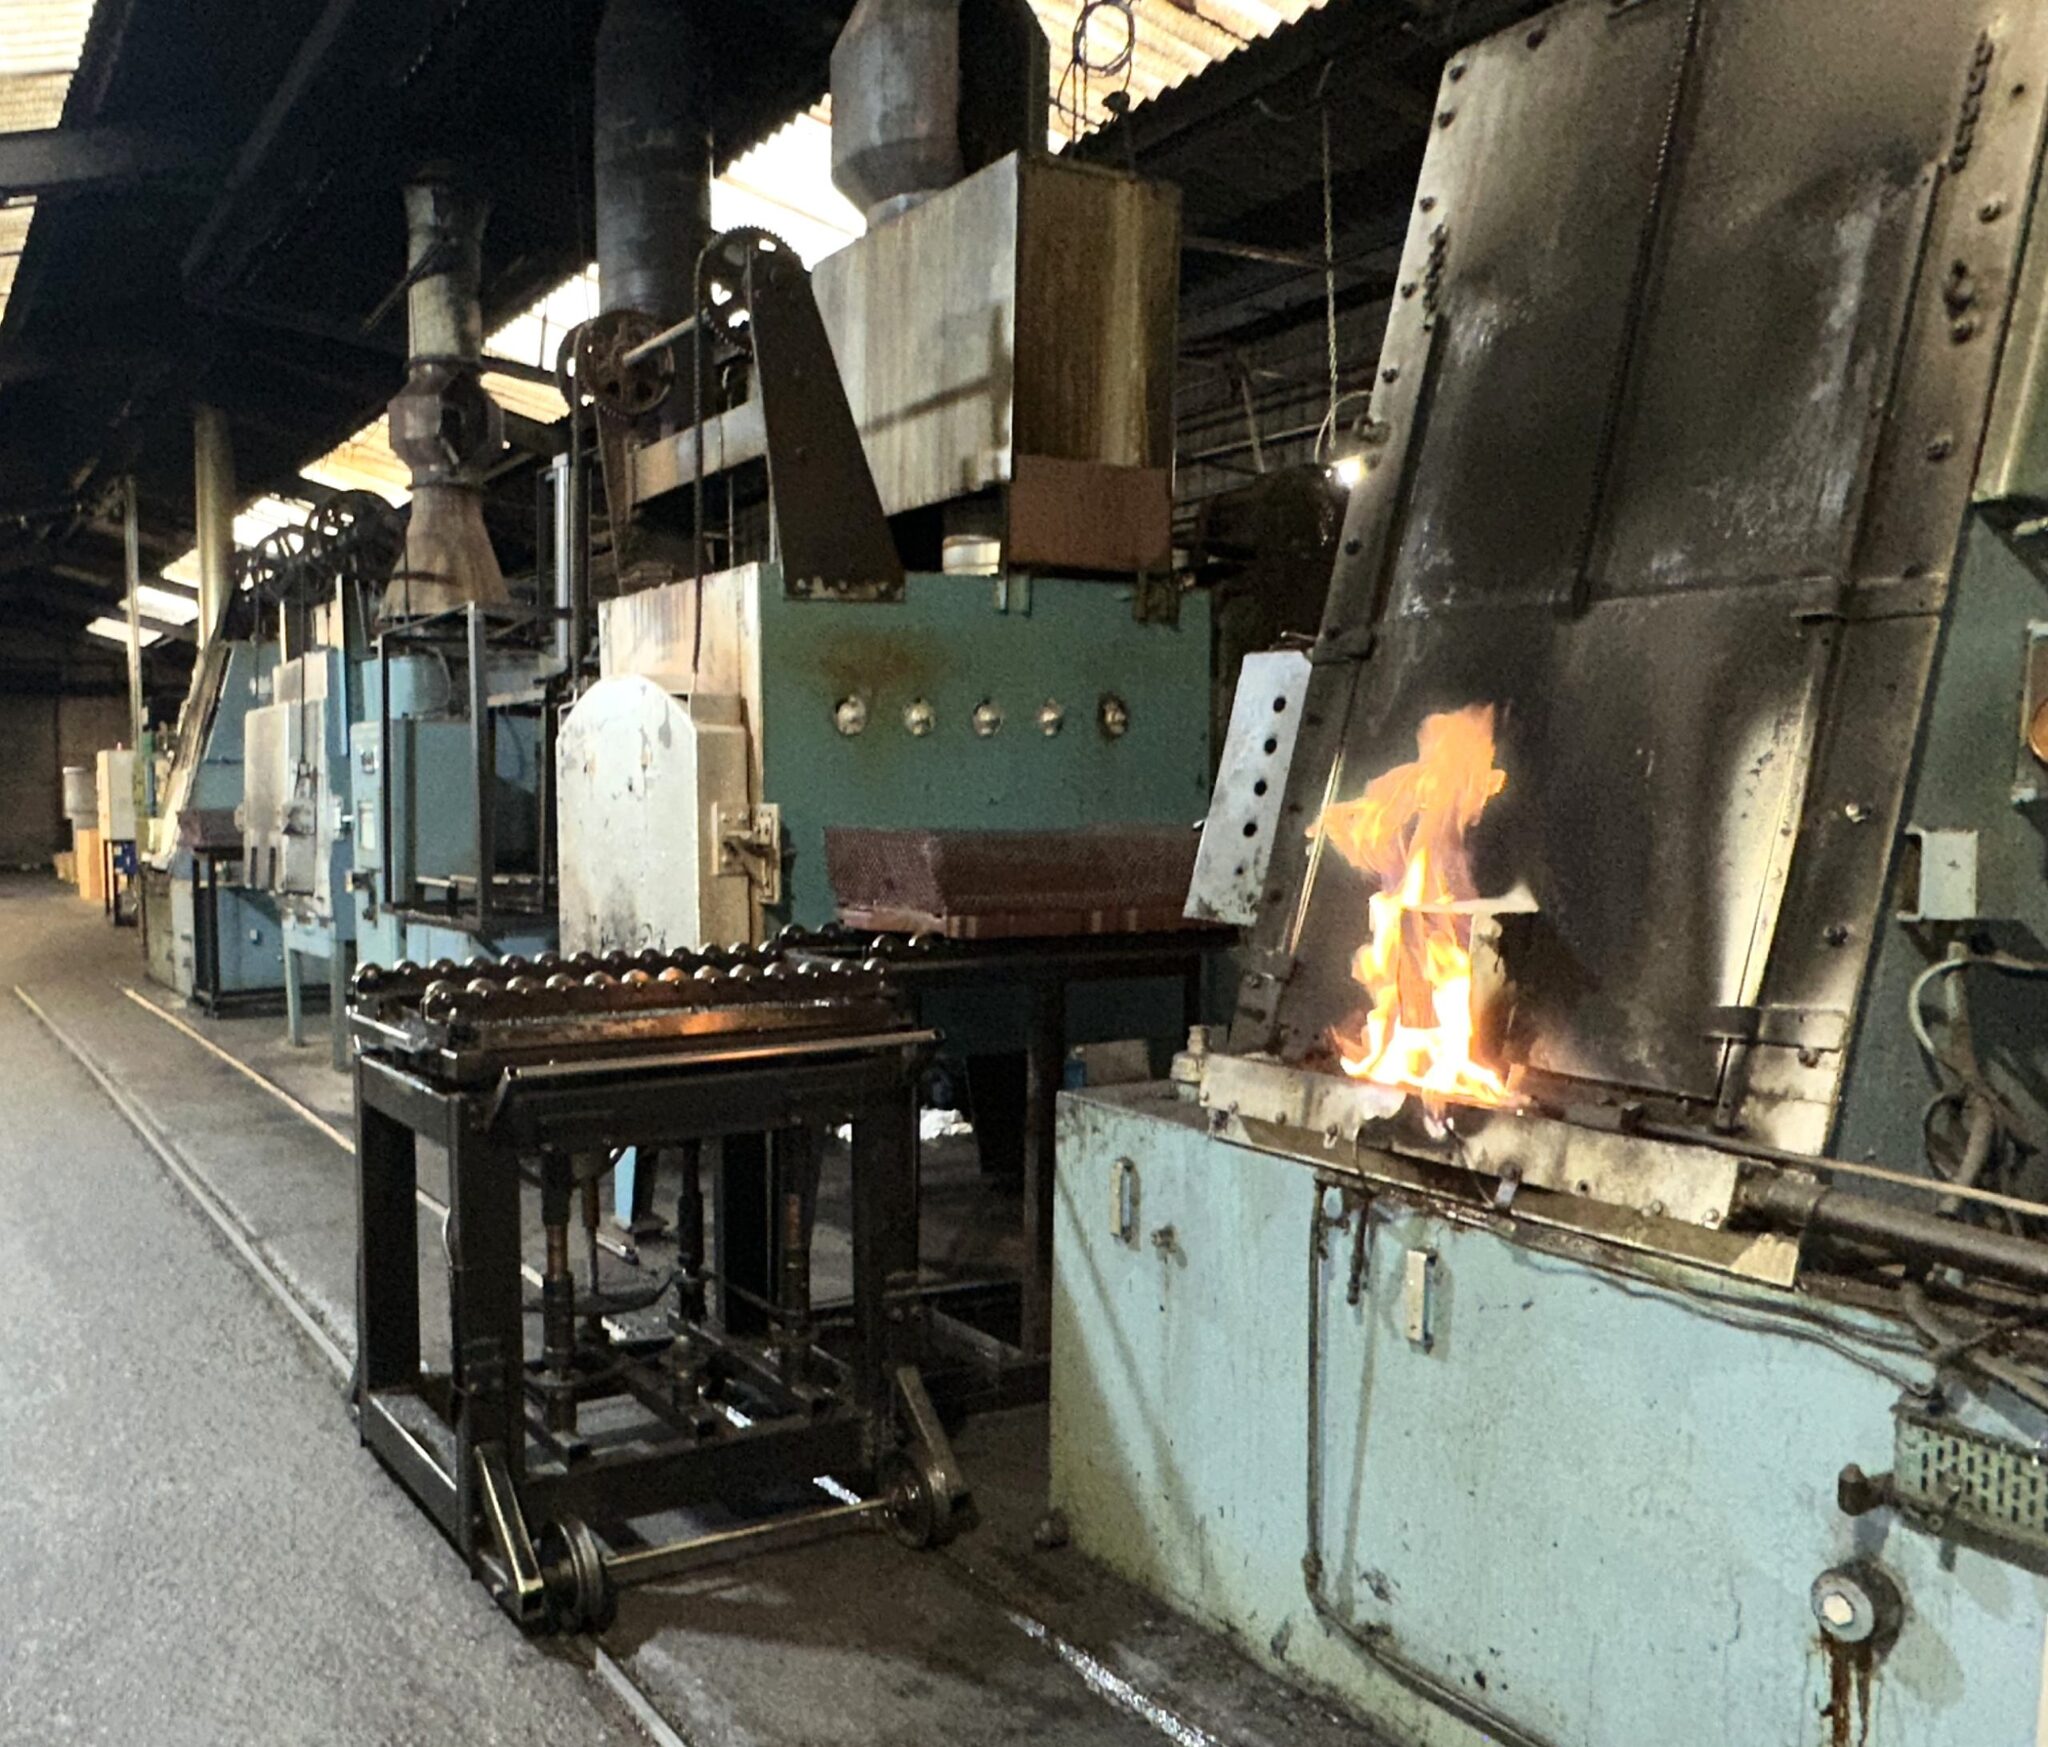
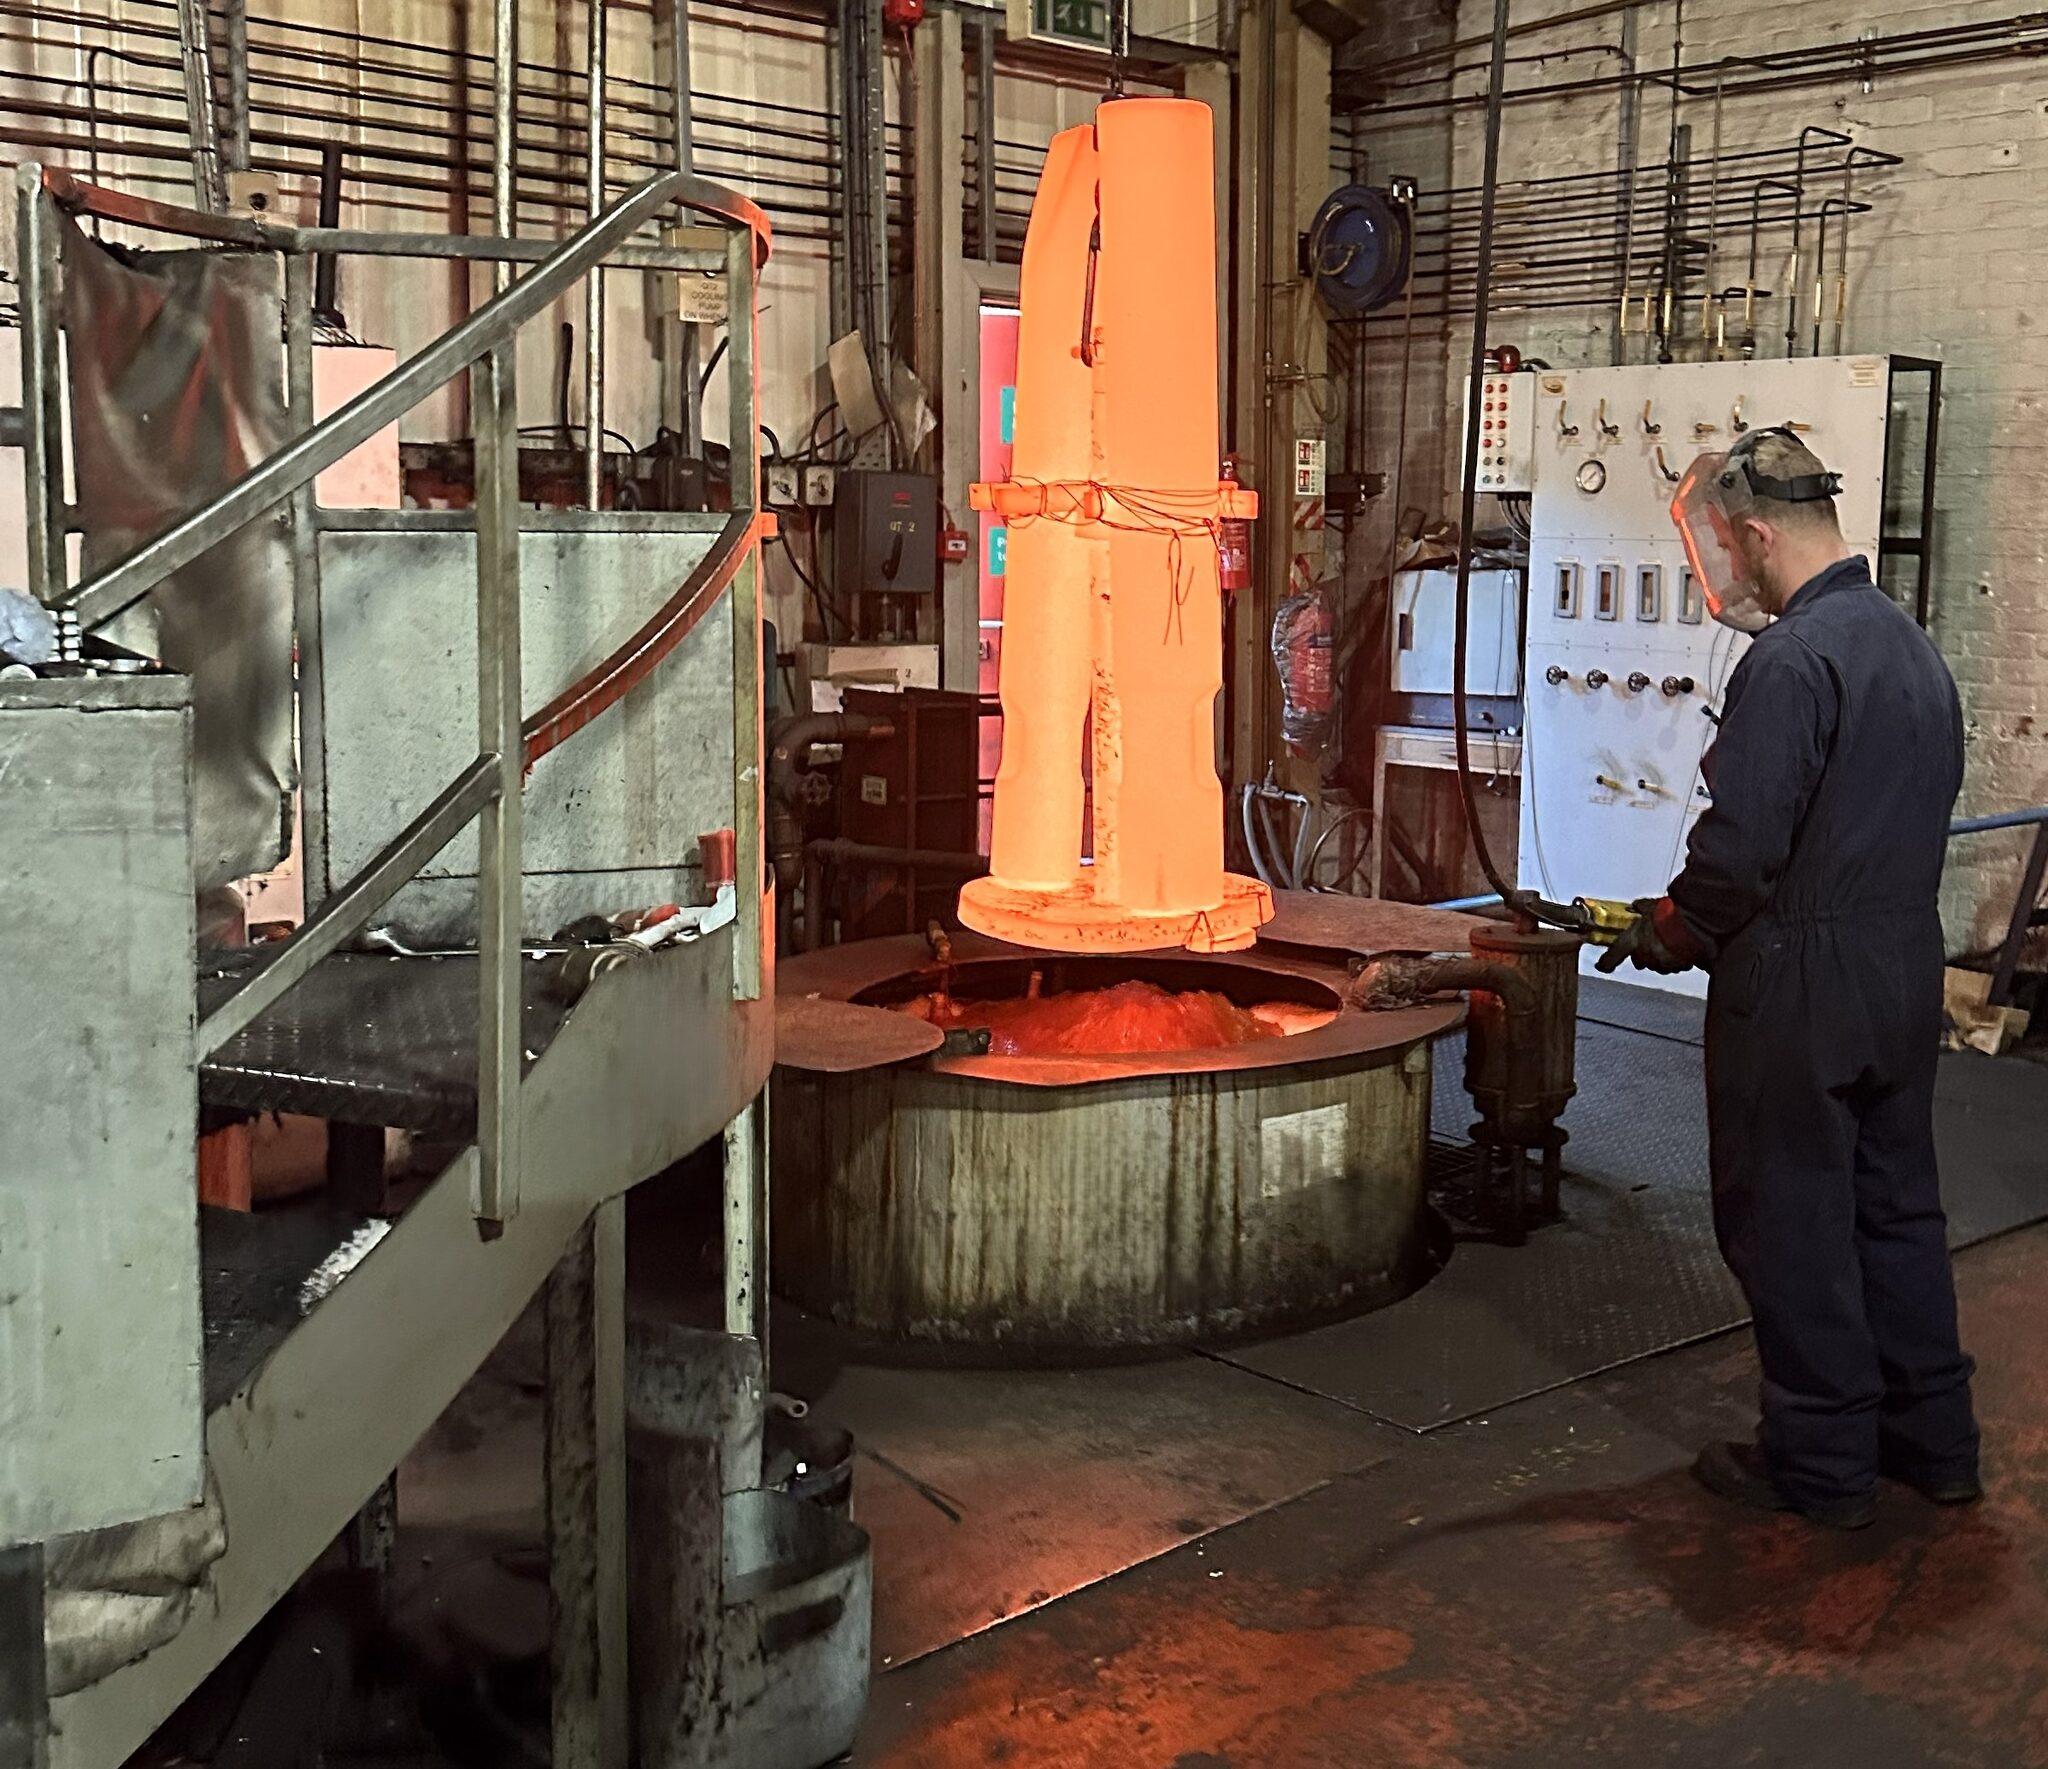
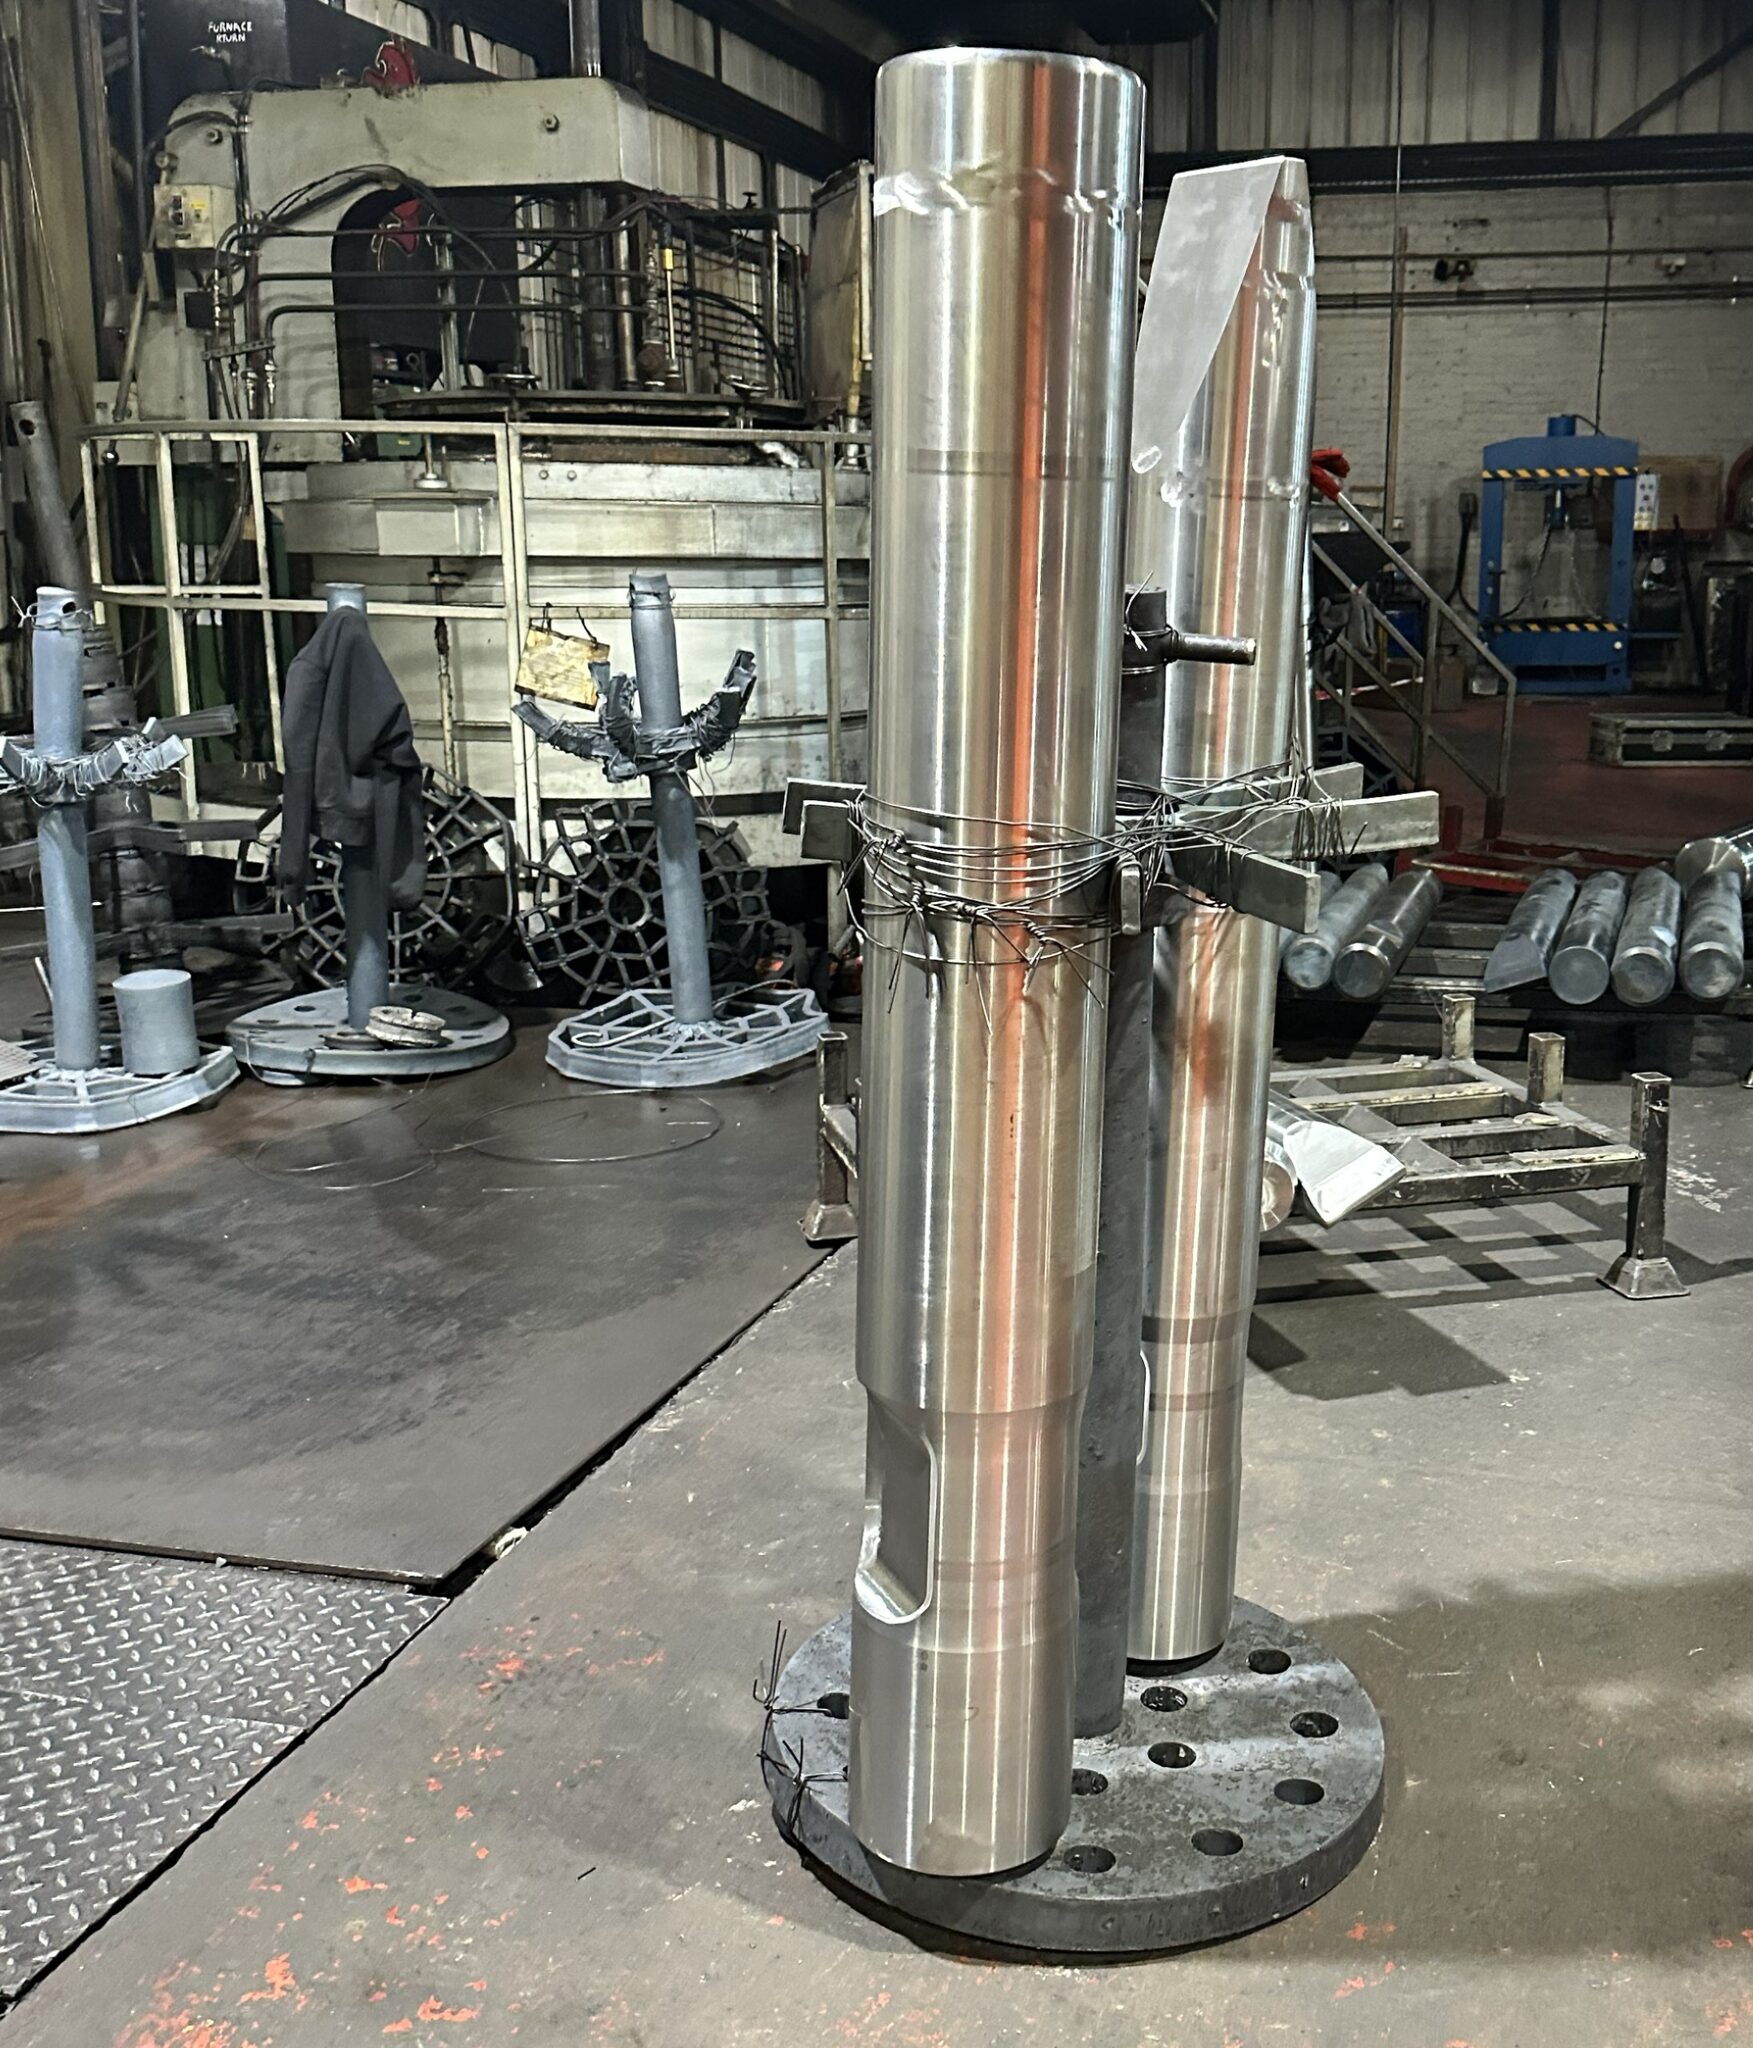
Rockbreaker Tools Prior to Heat Treatment
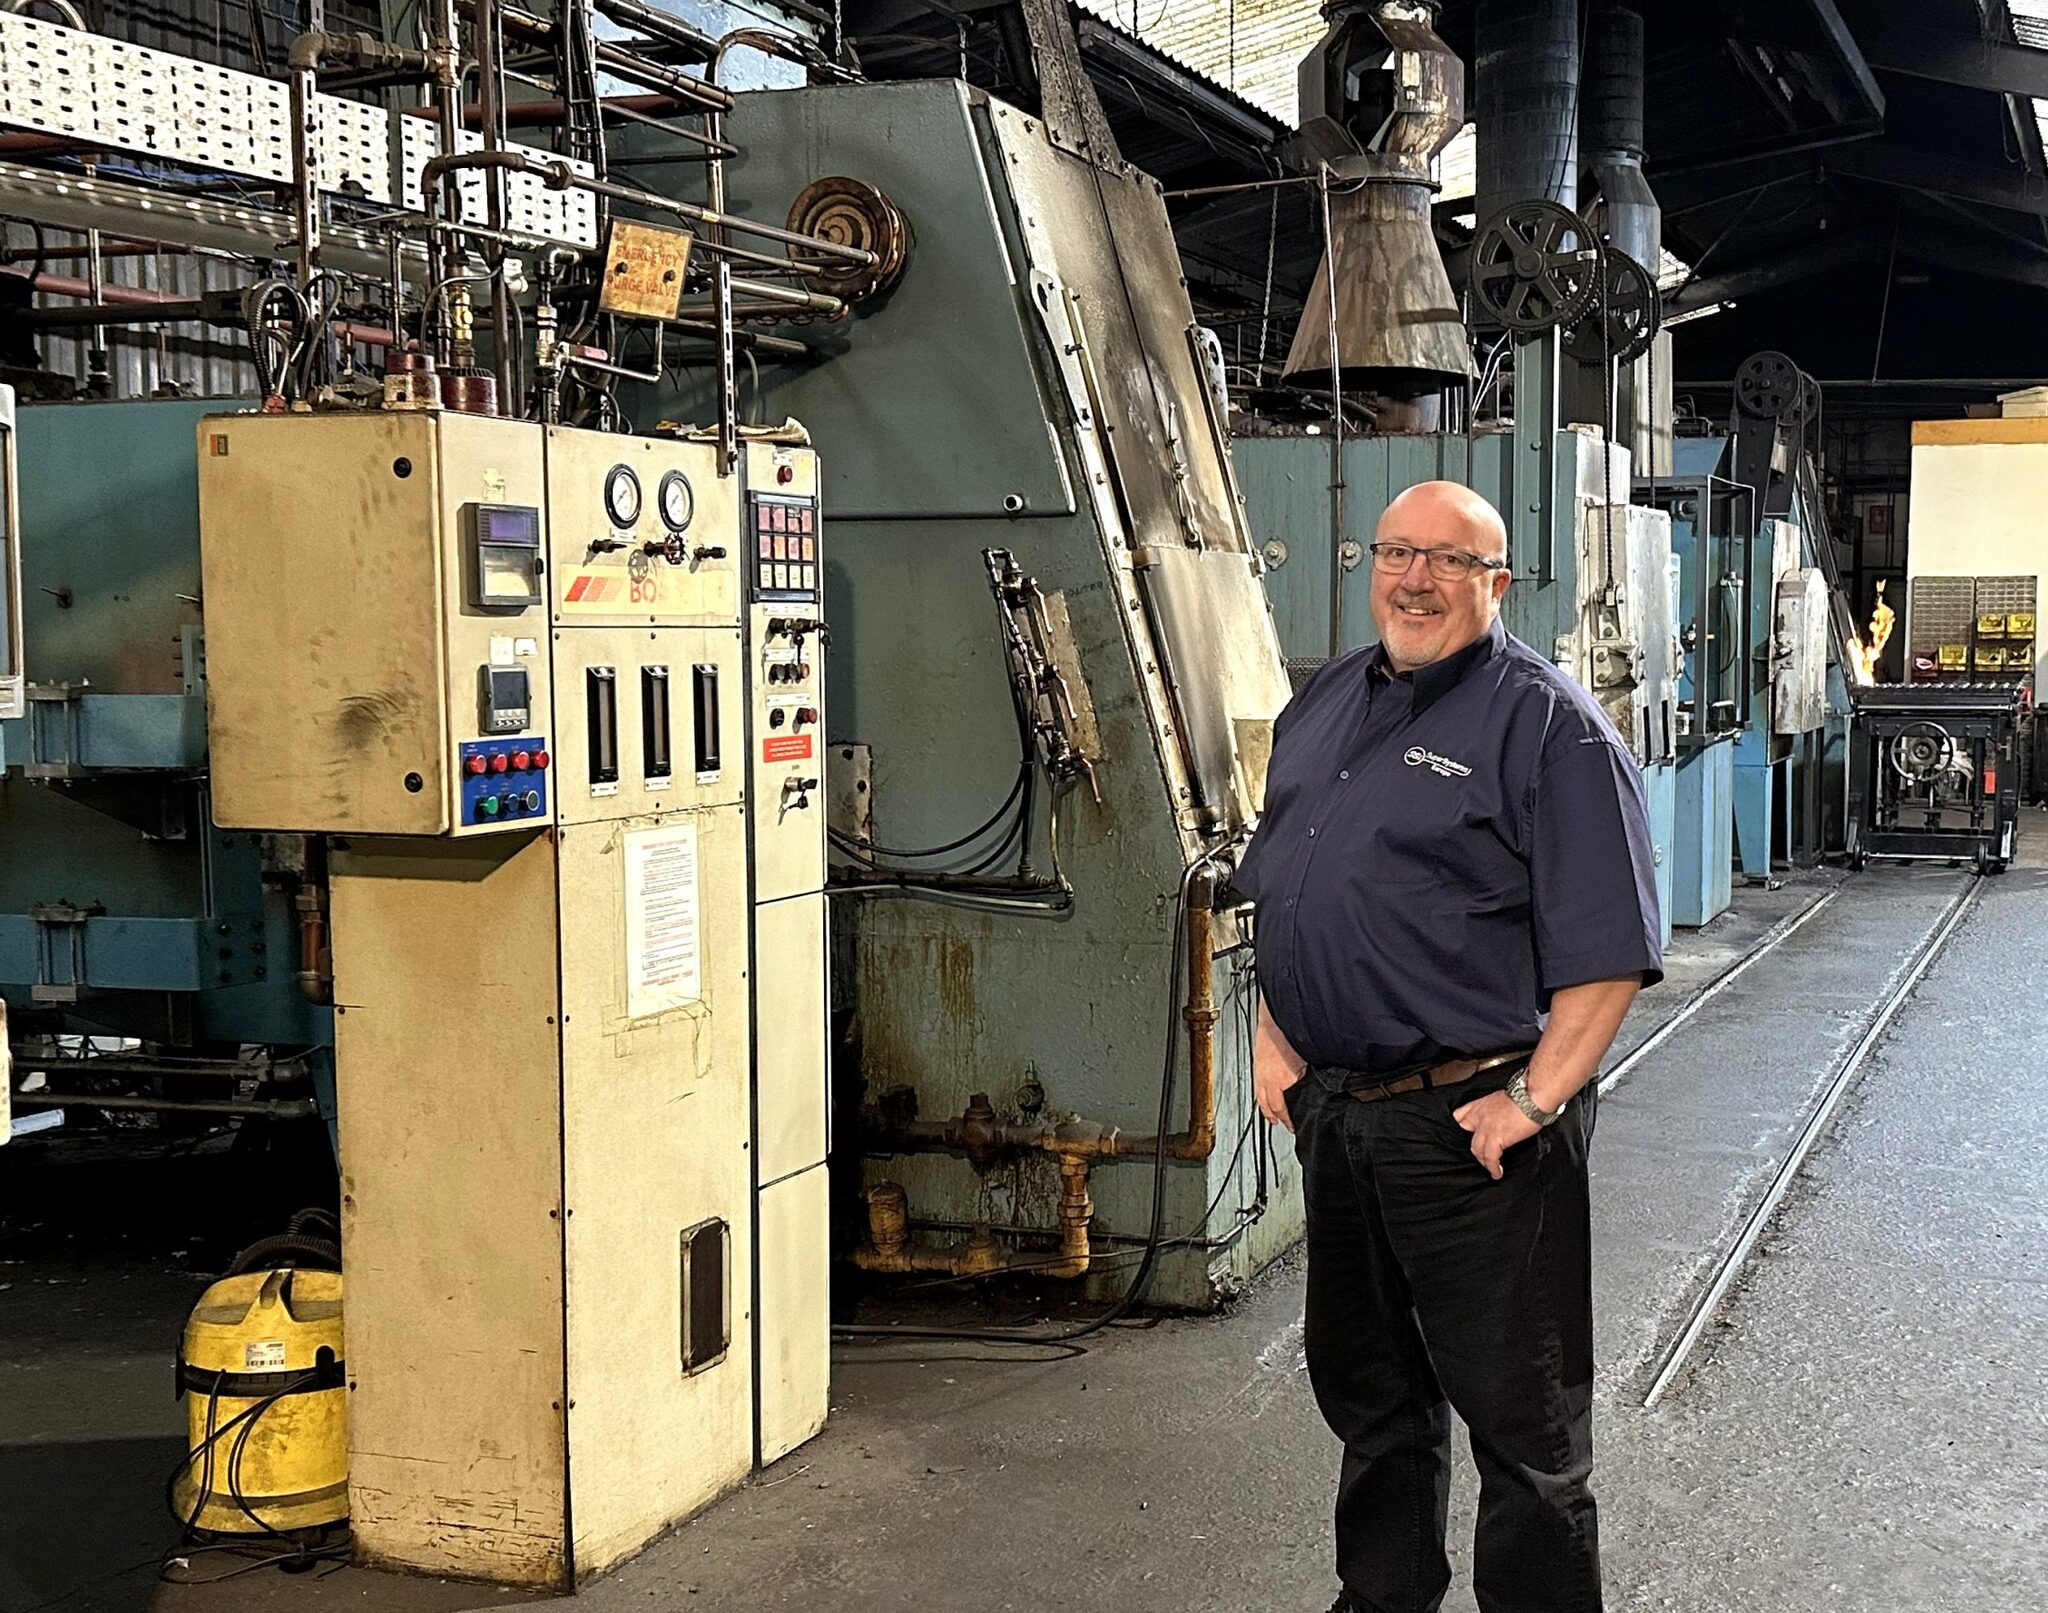
Monday November 10th, “Gord Montgomery” of “The Monty Heat Treat News”had the privilege of a guided tour of the facility, courtesy of Mr. Jim Hamilton, Technical & Sale Manager for the company.
This being our first experience with hydraulic hammer tools we weren’t entirely sure what to expect, as it turns out the heat treatment process for hammer tools is very similar to rock drills-carburizing in pit furnaces using an endothermic atmosphere with oil quenching-in the case of “Caldervale” the company has two reasonably large pit furnaces.
The pit furnaces form only a small part of the firm’s heat-treating capacity as “Caldervale” also operates as a commercial heat treater-the largest in Scotland as it turns out. To compliment the pit carburizing furnaces we found two induction systems (one a very long vertical scanning system, the other a dual spindle scanner) and several stress relieving, annealing and normalizing furnaces.
The centerpiece of the entire department is a substantial “salt” system offering the “QPQ” process-for those not familiar with this process we have this brief summary;
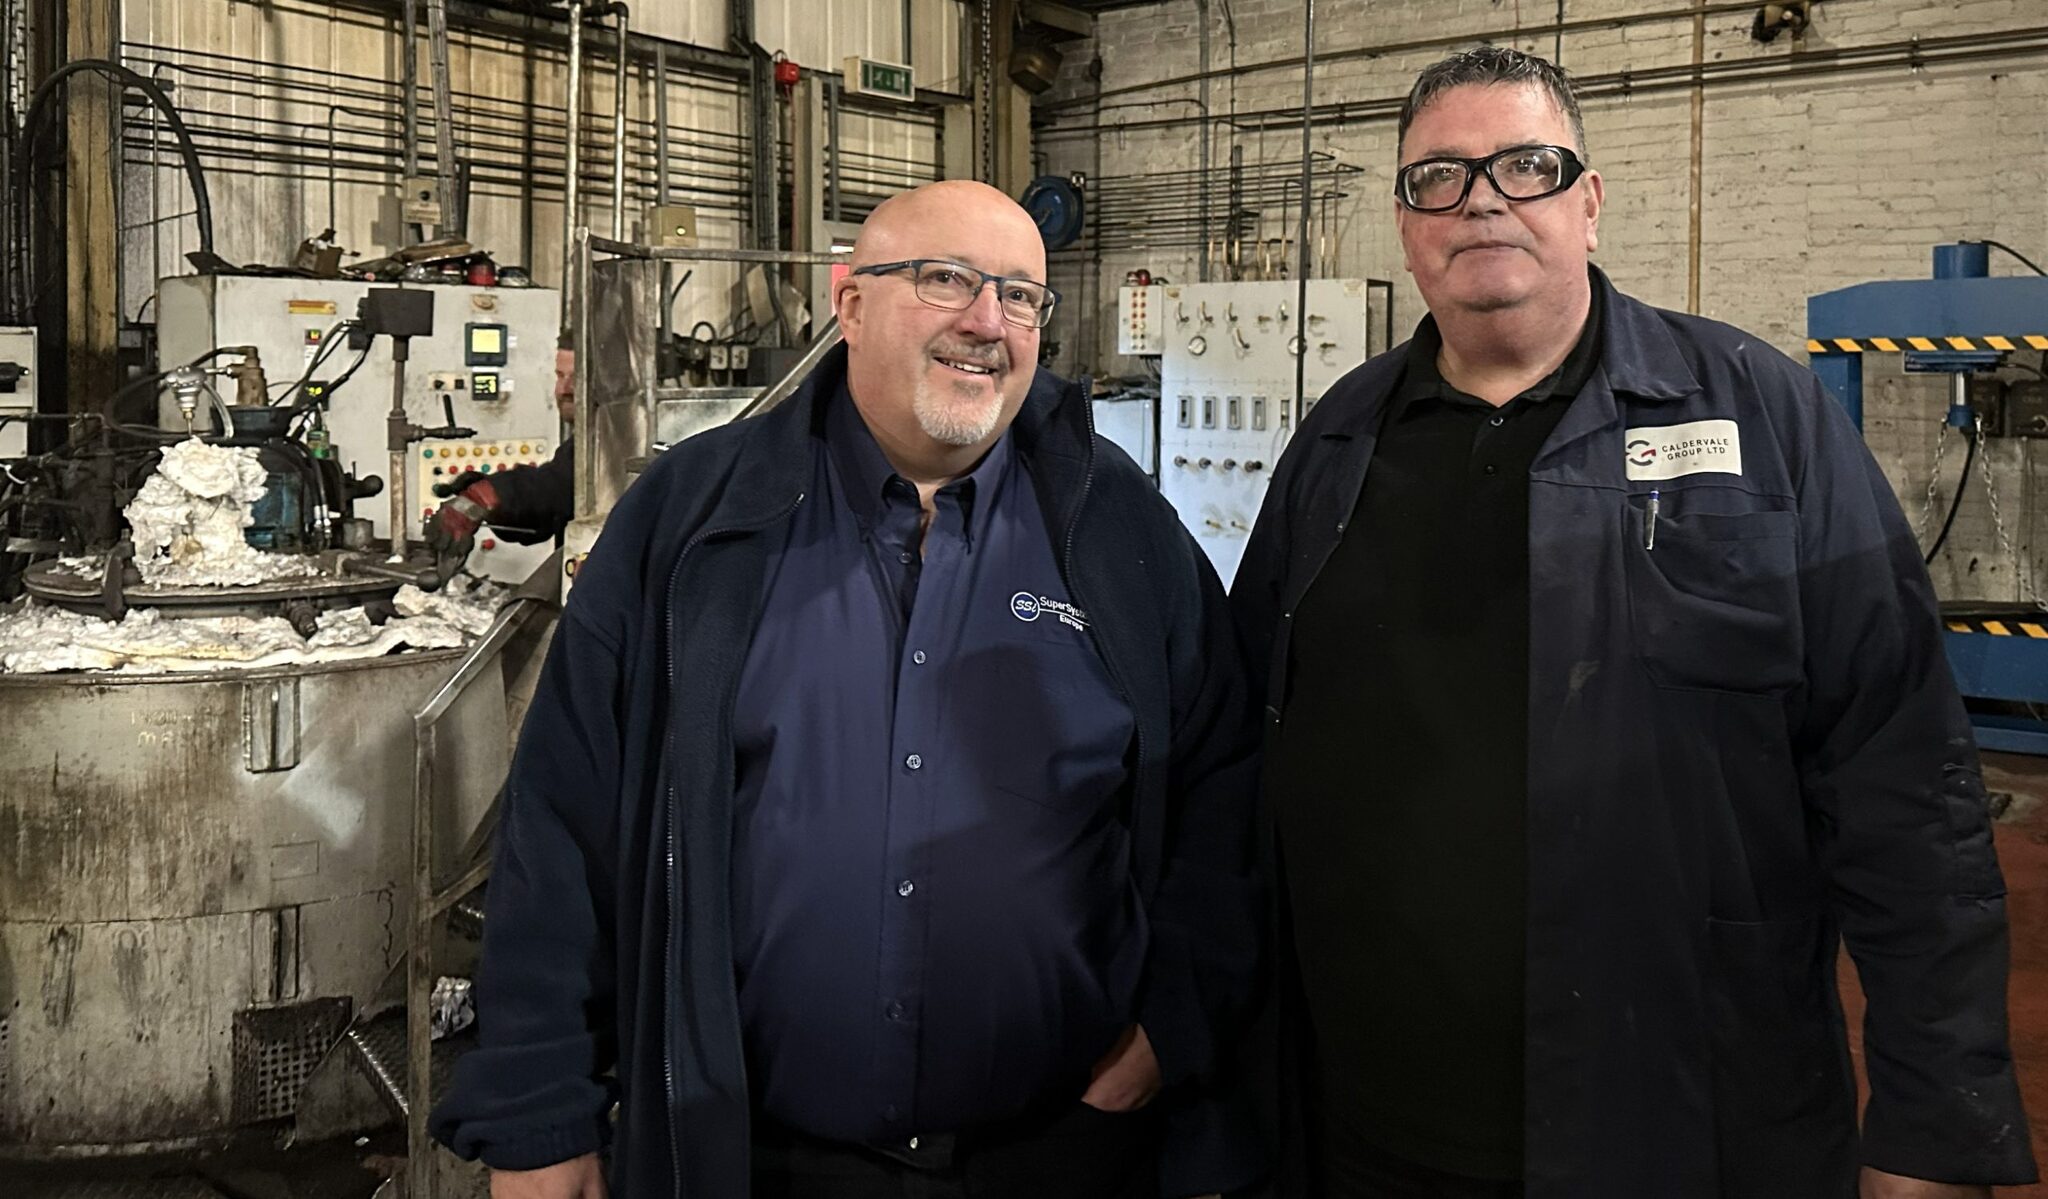
Nigel Troth, Sales Manager, SSi Europe, Jim Hamilton, Technical Sales Manager Caldervale Group
“QPQ” is a thermochemical surface treatment process that uses “quench, polish, quench” to significantly improve a metal’s wear resistance, corrosion resistance, and fatigue strength. It involves three main steps: an initial quench (nitrocarburizing) to form a hard compound layer, followed by a polish to improve the surface finish, and a final quench (oxidation) to create a corrosion-resistant oxide layer. This process results in a durable, black surface that can replace other treatments like chrome plating and minimizes distortion in the treated parts.”
Joining us in our tour was Mr. Nigel Troth, Sales manager for furnace controls company “SSi Europe”.
We thank Jim Hamilton for his time and his openness about the company.
“QPQ-Tuffride”; Gord Montgomery, “The Monty Heat Treat News”, Jim Hamilton, Technical Sales Manager, Caldervale Group
August 19th of the year we had this news item about a new commercial heat treating facility in Fairfield, Ohio, USA “Bodycote Opening New Facility in Fairfield, Ohio, USA”–we now have this update about the location achieving Nadcap Accreditation (Editors Note: while vacuum carburizing is not mentioned in this press release about being offered at this location the furnace picture sures looks to us like a multi chamber vacuum carburizing system).
“Bodycote, the world’s leading provider of advanced heat treatment and specialist thermal processing services, has announced that its new facility in Fairfield, Ohio, has achieved Nadcap accreditation for heat treating, vacuum brazing, and TIG welding, marking a key milestone in the site’s progression toward full operations.
This investment strengthens Bodycote’s North American footprint and supports growing demand for high-specification thermal processing in the aerospace, defense, and industrial manufacturing sectors.
Construction of the 55,000-square-foot facility began in March 2024, with initial production trials underway since March 2025. Strategically located in Fairfield, just north of Cincinnati, the site offers proximity to key customer hubs across Ohio, Indiana, and Kentucky—enabling faster turnaround times and enhanced logistics efficiency for regional manufacturers.
With Nadcap accreditation secured, Bodycote is now entering the final stages of customer qualification and production ramp-up. The facility is equipped with a state-of-the-art braze department, vacuum furnaces, aluminum furnaces, TIG Weld, FPI, and is designed to meet the most demanding performance and quality standards required in critical industries.
“This accreditation underscores our commitment to quality, consistency, and service excellence for our customers,” said Heidi McNary, President, Global ADE and Surface Technology at Bodycote. “Fairfield represents a key addition to Bodycote’s North American network, providing increased capacity and proximity for customers in this important industrial corridor.”
The Fairfield site is now accepting customer qualifications and new production work, with full-scale operations expected by January 2026. A formal customer open house and ribbon-cutting event is planned for Q1 2026, where guests will have the opportunity to tour the facility and meet the local and corporate leadership teams.
The facility is also expected to create 10 new skilled jobs in the Fairfield region, reinforcing Bodycote’s continued investment in advanced manufacturing and workforce development across the state of Ohio.
Bodycote’s expansion in Fairfield continues the company’s investment in world-class facilities and sustainable technologies to support customers’ long-term growth and performance needs.
About Bodycote: Bodycote plc is the world’s leading provider of precision heat treatment and specialist thermal processing services, delivering vital metallurgical solutions that improve the performance, reliability, and longevity of critical components. Serving customers across aerospace, automotive, energy, defence, medical, and other industrial sectors, Bodycote combines global scale with local expertise to meet demanding technical and sustainability requirements. Through its global scale (with more than 150 facilities worldwide), the company is committed to delivering innovative solutions that advance performance, sustainability and competitive advantage for its customers.”
60 Years ago “Clyde Fasteners” of East Kilbride, Scotland set out to produce fasteners for a variety of industries including oil & gas, defense, and heavy equipment.
From day 1 in house heat treatment was considered a crucial part of the firm’s success-the end result is that the company continues to this day to do all heat treating in house and recently the company invited Gord Montgomery of “The Monty Heat Treat News” to tour the company’s manufacturing facility in Scotland.
The tour occurred Monday, November 10, 2025 and the host was Mr. Gordon Russell, Production Manager and owner of the company who gave “Gord Montgomery” of “The Monty” and “Nigel Troth”, Sales Manager of furnace controls company “Super Systems Europe” his undivided attention for several hours.
“Clyde Fasteners” , East Kilbride, Scotland
What was witnessed was a small to medium sized fastener manufacturer who has survived, prospered and indeed thrived over the years and one has always believed in having all parts of the manufacturing process kept in house.
Generally, fastener manufacturers use continuous style heat treat furnaces and in the past “Clyde Fasteners” went the same route, however “Clyde’s” specialty is in smaller lot sizes and over time they have adopted batch IQ (Sealed Quench) furnaces because of their versatility.
Currently the company operates two hardening furnaces, two tempers, a batch washer and two endothermic generators (this heat-treating equipment is complimented by Induction heating systems also).
Nigel Troth, Sales Manager, “SSi Europe”
A new addition to the heat treat department which represents a sizeable investment is a “Neotherm” Endothermic generator which came on line just one week ago-the unit can be seen in one of these photos.
We thank “Mr. Gordon Russell” for his time and appreciate the fact that he was so willing to share all the details of his heat treating expertise with “The Monty” and indeed the entire global heat treating community.
Later this week “The Monty” will be profiling a captive/commercial heat treater also in Scotland who supplies “rock breaking hammers”.
Left to Right; Gordon Russell, Production Director, “Clyde Fasteners”, Nigel Troth, Sales Manager, SSi Europe, Gord Montgomery “The Monty Heat Treat News”
The team at “The Monty Heat Treat News”constantly looks at heat treating around the world-our latest efforts take us to Scotland where the team visited several captive heat treaters.
Detailed profiles of these firms will follow but we can share with our readers these photos of two different in house heat treating departments, one a supplier of fasteners to the wind energy, defense and energy industries the other a major supplier to the mining industry.
Stories will follow shortly.
“The 5,000th technological solution has just rolled off SECO/WARWICK’s production line, confirming the Group’s ongoing growth and global standing as one of the leading names in metal heat treatment.
This symbolic moment is the result of decades of innovation, investment and global expansion. The five-thousandth SECO/WARWICK device is a unique, powerful line of atmospheric electric furnaces designed for bright annealing of high-alloy tubes. The partner –Alleima, a global manufacturer of high value-added products in advanced stainless steels and special alloys– has previously ordered vacuum and retort devices from SECO/WARWICK. The current order will be used in the production of components for nuclear solutions.”
Today, SECO/WARWICK is a global organization, comprised of seven companies across three continents, employing over 900 people, of whom as many as 60 percent are engineers. The company supplies its technologies to customers in 70 countries worldwide, supporting strategic industries – from aerospace, energy, and automotive, to nuclear and medical sectors, and now, with its five-thousandth solution, boasts an impressive track record of achievements.
“SECO/WARWICK Group solutions are manufactured in five production plants with a total area of nearly 50,000 m² (538195 sg ft) – in Poland, the USA, China and India. That’s an area equivalent to seven full-size soccer field. In Asia and North America, production spaces have reached an impressive combined area of 13,500 m² in India and China, 23,350 m² in America, and 12,000 m² in Europe. Our brand’s five-thousandth solution is a source of pride, a commitment, and proof of continuous development and growth, today measured by the number of solutions produced,” said Sławomir Woźniak, CEO of the SECO/WARWICK Group.
Over the years “The Monty Heat Treat News” has had the chance to visit commercial heat treater “Wallwork Heat Treatment” in the UK several times-everything you ever wanted to know about the company can be found at “Wallwork Group. Bury, UK”
Today we have this press release from the company stating that they were so overwhelmed by customer demand for their first “Hot Isostatic Press” that they have moved up installation of their second system as can be read below;
“Wallwork Heat Treatment have announced their second Quintus Technologies hot isostatic press will soon be fully operational. Currently going through its final phases of testing, the company brought forward the investment by two years. This makes a total of £20 million now invested in the Wallwork HIP Centre.
“The demand for HIP has blown us away. We expected it from the UK. Now we are also servicing customers across Europe in France, Germany, Italy, Turkey and further afield. Advanced hot isostatic pressing technology offered on the Quintus HIPs is driving demand. Typical is uniform rapid cooling. This enables component manufacturers to push their product designs to the next level. In Wallwork they find an experienced partner, available 24/7 and with the knowhow to apply the HIP process to best effect.” explained Howard Maher, Wallwork HIP Centre and group sales manager.
“The second HIP is identical to the first one supplied by Quintus in 2023. Besides doubling capacity, this has many advantages. It allows the use of interchangeable rigging and mantles. It provides redundancy contingency planning during scheduled maintenance. And also ensures repeatable processes across both units. The Wallwork HIP Centre is now Nadcap and EN9100 accredited,” added, James Bailey, site director.
Like the first HIP, the new one can reach pressures from 40 to 207 MPa (5,800 to 30,000 psi). Temperatures range up to 1250°C, and it has the latest uniform rapid cooling technology. Increased cycle pressures at elevated temperatures, complements engineering advances in metal 3D printing. It is also suited to processing castings, near-net shape powder metallurgy and more. User industries include aerospace, automotive, autosports, medical devices and other precision high-value manufacturers.
Wallwork has four UK sites offering over 117 heat treatment processes, vacuum brazing, a range of standard and bespoke PVD coatings.
“This is not the end of our journey of investment in hot isostatic pressing. Discussions are in progress for ring-fencing further funds for a third HIP. We are looking into what this should be. How it will expand the depth of HIP services we can offer customers. It might be something quite specialized,” hinted group director, Simeon Collins.”
Want to know more about “Wallwork“-follow these really cool links provided by “The Monty”, including a daredevil motorbike rider on top of the furnaces:
A number of years back “The Monty Heat Treat News”, did a summary about the heat treatment market in South Africa, included in this summary was one of the largest commercial heat treaters in the country “Harchris Heat Treatment”.
It would now appear that the firm is under new management-“Erindale Holding” to be exact:
“With the imminent retirement of Managing Director Errol Preston, Harchris Heat Treatment has been acquired by Erindale Holdings (Pty) Ltd, new owners that have a background in the agriculture and mining sectors. As part of the agreement, which was signed just over a year ago, Errol Preston has remained on in a consulting capacity to oversee he handover and mentor the new owners.
“The acquisition of Harchris Heat Treatment is an important milestone for us as the new owners and provides significant end market diversification and additional reach, both of which are key strategic drivers for our business. We are pleased with this recent development and look forward to furthering our core values of customer service, quality, technical expertise, and providing solutions to our customers,” said Shane Potgieter, who is the new Managing Director.
“It was decided to purchase Harchris as a going concern, and therefore, the majority of the original staff have stayed on. Additionally, we have appointed a Business Development Manager, a Junior Production Manager and a Processing Plant Engineer.”
“The services that Harchris Heat Treatment, one of South Africa’s oldest heat treatment companies, offer includes stress relieving, annealing, spherodising, sub-critical annealing, solution heat treatment, normalising, water and oil quenching and we also specialise in annealing and hardening of chrome iron. The services include both the non-ferrous and ferrous sectors.”
“As part of constantly improving our customer service, we have endeavoured to turn Harchris into a one-stop manufacturing shop. Therefore, we have partnered with a local shot blasting company and can now offer shot blasting, corrosion protection, and painting services. In addition to this, we have a 500-ton press on the premises and a 30-ton, 14-ton and 7-ton truck for any transport requirements.”
“Future expansion plans include the commissioning of a brand-new pit furnace with recuperative burners by the end of 2025, as well as the commissioning of a muffle furnace in the second quarter of 2026.”
Not so fast says Eric Wilson, COO of “The Dayton Forging & Heat Treating Company” just down in the road in Dayton, Ohio. According to him, his company has been in continuous operation since 1919 making it just 2 years older than “Queen City”
Anybody else out there that would like to step up?
“OCTOBER 23, 2025. Oldest Continuously Running HT in North America Now Has Single Owner; Earlier this week “The Monty Heat Treat News” had a news item entitled “Heat Treat 2025”-Things You Have to Know“. This news item featured a number of trivia points about the heat treatment industry which every heat treater worth their salt should know.
A reader responded with a question addressed to “The Monty” team-“what is the oldest continuously running commercial heat treat in North America”–“The Monty” team got it wrong with our answer of“Bennett Heat Treating”in Newark, NJ founded in 1923.
It turns out the correct answer is “Queen City Steal Treating”, in Cincinnati, Ohio founded way back in 1921-it is believed that they are the only remaining charter member of “Metal Treating Institute” MTI – (our news item below features MTI).
In related news it is our understanding that “Mrs. Judy Rudy”, the longstanding and very competent President of the firm bought out her business partners earlier this year and is now sole owner of the company-a very impressive feat.”
In a very discrete, unpublished way it would appear that a Nadcap accredited captive heat treater in Phoenix, Arizona, USA by the name of “Joined Alloys”was recently acquired by a firm based in India.
This is how “Joined Alloys” describes their heat treatment/brazing capabilities:
“We specialize in furnace brazing with nickel, copper, and precious metal braze alloys. Heat treating services are performed in a vacuum and in hydrogen, and inert gas atmospheres. Typical heat-treating processes include stress relieving, normalizing, solution treating, precipitation age hardening, and tempering of exotic alloys.
Our in-house brazing capabilities allow us to provide our customers with advanced bonding solutions for use in fabricated components and assemblies. Heat Treating, Brazing and Non-Destructive Testing are NADCAP accredited.”
This press release from “TASE” Describes the Acquisition;
“NOVEMBER 2025; Chennai, India-based Trusted Aerospace Engineering (TASE Global) has completed its acquisition of Joined Alloys, a US-based firm specializing in aerospace manufacturing, special processes and specialized sheet metal fabrication and product development, for $12 Million USD.
TASE Global is a diversified manufacturing and technology group with operations across Europe, Asia and the Americas. The company specializes in precision manufacturing of components and providing solutions for aerospace, medical and industrial applications. It has factories in the US and India, along with offices in Portugal and France.
“Joined Alloys brings a legacy of technical excellence, strong client relationships and a culture of integrity that aligns with our own,” said Sankararaman Vaidyanathan, Chairman, TASE Global. “The acquisition is a part of our forward integration process that unlocks synergies in aerospace manufacturing, defense and medical applications, allowing us to pursue more ambitious projects across industries. TASE Global shall be an end-to-end strategic partner to large Tier 1 players.”
September 3rd “The Monty” had the exclusive news story below about a Michigan, USA heat treater installing one of the “Largest Vacuum Furnaces in the US Midwest”. As an update to this story we have these notes from “Darby Metal Treating” and this video.
“Today, DMT took delivery of a new vacuum hardening and annealing furnace and this one is an absolute unit. Work zone dimensions are 52″ W x 109″ L x 40″ H, with up to 5 bar nitrogen quenching capability. The furnace vessel alone was so large that we had to widen the opening for our roll up door to get it in the building. Stay tuned for further updates on installation and production readiness for this exciting addition to our heat treating equipment and thanks to our friends at Kandler Tool Company for a flawless setting on our shop floor!”
In that article we suggested the firm might be installing a very substantial vacuum furnace in the near future-we can now confirm that, that rumor has proved to be correct and “The Monty” can give you all the details in this exclusive story.
The furnace was manufactured by “TAV” and has working dimensions of 52″ X 40″ X 102″-making it not the largest in the Midwest but probably close to it. It has a maximum working temperature of 2,400F, an ultimate vacuum level of 10-3 torr (range) and up to 5-bar quenching with either argon or nitrogen. This almost new furnace came out of an aerospace facility in the western USA and was very lightly used, so much so that we would consider it in like new condition.
While we do not have a definite date as to when it will enter production, we would expect it to be within the next couple of months-certainly before the end of the year. These photos show the furnace at its previous location.”


 60 Years ago “Clyde Fasteners” of East Kilbride, Scotland set out to produce fasteners for a variety of industries including oil & gas, defense, and heavy equipment.