
Although Eltropuls has offered and sold many furnaces in the U.S. before, CEO Marc Straemke says “Our renewed focus on a new team, including local experts, assures customers that Eltropuls is your best option for the most advanced plasma nitriding technology. With a history of over 500 furnaces, and special automation skills, Eltropuls leads other plasma furnace providers, as we always have, since we introduced pulsed plasma in the 1980’s ”. Dr. Marc Pohlman will be in Indianapolis to welcome interested heat treaters. Our new team will be more responsive and focused on our many U.S. customers and future customers. The North American market now has a legitimate option for plasma nitriding systems from the leader in this field.”
Eltropuls’ commitment reflects an understanding that the U.S., Canada and Mexico are critical growth markets which merit focus by Germany’s largest plasma nitriding furnace company. Eltropuls also has nitriding service centers in Germany, and in Oxford, MI to assist with customer trials, spare parts and heat treating services.

“A U.S. based manufacturer of bearings for demanding industrial and aerospace applications has once again invested in SECO/WARWICK vacuum technology. One of its facilities will receive a Vector vacuum furnace with high-pressure gas quenching (HPGQ) and Low Pressure Carburizing (LPC) option. This is another project completed for this Partner, and the first SECO/WARWICK system at this facility.
In industry, the strongest endorsement of a technology is not a claim, but a repeat purchase. SECO/WARWICK’s U.S. Partner has decided to make another investment in vacuum technology, expanding its in-house heat treatment capabilities for bearing components. The new furnace will be used for hardening and carburizing a broad range of components, including larger loads. A working zone measuring 36 × 36 × 48 in (900 × 900 × 1200 mm) enables the system to efficiently process larger parts as well. The investment addresses the customer’s growing production needs and the increasing number of hardening and carburizing processes performed in-house.

The furnace on order belongs to SECO/WARWICK’s proven family of single chamber vacuum furnaces. The standard design has been configured to meet the bearing manufacturer’s specific needs.
The system features a cylindrical heating chamber that provides temperature uniformity of ±9°F (±5°C). Convection heating improves heat transfer at lower operating temperatures, while the directional cooling system enables proper process control for parts with more demanding geometries. Another important feature is isothermal quenching, which enables more precise control of load cooling and blower power at individual stages of the process.
The furnace is also equipped with Low Pressure Carburizing (LPC) technology, allowing the steel surface-hardening process to be performed as part of an integrated heat treatment cycle. This is particularly important for bearing manufacturers. Carburized case parameters, process repeatability and the cooling method directly affect the performance of components that will later operate under heavy loads.


Welcome to the “Monty Heat Treat News” “Monday Morning Briefing” where we provide the latest news and trends in the global heat treatment industry;

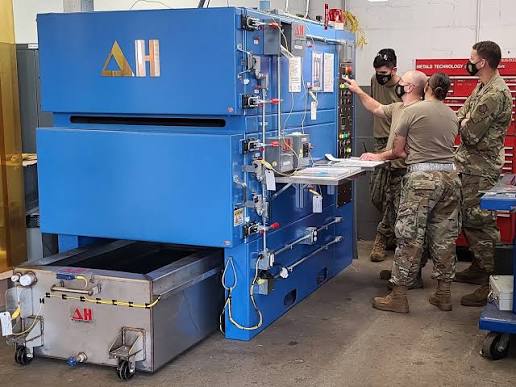 DELTA H® Technologies Experiencing Record 2026 with Expanded Commercial and Military Manufacturing Growth Strategy; “Carroll, OH – October 2026 – DELTA H Technologies has delivered multiple advance aerospace heat-treating systems for aerospace & defense (A&D), commercial, and military aviation over the past year. The aggressive growth strategy has required doubling DELTA H’s workforce, and re-tooling production capacity to manage a record-breaking backlog of systems in production simultaneously. This increased capacity provides a foundation for further expanding DELTA H’s ability to serve our valued clients with larger orders and systems that are built to last for decades. Richard Conway, Director and CTO of DELTA H Technologies and a U.S. Air Force veteran, adds: “DELTA H, through our partnership with Phillips Federal Division, continues to expand our presence at not only USAF bases, but also all branches of the Armed Forces. Upon completion of our current backlog, DELTA H will have furnaces installed in approximately 75% of the USAF bases worldwide that perform aircraft maintenance. DELTA H’s commitment to A&D contractors for technically advanced systems continues to be an exciting aspect of DELTA H’s expanded growth for the present and into the future.”


 “Alcon Industries” Asset Sale; At one time Alcon Industries of Cleveland, Ohio, USA was one of North America’s premier suppliers of cast and fabricated, high temperature furnace components. Unfortunately, that reputation slipped quite a bit over the past couple of years and the end result is that production has ceased and the remaining assets have been sold to “Wirco”.


 September 27th, 2026 “The Monty Heat Treat News” posted this exclusive story about layoffs at “Alcon Industries” one of North America’s largest suppliers of fabricated and cast high-temperature furnace components “Shortage of Hi Temperature Alloy Casting Capacity in North America?”. Since that time speculation has been running rampant that the firm would be closed or sold, it would appear that the remaining assets have been sold;
“September 30th, 2026, Avilla, Indiana, USA. WIRCO Inc. executed an asset purchase agreement to acquire selected manufacturing assets from Cleveland, Ohio-based Alcon Industries Inc.
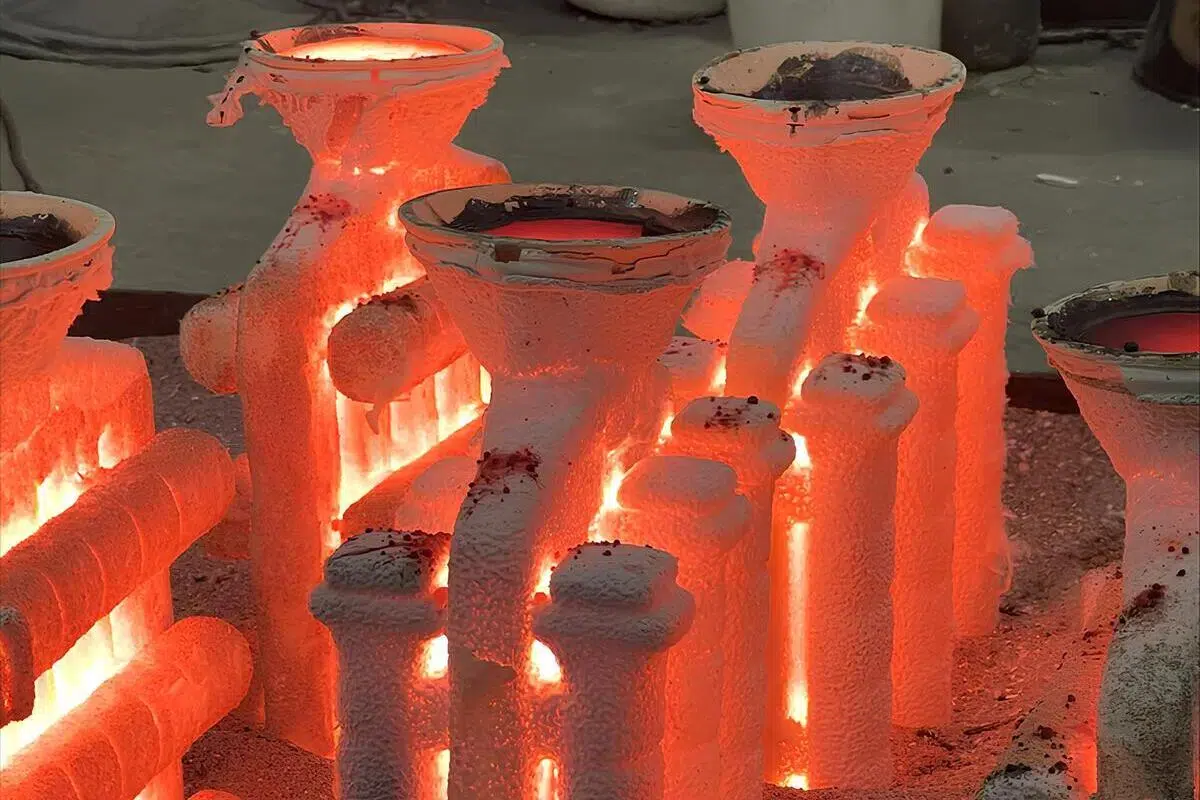 What was acquired: WIRCO purchased specific manufacturing equipment (including melting furnaces, fabrication equipment, and casting machines), designs, drawings, manufacturing processes, and over 1,000 active tools from Alcon.
- The Goal: Wirco Inc.,intends to absorb these assets into its own multi-state operations (spanning Indiana, Wisconsin, and Illinois) to boost its production capacity for centrifugal and static cast products.
- Company Status: WIRCO remains a separate entity and did not assume Alcon Industries‘ existing liabilities or financial obligations. The sale followed reports of recent layoffs and production capacity concerns at the Cleveland foundry.”
“Alcon Industries” was established in 1977 by “Dick” Chalet and his partner “Tom Waldin” who grew it into one of North America’s largest suppliers of fabricated and cast high-temperature furnace components. Mr. Chalet served as the company’s long-time leader and President until his passing in December 2018 from cancer. “Alcon” had always been known as a high quality supplier of furnace components and a reliable supplier, however that reputation had been slipping over the past year or so (WG Montgomery Ltd., parent company of “The Monty Heat Treat News” enjoyed a long relationship with the company).

The company was founded in 1996 by Prof. Dr.-Ing. Sabine Böhm, originally with a strong focus on plasma heat treatment, materials technology and research and development. Since 2012 the company has been headed by her son, Andreas Böhm, making this very much a second-generation, family-run heat treatment business.

The systems are available in a variety of sizes, allowing the company to process everything from smaller precision parts through to components weighing as much as 2 metric tons.
As most readers of “The Monty” will know, plasma or ion nitriding is particularly attractive for applications where high surface hardness, wear resistance and fatigue strength are required while keeping distortion to a minimum. Dr. Böhm processes components for industries including machine building, automotive, tooling, plastics processing, hydraulics and general mechanical engineering.

The laboratory includes multiple hardness and microhardness testers, digital microscopy, metallographic cutting, grinding and polishing equipment and surface roughness measurement equipment. Capabilities include Vickers hardness testing, determination of nitriding hardness depth, metallographic examination and measurement of compound layer thickness. The company’s contract heat treatment and furnace engineering operations are certified according to ISO 9001.

From our perspective, a family-owned company reaching 30 years in business is always worth mentioning, but what makes this story particularly interesting is the scale of the operation. With 15 plasma nitriding furnaces, an extensive metallurgical laboratory and three decades of specialized experience, “Plasmanitriertechnik Dr. Böhm” has quietly developed into one of Germany’s largest providers dedicated to plasma nitriding.
We would say that is a fairly impressive achievement for a specialist heat treater which started in Chemnitz back in 1996.

Manufactured by Heat Treat Equipment Inc. of Canton, Michigan, the new furnace significantly expands Solar Atmospheres of Western PA’s ability to provide controlled heat treatment for large titanium components weighing up to 7,500 pounds. The system is designed to maintain temperature uniformity within ±5°F and achieve rapid water quenching within seven seconds.
Titanium alloys are widely used in aerospace, defense, medical, and other critical applications where high strength-to-weight ratios and reliable performance in demanding environments are essential. The new furnace provides Solar Atmospheres of Western PA with the capability to process larger titanium components while thermocoupling the actual workload, providing precise monitoring and control throughout the heat treatment process. An in-process camera will also be installed to monitor the workload while being heated above the critical beta transus temperatures.
“This new furnace is an important investment in our continued commitment to serving our customers,” said Bob Hill, President of Solar Atmospheres of Western PA. “This equipment finally gives us the opportunity to solution anneal critical titanium alloys that our titanium customers have continuously asked for over the years.”
The 14-foot-long by 54-inch-wide by 48-inch-high furnace is positioned directly above an 11,000-gallon, multidirectional, highly agitated water quench tank. This configuration is designed to minimize transfer time between the furnace and quench tank, enabling extremely rapid quenching of titanium components that is required by stringent aerospace specifications. Additionally, a closed loop cooling system provides a water quenchant temperature never to exceed 100 F.
Once fully operational, the new system will further expand Solar Atmospheres of Western PA’s comprehensive range of vacuum and air heat treatment services. The investment reinforces the company’s commitment to maintaining state-of-the-art equipment and delivering advanced heat treatment solutions for customers across demanding industries.
For additional information about Solar Atmospheres, contact Mike Johnson at 855-934-3284 x2223, email at [email protected], and visit us at solaratm.com.

A perfect match
Founded in 2007, MetalPro Resources is an independent sales representative and full-service partner to the heat treating industry. Its portfolio includes heat treating equipment for steel and aluminum, control systems, analyzers, vacuum instruments and accessories, as well as consulting services for heat treat operations. The team combines more than 100 years of experience in heat treating and metallurgy. Many of those years were spent running captive heat treat shops, so MPR understands its customers’ needs first-hand.
From its location in Rockford, Illinois, RUBIG has been supplying and servicing plasma nitriding systems, gas nitriding/FNC systems, plasma coating systems and PVD thin-film coating systems in the US for around 30 years.
The partnership adds RUBIG’s nitriding and coating technologies to MetalPro Resources’ offering. Customers in the region benefit from expert local support, while delivery and service continue to be provided by RUBIG from Rockford.
Contacts at MetalPro Resources
Jim Senne (President), Steve Maus (Indiana, Greater Cincinnati, Kentucky), Bill Andreski (Eastern Ohio, Western Pennsylvania, West Virginia) and Dave Alvord (Michigan, Northern Indiana, Western Ohio).”

In this semi humorous column “Dan” points out the similarities between commercial heat treating and doing the laundry. After you have read the article we are sure you will agree with us that there are some very good lessons be learned about how to run a profitable and efficient commercial heat treat facility if you compare it to such a mundane task as doing the laundry.
Scheduling Your Heat Treat Shop – Or Your Home Laundry

But then I thought about how my own home laundry service works. The “simple business” of laundry is not so simple, as it turns out.
Consider the laundry room in your family home. There might be:
- A counter
- a faucet and sink,
- a washer,
- a dryer,
- a folded-up ironing board
- a rod holding for temporary storage of clothes on hangers
- a cabinet that contains all the needed supplies and hand tools including :
- a measuring cup or two
- a spray bottle of stain remover
- a bottle of detergent
- a bottle of fabric softener
- a bottle of bleach
- a box of dryer sheets
- a clothes iron
- a supply of clothes hangers (scattered all around the house)
- A clothes hamper or two in or near the bedrooms
- There are also a couple of baskets which are used to collect or deliver clothes etc. from the hampers to the laundry room and then back again.
Now consider when and how the laundry room is operated:
- most days
- once per week
- only after family members have been complaining for days
Putting it all together, we now have on site:
- incoming and outgoing clothing, towels, and sheets
- A logistics capability (hampers, hangers and baskets)
- A processing department (washing plus either machine drying or air drying)
- A straightening department (iron and ironing board)
- An inspection capability
- A rework capability
- Express service capability

How eficiently can this whole thing be operated? Surely an experienced production heat treater can put a plan together. Here is a generic router containing all of the operations performed in a home laundry:
- Collect clothing and deliver to laundry room
- Sort laundry into discreet piles, where all clothes in the same cycle are compatible with each other in every way except drying and ironing. Clothing, sheets, towels, rags, whites, colors, delicates, heavy work clothes, disgusting socks etc. There is actually a top secret matrix of illegal combinations, in the form of “never wash X with Y”, where X and Y are things that seem to change over time.
- Split all large piles into 2 or more smaller piles to suit the max load size limitation of the washer/dryer. It is common for floor space being consumed by all of the piles exceeds the floor space available in the laundry room by a factor of 3. Use of the hallway is encouraged.
- Before commencing any wash cycles, clean out the lint trap on the dryer. (Everyone forgets to do that until they’ve just loaded the dryer and started it before realizing that the lint trap has not been cleaned lately and might be ready to catch fire very soon.)
- Consider what ought to be washed first. If there is a pile that contains a rush order, get it going first, easy decision and no stress so far.
- Load the selected pile into the washer, piece by piece, checking to see if there are stains that might need a squirt of stain remover. Once everything is in, guess an appropriate cycle from the 10x5x7 matrix of possible knob settings on the washer, and press start to begin the cycle.
- Realize that having just pressed the start button, there is nothing else to do for 45 minutes or so. Labor is now being wasted. Note that the dryer is also still down cold, as is the iron. Totally under- utilized, what a waste.
- Then realize that when you split the first big pile up, you forgot an important piece of clothing that MUST go into the first load. Try to open the washer lid only to discover that the washer has a mechanism that prevents the door from being opened during a cycle. Force the interlock to be released by aborting the cycle, which takes almost 4 minutes these days in the name of safety.
- When the washing machine finally grants access, throw the errant missing clothing item in, and start again.
- After 45 minutes, the washer’s cycle end buzzer goes of. Now it’s time to get really eficient.
- Open the washer and lift the entire load out in one go, with intent to dump the whole thing in the dryer.
- Notice that the dryer door is still closed because no one has opened it yet.
- Sit entire load back down on top of the dryer, open the dryer door, lift the load again, shove the load in, and close the dryer door.
- Guess an appropriate cycle from the 10x5x7 matrix of possible knob settings on the dryer, and press start to begin the cycle.
- Forgot to put a dryer sheet in – Stop the cycle, open the door, throw the dryer sheet in there, close the door again, and continue the dryer cycle.
- The washer is now empty, ready for the next pile to go into the washer. This is too easy.
- Pick up the next pile on the floor and throw it into the washer along with detergent and start it up.
- Congratulate self, this is working well. We are at the highest possible eficiency. Plenty of time to relax for cofee.
- A buzzer sounds, indicating an end-of-cycle alarm on one of the machines. It’s the washer, the dryer is still humming away.
- Grab the wet clothes from the washer and pile them on top of the dryer, a homemade temporary storage point.
- Put the next pile on the floor into the washer, add detergent, and start it up.
- Note with satisfaction that with 3 loads in progress, we are now at absolutely the highest possible production rate. More cofee.
- Another buzzer sounds. It’s the dryer finally. Apparently the dryer cycle time is more than 2X the washer cycle time. Never realized this before. It kind of makes sense, it’s way quicker to get things wet than to remove water from soaking wet cloths with hot air. Maybe dryers are under- powered? That can’t be right, they run on 220VAC. The real limits must be volume and the max temperature that clothing should be exposed to? Gotta look that up.
- Time for a bathroom break. While doing that, a buzzer sounds – the dryer must be finally done.
- Remove cloths from dryer and put them …on the dining room table, a new 4th station in the line. No more room on top of the dryer and these warm clothes need to be folded ASAP.
- Take one of the standby wet loads and shove it in the dryer and start again. Possibly forgot a dryer sheet this time, can’t remember.
- Rush over to the dining room table and start folding. After a couple of minutes 3-4 nicely folded stacks of folded laundry are sitting to one side on the table. It seems silly to deliver these clothes back to the bedrooms yet, better to wait and accumulate more in the stacks and run a more eficient delivery route later.
- Another buzzer sounds. It’s the washer again. That machine is relentless. Need to program a longer cycle somehow.
- Remove load from washer and squeeze it in on top of the dryer, back up to two loads there again.
- Fire up the washer again.
- Is it lunch time yet? Need a break. Nope, the dryer buzzer just sounded. Time for another folding session and need to reload the dryer.
- At this point, a review. We’ve run 5 loads in the washer and just two in the dryer. The dryer turns out to be a huge constraint on how fast this laundry task can be completed! There is not enough room to put a second dryer in. Maybe we need to put a clothesline out back for air drying, which would unfortunately bring weather into the picture. Also, no clothes requiring ironing have been run yet – should we have done these first? And no towels have been washed yet, bet they take even longer to dry than the clothes washed so far.
The conclusion: The average consumer is trapped in a paradigm of one washer and one dryer per household. It is inevitable that the washer be throttled back. There are two ways to do this – let it sit empty more than half the time or run more, and smaller, loads and develop a production rhythm. Now I understand why my mate has been criticizing me for many years about my tendency for overloading our washer – she knows it’s a fool’s errand.
Now back to heat treating, where surely, problems like these don’t pop up much.

- “The Monty” Talks Vacuum Furnaces with “Jay Jefsen of Furnacare”
- The Differences Between Automotive & Aerospace Heat Treating-“Mr. Raman Bawa”
- You Can’t Buy a Vacuum Furnace This Year. You Can still buy capacity! CFC Fixturing
- Heat Treatment Names in the News
- Heat Treater Makes Very Substantial Investment in USA Facilities
- President of Furnace Builder “CAN-ENG Furnaces International” Retiring
As regular readers of “The Monty” know our list of surplus heat treatment equipment is substantial and constantly changing. Some recent additions include these;
- Item# B495 Pit Nitriding Furnace-45″ Diameter X 96″ Deep
- Item# O421 Electric Wisconsin Oven 500F (Brand New)
- Item# IQ529 Ipsen T-4 Batch IQ Furnace
- Item# I199 Radyne 300KW induction System
- Item# G226 4500 CFH AFC – Holcroft Endothermic Gas Generator, Air Cooled
- Item# L238 Leco M-400-G1 Semi-Auto Microhardness Tester
As always the entire team at “The Monty Heat Treat News” looks forward to your thoughts, comments, press releases and used equipment inquiries. Sincerely, Gord, Jordan and Dale Montgomery.
“The Monty Heat Treat News” is a division of “WG Montgomery Ltd.“, a family owned business serving the heat treat industry since 1969.
Click Here To Read The Full Magazine

“Aichelin Americas Unites AFC -Holcroft, GM -Enterprises and Nitrex Under One Organization”
Unified identity brings together decades of thermal – processing expertise, engineering capabilities and customer support across the Americas
WIXOM, Mich. — October 1st, 2026 — Aichelin Americas LLC today announced the introduction of Aichelin Americas, a unified organizational identity bringing together AFC-Holcroft, GM-Enterprises and Nitrex. Each company has built a respected reputation within the thermal – processing industry through engineering excellence, innovative technologies and dedicated customer service. Operating together as Aichelin Americas will allow the organization to more clearly present the full breadth of its combined technologies, manufacturing capabilities, application expertise and aftermarket support.

Customers will continue working with the same experienced teams and receiving the products, services and technical support they have come to trust. The individual brands and their areas of expertise will remain important parts of the organization, now supported by the broader resources and capabilities of Aichelin Americas. The combined organization offers expertise across a wide range of thermal – processing equipment, technologies and services. By aligning its engineering knowledge, application experience, manufacturing resources and customer -support capabilities, Aichelin Americas will be better positioned to address increasingly complex customer requirements and deliver more comprehensive solutions throughout the Americas.
As part of the new organizational structure, Aichelin Americas is also launching a dedicated Parts and Service division to support thermal – processing equipment throughout its operating lifecycle. Customers will have one coordinated source for replacement p arts, field service, technical support, preventive maintenance, repairs, equipment upgrades and modernization solutions for AFC -Holcroft, GM- Enterprises and Nitrex equipment, as well as systems manufactured by other OEMs. Bringing these capabilities together will help customers reduce downtime, improve reliability and extend equipment life. “Our goal is to make it easier for customers to get the support they need from one coordinated team,” said Tracy Dougherty, President of Sales and Service at Aichelin Americas. “Whether the equipment was manufactured by AFC -Holcroft, GM-Enterprises , Nitrex or another OEM, our Parts and Service division will provide the expertise and responsive support needed to improve reliability, reduce downtime and extend equipment life.”
The formation of Aichelin Americas represents the next chapter in the organization’s development: one unified company built on decades of experience, driven by innovation and committed to helping customers improve performance, reliability and long -term operational success.
About Aichelin Americas; Aichelin Americas LLC brings together AFC-Holcroft, GM-Enterprises and Nitrex, combining decades of experience in thermal – processing equipment, technologies and services. The organization provides engineered solutions, manufacturing capabilities, application expertise and lifecycle support to customers throughout the Americas. As part of the global Aichelin Group, Aichelin Americas connects established regional expertise with the resources and capabilities of an international thermal – processing organization.”