(Editors Note: While “Oerlikon Balzers” is best known as a coatings company they do also get involved in commercial heat treating. In this case their Pell City, Alabama location also offers nitriding services.)
“BIRMINGHAM, Ala. (WIAT) — Eight people will soon be out of work after Oerlikon Balzers Coating USA closes its one plant in Pell City. The company, which operates over 30 locations across the country, announced in a WARN notice that it was closing its plant in Pell City, beginning March 31.
Oerlikon Balzers is a subsidiary of Oerlikon Group that provides protective coatings for different automotive parts. No other closings have been announced by the company.”
About Oerlikon Balzers; “Oerlikon Balzers, world-leading provider of surface technologies, develops solutions and equipment and offers services to considerably improve the efficiency and longevity of precision components and tools for the metal and polymer processing industry. Oerlikon Balzers is the only contract coating services provider with a dense coating centre network located throughout all of the major industrial regions of Europe, the Americas, and Asia. This guarantees efficient procedures, short delivery times and local customer advice and support. For 75 years, Oerlikon Balzers has stood for pioneering developments and global technology leadership in thin-film coatings.”
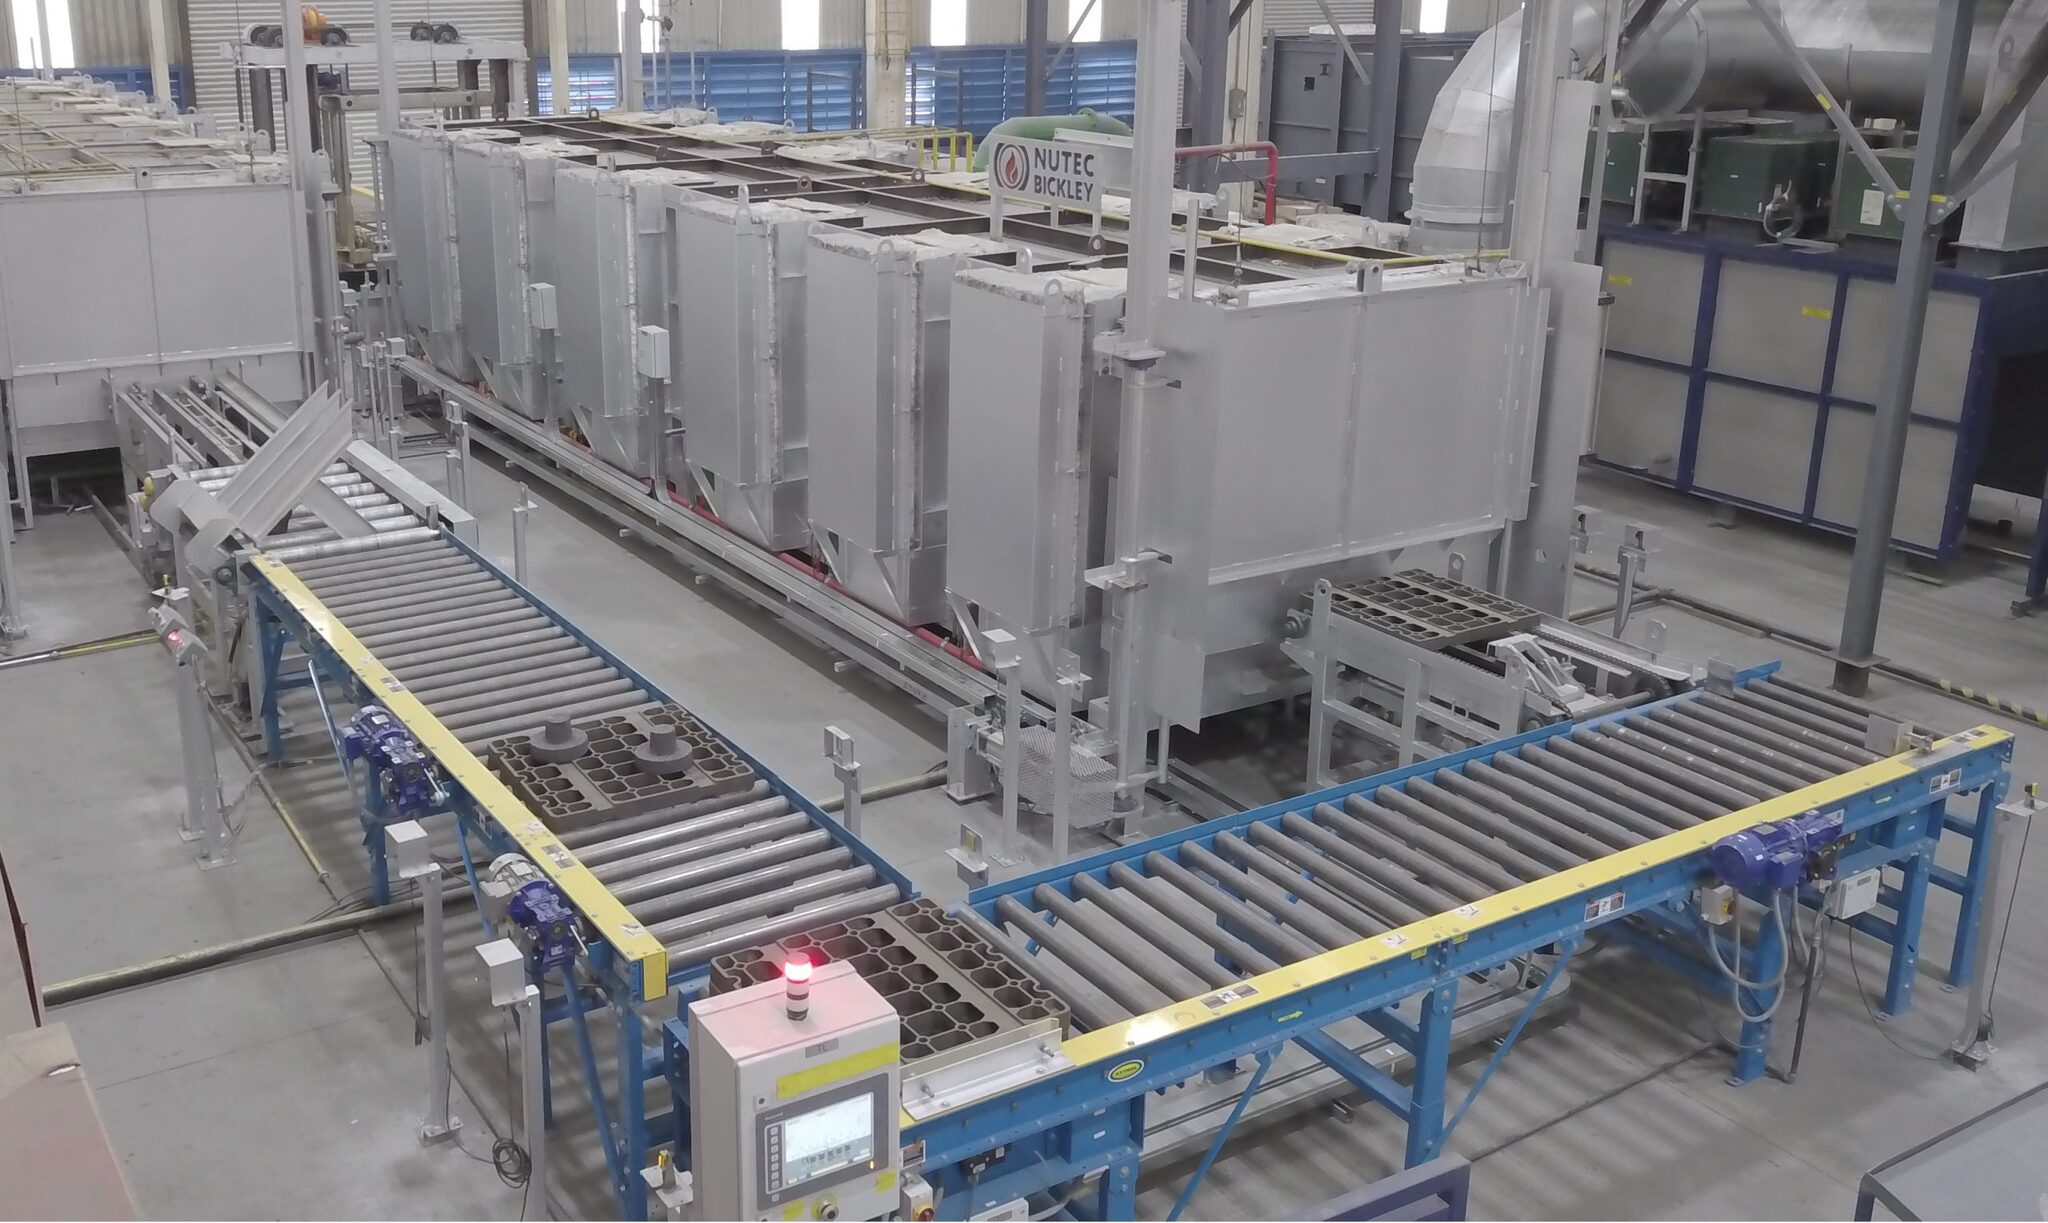
“An international, multi-billion-dollar corporation at the forefront of drivetrain technologies has awarded NUTEC Bickley the contract for a complete isothermal annealing line, due to be delivered in Q1 2026. This prestigious heat treat project is highly customized and the system has been designed in close collaboration with the customer to ensure everything meets its specific operational needs.
The contract comprises both high-temperature and low-temperature furnaces, as well as an isothermal cooling chamber and blast cooling tunnel, together with all the ancillary equipment and full material handling and conveying system. The furnaces are designed to be in compliance with CQI-9, the comprehensive audit covering the most common heat treat processes employed by the automotive industry.
Arturo Arechavaleta, NUTEC Bickley’s VP, Metal Furnaces, said: “Our client for this multifaceted project is an auto component world leader that supplies nearly every major vehicle manufacturer. It has an established reputation in delivering the highest quality parts and promoting sustainability in the supply chain. I am delighted that NUTEC Bickley was chosen to partner in the design and manufacture of this isothermal annealing line.”
At the heart of the new facility will be a double pusher tray high-temperature furnace (HTF) that will process carbon steel automotive parts. The furnace will incorporate a fully automatic electrical double pusher system with steel trays sliding over rails with idle rolls. Processing two trays across the width helps reduce the length of the line.
This natural gas unit has four automatic temperature zones, each with two high-velocity nozzle-mix burners that provide excellent turbulence and outstanding recirculation within the furnace chamber. The burners are positioned on top of the sidewalls of the unit, mounted to fire horizontally above the load.
The operating temperature is between 850°C and 950°C (1560°F-1740°F). As with all NUTEC Bickley projects, achieving temperature uniformity is a priority, and the broadest aims here are ±5°C for processes below 680°C, and ±10°C at or above 680°C. The combustion program is based on pulsed firing, with all the latest control software for this type of system.
After initial heat treating, the forged carbon steel parts are moved into an isothermal cooling chamber (ICC), also supplied by NUTEC Bickley. The exit door from the high-temperature furnace links directly to the ICC. Cycling time in the ICC varies between five and 10 minutes – with ambient air being supplied from an external cooling air fan – during which time the load temperature is rapidly reduced from 950°C (1740°F) to 660°C (1220°F), bringing it to transformation point. Tray push rate and maximum product throughput fall into sync with the furnace.
The parts are then conveyed to a second, low-temperature furnace (LTF), and again this matches the high-temperature unit in terms of tray push rate and maximum product throughput. This furnace relies on three automatic temperature control zones and has six burners. It operates at between 630°C and 700°C (1170°F-1290°F) and uses a fuel-only control system for enhanced temperature uniformity.
DCIM100MEDIADJI_0077.JPG
After the secondary isothermal heat treat process is complete, the tray loads pass into a blast cooling tunnel (BCT). Cooling takes place with air at ambient temperature with forced convection downward by means of two axial fans. By the time parts exit the tunnel, they have been cooled to around 400°C (750°F).
In addition to the HTF, ICC, LTF and BCT, NUTEC Bickley is supplying all the external and conveying equipment for this line, including entrance and transfer cars, complete with car movement system; transfer car tracks; exit transfer cars, with tray dumper unit and car movement; integrated air cooling unit; return conveyor, with electrical dolly system to move trays to the transfer car; and loading station, directly on trays at the transfer car, featuring a carbon steel basket with a lift-rotation movement via a pneumatic cylinder system. The parts handling system operates fully automatically and is linked to the whole process via the Master PLC and HMI.”
“SECO/WARWICK India has signed a contract to supply a vacuum furnace to the renowned precision components manufacturer, Bhuj Polymers. This is an exceptional event for the SECO/WARWICK Group – the single-chamber VECTOR vacuum furnace will be built locally in India under the Made in India program. The equipment is being manufactured at the production plant in Pune.
The vacuum furnace on order will be used to carry out advanced vacuum hardening processes for tools, dies and rolls. The partner will process tool steels with high thermal requirements, such as H13, H11 and D2. Until now, technological capabilities were limited by a locally manufactured furnace with a cooling pressure of up to 4 bar, which did not allow for effective processing of components requiring high-pressure gas hardening. Increasing production loads and customer requirements, including one of the key partners, prompted Bhuj Polymers to invest in next-generation vacuum technology.
“The furnace delivered combines 15-bar high-pressure gas cooling with perfect temperature uniformity and precise control of thermal processes. This solution meets NADCA (tool & die global standard) requirements and is ready for NADCAP (aerospace global standard) certification, enabling Bhuj Polymers to offer vacuum hardening services to the most demanding customers from industries such as automotive and aerospace,” says Maciej Korecki, Vice President of the VacuumSegment of the SECO/WARWICK Group.”
Ipsen USA announces the successful ISO/IEC 17025:2017 reaccreditation of its Calibrations Lab, ensuring continued certification of inspection equipment used by Ipsen field service engineers to calibrate heat-treating systems across the U.S. and worldwide. The reaccreditation directly supports industries such as aerospace and medical where calibrated instruments are critical in producing high-precision parts. According to the International Organization for Standardization (www.ISO.org),
“ISO/IEC 17025 enables laboratories to demonstrate that they operate competently and generate valid results, thereby promoting confidence in their work both nationally and around the world.” For Ipsen customers, this means added assurance that their furnaces and heat-treating equipment aremaintained to exacting standards and remain compliant with industry specifications, such as AMS 2750, governing aerospace heat-treating processes. “Renewing our accreditation is largely a verification process, making sure that we are doing what we say we’re doing,” explained Cavan Cardenas, Ipsen Technical Training Lead.
“The reaccreditation process involves multiple audits, both internally and externally, virtually and in person, over the course of the two years since our initial accreditation.” The audits for the reaccreditation are overseen by Perry Johnson Laboratory Accreditation, Inc (PJLA), a private third-party accreditation body that validates the competency of testing and calibration laboratories. “We want to make sure that we’re giving the right instructions, following the instructions, and documenting the process,” Cardenas added. “Following this process ensures that we will continue to meet the ISO standards required by our customers, and that our system doesn’t have any blind spots.”
Luigi Moruzzi, Ipsen Customer Service Lab Technician, added: “We were able to collect our documentation and calibration certificates, making sure that all of our paperwork was up to date and confirming that they matched AMS 2750 and ISO standards. ISO reviewed our uploaded documentation and visited our lab for the audit, reviewing the documents and procedures with us, making sure that each piece of equipment that comes into the lab is inspected properly and leaves meeting strict quality specifications.”
(Editors Note; Milwaukee Forge has a substantial in house heat treating department with the ability to offer Normalizing, Annealing, Quenching & Tempering in a wide variety of furnaces)
“Milwaukee Forge, a 112-year-old company in Bay View, is being sold to a politically-connected ownership group for $4.6 million.
The company, located at 1532 E. Oklahoma Ave., is now being sold to a private ownership group after being placed in receivership earlier this year. Creditors previously reported the business had at least $9.3 million in outstanding liabilities, including bank loans and unpaid invoices from vendors and equipment suppliers.
Milwaukee Forge, which has operated since 1913, is being sold to an ownership group doing business as Milwaukee Forgetech, Inc. A holding company, Milwaukee Forgetech Holdings, LLC, is registered to Phillip Prange, of Waukesha. Prange is a former lobbyist, well-connected Republican and a co-founder of the publication WisPolitics, and currently the Senior Government Solutions Architect for Fiserv. He is married to Alison Prange, managing director of Michael Best Strategies and the former COO of the 2024 Republican National Convention host committee.
The company provides heat-treating and forging services. It operates out of a 132,000-square-foot facility on an eight-acre property in Bay View owned by an affiliate.
In March, creditors petitioned in state court to have the company placed in receivership. Milwaukee County Circuit Court Judge Thomas J. McAdams granted the petition and ordered the company and its assets placed under the control of a court-ordered receiver, attorney Michael Polsky.
At first, the company kept up operations, and President and CEO Dave Mesick said all employees would stay on. “It’s business as usual,” he said in a press release in March. By June, though, the company filed a notice with the state reporting it would start laying off 67 employees in August as a result of the delayed sale.
Initially, Polsky sought to sell the company’s assets as a going concern. However, attempts to sell the business at auction were unsuccessful. Then, in late August, Polsky sought a hearing before McAdams seeking approval of a sale to Milwaukee Forgetech. McAdams approved the sale Friday, Nov. 13.
It is the second time Milwaukee Forge has been sold out of receivership. In 2010, Mesick led an ownership group that purchased the company for $7.1 million.
City of Milwaukee Mayor Cavalier Johnson and County Executive David Crowley both wrote letters to the court in support of the sale. The officials wanted to see the company sold in order to continue operating and providing union-represented jobs. The ownership group has indicated it will represent and bargain with the unions representing Milwaukee Forge workers: the International Association of Machinists and Aerospace Workers Local 140 and the United Steelworkers.
“This is a facility with a long history of industrial production and employment that contributed to the city’s economy,” Johnson wrote.”
Commercial heat treater “Bodycote”, the globe’s largest commercial heat treater on Tuesday, released a report forthe four months ending October 31, 2025. As a diversified, global heat treater their results mirror the entire heat-treating industry-it comes as no shock to us or indeed for most heat treaters that aerospace & defence are strong, automotive and industrial not so much. This report from “AJ Bell”, gives as good a summary as any’
“Bodycote PLC on Tuesday reported improving trading momentum across most of its end markets in the four months to October 31, although group revenue growth remained held back by ongoing plant closures under its restructuring programme.
The Macclesfield, England-based metal heating company said core organic revenue rose 2.2% year-on-year in the period, an improvement on the first half, leaving year-to-date core sales down 1.4% compared with a 3.6% decline in the first six months.
At group level, organic revenue edged up 0.3% as the company continued to wind down non-core sites as part of its multiyear Optimise programme.
Year-to-date group revenue was 2.7% lower at £613 million, compared with a 4.6% drop at the half-year stage.
Bodycote said Aerospace & Defence was the standout performer, delivering ‘strong’ and accelerating growth, helped by a ramp-up in work related to LEAP aircraft engines.
Automotive and Industrial demand remained challenging but showed better year-on-year trends due to easier comparatives, Bodycote said.
Oil & Gas remained a drag, with low upstream investment in the Middle East delaying the ramp-up of recent contract wins.
The Specialist Technologies division saw organic revenue fall 1.8% in the period and remain 5.4% lower year-to-date, although Bodycote said momentum strengthened in September and October.
In HIP Product Fabrication, several defence-related contracts won in the first half are expected to drive a higher level of deliveries in the fourth quarter.
The Precision Heat Treatment division posted 4.1% organic revenue growth in the period, turning year-to-date performance positive at 0.6%. Industrial gas turbines and aerospace drove the gains, while automotive demand improved modestly.
Bodycote said execution of its Optimise programme accelerated, including revenue transfers to core sites and progress on the planned sale of 10 French automotive and industrial locations.
The company expects to have exited more than one-third of the remaining 20 non-core sites by year-end.
Looking ahead, Bodycote reiterated that second-half operating profit will be higher than the first half and ‘broadly in line’ with the £62.2 million delivered in the second half of 2024.
‘Our focus remains on execution as well as delivering on our Optimise, Perform & Grow initiatives, which will create a higher-quality, more resilient and faster-growing Bodycote,’ the company said.
Bodycote shares were 0.4% lower at 600.00 pence in London on Tuesday morning.”
Ten Ipsen field service engineers are completing Pyrometry II training through the Performance Review Institute (PRI), a national organization that focuses on certification for processes that need to meet Nadcap and AMS standards. These engineers are on track to be fully certified by the end of December 2025.
“While Ipsen has had calibrations staff on hand trained in AMS and Nadcap pyrometry standards for years, this push for expanded training helps our field service engineers better understand the fundamental technical knowledge behind the testing and results,” explained Cavan Cardenas, Ipsen Technical Training Lead. “Understanding the context behind the testing process helps our service team better understand why the standards need to be met and helps us push to meet those standards.”
The call to expand Pyrometry II certification to Ipsen field service engineers was discussed prior to the October 2025 PMI Calibrations Conference, held in Pittsburgh, Pennsylvania. At the meeting, Cardenas connected with certified trainers and industry leaders, each of whom encouraged the pursuit of expanding calibration knowledge across service lines. “We’ve typically offered field technicians a basic, fundamental pyrometry course to deliver essential information to understand physically what they may be doing on the job,” Cardenas explained, “but by offering this higher level of training to our FSEs, we can make sure Ipsen’s customers have confidence that their future Nadcap AMS audits go well, providing them with a higher level of service.”
Cardenas projects ten additional Ipsen field service engineers completing their Pyrometry II certification in the first half of 2026. Pyrometry II certified FSEs will also be expected to review updates from each AMS 2750 revision every two years, with a full recertification planned every fifth year. “It’s like we say in the ISO world: say it, do it, prove it. Training in depth about the process of pyrometry, studying calibration with industry experts, and taking those skills with us into our customers’ production line help us better explain what we’re doing, why we’re doing it, and show proof that we’ve done it properly,” Cardenas concluded. For more information on Ipsen’s pyrometry services, visit https://ipsenglobal.com/calibrations/.
“Fort Worth, Texas — November 17, 2025 — Southwest Metal Treating Corp (SWMT), a leading provider of precision heat-treating services and an AS9100D / ISO 9001:2015 and NADCAP-accredited facility, is proud to announce the addition of a new TRU-CRYOTHERM 36x48x36 system from “McLaughlin Furnace Group”.
The new unit has been delivered and is currently installed as part of SWMT’s ongoing expansion of its Integral Quench (IQ) department. This investment further enhances SWMT’s ability to provide advanced, consistent, and high-quality heat-treating and cryogenic processing solutions for aerospace, defense, and precision manufacturing partners.
“The TRU-CRYOTHERM expands our thermal processing capabilities and strengthens our ability to meet demanding specifications with precision and reliability,” said Ryan Fussell, CEO of Southwest Metal Treating Corp. “As we continue to invest in state-of-the-art equipment, our goal remains the same — to provide our customers with unmatched quality, turnaround, and technical excellence.”
The TRU-CRYOTHERM’s robust design, advanced temperature control, and uniformity standards make it an ideal complement to SWMT’s growing IQ and vacuum processing operations. With this addition, SWMT continues to set a higher standard for metallurgical performance and process consistency across its full range of services. According to “Jeff McLaughlin”, founder and owner of the company this -300F to +1400F unit is the first gas fired system on the market.
About Southwest Metal Treating Corp; Founded in 1985 and based in Fort Worth, Texas, Southwest Metal Treating Corp (SWMT) provides a full range of heat-treating and cryogenic services to aerospace, defense, and industrial markets. SWMT maintains NADCAP accreditation and AS9100D / ISO 9001:2015 certification, ensuring compliance with the highest quality and process standards in the industry. For more information, visit www.southwestmetaltreating.com or contact [email protected].”
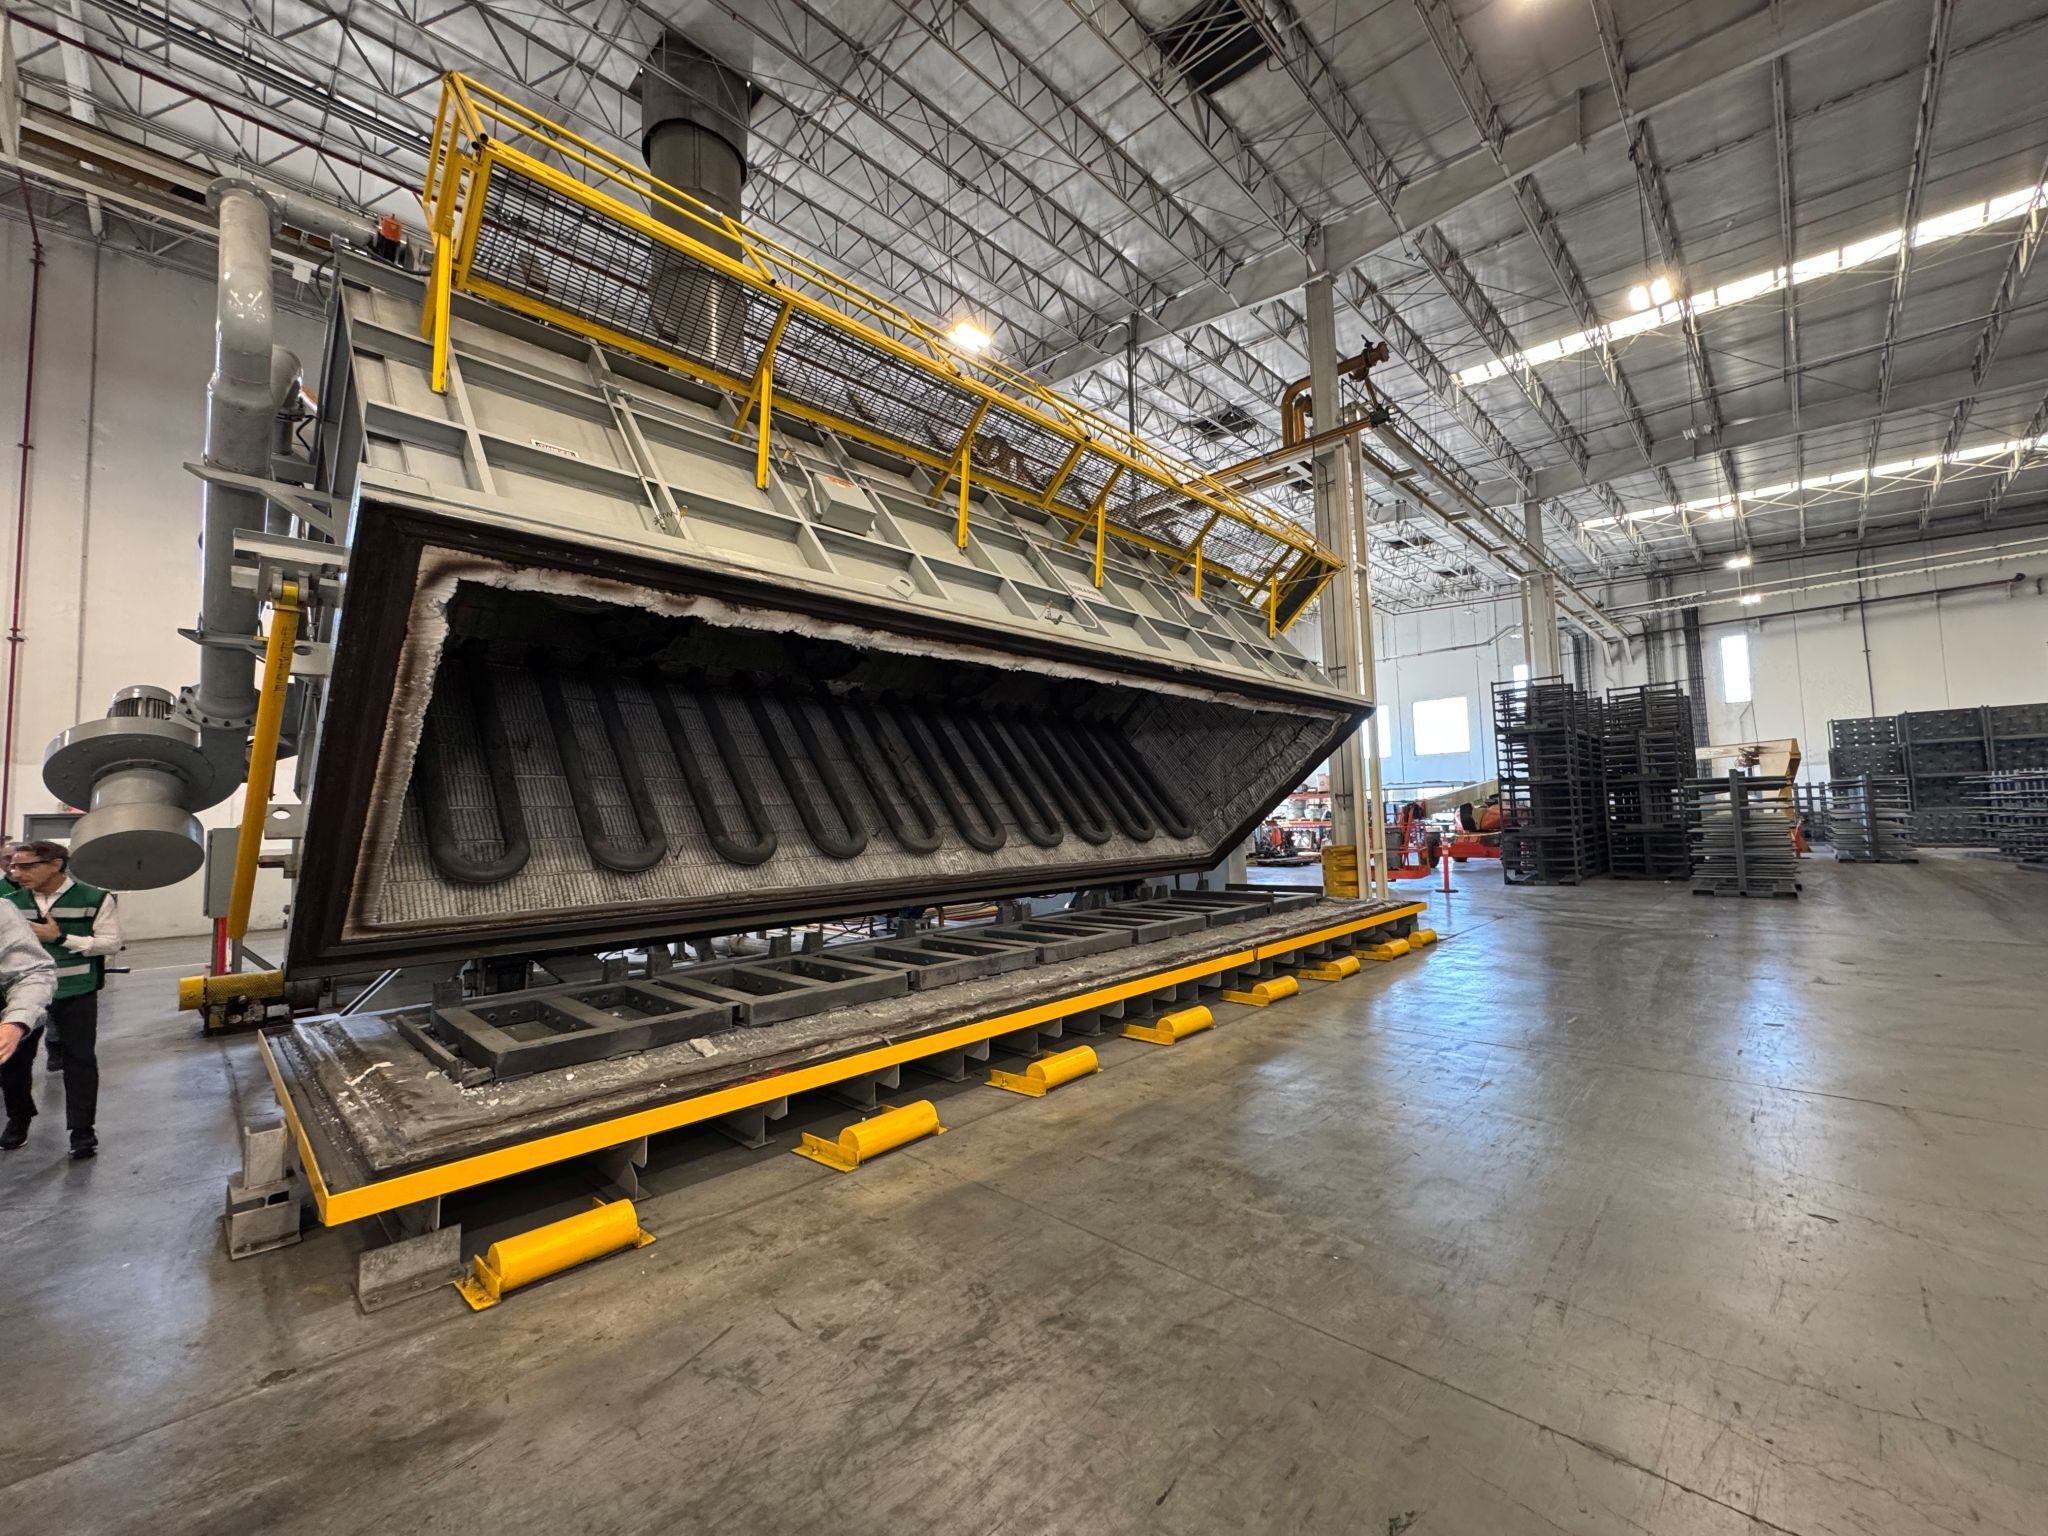
Back in 2009 furnace builder JL Becker, Co., (acquired by “Gasbarre” in 2011) working with commercial heat treater “Woodworth, Inc.”, in Flint, Michigan, USA revolutionized the automotive brake rotor sector by offering FNC (ferritic nitrocarburizing) in large tip-up furnaces.
The benefits of the process were readily apparent and combined with the economy of scale offered by the very large volumes (50,000 pound loads as an example) the tip up furnaces were capable of meant that the process was quickly adopted by most of the large automotive companies. This success propelled Woodworth into one of the largest commercial heat treaters in North America “52 Largest North American Commercial Heat Treaters 2025”.
This success lead another other commercial heat treaters to enter this market, US based “Paulo”(now part of “Aalberts Surface Technologies”) set up a plant in “Monterrey, Mexico”in 2018 offering the same process in the same furnaces. The subject comes up today as “Aalberts” has recently been “showcasing” the plant, this includes these very interesting pictures showing one of the furnaces both empty and full.
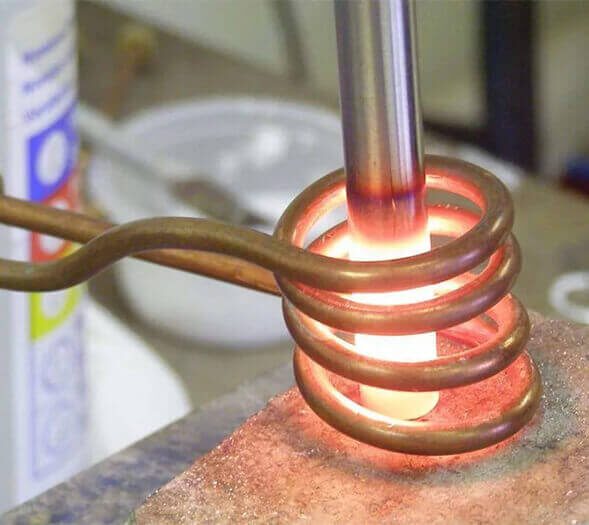
“Aluminium extrusion company Extrutec North America, has acquired Induction Professionals, leading to the formation of the new company Induction Professional Solutions (IPS). The acquisition will combine Extrutec’s energy efficient technology with Induction Professionals extensive experience to provide customers with advanced heating solutions.
Uwe Günter, managing partner of Extrutec, said: “We are thrilled to welcome Induction Professionals assets and expertise into the Extrutec family, “This is an exciting and strategic step for our company. By integrating Induction Professionals’ capabilities into our North American operations, we are well-positioned to offer a comprehensive portfolio of the most modern, energy-efficient induction heating solutions.
“We are committed to building on the foundation of trust and quality that Tom Kearney and his team have established.” Kearney, the former owner of Induction Professionals, will serve as general manager of IPS. As well as heating systems, IPS will also provide comprehensive service repair, and upgrade solutions. The new company will be situated in Induction Professionals former facility in Youngstown, Ohio.
Kearney added: “By joining forces with Extrutec to form IPS, I am confident that we are entering an exciting new chapter that will bring you even greater value. “Combining our local expertise with Extrutec’s global resources and cutting-edge technology will enable us to offer a broader range of products and services.”