- We were chatting the other day and you mentioned how “McLaughlin” just received an order for a pit nitriding system along with several other inquiries which you are optimistic will turn into orders. What can you share with us about the order and can you give us your thoughts on why gas nitriding inquiries appear to be ramping up these days?
A: I can’t share all the specifics, but I can say that the order is for a gas-fired pit nitriding furnace that includes a McLaughlin dissociator/incinerator system. This is a dual-function unit that produces dissociated ammonia while also handling exhaust incineration in a single integrated system. We have installed quite a few of these systems and have had great customer feedback.
As for the increase in nitriding demand, I believe it’s driven by a continuous push across industries for improved part performance and extended life. Additionally, our recent increase in inquiries is largely due to our ability to offer shorter lead times and our flexibility in customizing equipment to meet specific customer requirements. - Historically has nitriding been a “core competency” at McLaughlin or is this a market that you are growing into as market demand grows?A: Nitriding has been part of our capabilities in the past, but I would say it’s an area we are now actively strengthening. Our goal is to add nitriding furnaces as a core product line that we are known for. We are investing time, resources, and engineering focus into this market because we see strong long-term demand and opportunity.
- At the “FNA” show in Indianapolis you introduced a brand new product for the company, a “TRU-CRYOTHERM” about which you were very excited. Perhaps you could tell us what this product is and what market niche it fills? A: The TRU-CRYOTHERM is a dual-process system that combines a cryogenic freezer with elevated temperature capabilities, operating across a wide range from -300°F to 1200°F. This versatility allows customers to perform both deep cryogenic treatment and thermal processing within a single unit.We offer fully customizable sizes and configurations, including direct gas-fired designs. The product fills a gap in the market where there are limited solutions offering this combined capability. Our approach focuses on delivering industrial-grade, robust equipment that meets demanding production environments while providing long-term reliability.
- Has it been a successful product line for you? Perhaps another way of phrasing this question is how many units have you sold and how many do you predict for 2026 A: Yes, it has been a successful launch for us. To date, we have sold five TRU-CRYOTHERM units. Looking ahead, we are targeting to double that number in 2026 as awareness grows and more customers recognize the value of this technology and the McLaughlin’s quality.
- Out of all of the product lines you offer which one would you say has proven to be the most successful? Let me put is another way-is there anything you offer where you feel absolutely, 100% confident that it is the best offering in the industry bar none? A: Without question, our TRU-MIX generator stands out as a best-in-class product. Over the past year, we have achieved record sales for this system, which validates its performance and reliability.These units have transformed customer operations by providing consistent, high-quality atmosphere control—something that is critical in heat treating. Many customers struggle with gas consistency, but once a TRU-MIX generator is installed, that concern is essentially eliminated. It allows them to focus on other aspects of their operation.
- McLaughlin Furnace Group since day 1 has been extremely successful in a particular style of furnace, a style which many in the industry probably don’t associate with the company-carbottom furnaces. I am sure our readers would like to know why you excel at this product, how many you have built over the years and what is the largest you have built? A: Car bottom furnaces align extremely well with our core strengths heavy fabrication, pulse-fired combustion systems, and custom engineering.Over the years, we have built more than 15 car bottom furnaces. We have built car bottoms ranging from over 50 feet long and 25 feet wide to much smaller units. Beyond size, our real strength lies in custom engineering solutions that significantly improve process efficiency and cycle times for our customers.
- The most popular style of furnace in North America by a very wide margin is the tried and true batch IQ furnace (sealed quench for our European readers). It is also the hardest market for new (or newer) furnace builders to break into as there are a couple of long entrenched suppliers in the industry. You broke into this market 3 or 4 years ago-are you continuing to make in roads into this arena? A: Absolutely. We are currently building multiple units and continuing to expand our presence in this market. Our TRU-CARB IQ furnace is designed to be one of the most innovative and consistent systems available. We’ve focused heavily on performance, repeatability, and ease of operation and maintenance, which is helping us gain traction even in a competitive market.
- I have run across a couple of very large projects “McLaughlin” has been involved with over the years either completed or partly completed. Are you able to share any details about these projects? A: While we’ve discussed several new equipment projects already, I also want to highlight our rebuild and retrofit capabilities. This is an area where we bring a unique perspective.We help customers upgrade and modernize their existing equipment rather than replacing it entirely. In many cases, we’ve been able to significantly improve performance and extend equipment life while saving customers substantial capital investment.
- Back in 2023 I asked you and Ben to make a prediction about the heat treating market in 2024. At the time Ryan you said you didn’t have time to think about a recession and that your were predicting a great 2024. Ben concurred with that statement. So did you prove to be correct about a very good 2024. Yes, it did. We saw continued growth in 2024 and 2025, and overall, it has been a very strong period for us and for the industry.
- Last question Ryan, what can we expect to see from “McLaughlin” in 2026? New technologies? Acquisitions perhaps? Growth into oversea markets? You can expect continued growth and expansion across several key areas. We will be increasing our presence in nitriding, cryogenic systems, and car bottom furnaces. In addition, we are expanding our service and support footprint across the United States.Overall, 2026 will be focused on scaling our capabilities, strengthening our product lines, and continuing to deliver high-quality, customized solutions to our customers.



ORIGINAL ARTICLE (OCTOBER 2023) Lets start with some basic background; “The Winning BLW Group develops, produces and sells drive and synchronization elements for the automotive industry at 3 locations in Germany. With more than 72 years of experience in the field of precision forming, the company is an innovative and competent partner to the national and international automotive industry as well as its suppliers Home – Winning BLW GmbH”.
As you would expect the firm’s heat treating requirements are substantial and for its most recent facility in Penzberg, Germany the company turned to one of the largest commercial heat treaters in the country “Hanomag” for assistance in their heat treating needs Hanomag: Home (haertecenter.de) (to find out the relative size of Hanomag we would suggest this ranking as provided by “The Monty Heat Treat News” Largest European Commercial Heat Treaters | The Monty).

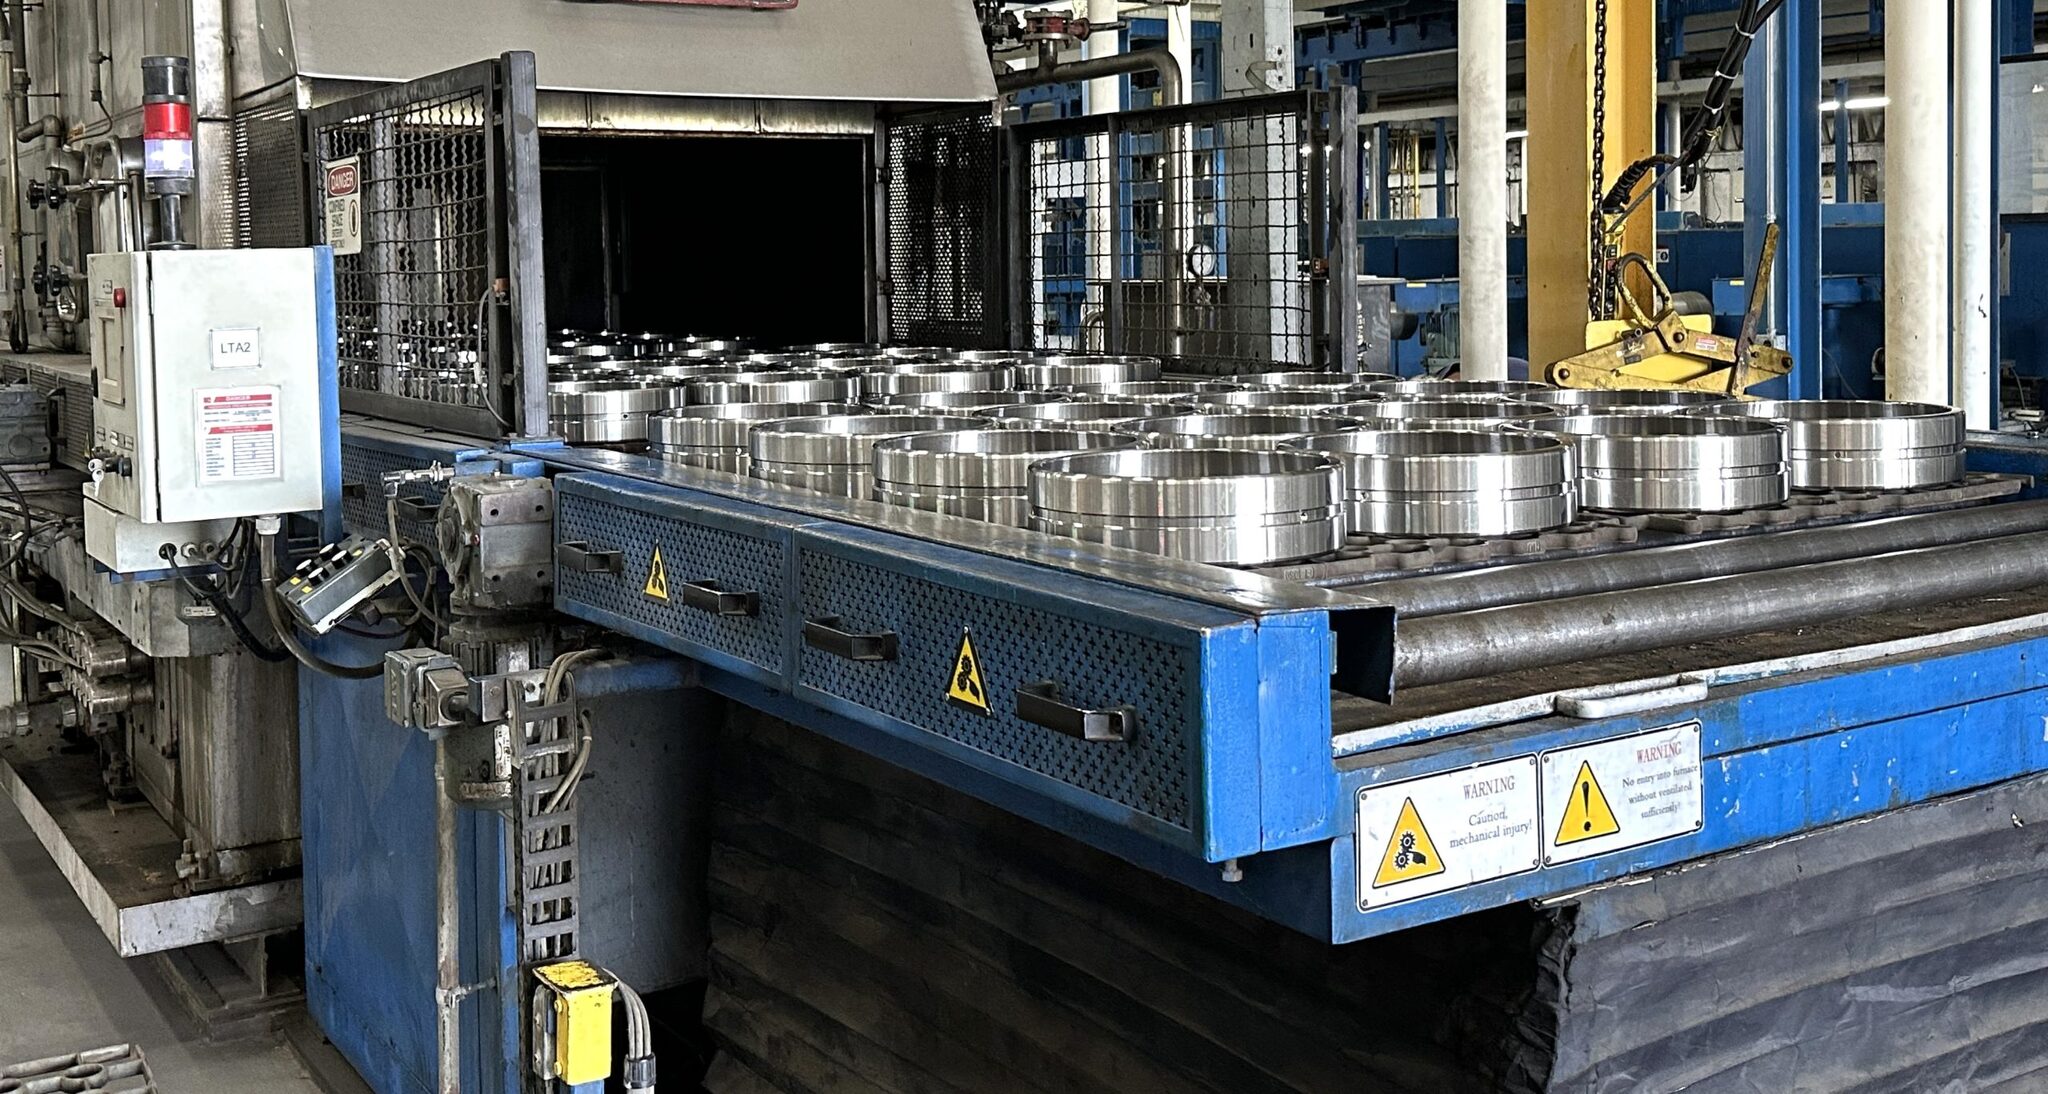
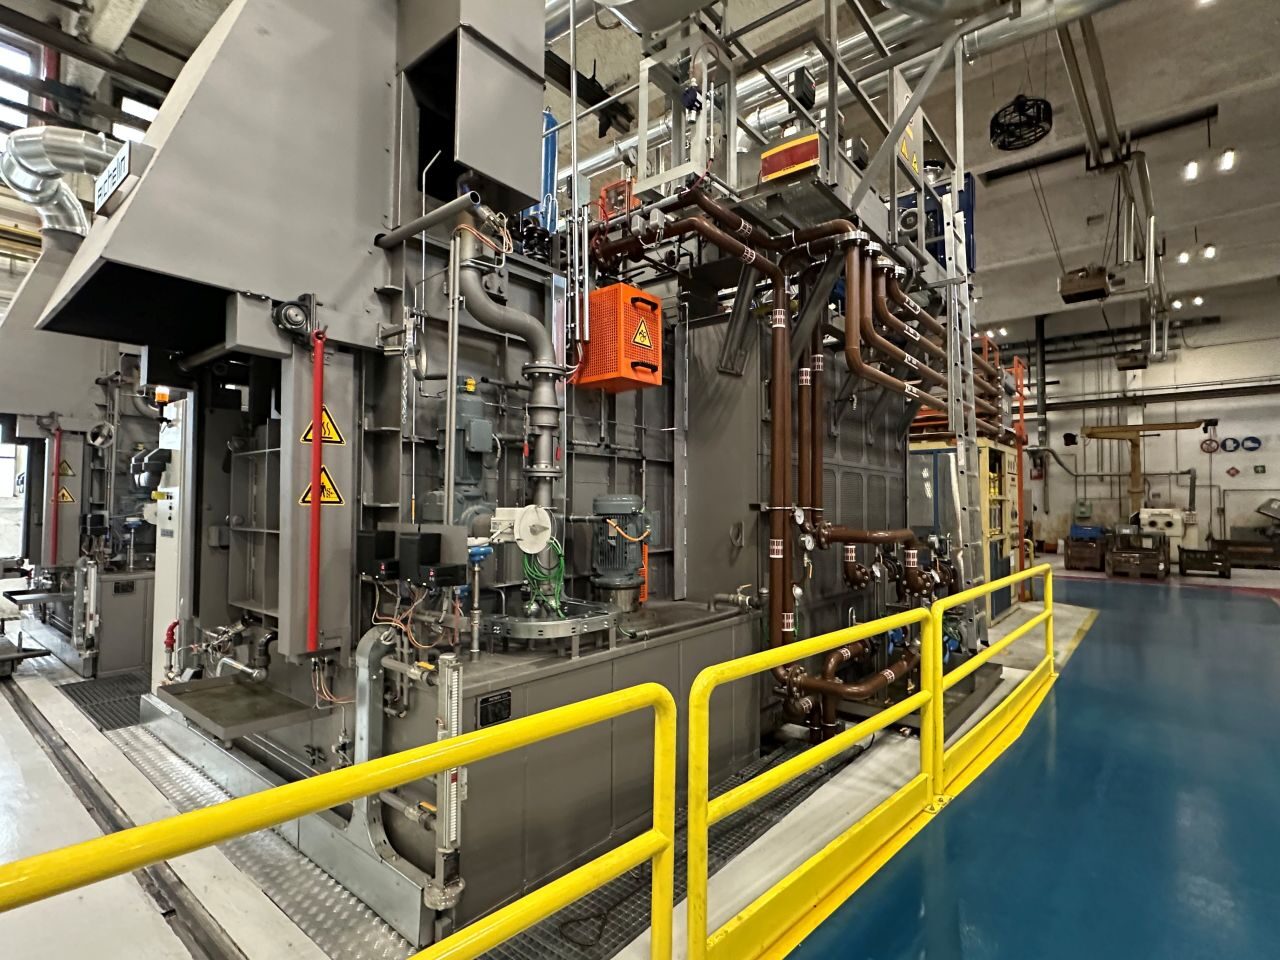
The heat treat department will be staffed by roughly 25 individuals all of whom will be Hanomag employees. Currently the furnaces are just entering production with full production expected in 2024. The Aichelin sealed quench line is completely automated and can be considered a “lights out operation”. All furnaces are gas fired with atmosphere provided by 3 endothermic generators, atmosphere is controlled by oxygen probes with portable 3 gas analyzers and regular shim stock checks providing backup.
While this location’s heat treating needs are being provided by Hanomag, Winnings’ Munich location handles their own in house heat treating which includes nitriding and vacuum hardening. A number of the largest commercial heat treaters in the world have targeted in house heat treating departments as a natural progression for their businesses but it is still not a common occurrence. This is one of the best examples we have seen and while this project is in it’s initial stages it would at this point in time appear to be a “win/win” situation for both companies. These photos tell the rest of the story.





 For some time now “The Monty Heat Treat News” has been aware of a smaller heat treat furnace builder in Michigan, USA being for sale. The prospectus has this to say about the company;
March 10th, 2025 “The Monty Heat Treat News” had a story about vacuum furnace builder “TAV” landing an order for their “1,001st New Vacuum Furnace”–we learned this very interesting fact during a visit to the firm’s headquarters in Bergamo, Italy (close to Milano, Italy).
During a very interesting visit hosted by Mr. Guido Locatelli (General Manager), Mr. Marco Baretti, (Area Manager) and Mr. Jan Massholder (Managing Director, Furnacare) we learned a number of very interesting facts about the company;
The reasons for this success are many and varied, however in our opinion a large factor is the company’s laser like focus on one technology and one only-vacuum furnaces. The company has never ventured into the “atmosphere” market and as far as we can tell they have no plans to do so.
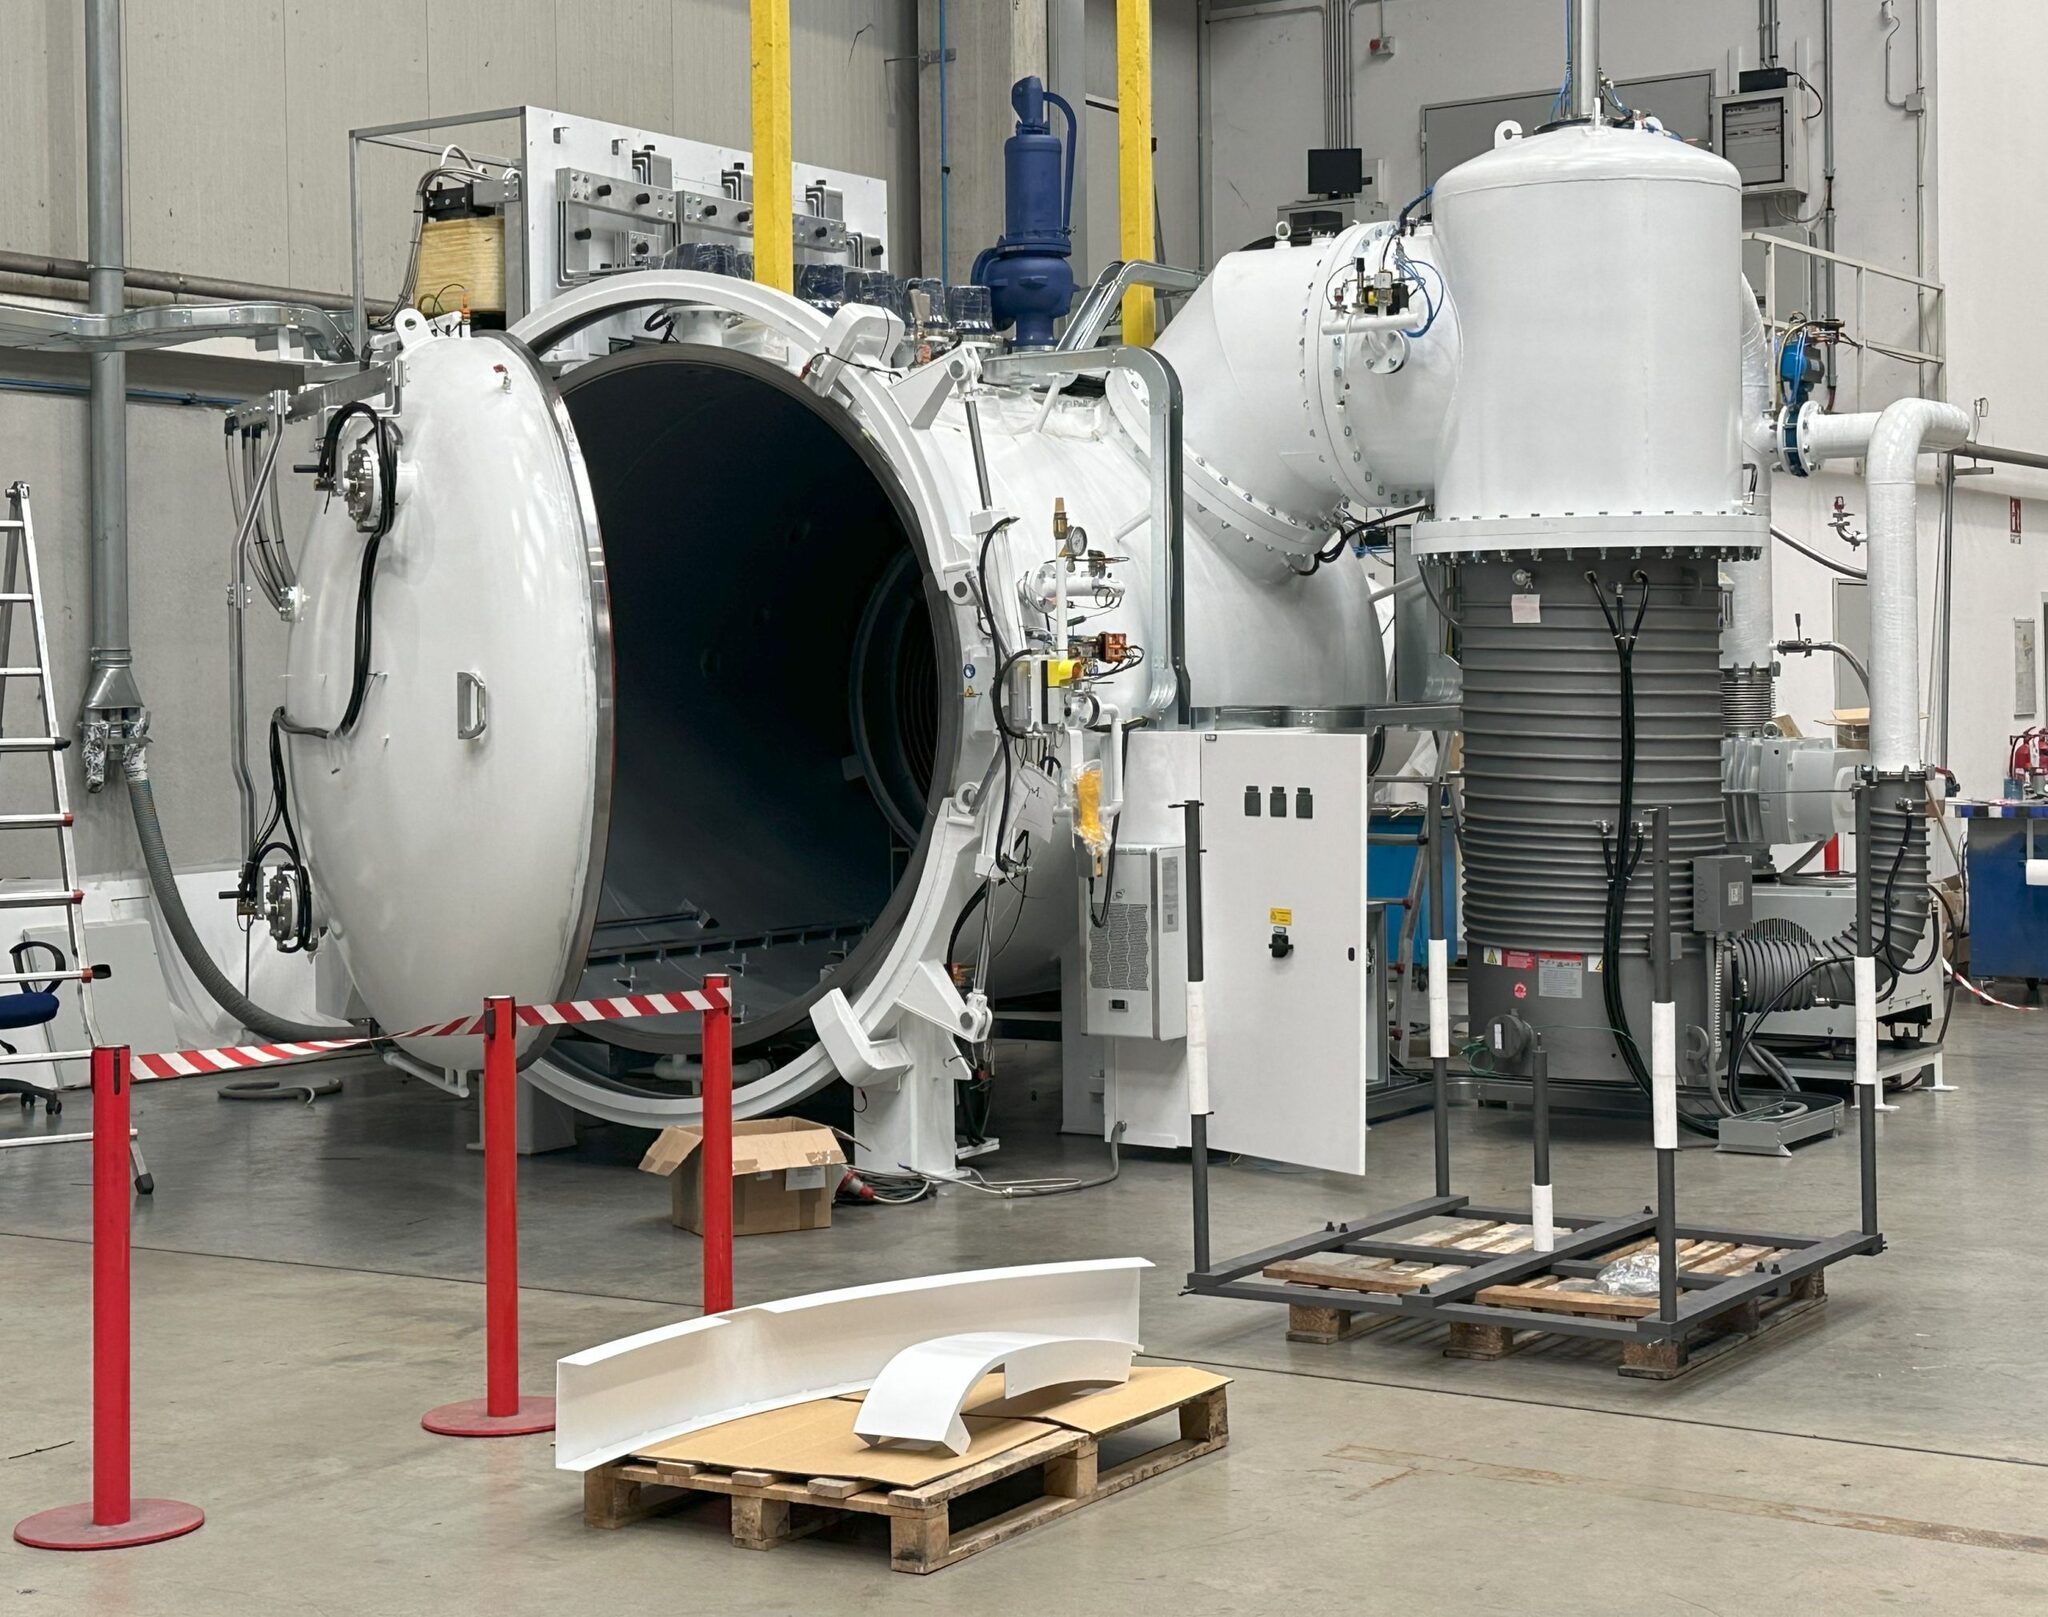
This focus on vacuum has certainly not stopped the company from entering the “LPC” (low pressure carburizing) arena as we inspected a brand new “LPC” system with 20 bar quenching that “TAV” has in their R & D department,-the “LPC” system can be clearly seen in the one photo in this article.
In the capabilities arena we can say that the company produces both horizontal and bottom loading vacuum furnaces capable of up to 2500C with vacuum levels down to 10-8 Torr (speaking of bottom loading vacuum furnaces you can see a prime example in these photos, a bottom load furnace almost ready to ship to an aerospace customer in India). In addition, “TAV” can make vessels capable of up to 100 bar pressure. On a side note, the firm keeps most of their supply chain local which greatly speeds up delivery time. This includes a local firm being acquired by “TAV”which for years has produced all the chambers required.
“Hot Zone Construction”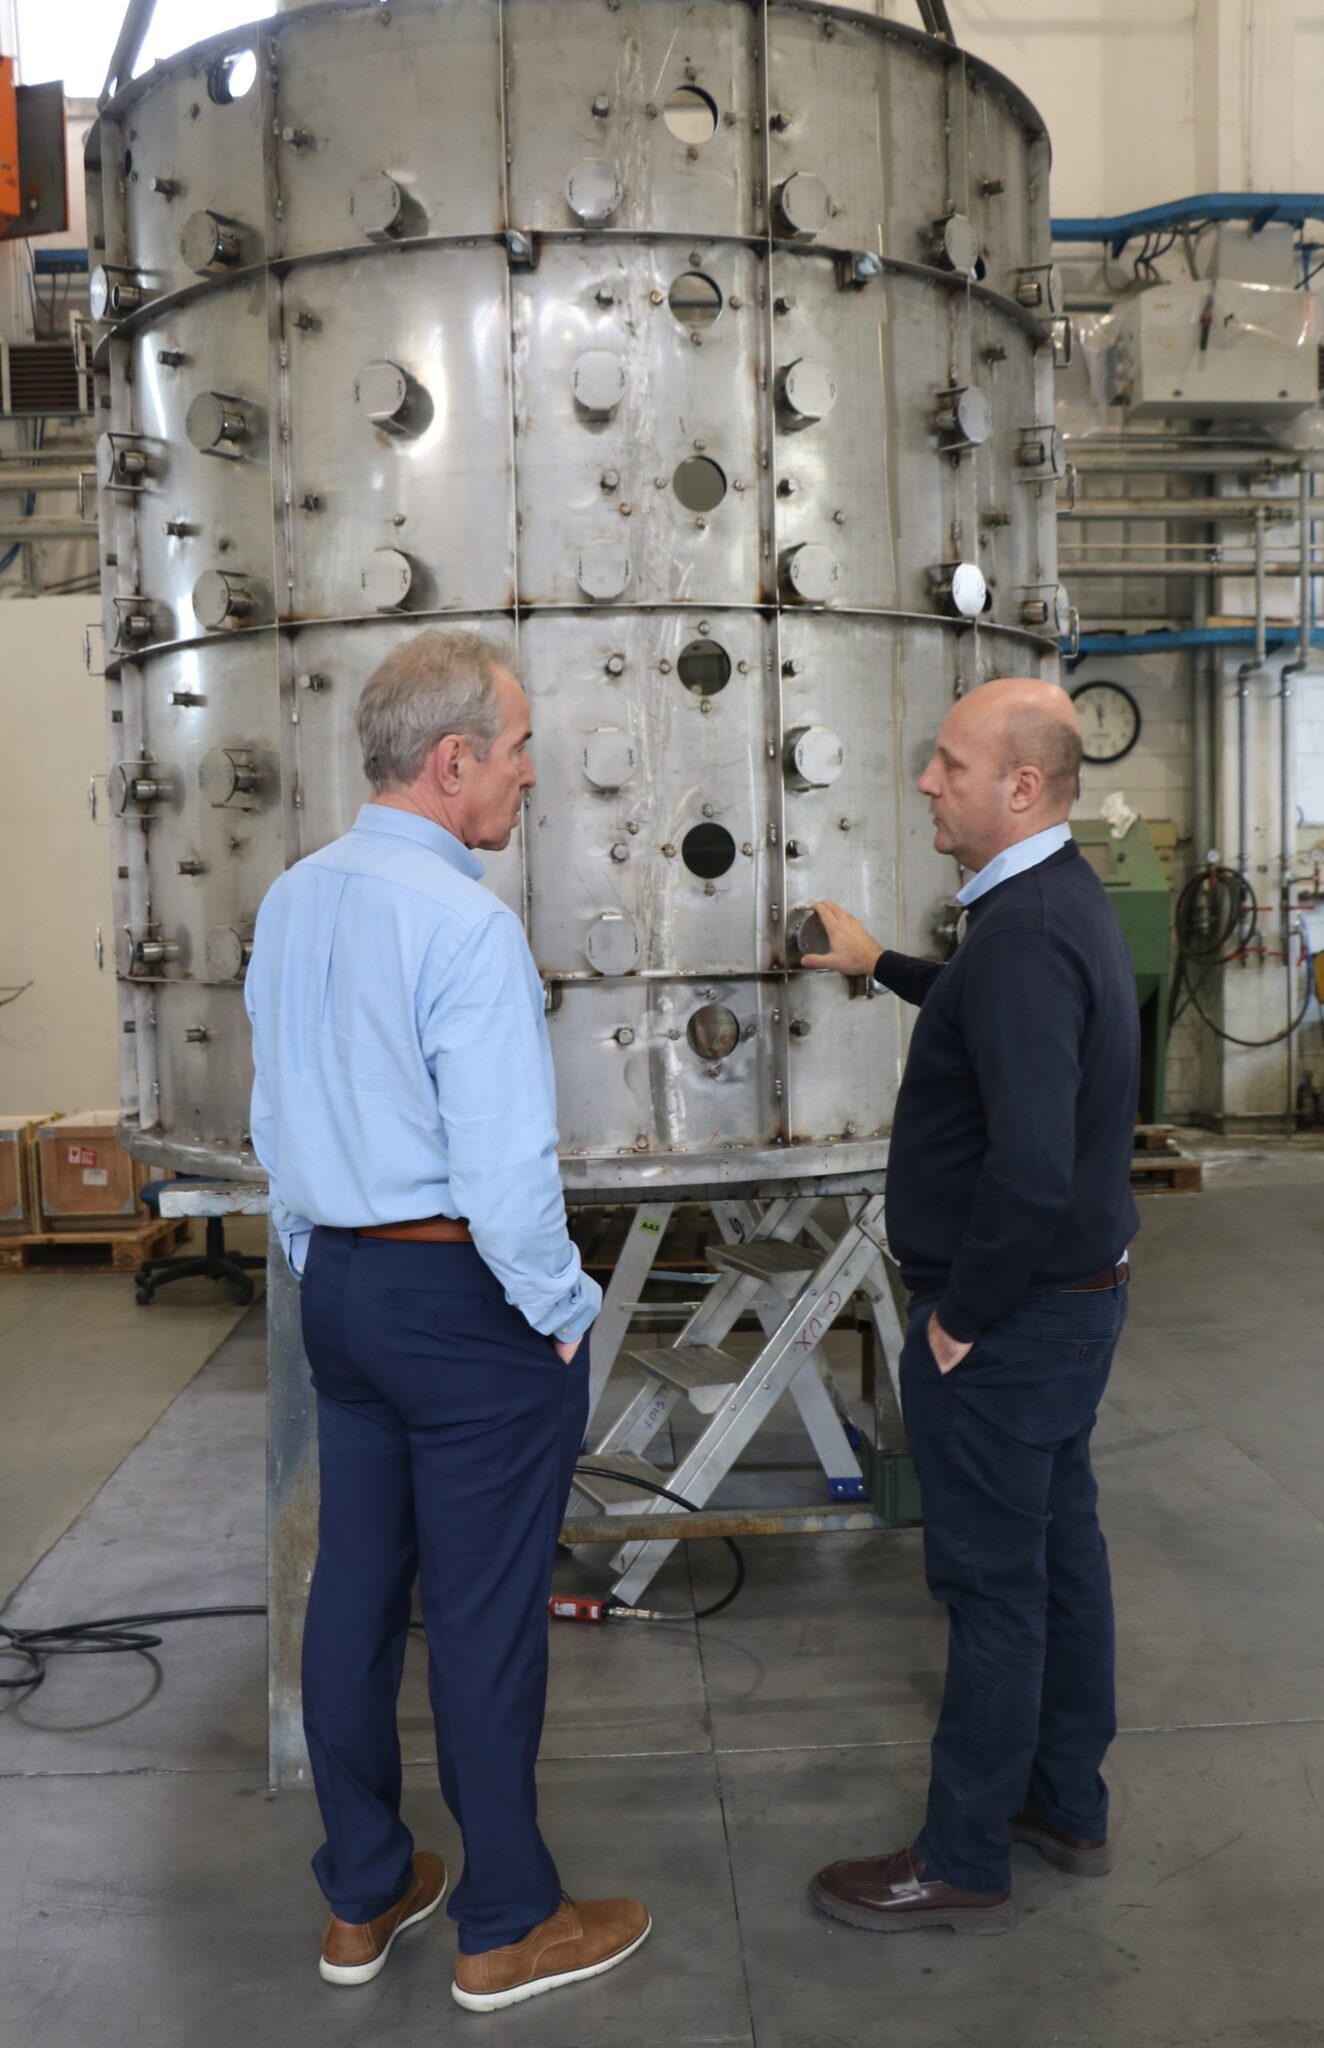
Earlier we suggested that part of the success of the company is due to the fact that they focus all of their energy on vacuum technology only-while this true there is another reason “Guido” told us was a factor in their success. “TAV” has always worked very closely with their customers on process development, in other words they help their customers come up with the correct process for their particular parts. This is reflected in the fact that the “R & D” department (shown in some of these pictures) has 4 furnaces entirely dedicated to helping their customers achieve the correct metallurgical results, these systems can also help customers with short term production.
While the Bergamo, Italy location services South America, Europe, Scandanavia and Aisa, North American Sales & Service is handled by the “Furnacare” division of the company located in Spartanburg, SC, USA. This facility was established in 2015 and over the years it has been responsible for selling and installing 75 furnaces in the US-as a matter of fact the US has been the largest market for “TAV” the past 4 years running. As an example of this out of the 11 or so furnaces we saw on the assembly floor, roughly half are destined for the US market. As mentioned earlier Mr. Jan Massholder is the Managing Director of this facility.
We thank the entire “TAV” team for their time and hospitality.


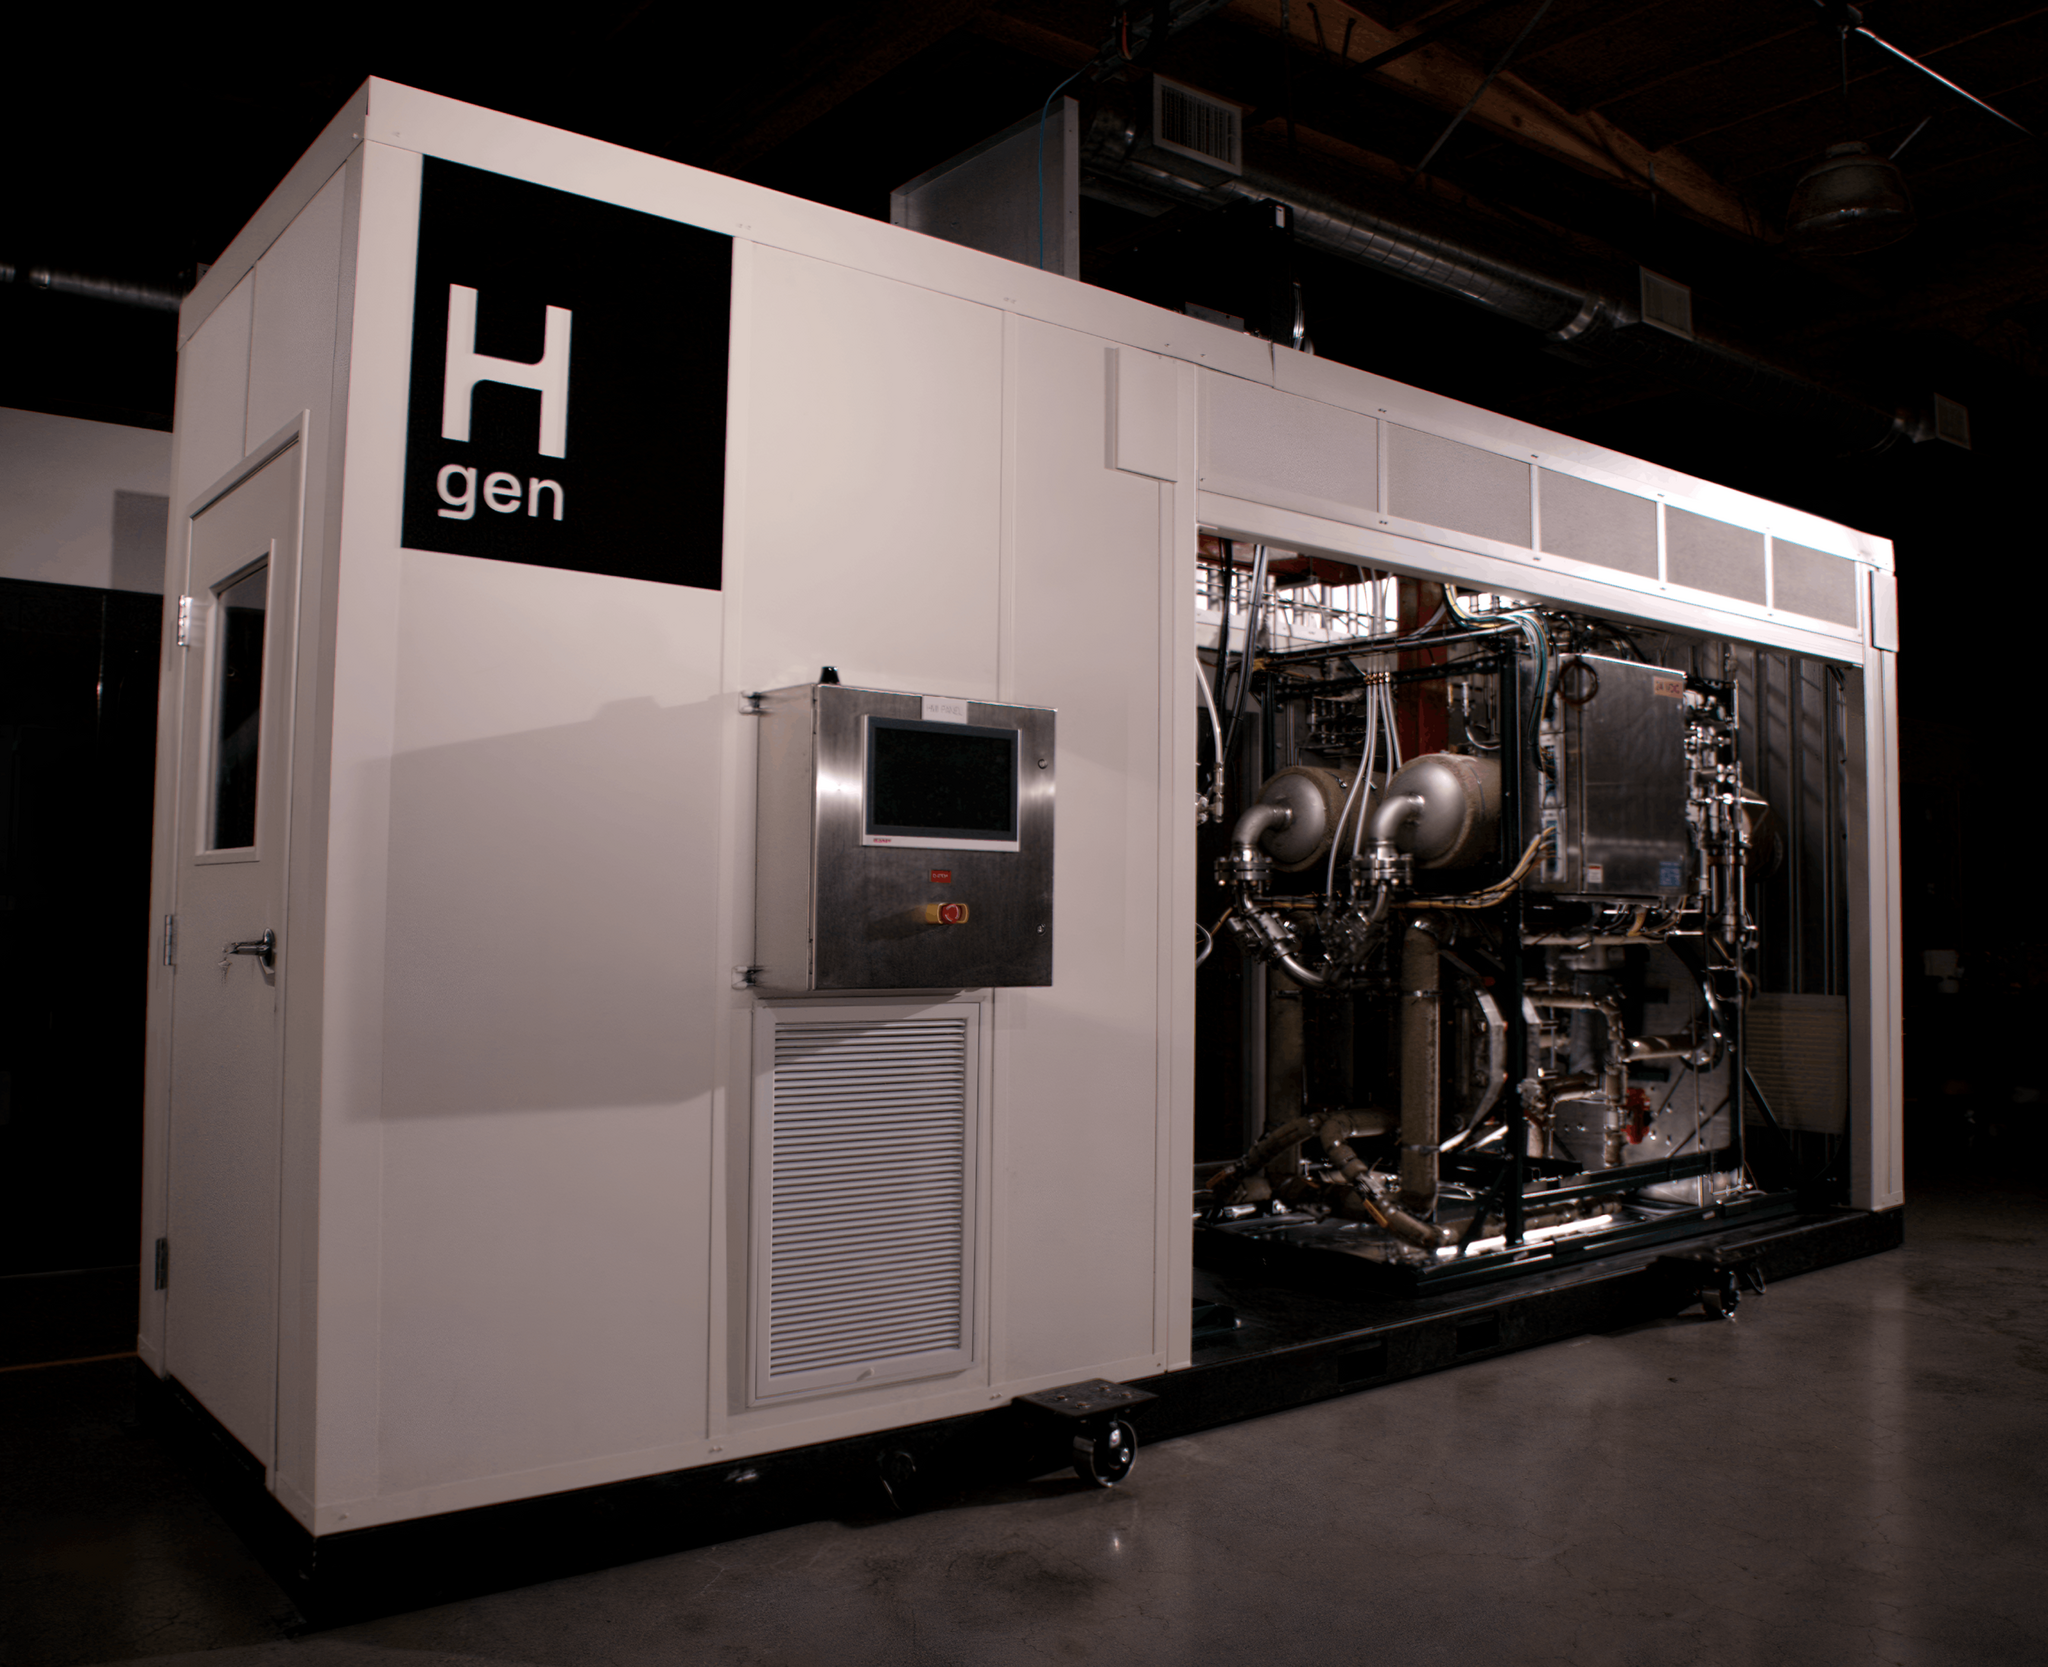
Installation of Hgen equipment at the Rancho Dominguez plant in the U.S. supports commercial and environmental objective
- Durable and compact Hgen module to produce hydrogen and oxygen from electricity and water
- On-site industrial gas generation reduces dependence on third-party hydrogen supply chains and associated road transport impacts
- Installation creates a pathway to lower cost of hydrogen and reduced emissions, advancing broader decarbonization objectives

Hydrogen is an essential industrial gas used in Bodycote’s precision heat treatment and surface coating technologies, treating metal and metal-alloy components for the aerospace, defense, automotive and energy sectors. This installation provides a lower-cost, lower-emissions solution.
The new system at Rancho Dominguez generates hydrogen at the point of use from electricity and water, eliminating impacts associated with bulk hydrogen transportation, distribution, and vendor handling and reducing associated emissions by more than 90%. It will also help drive down the cost of hydrogen.
Bodycote partnered with industrial gas innovator Hgen to deploy the hydrogen generation system at the plant. The Hgen module footprint is 20 times smaller than alternatives that produce the same gas volume, reducing system cost and space requirements. Its modular, expandable design allows production capacity to scale with process demand, supporting efficient resource use at Bodycote’s California site while strengthening long-term supply security.
The containerized module was supplied pre-assembled, minimizing custom integration, and installation took less than two weeks.
“On-site gas generation avoids the need for expensive gas compression, transport, and storage,” says Molly Yang, Chief Executive Officer at Hgen. “The high efficiency of Hgen’s technology allows Bodycote to reduce gas costs while advancing its sustainability goals.”
Success at Rancho Dominguez is expected to pave the way for broader deployment of distributed hydrogen generation across additional sites, reinforcing Bodycote’s long-term energy transition strategy and sustainability commitments.”