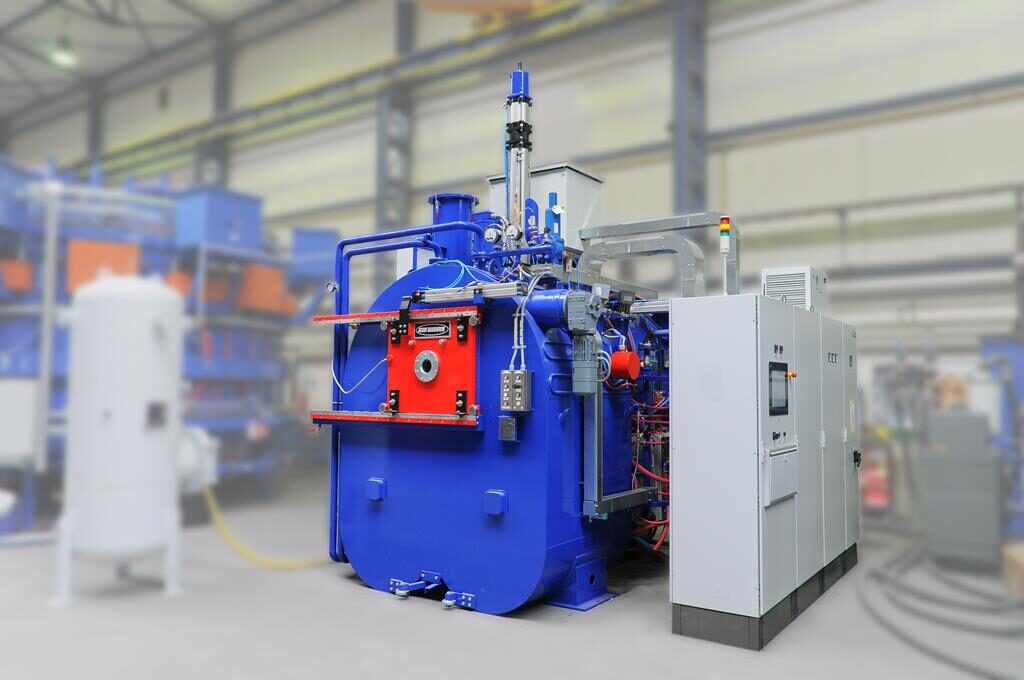
Ipsen USA is expanding the TITAN assembly line at its Vacuum Technology Excellence Center in Cherry Valley, Illinois. This major investment is expected to increase production capacity from 36 TITAN vacuum furnaces per year to 60, allowing the company to better meet growing global demand.
The expansion comes on the heels of a record-breaking month; in May alone, Ipsen received orders for 21 TITAN furnaces, driven by continued investment in the aerospace and energy sectors.
Since its debut in 2009, the TITAN platform has become one of Ipsen’s most successful product lines, with more than 450 systems installed worldwide. Engineered with standardized features, competitive pricing, and shortened delivery times, TITAN provides manufacturers with a reliable and cost-effective vacuum heattreating solution.
By transforming Ipsen’s former showroom into a dedicated TITAN assembly area, the expansion optimizes production flow while keeping engineering, manufacturing, and assembly under one roof. The project adds approximately 7,000 square feet of production space, with customer orders already scheduled to be built in the new area starting in July. This added capacity positions Ipsen to support rapid growth without compromising on quality or performance.
“We continue to see strong demand for the TITAN product line, and we’re investing today to ensure we can support our customers tomorrow,” said Geoffrey Somary, CEO of Ipsen. As Ipsen builds on nearly eight decades of innovation in thermal processing technology, this project reflects a broader commitment to investing in its facilities, products, and people. The Cherry Valley campus serves as
Ipsen’s Global Vacuum Technology Excellence Center. The expanded TITAN assembly area is expected to be fully operational by late July 2026.
ABOUT IPSEN. Ipsen is the global leader in heat-treatment solutions with more than 10,000 operating systems in 70 countries. Through its Global Excellence Centers in Vacuum and Atmosphere Technology, Ipsen delivers innovations that advance thermal processing and help customers achieve their goals. Focused on performance and quality, Ipsen supports commercial heat treaters and customers in many industries including aerospace, automotive, energy and medical. With locations in North America, Europe and Asia, and the largest service team in the industry, Ipsen is committed to providing 360° support for customers worldwide.
Today we are excited to be speaking with “Dennis Beauchesne” of “ECM USA” about “AI” and “Robotics” in the heat treat industry.
We are very pleased to be speaking with Dennis Beauchesne of ECM USA, an individual who we at “The Monty” have known for many years and consider a friend. Dennis obviously we know your background but I am sure our readers would like to know your background and how you ended up in the heat treatment industry and in particular with ECM USA. By the way I just mentioned that we have known each other for years, so I am almost embarrassed to ask what your title is.
Thank you for interviewing me, Gord, for The Monty. I am excited to be with you today and am honored to have the opportunity to speak with you. We met in 2001 and visited with you and your lovely wife, Dale, in Canada when I made our first sales calls in the Toronto area. I am ECM USA’s General Manager and am currently in charge of all sales and support activities for ECM Technologies (Grenoble, France) in North America under their USA subsidiary, located in Wisconsin between Milwaukee and Chicago. My start in the heat treat industry was by a chance meeting as a rep in the Carolinas after my 9 year stint with Despatch Industries, which ended in 1998. I bought a rep firm from Richard Kellenbarger (K&B Thermal) which included a contract with the principal – ECM USA. With his guidance and a huge amount of help from others in the heat treat realm, it has been my home for the last 25 years. I then joined ECM USA as the Sales Manager and direct employee in 2001. My question to you is – what is YOUR title, Gord??
Tell us about ECM USA and ECM Technologies, the background of both companies, the size, sales and what products you offer.
ECM Technologies is our parent company based in Grenoble, France and has been in business since 1924 in many industrial markets and industries, in which it has provided a large quantity of heat processing equipment. Over the years, the company has transitioned from atmosphere furnaces to induction, and now a large volume of the business is vacuum based furnaces. Even though ECM Technologies has large portions of business in other markets, including photovoltaics, semiconductors and vacuum induction systems, your readers would mostly connect ECM with Low Pressure Vacuum Carburizing (LPC or Vacuum Carburizing) systems. With the early successes from this process in Europe, in 1998, they started the subsidiary, ECM USA, in Wisconsin where they started installation of their signature FLEX systems all over North America. These systems are built for high production carburizing with inherent designs to provide ease of start-up and operation and a high level of safety with no flame curtains or a need for endo generators providing a high quality carburized case. These systems also utilize mostly 20 bar high pressure nitrogen gas quenching systems. Today, ECM Technologies is the second largest global vacuum furnace manufacturer with over 700 personnel all over the world.
Earlier this year, “The Monty Heat Treat News” published a list of the 15 Largest Single Location Captive Heat Treaters in North America and the ECM name was very prominent. So prominent in fact that the 3 largest in North America, Ford Sharonville (Ohio), Jatco Mexico, and GKN Driveline (North Carolina) all exclusively have ECM LPC systems – Congratulations! Now tell me why such prominent heat treaters decided on ECM.
Great question and thank you for pointing out these very high quality gear manufacturers as ECM customers. We take pride in surrounding ourselves with these prestigious customers that demand high quality metallurgy and a high level of productivity from their equipment. These customers were not easily convinced by just producing great metallurgy, but also the manufacturing and engineering capabilities needed to be top-notch, the experience that ECM acquired over the years helped to convince them that ECM was their best choice. As I mentioned, with over 700 personnel worldwide, ECM is committed to being close to the customer to support their needs with spare parts and technical support, wherever the customer is based. This was the main reason to open ECM USA and support North America as we have for the last 28 years. These systems, as you mentioned, are producing high quality gearing with 1000’s of parts each day and in some of these vacuum systems for over 25 years. We look forward to supporting them and others for many more years to come.
Each of the examples I mentioned above are using ECM LPC systems, but I know that is not the only product line you offer, can you tell us what are your signature product lines?
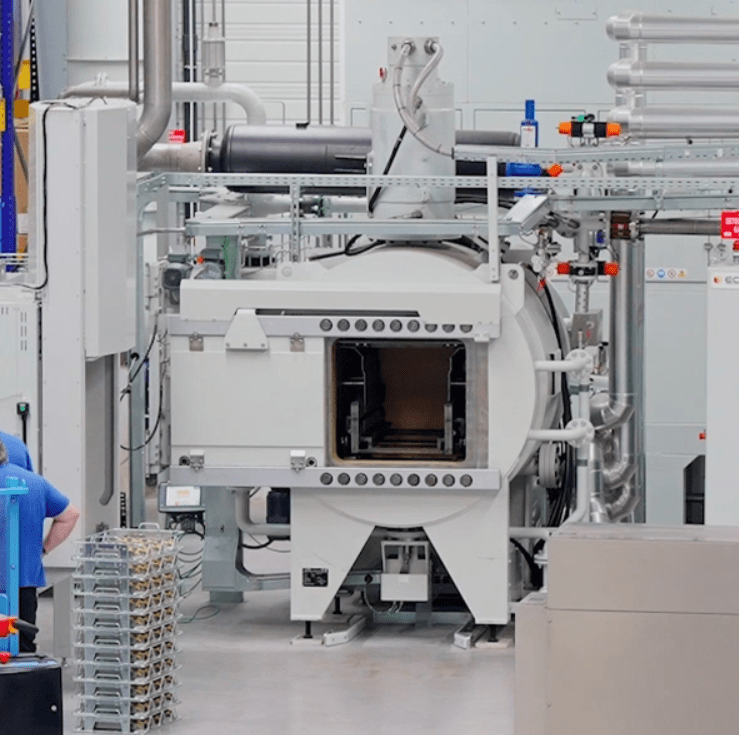
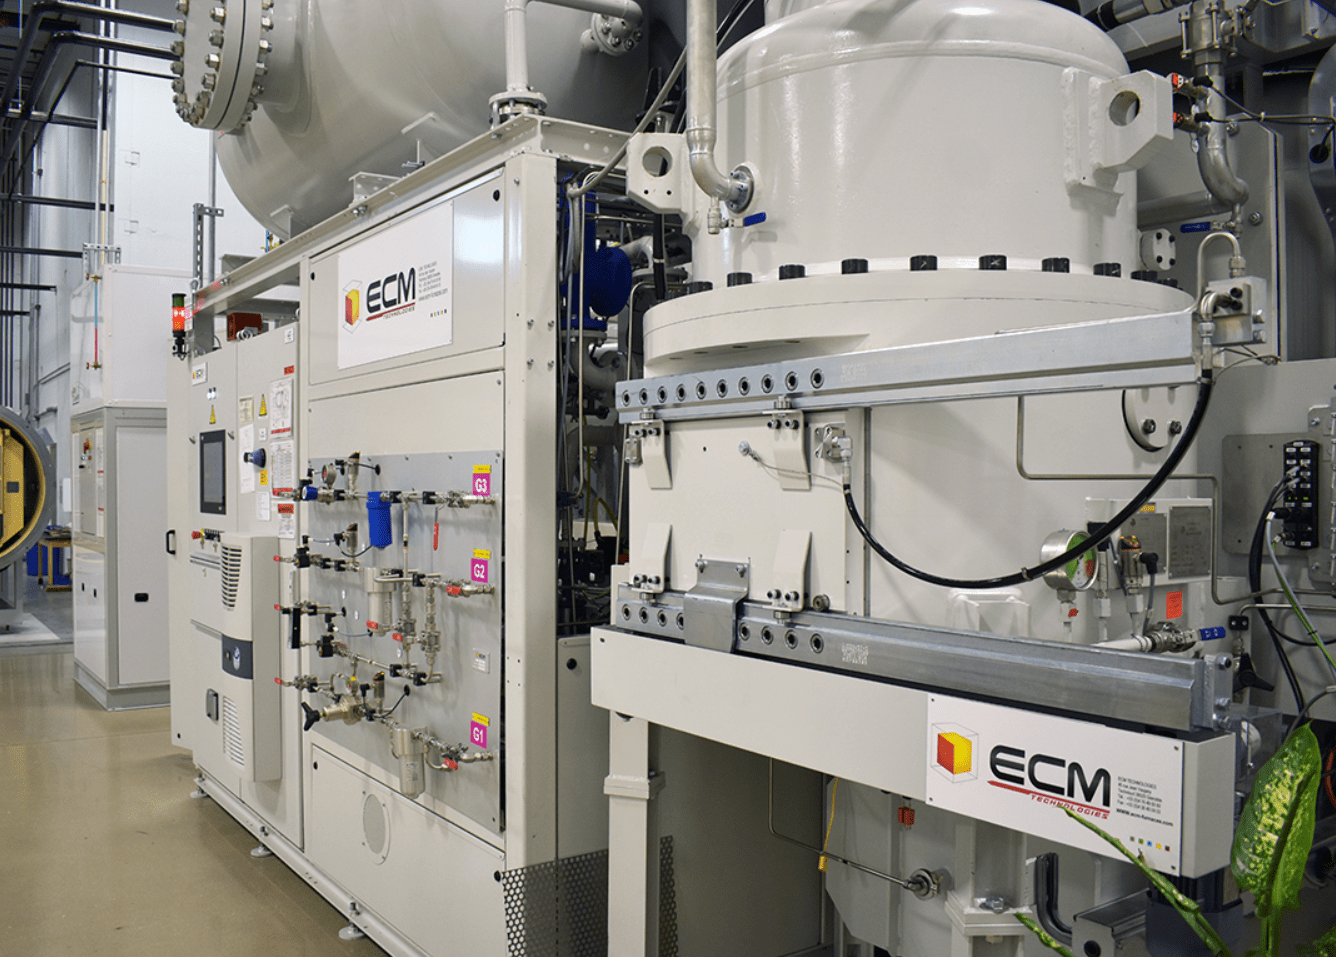
Yes, our signature product is LPC equipment, but it is all based on a modular continuous batch system. We have been manufacturing this product for over 28 years and are still finding new applications for the existing design with only minor modifications. The FLEX, NANO and JUMBO are the main systems of this modular equipment family. These systems are utilized for FNC, sintering, de-gassing, de-binding, hydrogen decrepitation and several other processes. The modular design and the ability to transfer loads under vacuum or partial pressure has a great advantage in the industry where this type of transfer is imperative. Additional equipment we provide is specific for the nuclear industry, such as vacuum induction casting and vacuum induction melting (VIM). The semiconductor industry also relies on our equipment for electrostatic chucks (E-Chucks) and single to multi-wafer processing systems. The product lines are varied, but the one thing that is the same – they are all for high-value and highly precise thermal processing.
Dennis, before we move on from LPC systems I have to say that for many heat treaters ECM is synonymous with the LPC process. Can you tell us how this process evolved and how many systems you have installed around the world?
As some of us may have learned from one of the many presentations given by “The Heat Treat Doctor” Mr. Dan Herring, the Low Pressure Vacuum Carburizing process seems to have evolved in the late 1960’s as a high pressure vacuum carburizing process that ECM eventually tailored into an efficient and highly accurate low pressure process in the early 1990’s. Once this simulation software and process was perfected and proven, several companies lined up for trials and large installations were installed in Europe in the late 1990’s. Since then, we have installed over 400 systems with over 1800 heating cells. And as a highlight, I would like to mention that in 2026 we are happy to celebrate our 500th heating cell installed in North America.
ECM USA is part of a larger global organization; can you explain how the French based ECM Group influences ECM USA and the products offered in the NA market?
ECM Group is our parent organization and is very much a part of ECM USA’s daily lifeline to our product bloodline for technical and manufacturing support. ECM USA represents several of the ECM GROUP brands (Annealsys, Cyberstar, ECM Greentech), and companies (ECM Robotics, SEMCO Technologies) and, of course, ECM Technologies products for sales and service. ECM USA provides marketing, sales and service for all these products in the North American market including any regional input necessary to service our customers.
Recently you provided “The Monty” with an article about AI and robotics in the industry-I recall that you were very passionate on these topics. Currently you find few examples for both in the industry – do you feel that these technologies have advanced enough that it will soon be commonplace to see examples of both in our rather conservative industry? Along the same lines do you feel that there might be some reluctance to integrating technologies which can be perceived as taking jobs away?
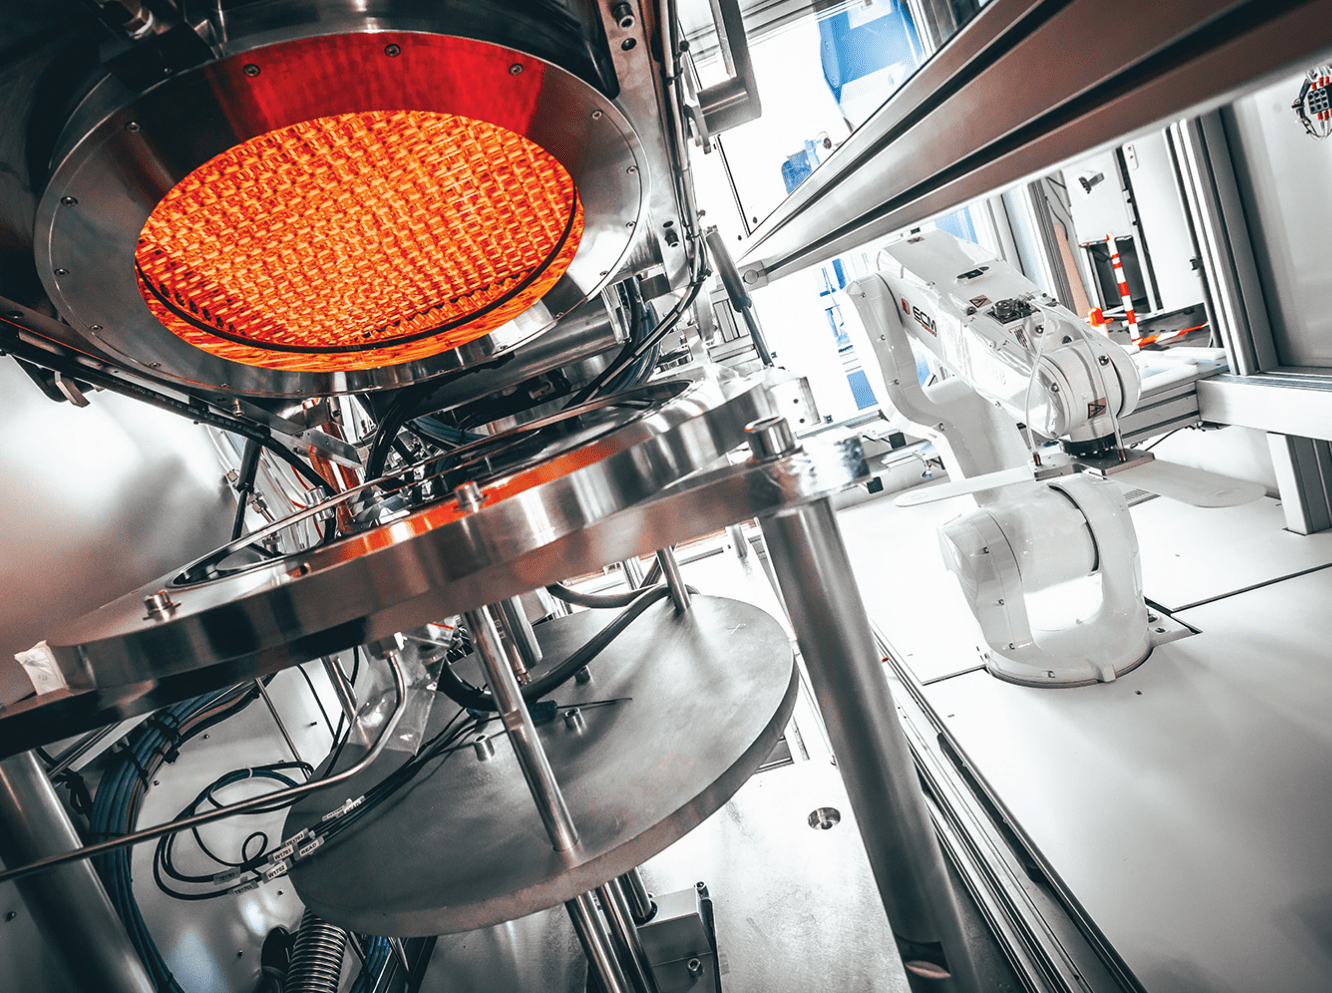
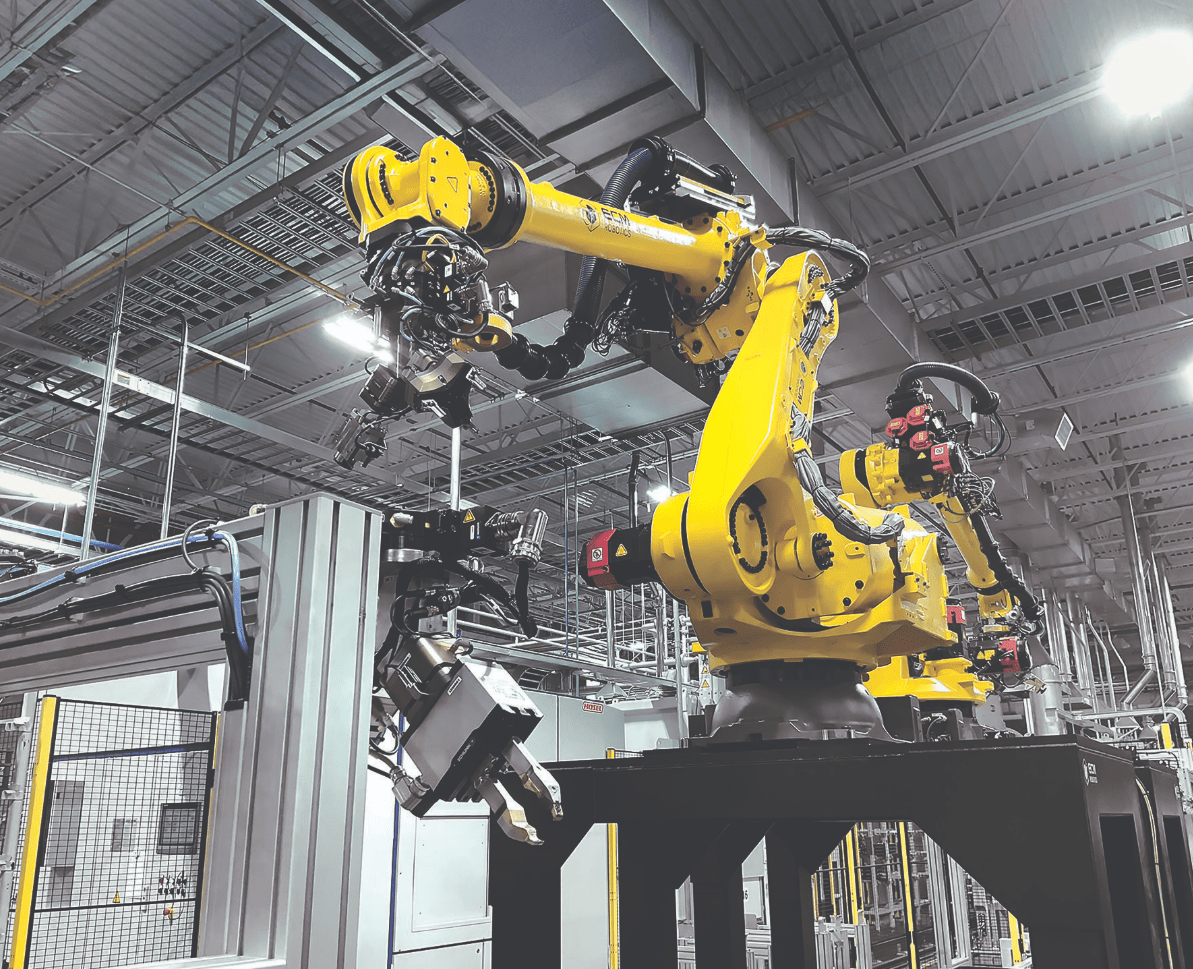
Thanks for mentioning this important evolution in the heat treat industry. It is becoming rarer to see reluctance due to job loss as the reason to avoid these integrations. As we know, finding qualified personnel over the last 5 years has been difficult, so the implementation of AI and robotics has been an aid to those companies trying to fill jobs. I remain passionate and motivated as ECM Robotics has been an on-going part of our offering and has helped several companies implement robotics into their heat treat process. It allows companies to have one supplier integrating automation and heat treat processes into one layout – one production software solution. Interestingly enough, you would think robotics would be used mostly in high production of a large and heavy parts, but in our situation, using the NANO system with a high quantity of parts is more likely the case. We are finding more and more customers preferring to buy robotics packaged with the heat treat furnace systems and we are happy to be able to fulfill that request. In addition, we can also provide robotics for existing furnaces, no matter what brand/models, to automate their processes.
In the previous question I mentioned that the heat treatment industry is rather “conservative”, a statement which I firmly believe to be true. Your offerings, namely modular vacuum systems are a real break from more traditional types of furnaces such as batch IQ furnaces. Why are heat treaters choosing your systems over more technologies that they are more familiar with?
This is a great question and one that more and more heat treaters have wrestled with these days. There are many advantages to the modular systems, including: energy savings, CO2 reduction, higher quality metallurgy, reduced cycle time, production flow, cleaner and safer work environment, floorspace savings, and, above all, a much simpler equipment operation. ECM also has a system that integrates into existing batch IQ (BIQ) lines. The ECO will give you LPC in your existing line by removing an aging BIQ furnace, so all is possible. Another major factor is the reduction of quenching capacity needed as the modular system allows for the use of many heating cells to utilize only one quenching device or to provide both oil and high pressure gas quenching on the same system. More often than not, the main reason is FLEXIBILITY in so many ways. There is also the generational-shift consideration that those familiar with traditional atmosphere carburizing are retiring and a new generation are coming on board who see the benefits of our equipment.
A number of the benefits touted by ECM about your systems revolve around environmental issues such as reduced emissions. Do you think this is a selling point with North American heat treaters? You and I have discussed this in the past and I know our positions are a little different on this question. Personally I don’t believe this is a major consideration with North Americans, but not everybody agrees with me-what are your thoughts?
My thoughts, and what we see from customers, is that most US based customers do not have strict requirements when buying new equipment and reduced emissions. However, more and more pressure is being placed on those doing business with European or large global companies. European companies are now extending their environmental requirements to all part suppliers including those coming from North America. Even smaller heat treaters bidding on parts from European connected suppliers must comply with reducing emissions output. In those situations, it is an important part of their equipment selection. We also see companies that are trying to bring heat treating in-house are choosing cleaner options, such as, a cleaner shop environment and what they exhaust through the roof. As you know, LPC or vacuum carburizing can reduce process CO2 emissions by nearly 90% compared with atmosphere carburizing – with the furnace itself emitting zero. So, yes, in many cases it is a selling point.
How have ECM systems and services paved the way for progressive thinking and advancements in heat treatment?
These systems and services have paved the way by offering a heat treater a much better metallurgical product, along with a workplace that is safer and more flexible than ever before. With the advancement of high pressure gas quenching and gas-quenchable steels, the need for oil quenching has been reduced. Therefore, by eliminating the need for oil, and to replace and clean it up, it has proven to be a huge savings for many heat treat operations. In addition, the ability to automate and be flexible about processes and products has been a huge plus with our systems. In the end, it has definitely changed the mentality of installing a pusher furnace without having the need to provide operational and maintenance support 24/7. The ECM system can be run on a 5 day shift, a single shift or any production schedule without the need for personnel when the equipment is idle. By being idle during holiday vacations, this allows companies to save an enormous amount of energy and labor, as well as, cost savings with alloy fixturing investment.
Per recent ECM advertising, your vacuum furnace technology is “ideal” to replace atmospheric/traditional heat treating technologies – I would suggest that this is a rather “provocative” statement. Can you explain your reasoning on this?
Provocative or not this is what has been happening for the last 28 years! Every major automotive manufacturer has now implemented low pressure vacuum carburizing as their choice for carburizing in North America. Customer after customer that has replaced atmosphere carburizing with LPC has seen an improvement in operational and metallurgical quality. These improvements are just not possible with how atmosphere systems operate. I am not saying that it will replace ALL atmosphere heat treating equipment, but, in most cases, it can. Everyone currently using atmosphere carburizing equipment should take a hard look at low pressure vacuum carburizing and how it can benefit their product and daily operation.
Beyond your technology, what are other factors you can apply to the success of ECM in North America?
We feel that ECM USA can offer a quality, flexible, and reliable product with the support located in Wisconsin. Specifically, within our WI facility is our Synergy Center. This recipe development center can run detailed testing for metallurgical and dimensional data to prove out concepts, metallurgical results and production capacities. Support and maintainability are a huge focus of our US subsidiary. With the feedback we get from our customers, we are able to implement necessary changes to evolve, adapt and improve the ECM Group equipment offering worldwide. We believe great equipment cannot always be great without great support. And that is our goal!
Over the years “The Monty Heat Treat News” has visited and profiled well over 100 captive and commercial heat treaters in Germany, and at the end of the day one of the cleanest, most well organized and modern is “WERZ Vakuum-Wärmebehandlung GmbH & Co.”, based in Gammertingen, Germany.
This family owned firm of over 70 employees focuses only on vacuum heat treating, vacuum nitriding and coatings and the facility is so clean that live potted plants can be seen throughout the plant-which has to be a first.
The company makes our news today because “Werz” recently upgraded an almost 30 year old plasma nitriding system with the one shown in these photos.
Interestingly enough while plasma nitriding is very common in Europe it has never received the same level of popularity in the rest of the world. In North America as an example only a handful of companies have made a go of this technology, most notably “Advanced Heat Treat Corporation” of Waterloo, Iowa.
Dave’s history in the North American heat treat industry go way back to the days of “Lindberg Heat Treating” a commercial heat treater swallowed up by the world’s largest commercial heat treater “Bodycote” quite a few years ago now. Since that time Dave has held a variety of high-level sales positions at Bodycote, most recently as “Vice President Aerospace Sales-North America”.
After over 27 years in the commercial heat-treating industry Dave has made a change and is now Vice President Business Development – Aero Metals Alliance – North America.
About Aero Metals Alliance;Aero Metals Alliance (AMA) provides Aluminum, Stainless Steel, Alloy Steel, Titanium, Nickel Alloys and supply chain management services to the world’s leading aerospace companies. The company operates from fourteen Service Centres in five countries throughout the America, Europe and Asia.
Happy 4th of July! The offices of WG Montgomery Ltd., “The Monty Heat Treat News” will be closed Friday, July 3rd due to the USA July 4th celebration. Regular news items will resume Monday, July 6th.
For this news item we go to Brazil where we see that fastener manufacturer Hassmann S.A has just commissioned a fully automated chamber furnace line (batch IQ to our North American readers) provided by Ipsen of Kleve, Germany-we will let “Ipsen” tell the rest of the story;
“Hassmann S.A: Commissioned. Tested. Producing. Following the successful mechanical installation, the next important milestone has now been reached: the fully automated Ipsen chamber furnace line size M has been commissioned at Hassmann. Commissioning started in May and has been supported by two Ipsen technicians: Lukas Voigt and Jürgen Schnell. Together with the Hassmann team, they brought the system into operation step by step.
This week, the final production monitoring is taking place on site. A strong final step before the line fully moves into regular production. Thank you to everyone involved for your commitment and excellent collaboration.
“Hassmann S.A.” is one of Brazil’s leading fastener manufacturers and supplies customers in the automotive, agricultural, truck and construction machinery sectors, among others. It produces over 40,000 different screws, rivets and custom parts, and exports to more than 25 countries.”
June 29th, 2026 “The Monty Heat Treat News” published our annual list of the “52 Largest North American Commercial Heat Treaters”, a list which included 4 new entries. One which we pointed out earlier was a Texas firm by the name of “Worldwide Heat Treat”-a second new entry is “Grupo “ETSA” of Mexico, a description of which is below.
“Grupo ETSA” (Especialidades Térmicas, S.A.), Mexico; “Grupo ETSA” has 7 plants in Mexico, Guadalajara, Celaya, Aguascalientes, San Juan del Río, and Mexico City. The company is privately owned, Mario Fabian Mendez, President. Typically their operations have heavily focused on automotive and oil components (~85%), with the remaining 15% dedicated to vacuum tooling. However during a recent meeting with Mario he said that the firm is investing in more aerospace work.
“The Czech commercial heat treatment company CZECHmetal s.r.o. has selected SECO/WARWICK technology. The company has purchased a horizontal, two-chamber CaseMaster Evolution vacuum furnace equipped with an oil quenching system and an option for vacuum carburizing.
CZECHmetal is upgrading its Olomouc plant with a custom SECO/WARWICK vacuum furnace to boost production efficiency, precision, and capacity using advanced carburizing technologies.
Project key points: / SECO/WARWICK is installing a custom CaseMaster-D vacuum furnace at CZECHmetal. / The furnace features FineCarb, PreNitLPC, and LPCN technologies. / The system is custom-sized to fit existing plant infrastructure. / It offers improved efficiency, process repeatability, and faster quenching. / The deal highlights the rising demand for vacuum tech in Central Europe.
The system will be installed at the plant in Olomouc and will significantly increase the heat treater’s production capacity. The new furnace will replace an older unit, providing higher efficiency, cleaner processing, and greater repeatability of heat treatment parameters.
The contract with the Czech commercial heat treatment company confirms the growing importance of vacuum technologies in Central Europe.
„The Czech Republic is a very important market for vacuum technologies. We see increasing demand for modern carburizing and hardening processes, particularly in the machinery, automotive and tooling sectors. We are pleased that CZECHmetal is joining the group of our partners in the region. Geographic proximity, ease of communication, and fast service support foster long-term cooperation,” said Maciej Korecki, Vice President of the Vacuum Segment at SECO/WARWICK.
“The system supplied is a two chamber vacuum furnace (CMe-D) equipped with an oil quenching system and the advanced FineCarb vacuum carburizing technology, featuring a custom-designed heating chamber measuring 700 × 1200 × 700 mm (27.6″ × 47.2″ × 27.6″), tailored specifically to the customer’s requirements. As a result, the new furnace can be installed in place of the existing unit without modifying the current plant infrastructure.
The design is based on proven technology, comprising a heating chamber and a charge-loading/unloading vestibule with an oil quench tank. The system enables cooling of the charge in two media – dynamically in an inert gas (1.5 bar abs) above the oil surface, or by immersing the charge directly in the quench oil.”
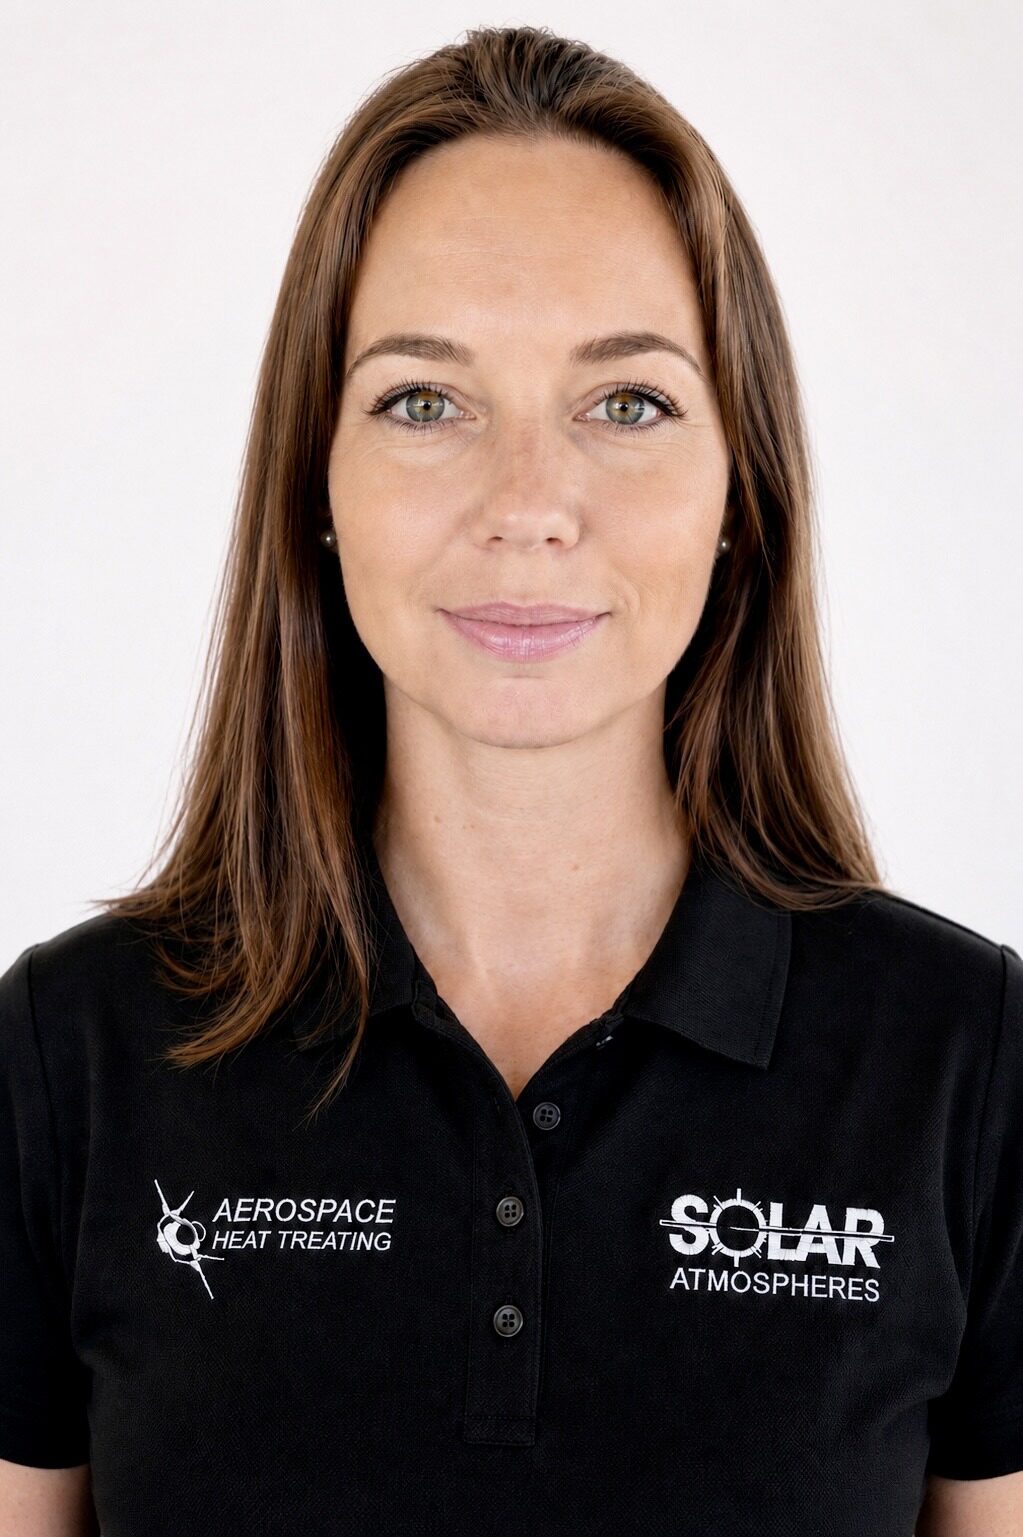
Solar Atmospheres of San Diego, a leading provider of high-performance vacuum heat treating, is pleased to announce the appointment of Karla Clement as the company’s new Quality Manager.
Karla brings a wealth of experience and expertise to this crucial role. Her extensive background in quality management aligns perfectly with Solar Atmospheres’ commitment to excellence and customer satisfaction.
“We are thrilled to welcome Karla to the Solar Atmospheres team,” said Derek Dennis, President. “Her dedication to quality and proven track record will be invaluable as we continue to uphold our high standards.”
Karla will be instrumental in overseeing our quality management systems and ensuring compliance with industry standards. We are very excited to have her on board and look forward to her contributions.
For more information about vacuum heat treating services at Solar Atmospheres, visit solaratm.com, or contact Frank Trujillo at 866-559-5994 ext. 1333, or [email protected].
Tuesday June 30 “The Monty Heat Treat News” will publish our annual list of the 52 largest commercial heat treaters in North America for 2026, the only such list in the world. This year’s list will feature a number of changes as some companies expand, others contract which leads to come firms being removed from our list with others being added.
“Worldwide Heat Treat/Houston, Texas. “Worldwide Heat Treat” in Houston, Texas was founded in July of 2018 by Mr. Robert Gutierrez as a 6,000 square foot facility offering small batch atmosphere heat treating. After a tremendous growth spurt, only doable by a consistent volume of work from our loyal oil and gas customers, the company moved into their current location of 40,000 square feet under roof and added employees to bring our employee count to 32 presently. We now offer some of the largest vertical atmosphere / carburizing capabilities in the USA. We can accommodate up to 90.00″ diameter x 140.00″ long parts in our largest pit furnaces.
We can process up to 38′ long in our car bottom furnaces for various types of heat treat processing. Due to our growth, we have opened a second location, “Worldwide Bor-X” here in Houston this past year. We are currently offering gas nitriding and boronizing up to 72.00″ diameter x 95.00″ long at this current moment in our line of pit furnaces. We will be installing another 2 pit furnaces in the 3rd quarter of 2026 to add to our fleet. This location started off with just 1 employee last year and we are up to 10 employees at this time and we anticipate adding an additional 5 throughout this year. We anticipate opening up several more plants around the USA that offer these types of services. “