Commercial heat treater “Aalberts Surface Technologies” recently appointed “Mr. Mike Harrison”, Director of Operations” for their Livonia, Michigan, USA facility.
Mr. Harrison, brings a great deal of experience to this position, having worked with firms such as “Engineered Heat Treat”, “AFC-Holcroft”, “Gasbarre” and “Atlas Copco”.
Far too often “in house” heat treaters fail to realize that a “great” heat treat department requires constant upgrades in terms of technology and maintenance and become rather complacent when it comes to keeping their equipment up to date-such is certainly not the case with “Snyder Industries” in Tonawanda, NY, USA.
“In 1970, Wayne J. Snyder founded W.J. Snyder Manufacturing in a rented 2,000 sq. foot facility. They supplied their clients with packing glands, rollers, and other miscellaneous machined parts. The W.J. Snyder Manufacturing Company developed a reputation for manufacturing as a reliable source of machined parts with a knack for solving unique machining challenges. This approach led to the introduction of Snyder as a Supplier of wheel units and internal gears for the mining and machining industry.”
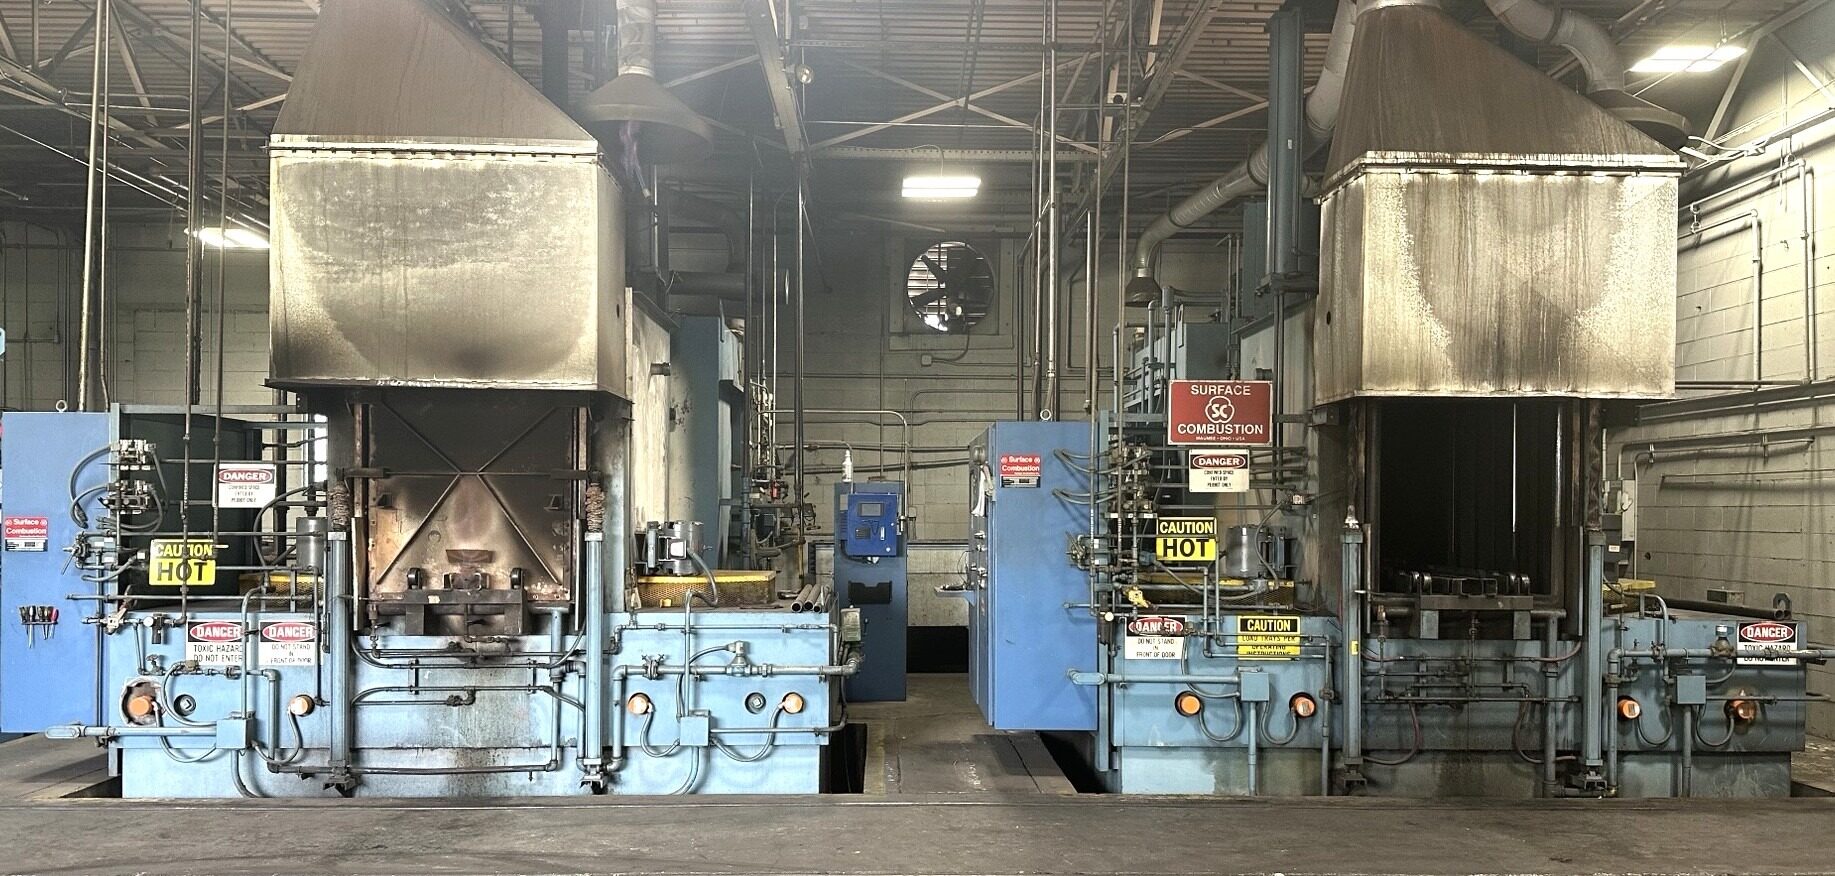
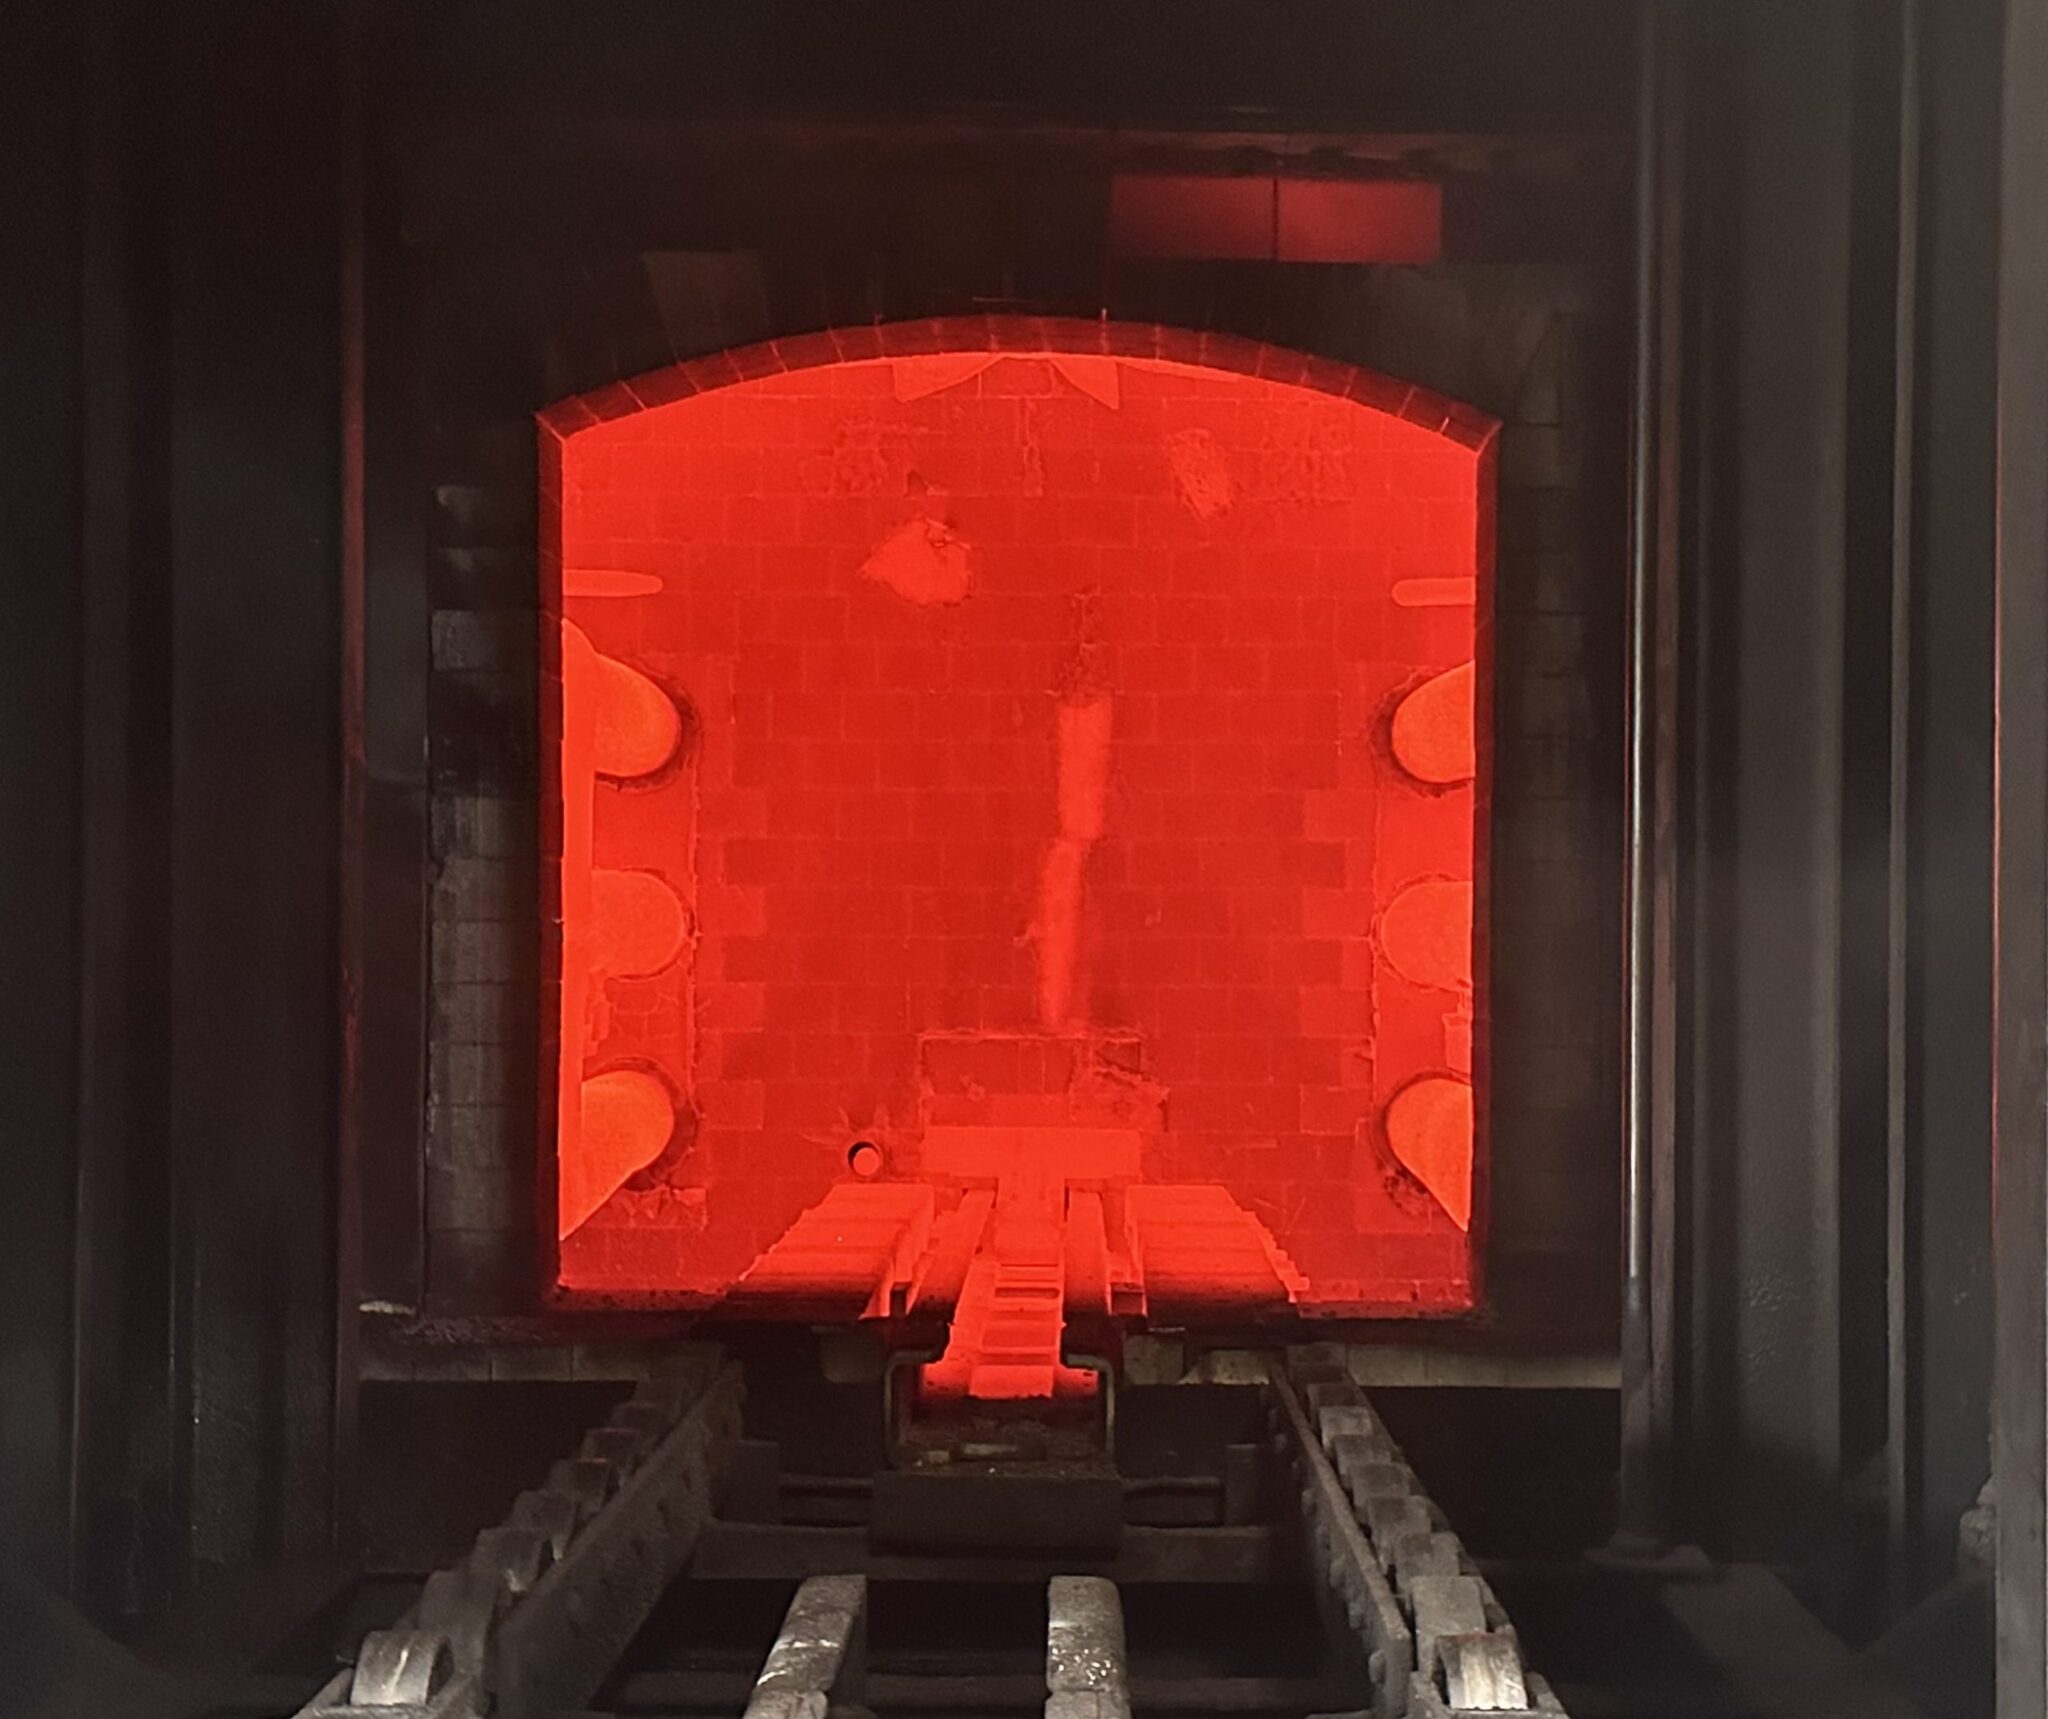
Subsequent to the incorporation of the company it was decided that an in-house heat treat department must be a core competency of the company and consequently in 1992 the first “Surface Combustion” batch IQ furnace was installed, quickly followed by a second which was in turn followed by a number of Induction heating systems and a cryogenic system.
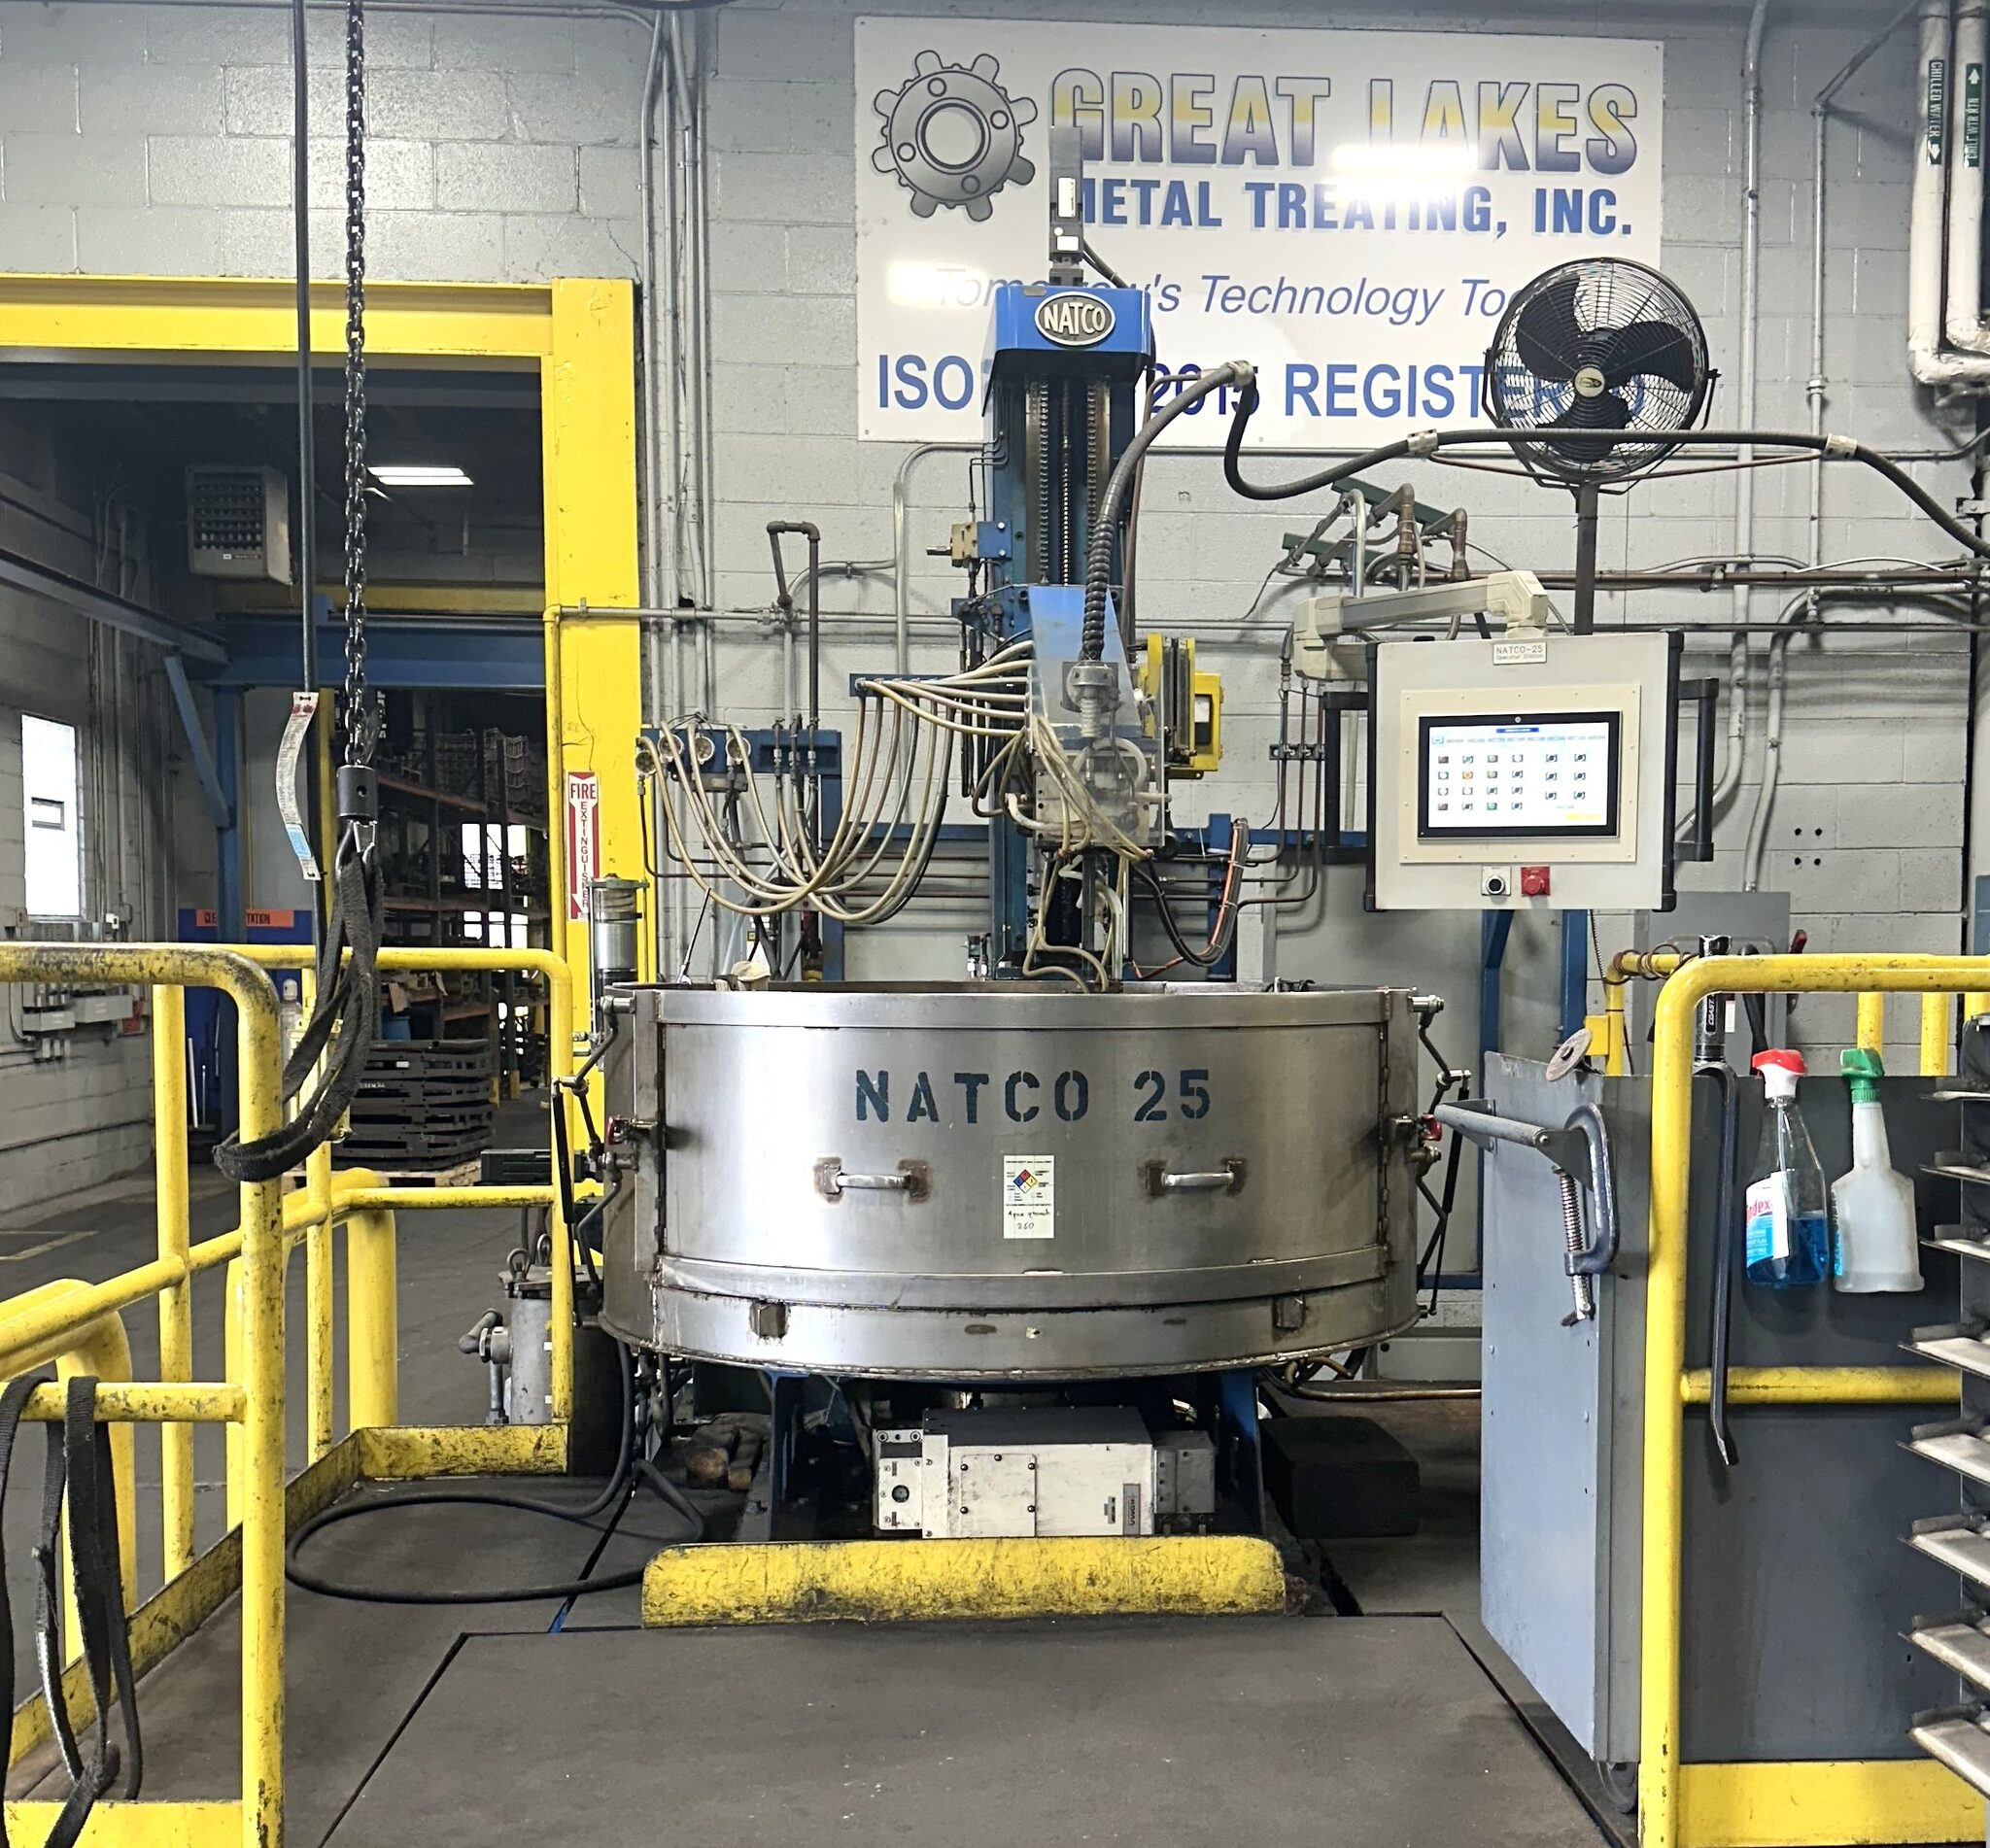
All of this equipment was installed in a separate 30,000 square foot building just down the street from the main manufacturing facility operating under the name “Great Lakes Metal Treating”. While “Great Lakes” is primarily a captive/in-house heat-treating operation, it does offer commercial heat treating to a number of local manufacturers.
Under the direction of two really top-notch individuals, Mr. Rick Rife”, General Manager and “Mr. JT Wilson”, Maintenance Manager, the heat treat department is constantly being upgraded to the latest standards. Very recent investments include complete furnace rebuilds/upgrades by “McLaughlin Furnace Group”(which includes their unique heath design), a brand-new dunk/spray washer also provided by “McLaughlin” and a state-of-the-art probe/IR furnace control system provided by controls company “SSi”.
The induction department is no exception; each of the induction systems has recently undergone software and controls updates, also bringing them up to the latest standards.
None of these investments are cheap, which means the heat treat team requires a great deal of support from top management and this is provided by “Mr. Aaron Bruning”, “Snyder Industries” President who provides whole hearted support to the heat treat division (indeed we would suggest that he has a true affinity for the heat treat department which is rather unusual for company Presidents in our experience).
“Snyder” is a perfect example of a captive heat treat department that receives the support and financial backing from top management that is required to transform an average heat treat department into a really impressive heat treat department.
Left to Right; Rick Rife, General Manager, Great Lakes Metal Treating, Aaron Bruning, President, Snyder Industries, JT Willson, Maintenance Manager, Great Lakes Metal Treating
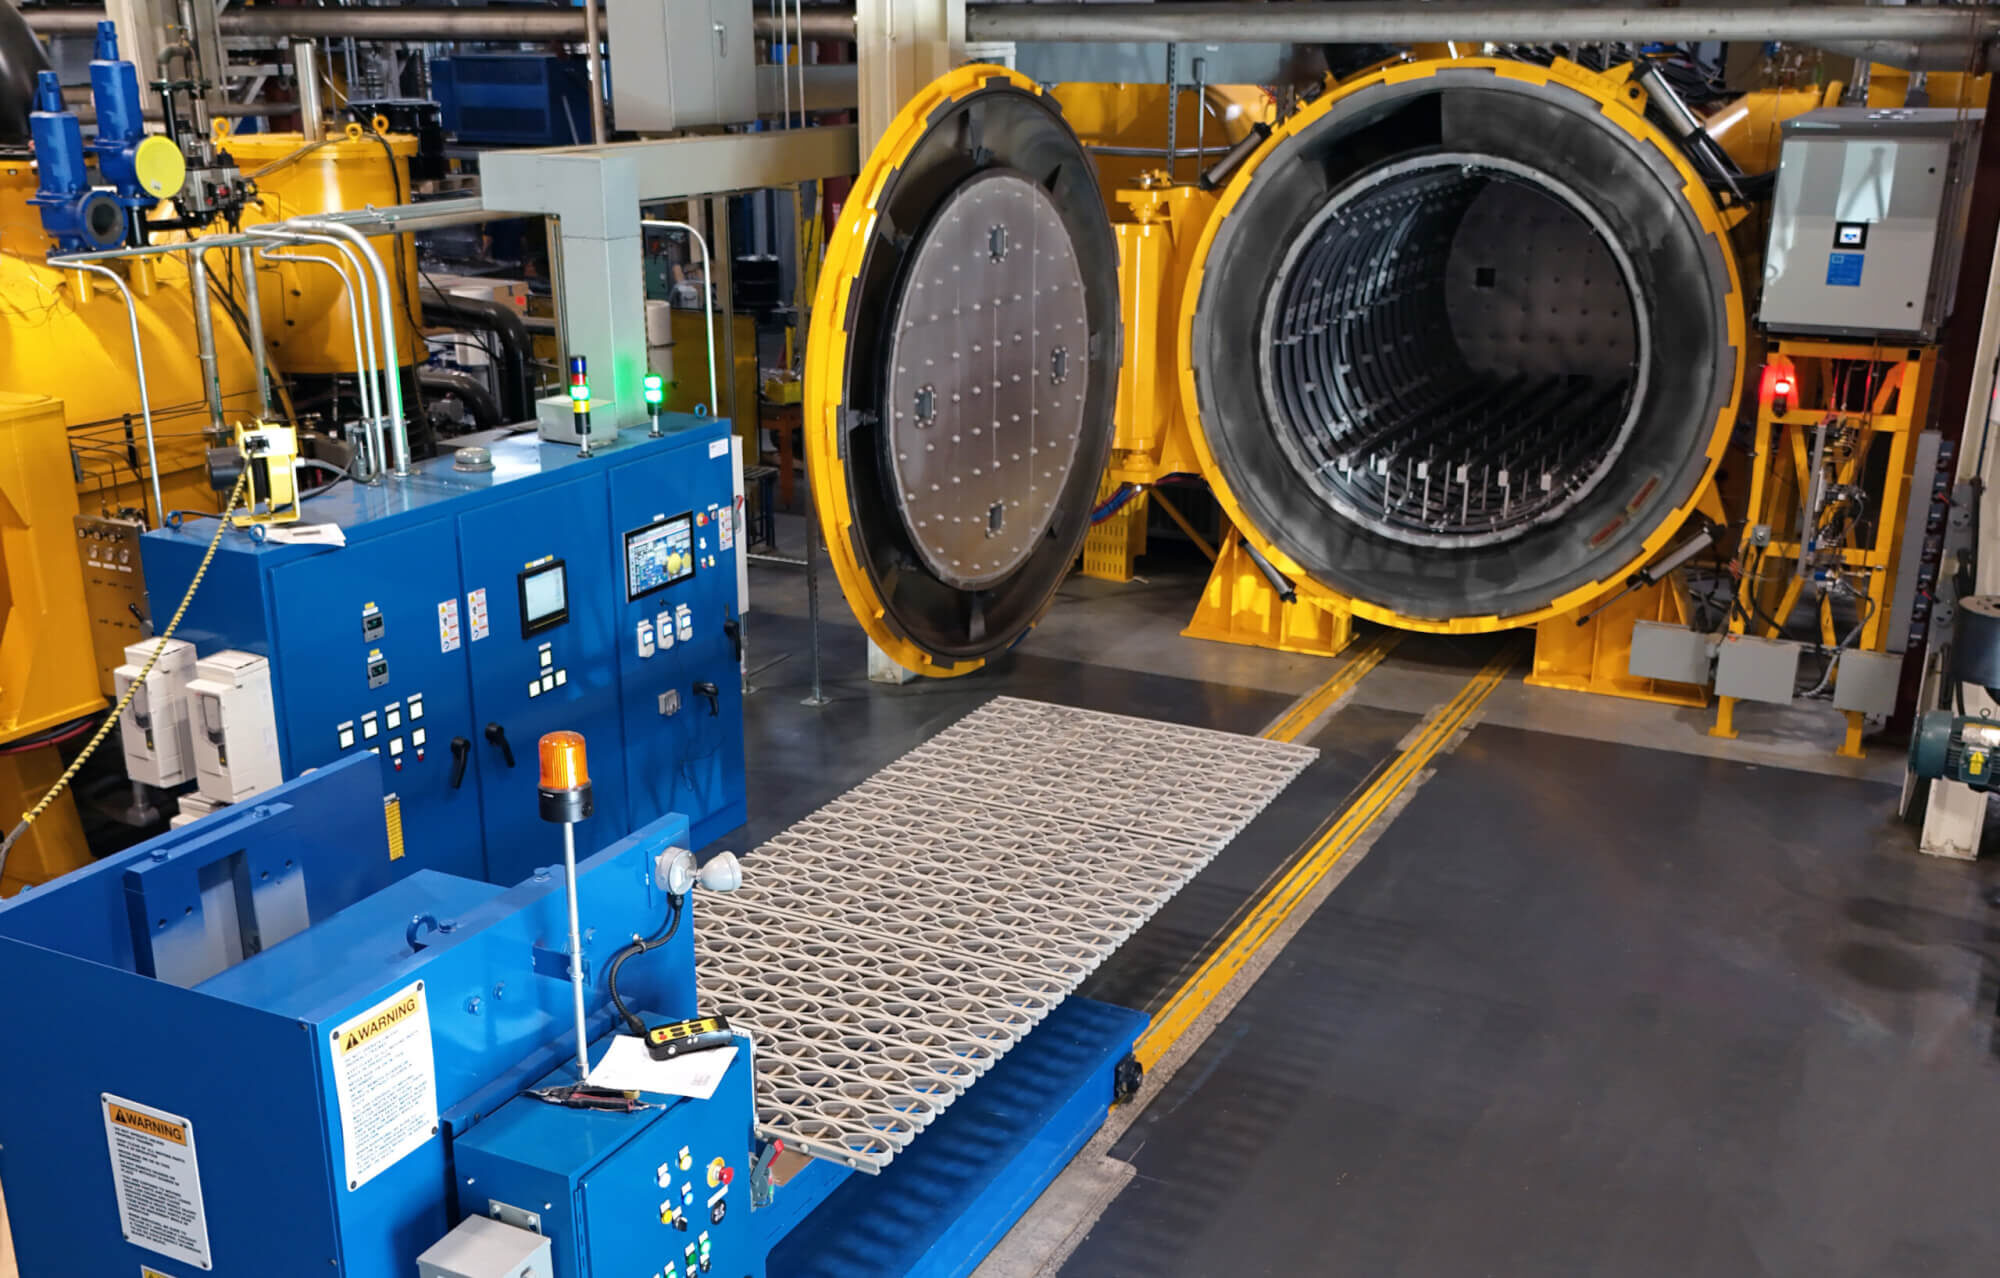
Wall Colmonoy Corporation announces the continued expansion of vacuum heat-treating capabilities with the addition of new Ipsen TITAN H6 vacuum furnaces at its Oklahoma City and Cincinnati facilities. The Oklahoma City location, which manufactures heat exchangers and other components for aerospace and defense, recently installed a second Ipsen TITAN H6 2-bar vacuum furnace. The system features a 36″ x 48″ x 36″ graphite hot zone, 3,000-pound load capacity, operating temperatures up to 2,400 °F, and ±10 °F temperature uniformity. Designed for high-vacuum brazing, the furnace supports consistent processing of critical components while increasing capacity to meet growing demand. This investment builds on a long-standing relationship between Ipsen and Wall Colmonoy. The Oklahoma City team previously installed its first TITAN H6 in 2017. “Due to rapidly increasing stainless steel/nickel alloy heat exchanger core production, we needed to expand high-temperature vacuum brazing capacity,” said John Mars, Vice President/General Manager for Wall Colmonoy, Aerospace and Defense Division. “The location has had an Ipsen TITAN for several years, and we could not be more pleased with the level of customer and field support.” The Oklahoma City expansion is part of a broader effort to strengthen heat-treating and brazing capabilities across Wall Colmonoy’s operations. An order was recently placed for another TITAN H6 for its Cincinnati facility, set to ship this summer. “Wall Colmonoy has been a trusted partner for more than 50 years,” said Ipsen Vice President of Sales Matt Clinite. “These investments demonstrate their commitment to quality, performance, and continued growth in demanding aerospace applications. We’re proud to support their operations with reliable, high-performance vacuum furnace technology.” With nearly 90 years of engineering experience, Wall Colmonoy is known for its materials expertise and long-term customer partnerships. The company continues to develop practical, value-driven solutions that support performance, reliability, and growth across aerospace and industrial applications.
ABOUT IPSEN Ipsen is the global leader in heat-treatment solutions with more than 10,000 operating systems in 70 countries. Through its Global Excellence Centers in Vacuum and Atmosphere Technology, Ipsen delivers innovations that advance thermal processing solutions for customers across commercial heat treating, aerospace, automotive, energy, and medical industries. With locations in North America, Europe, and Asia, and the largest service team in the industry, Ipsen is committed to providing 360° support for customers worldwide.
ABOUT WALL COLMONOY U.S. AEROSPACE & DEFENSE (A&D) DIVISION Wall Colmonoy’s U.S. Aerospace & Defense Division, headquartered in Oklahoma City with operations in Cincinnati, designs, engineers, and manufactures heat exchangers, aircraft exhaust systems, and related components for military, commercial OEM, and MRO markets. Leveraging advanced manufacturing capabilities – including brazing, precision CNC machining, welding, fabrication, and assembly to deliver high-performance solutions tailored to the complex demands of the aerospace and defense industries.
Recently “Gord Montgomery” of “The Monty Heat Treat News” had the opportunity to pose a number of questions to “Mr. Sławomir Woźniak”, CEO of “SECO/WARWICK Group”. The result was this very open, insightful and thoughtful interview;
1) We have been privileged to have had several interviews with SECO/WARWICK over the years, but this is the first of 2026 and I’m sure our readers are interested to know what is new at SECO this year. To start off, I understand this is the 35th anniversary of SECO/WARWICK. Congratulations on this very impressive milestone. Using this as a starting point perhaps you could give us some background, starting with your beginnings back in the early 1990’s in Poland.
“Thank you. The 35th anniversary of SECO/WARWICK is a very important moment for us because it reflects the journey from a small, ambitious engineering company in Poland to a global Group operating across several continents. Our story began at the turn of the 1980s and 1990s, during a period of major economic transformation in Poland. The first vacuum furnace was built under very modest conditions, but it was good enough to attract the interest of the American company, SECO/WARWICK, which at the time was looking for a partner in Eastern Europe. On June 1, 1991, SECO/WARWICK Ltd. was established in Świebodzin, and we consider that the symbolic beginning of our shared history.
This story is also interesting because it brought together two worlds: the American industrial tradition of a brand rooted in the Sunbeam Equipment Corporation and Warwick Furnace Company, and the Polish engineering culture. Over time, that relationship followed a very unusual path. First, the American company entered Poland, and later the Polish company acquired a majority stake in the American business. Today, SECO/WARWICK is a Group with its competence and decision-making center in Poland, but with a global reach.
After 35 years, we can speak not of aspiration, but of position. We have delivered more than 5,000 systems to our partners, employ more than 900 people, and our solutions operate in more than 70 countries. That is a source of pride, but also a responsibility to continue setting the direction for heat treatment and vacuum metallurgy.”
2) The company has made enormous investments over a relatively short period of time; this includes growing your USA facilities, investing in advanced metallurgical technologies and financing your very impressive R & D Development, all of which means money. Perhaps I am being rather forward with this question, but where is the financing coming from?
The financing for our growth comes from several sources. First, from our operating business and the consistently improving results of the Group. The year 2025 showed that SECO/WARWICK generates stable revenue, improves profitability, and effectively builds value based on a global operating model. The Group’s revenue reached PLN 745.9 million, the highest in its history, while EBIT increased to PLN 43.1 million.
Second, we use external financing when it helps accelerate strategic projects. A good example is the financing of Retech Systems LLC’s growth. We secured a long-term USD 10 million loan from the Foreign Expansion Fund managed by PFR TFI. These funds are intended to support the development of metal powder production technology, including the construction and installation of Plasma Gas Atomizer furnaces, as well as the expansion and outfitting of Retech’s production and assembly facility.
Third, an important source of advantage is our organizational model. We are building local manufacturing, service, and engineering capabilities in the U.S., Europe and Asia. This allows us to reduce risks related to logistics, tariffs, labor costs and local market requirements. It also enables us to invest more efficiently and work more closely with our customers.
3) This question is related to the previous one and involves financing. You recently consolidated your USA companies, and I gather you were able to access a program provided by the State of Pennsylvania — can you provide any details about this?
Indeed, in Meadville, we recently invested USD 4 million in the development and expansion of our U.S. facility. This investment is part of the “Made in USA” strategy we have been implementing since 2024. Thanks to this investment, we have significantly increased the Group’s production capabilities for the American market. To support this expansion, the Commonwealth of Pennsylvania awarded our two U.S. Group companies last year a USD 2 million grant package from the Department of Community and Economic Development (DCED) under the Redevelopment Assistance Capital Program (RACP).
This initiated an important process of streamlining our structure in the United States. The merger of SECO/WARWICK Corporation and SECO/VACUUM Technologies into one company, SECO/WARWICK USA, was an important step toward simplifying the organization, reducing administrative costs, and strengthening our position in the North American market. For customers, this means a clearer operating model, better resource use, and greater management efficiency.
As for financing development in the U.S., based on the materials we can currently share, the key element is the long-term USD 10 million loan from the Foreign Expansion Fund managed by PFR TFI, dedicated to our subsidiary Retech. This financing supports the development of Plasma Gas Atomization technology and the expansion of production and assembly capacity in Buffalo.
At this stage, I would prefer not to go into detail about any additional state-level programs beyond what we can officially communicate. What I can say is that the U.S. remains one of our most important markets, and investments in American production capabilities, R&D and vacuum metallurgy are one of the pillars of the Group’s continued growth.
4) I briefly mentioned your R & D Development program, of which I can clearly see you are very proud of. All I know is that this includes three R & D centers, but that is all I know. Could you please elaborate on what form your R & D work takes?
R&D at the SECO/WARWICK Group is not a department detached from the market. It is a very practical part of our business model. We currently operate R&D centers in Poland, the U.S. and China. Their role is not only to develop new technologies, but also to test processes for customers before industrial implementation.
In practice, this means the ability to conduct technological trials using materials and parts supplied by the customer. Among the processes we test are FineCarb low-pressure carburizing (LPC), high-pressure gas quenching (HPGQ), ZeroFlow gas nitriding, ferritic nitrocarburizing, aluminum brazing in a protective atmosphere and in vacuum, as well as processes for equiaxed, directional and single-crystal castings.
In Europe and China, our R&D teams continue to develop CAB technology, where we are a leader in this segment. R&D in CAB focuses on reducing energy consumption, shortening process time, improving the quality of the nitrogen atmosphere, and integrating additional stages, such as thermal degreasing, drying, fluxing, final cooling and internal transport. In practice, this means delivering not a single furnace, but a complete, optimized process that increases control over production and improves the partner’s process reliability.
A very important role is also played by the metallographic laboratory in Świebodzin. That is where we verify microstructure, hardness, case depth, and carbon and nitrogen profiles. In other words, we do not just design the furnace — we scientifically confirm that a given technology will enable the customer to achieve specific properties in the final product.
This is extremely important for our partners because it reduces investment risk. The customer can validate the process, optimize the parameters, and make sure the technology will work in the intended application.
5) Are these R & D efforts taking you into any new technologies or directions that you can share with us? A revolutionary new type of heat treating as an example? Energy savings beyond anything now seen in the market?
Yes, our R&D efforts are taking us in new directions. One of the most important areas is the development of technologies related to specialty materials in the form of metal powders. In the U.S., through Retech, we are developing Plasma Gas Atomization technology that enables the production of advanced metal powders used in aerospace, space and metal 3D printing, among other applications.
This is a highly promising direction because powder metallurgy enables greater efficiency, higher process purity, lower costs, and lower energy consumption in production. For industry, this means both technological and environmental benefits.
The second direction is further digitalization. We use digital twin technology to design, test and implement equipment more predictably, faster and with lower risk. This is especially important for custom-engineered projects, which naturally entail greater project risk.
A third important area is solutions that support energy efficiency and industrial decarbonization. We do not view the green transition solely as a regulatory obligation. For industrial customers, energy savings mean a real cost advantage, higher efficiency, and greater business resilience.
6) Recently I read a press release from SECO/WARWICK in which you mentioned record profits — needless to say it caught my eye. Could you please summarize the press release and more importantly tell us why? In other words, what contributed to such a great year?
The year 2025 was very strong for the SECO/WARWICK Group. Revenue reached PLN 745.9 million, which means 4.6% year-over-year growth and the highest result in the Group’s history. EBIT increased to PLN 43.1 million, up 35.7% year over year, and the EBIT margin rose to 5.8%. Net profit reached PLN 26.1 million, and EPS increased to PLN 3.82.
Several factors were behind this performance. First, organic growth and a better sales mix. Second, the very strong performance of the Aluminum Process segment which became one of the new growth engines. Third, the solid position of the melting furnaces segment which generated revenue of nearly PLN 250 million.
Geographic diversification also played an important role. Europe generated PLN 260 million in revenue and accounted for 35% of the Group’s sales, the U.S. represented 36%, and Asia was the fastest-growing region with year-over-year growth of 25.4%. This shows that our global operating model delivers results.
These results are also the outcome of a consistent strategy: customer proximity, local capabilities, investment in technology, and simplification of the organizational structure. So this was not a one-time success, but the result of many decisions made over several years.
7) I have always considered SECO/WARWICK to have the most diversified product mix of any major furnace builder. You are strong in the vacuum market, well respected when it comes to aluminum heat treat and melting furnaces and have a strong following in atmosphere furnaces to name just a few. This leads to a number of questions including doesn’t this spread your resources too thinly? And second can you say that any of these technologies is your “main focus”?
Indeed, SECO/WARWICK has a very broad portfolio. It includes five key technology areas: vacuum heat treatment, aluminum heat treatment, atmosphere technologies, heat exchanger brazing, and vacuum metallurgy.
We do not see this as dilution, but as strategic diversification. Our customers operate in industries with different investment cycles. Defense, aerospace, automotive, energy, medical, recycling, tooling and aluminum production all have different needs and different development tempos. A broad portfolio allows us to stabilize the business, capture opportunities across segments, and offer customers end-to-end solutions.
Of course, each of these technologies requires specialized expertise. That is why the Group is organized by segment. We do not manage everything from one place as a single, uniform offering. We build centers of competence with their own know-how, engineering teams, and responsibility for developing each area.
Do we have one main focus? We are not focused on a single furnace type, but on advanced heat treatment and metallurgy. We want to be the first-choice company wherever a partner needs quality, process repeatability, reliability, and technology tailored to a specific application.
8) What are your customers asking for these days; let me elaborate on this question before you answer. For instance, I see little interest amongst North American heat treaters for reduced carbon emission technologies which is substantially different I know from European heat treaters. Reduced energy usage is not a major concern for North Americans, again very different than Europeans. However, the increased cost of new furnaces is a major issue for everybody around the world. So what are your customers most concerned about and does this vary by region?
Customer expectations vary by region, but several themes are shared worldwide. The first is investment cost. New furnaces are becoming increasingly advanced technologically and therefore more capital-intensive. As a result, partners expect not only a good purchase price but, above all, a predictable total cost of ownership, a stable process, shorter downtime and effective service support.
The second theme is operational security. After the pandemic, logistics crises and geopolitical changes, our partners pay much closer attention to supply continuity, local capabilities, service availability, and the ability to produce closer to the end market. That is why we continue to develop a model based on local manufacturing and service resources in Europe, the U.S. and Asia.
The third area is energy efficiency. I agree that in Europe this topic is often more strongly linked to climate regulations and CO₂ emission costs, while in North America it is more often viewed through the lens of process economics. But ultimately, all customers want to reduce costs, increase efficiency, and achieve more predictable production.
In Asia, in turn, we see very strong price competition, but at the same time a growing group of customers that want to move to a higher level of quality and export to demanding markets — and that is why they choose premium technologies, exactly the kind SECO/WARWICK offers.
9) I get a real kick out of a recent award that Mr. Slawomir Wozniak CEO received — “Personality of the Year 2025” — what is the story behind this award?
This award is, of course, a personal distinction, but I see it above all as recognition of the work of the entire SECO/WARWICK team. The company’s history and my professional story are closely connected. I started at SECO/WARWICK in 1994 as an electrician intern, later worked as a service engineer, helped build structures in China and India, and today I have the honor of leading the entire Group.
Perhaps that is exactly the perspective that was recognized: the journey from the shop floor and service work to managing an international organization. It gives me a very practical view of the company. I understand the technology, the people, the customers, and the operational challenges because over the years I have seen them from different levels of the organization.
For me, “Personality of the Year” is not an award for media visibility. It is rather a symbol of leadership built on experience, consistency and trust in people. SECO/WARWICK is now a global Group, but its strength still comes from the expertise of specific engineers, technologists, service teams, salespeople and managers. Without them, no leader’s personality would matter.
10) For our final question — in 2026, are you going to be able to beat your very impressive 2025 results?
After a record year, the bar is always set high. I do not want to make statements that would sound like a market promise, but I can say that we are entering 2026 with strong fundamentals.
We have a global presence, a diversified portfolio, growing local capabilities, a strong R&D base, and very clear development directions: vacuum metallurgy, metal powders, energy efficiency, digitalization, automation and the continued strengthening of our presence in the U.S. and Asia.
The goal is not only to “beat the result,” but to maintain the quality of growth. We want to grow profitably, securely, and in a technology-driven way. The year 2025 showed that the strategy works. In 2026, we will continue to execute it consistently, keeping in mind that in our industry, true success is measured not by a single quarter, but by the durability of customer relationships, the effectiveness of implementation, and the resilience of the business in changing market conditions.
Ipsen announces the launch of its newest regional Service HUB, strategically located to support customers throughout Alabama and Georgia. Officially launched in June 2026, the new HUB provides regional customers with a single point of contact for routine maintenance, preventative service, and technical support — helping deliver faster response times from Ipsen’s Field Service Team. The HUB supports customers across major manufacturing regions, including Huntsville and the surrounding aerospace and defense corridor, as well as the Birmingham and Montgomery areas in Alabama and the greater Atlanta region in Georgia. The expansion strengthens Ipsen’s ability to provide localized service and support to thermal processors operating in high-demand manufacturing environments. The Southeast HUB will be overseen by Rodney Strasser, Regional Service Manager for the Southeast. “The Southeast continues to see strong growth across aerospace, defense, and advanced manufacturing,” said Strasser. “Establishing a dedicated regional HUB allows us to stay closer to our customers, improve responsiveness, and provide the level of service and support they need to stay competitive.” Ipsen Service HUB response teams help customers maximize production and reduce downtime by identifying potential issues early and delivering skilled troubleshooting and repair services between scheduled maintenance visits. The HUB model also allows customers to work with familiar technicians who develop a deeper understanding of their equipment, operations, and service history over time. In addition to improving customer support, the HUB structure supports Ipsen’s workforce strategy by enabling technicians to work within dedicated regions, helping improve responsiveness while supporting employee retention and work-life balance. With this latest addition, Ipsen continues to strengthen its national network of localized support, helping thermal processors stay competitive, compliant, and production-ready. Existing Ipsen HUBs serve major regions across the Pacific Northwest, Southern California, Texas, Wisconsin, Illinois, Michigan, Indiana, Ohio, Kentucky, Virginia, North Carolina, and South Carolina. Additional HUB expansions are planned as Ipsen continues investing in regional service capabilities across North America.
“June 1, 2026, Souderton, PA – Solar Atmospheres Eastern PA facility recently commissioned a new 12′ horizontal vacuum furnace. The furnace was designed primarily for Hydriding and Dehydriding (HDH) of titanium. The furnace can also perform the standard gamut of heat-treating processes typical of Solar’s extensive customer base. The furnace features a working zone of 54″ x 54″ x 144″. It is equipped with a 15,000-pound conventional load car arrangement. Other features include a 300HP external forced cooling system with VFD control, Solar Manufacturing’s Polaris control system, and dual mechanical pumping systems.
“This new furnace adds much-needed capacity to support growing HDH demands” states Mike Moyer, Vice President of Sales. “With dual mechanical pumping systems, we are able to more efficiently process larger degas loads and improve our delivery metrics”. “The new 12-foot furnace is also well equipped for all the standard vacuum heat treating process that we currently employ. From annealing and stress relieving to solution treating and aging, the new furnace adds considerable capacity to meet customers’ growing demands.”
“SECO/WARWICK will deliver a Vector single chamber vacuum furnace equipped with the FineCarb option and low pressure carburizing (LPC) to Treatnorte, a commercial heat treatment company The Vector furnace ordered will serve both the Portuguese and Spanish markets and will be used for tool steel heat treatment.
This is one of the two SECO/WARWICK vacuum furnaces ordered by Treatnorte.The delivery represents an important step in developing local industrial infrastructure for advanced metal heat treatment technologies.
FineCarb – Where Precision Matters; The furnace joining Treatnorte’s machine park is a medium size system from the SECO/WARWICK vacuum furnace family, configured to provide the heat treater with the broadest possible process range and high production flexibility.
The round heating chamber allows processing of relatively large parts, while the combination of high-pressure gas quenching (HPGQ) up to 15 bar abs with dedicated low-pressure carburizing (LPC) technology enables complete process cycles for a wide range of steels used by Treatnorte’s customers. The furnace design ensures excellent temperature uniformity, convection heating at lower temperatures, and directional cooling, enabling optimal control of quenching processes for complex and demanding geometries.
The key advantage of this solution is FineCarb technology, which changes how carburizing is perceived in modern commercial heat-treatment shops. FineCarb is a low‑pressure carburizing process carried out in a vacuum atmosphere, where carbon introduction is precisely controlled through successive pulses of carbon‑bearing gases. Unlike traditional endothermic gas carburizing, this process takes place under controlled vacuum conditions ensuring superior process quality and cleanliness.
As a result, uniform and repeatable carburized layers are achieved, while total cycle time is reduced and part distortion is minimized.
“FineCarb enables precise shaping of the carbon content profile in the carburized layer, translating into optimal performance of components requiring high precision, such as gears, shafts, or pins. An additional advantage is the environmental aspect, as the absence of an open flame and the reduced amount of process gases make this method more environmentally friendly than traditional carburizing technologies. Treatnorte’s investment fits perfectly into the broader trend of modernization in the European commercial heat treatment sector. Vacuum technology and low-pressure carburizing is no longer reserved exclusively for the largest industrial plants and is becoming accessible to fast‑growing regional players. Until now, Portugal has not been widely associated with LPC technology, and the implementation of a Vector furnace with FineCarb may become an important reference point for the entire Iberian market. For SECO/WARWICK, the key is not only delivering the furnace, but above all supporting our Partner in building new technological competencies,” said Maciej Korecki, Vice President of the Vacuum Segment at SECO/WARWICK Group.
In the configuration prepared for Treatnorte, the vacuum furnace is additionally equipped with PreNitLPC pre‑nitriding technology, expanding the range of available processes and allowing the surface layer structure to be tailored to the requirements of different industries. This enables a single furnace to handle both classic precision mechanical components, tooling and stamping parts, as well as components requiring high fatigue strength for the automotive industry.
“From the very beginning, cooperation with Treatnorte has been based on a partnership approach. The customer clearly defined their expectations and the need to enter the vacuum heat treatment segment to fulfill a new contract for a complete product requiring vacuum hardening. Selecting a furnace with a broad package of options is an optimal solution, as it creates further potential for expanding the service portfolio,” emphasizes Paweł Okińczyc, Sales Manager at SECO/WARWICK.
Heat Treatment on the Iberian Peninsula; Treatnorte, headquartered in Celorico de Basto in northern Portugal, has been operating on the market since 2021, and in a short time, has built a position as an ambitious, technology-oriented partner for industries such as precision mechanics and automotive. The company invests in the development of its technological capabilities through the InovMetalTreat project co‑financed by European Union funds, aimed at building a modern machine park and expanding advanced heat treatment services.
The new SECO/WARWICK vacuum furnace is a key element of this strategy; “The ability to independently perform vacuum hardening and carburizing processes significantly increases operational independence, shortens the supply chain, and allows for better quality control. FineCarb technology, combined with 15‑bar gas quenching, opens up opportunities for Treatnorte to win more demanding projects for customers in Portugal and Spain,” said Nuno Carvalho from Treatnorte | Tratamentos Térmicos do Norte.
The introduction of advanced vacuum technology for low-pressure carburizing demonstrates that local service providers are ready to compete with Europe’s largest industrial centers on quality and technology. For SECO/WARWICK, this is further proof that proven solutions from the Vector vacuum furnace family, when properly configured, can become a catalyst for the development of local markets, elevating them to a higher level of technological advancement.”
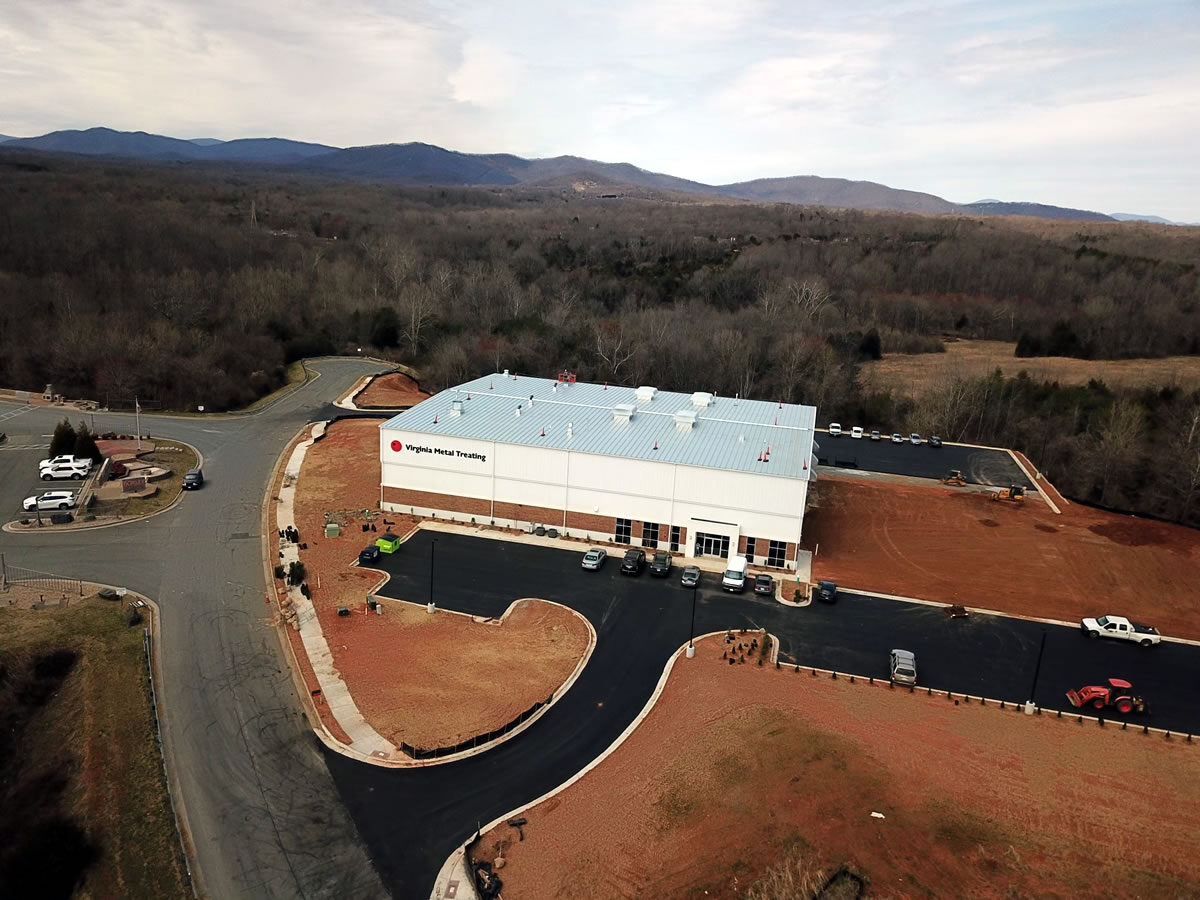
“East Carolina Metal Treating, Inc.” (dba Virginia Metal Treating (VMT) has broken ground on their 20,000 square foot addition to their existing facility in Lynchburg, Virginia. The expansion will include a significant investment of new equipment from Surface Combustion. This includes an additional integral quench furnace (36″ x 36″ x 48″), an aluminum quench furnace (36″ x 36″ x 48″), temper furnaces, and applicable accessory equipment. The expansion is expected to be complete with the equipment operational by January 2027.
We will be seeking Nadcap accreditation, already achieved at the company’s sister facility (East Carolina Metal Treating) in Raleigh, North Carolina. The expansion will enhance VMT’s capabilities specifically within the aerospace and defense industry. The addition of aluminum heat treating capabilities supports the company’s goal of becoming a single-source provider for customers requiring high-quality, fast, and dependable heat treatment solutions.”
For more on this growing heat treat facility we would recommend these exclusive stories from “The Monty Heat Treat News”
Each and every year “The Monty Heat Treat News” puts together an industry exclusive, a list of the 52 largest commercial heat treaters in North America (the 2025 list can be found at “52 Largest North American Commercial Heat Treaters 2025″). Our 2026 list will be published in the near future and we will be seeing some changes-this is one of the changes. “Worldwide Heat Treat” in Houston, Texas has been growing steadily over the years, recently the firm landed their largest order ever catapulting the company into the “Top 52” in 2026. Read the company’s history below as written by the owner, “Mr. Robert Gutirrez” and stay tuned for our 2026 list.
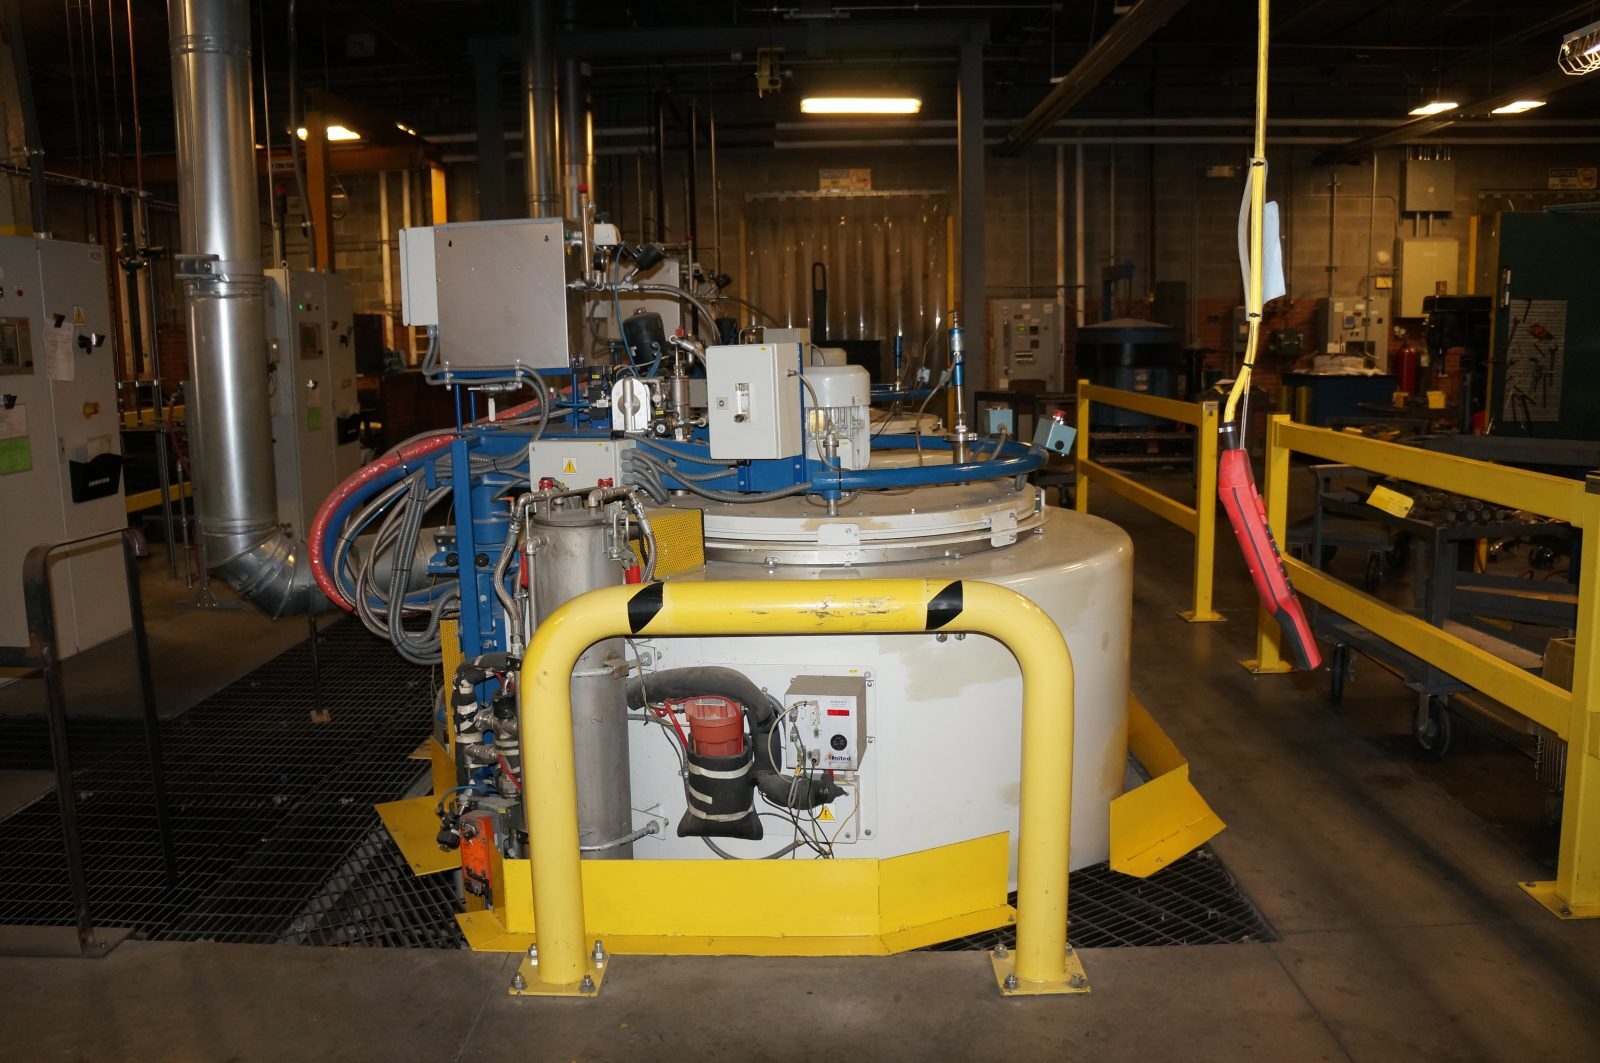
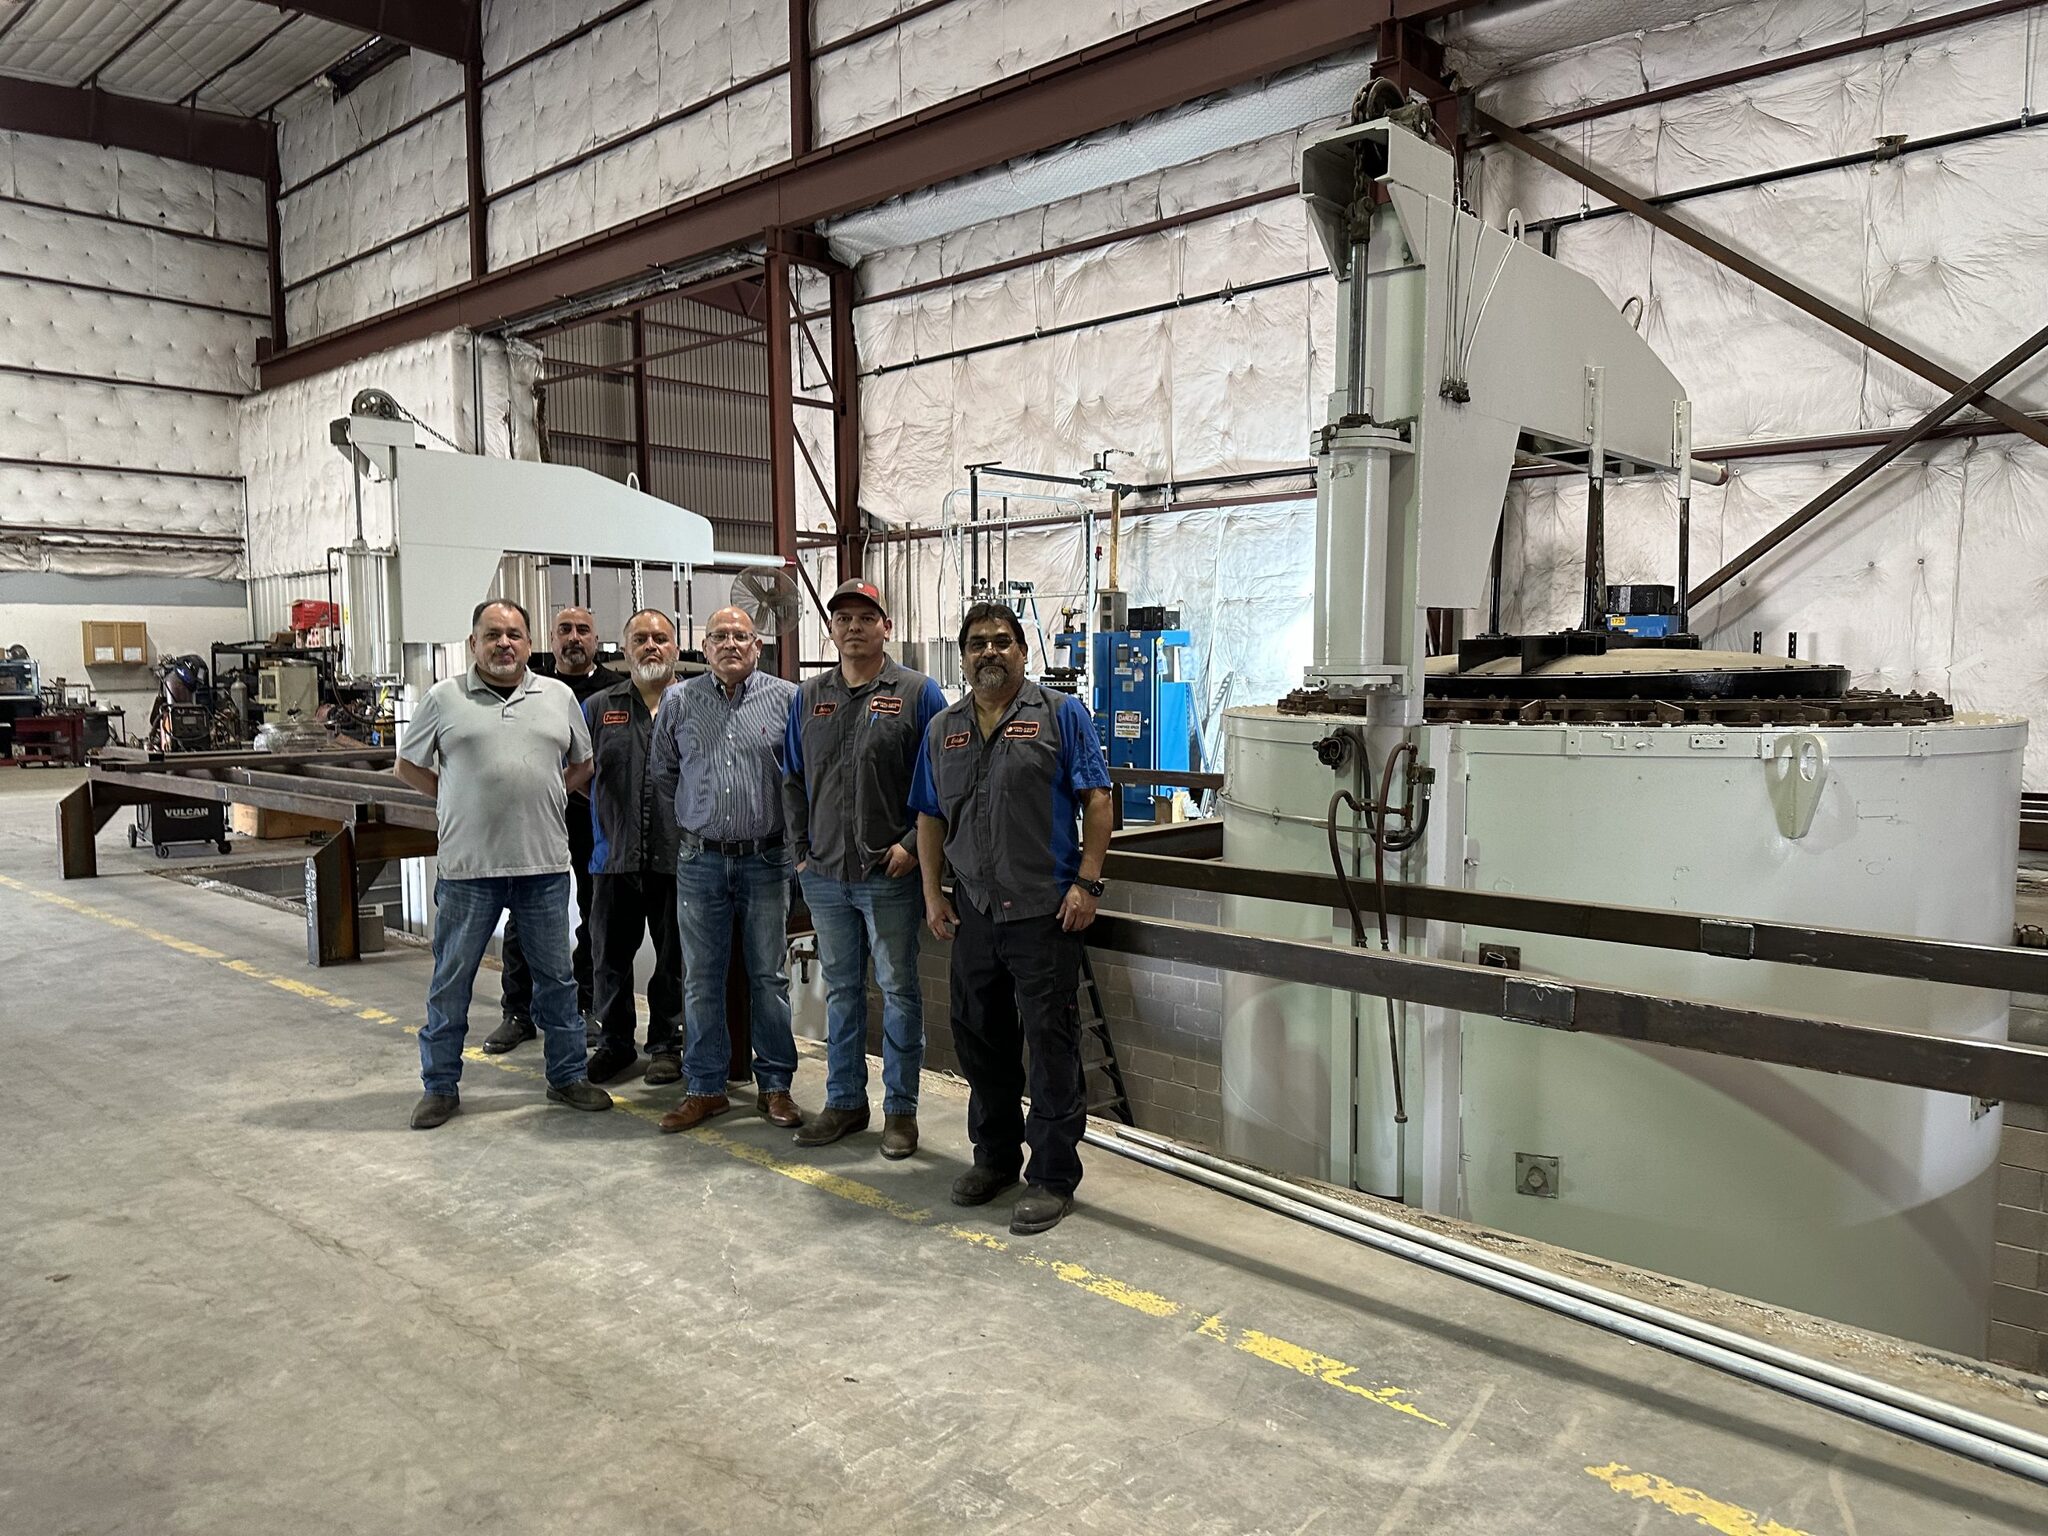
“Worldwide Heat Treat was started up in July of 2018 in our humble beginning’s location of 6,000 square feet with just 2 employees at that time offering small batch atmosphere heat treating. After a tremendous growth spurt, only doable by a consistent volume of work from our loyal Oil and gas customers, We moved into our current location of 40,000 square feet under roof an a additional 30,000 square feet of outside storage space to store additional green work and added employees to bring up our employee count to 32 presently. We moved into this location in winter of 2023 and haven’t looked back. Since that time our heat treat services have broadened quite a bit. We now offer some of the largest vertical atmosphere / carburizing capabilities in the USA. We can accommodate up to 90.00″ diameter x 140.00” long parts in our largest pit furnaces.
By doing so our customer base has grown such as processing large gears for sugar mills, oil and gas drilling gears, heavy machinery gears and various types of down hole mandrels. We are now servicing the aero-space and USA government companies thru-out the USA such as the fuel cells for SpaceX. Our customers come as far as Singapore, Mexico, Canada and all thru-out the USA.
We can process up to 38′ long in our car bottom furnaces for various types of heat treat processing. Worldwide Heat Treat in my eyes has the best staff around and we will only to continue to grow in the future. I can say this we have already out-grown this place and will be needing to buy-out one of our competitors to gain more space or build another location.
Due to our growth, we have opened up a second location Worldwide Bor-X here in Houston this past year. We are currently offering Gas Nitriding and Boronizing up to 72.00″ diameter x 95.00″ long at this current moment in our line of pit furnaces. We will be installing another 2 pit furnaces in the 3rd quarter of this year to add to our fleet. This plant is growing as well at a tremendous rate as we grow our capabilities. Our customers can fill the units faster than we can install them. This location started off with just 1 employee last year and we are up to 10 employees at this time and we anticipate to add an additional 5 throughout this year. I cannot discuss it much due to my non-disclosure but as you know I have been in the industry for more than 40 years now and I recently signed off on the largest customer contract in my life time. Times are great and only getting better. I anticipate on opening up several more plants around the USA that offer this type of services. Sincerely, Robert Gutierrez, President, Worldwide Heat Treat, Worldwide Bor-X, 12249 B Northwoods Park Drive, Houston, Texas 77041″
(Background Information; vacuum furnace builder TAV, the subject of this press release is one of the largest in the world. To find out the background of the company and where they are going we would suggest this exclusive article “Vacuum Furnace Builder Promotes Sales & Strategic Marketing Director”)
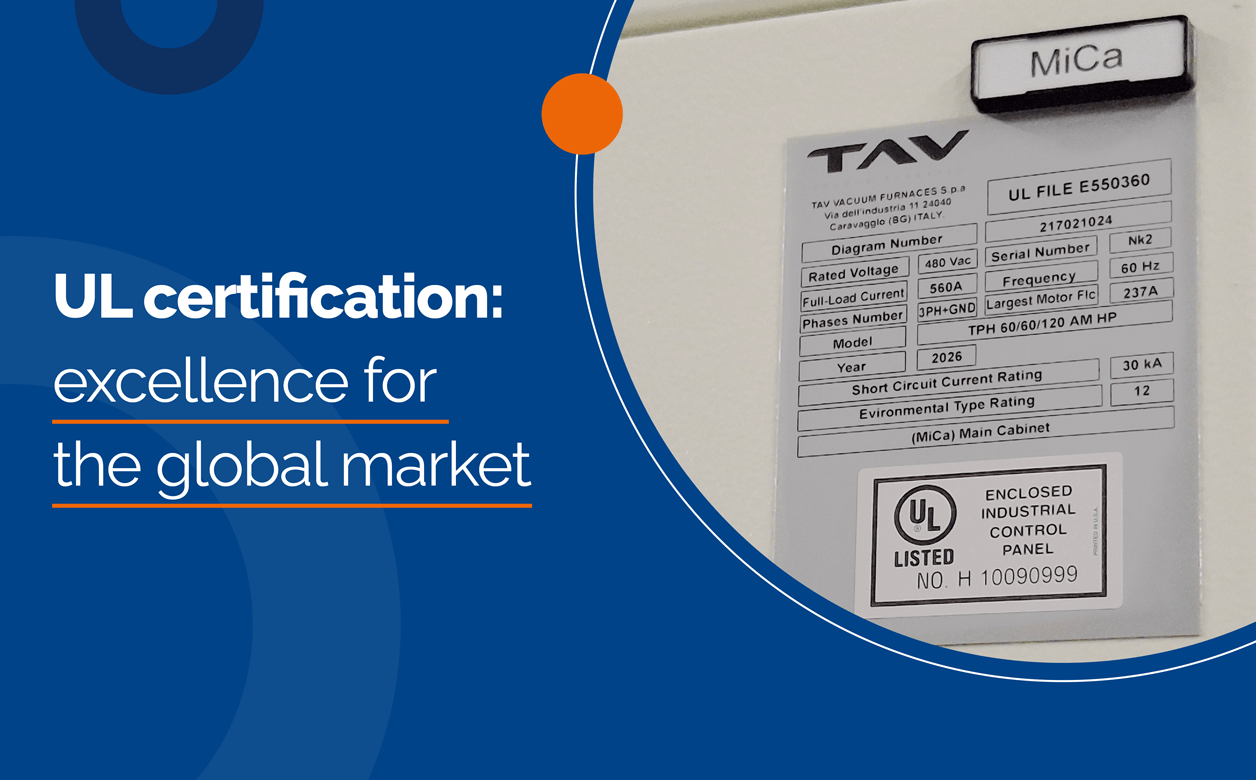
“In an industrial landscape where reliability is not merely an added value, but the beating heart of every successful project, TAV takes a new, decisive step towards excellence. We are proud to announce that we have obtained UL (Underwriters Laboratories) certification: not just a simple mark, but an international recognition that attests to our role as a cutting-edge technology partner for the US and Canadian markets.
The UL mark represents the world’s most rigorous safety standard for electrical and electronic systems. In North America, compliance with these protocols is subject to extremely stringent checks: the absence of the mark gives the local inspector (AHJ – Authority Having Jurisdiction) the power to block the installation of a system, triggering unforeseen costs and bureaucratic delays.
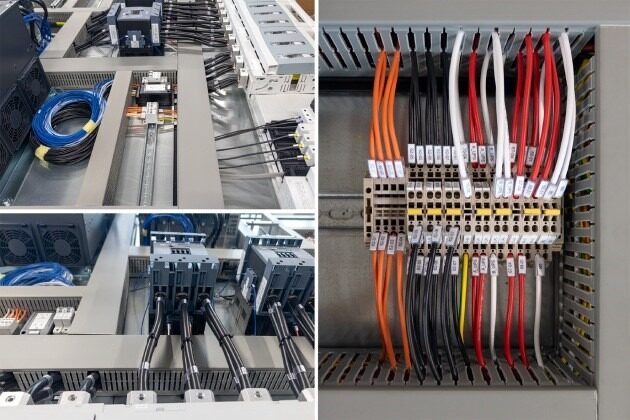
Thanks to this achievement, TAV has brought the certification process in-house. Today, we are able to design, manufacture and certify the electrical control panels for our furnaces directly at our headquarters, guaranteeing ‘plug-and-play’ products ready for immediate operation overseas.
Innovation and Safety: the DNA of a reliable partner; Achieving UL certification is not an end in itself, but tangible proof of our commitment to ongoing technological research. This achievement stems from the high level of specialization of our technical team, which has acquired the necessary expertise to manage the entire lifecycle of electrical safety. Integrating UL certification into our corporate ecosystem, which already boasts ISO 14001 (environmental), ISO 45001 (occupational health and safety) and ISO 9001 (quality) standards, reinforces our vision of safe, sustainable and cutting-edge engineering.
We oversee the entire production chain to offer not just machinery, but complete engineering solutions, where quality is certified in every single component.
Competitive advantages for our customers; Choosing a UL-certified partner means turning regulatory compliance into an economic and operational advantage.
Speed and Cost Efficiency: We eliminate the need for ‘Field Evaluation’ (post-installation inspection). The customer receives a machine that is already approved, eliminating uncertainty regarding start-up times.
Maximum Reliability: Every component is strictly ‘UL-listed’. We implement an architecture with high reliability standards to ensure operational continuity and drastically reduce the incidence of faults.
Agility in After-Sales: our accreditation as certifiers enables us to manage every technical update in-house. This allows us to intervene directly for modifications or updates, certifying the control panel internally without having to wait for external experts. Less red tape, more productivity.
Conclusions; With UL certification, TAV reaffirms its mission: we do not simply sell industrial furnaces but provide the peace of mind that comes with engineering excellence. We are the partner that supports companies on their path to internationalization, breaking down technological barriers through the power of innovation and safety.